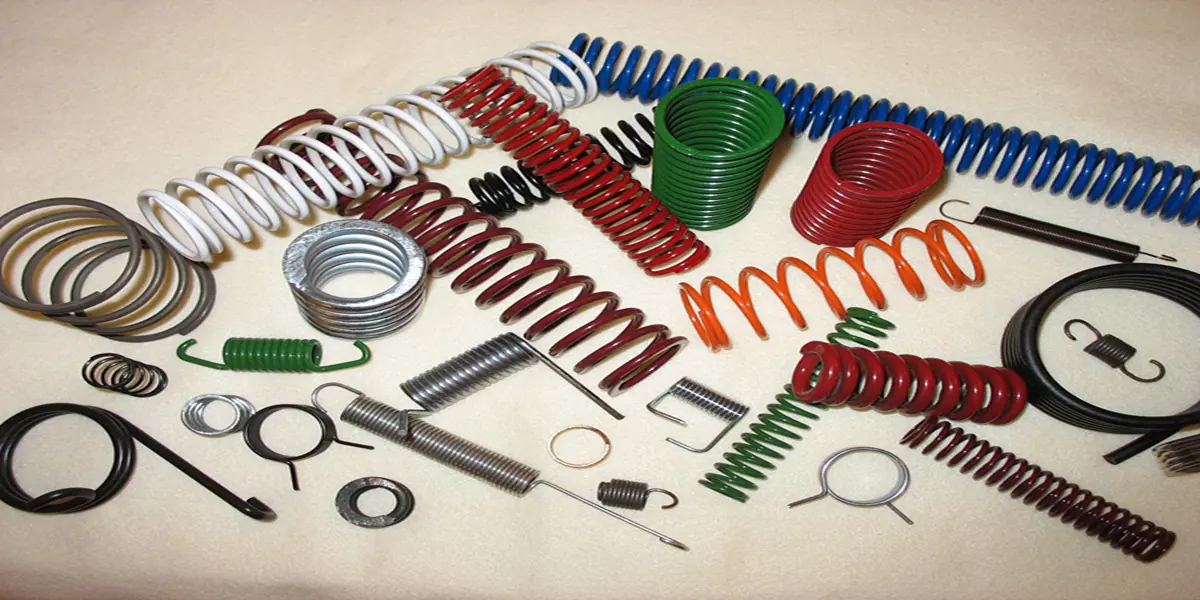
Xinshunyan coils, forms and finishes torsion, tension, compression, flat and wire form springs for appliance, automotive, electronics and fitness manufacturers. Send a drawing or a sample and get a quoted, inspected part.
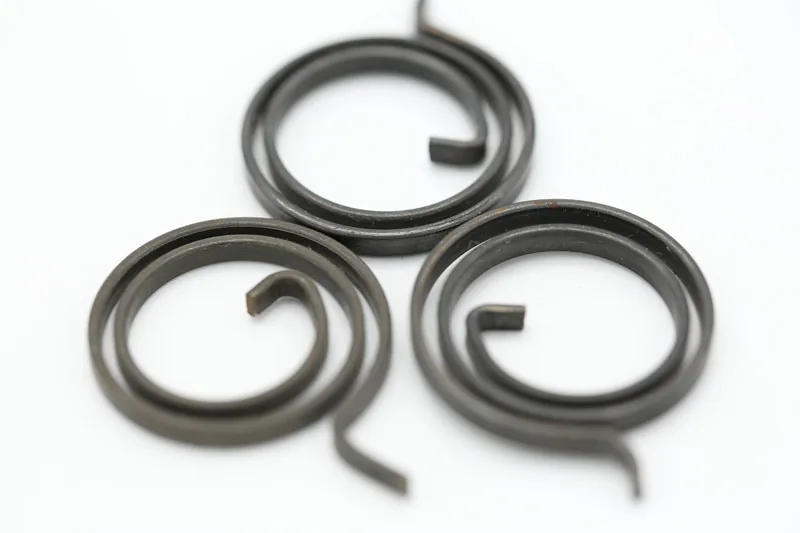
Torsion springs, extension springs, compression springs, flat springs, wire forms, clips and hooks come off the same floor, so one purchase order and one inspection standard cover the whole assembly.
Fully automatic CNC spring machines from Taiwan and Japan hold the geometry. Tensile strength testers and magnetic powder flaw detectors confirm it before the parts are packed.
Every part below is wound, formed, heat treated and finished in our own plant in Xiamen, which is why one purchase order can cover every spring in your assembly.
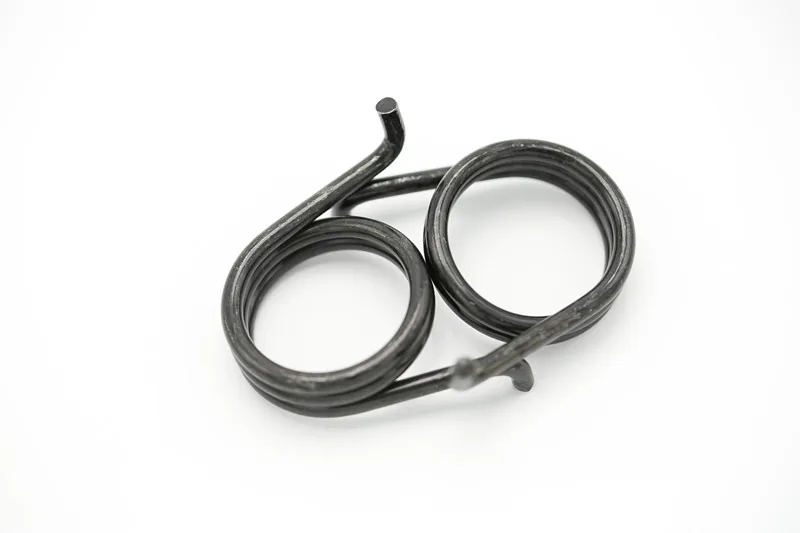
Torque delivered through an angle, not a stroke
16 catalogued parts
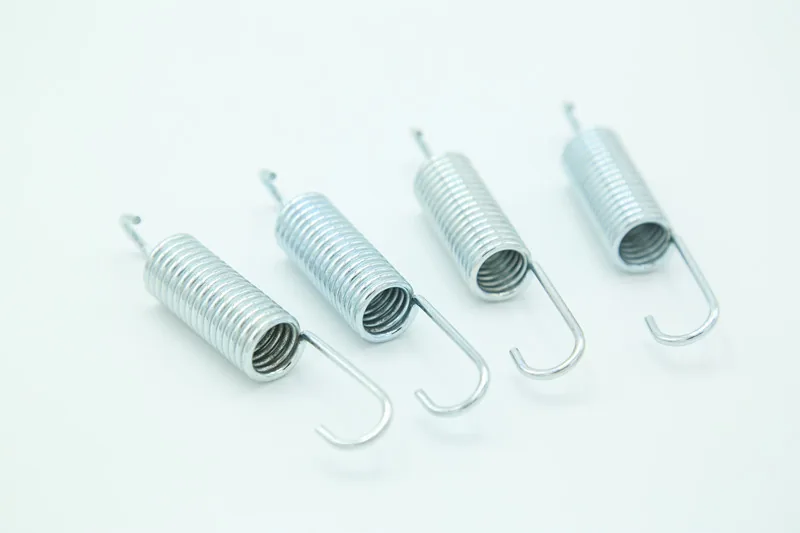
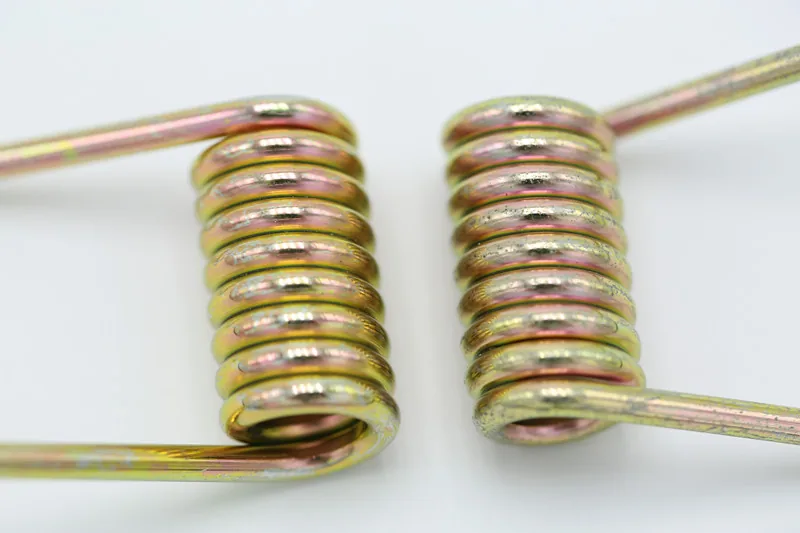
Extension springs that pull a mechanism closed and hold it there
15 catalogued parts
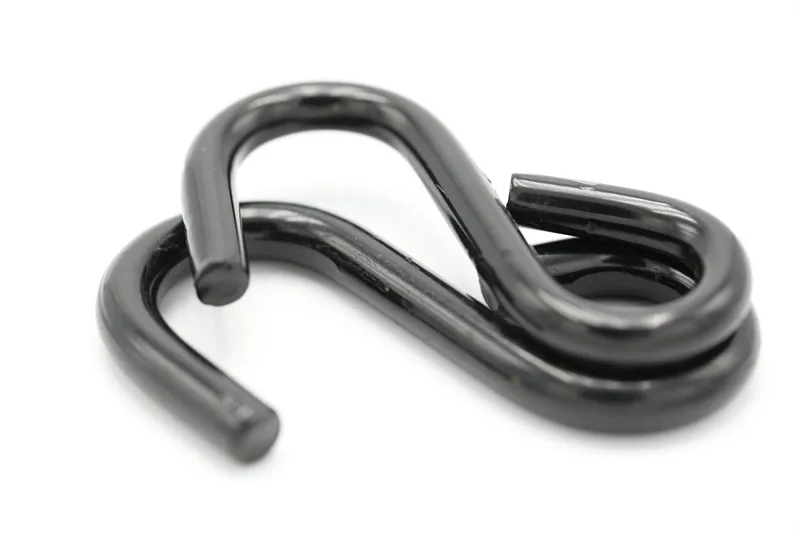
Bent wire parts that are not coils at all
16 catalogued parts
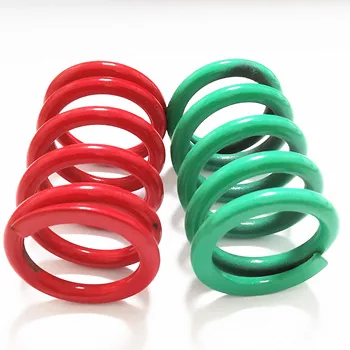
Helical springs that push back under load
16 catalogued parts
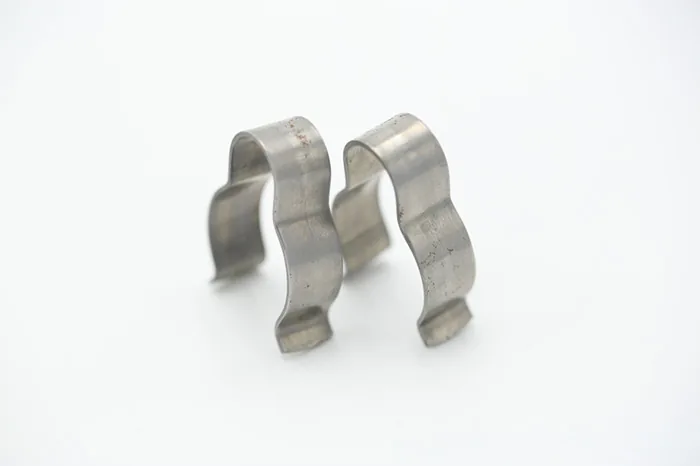
Clips that hold position without a fastener
11 catalogued parts
Formed hooks for hanging, tensioning and retail display
13 catalogued parts
Strip and coil springs for clamping and constant force
15 catalogued parts
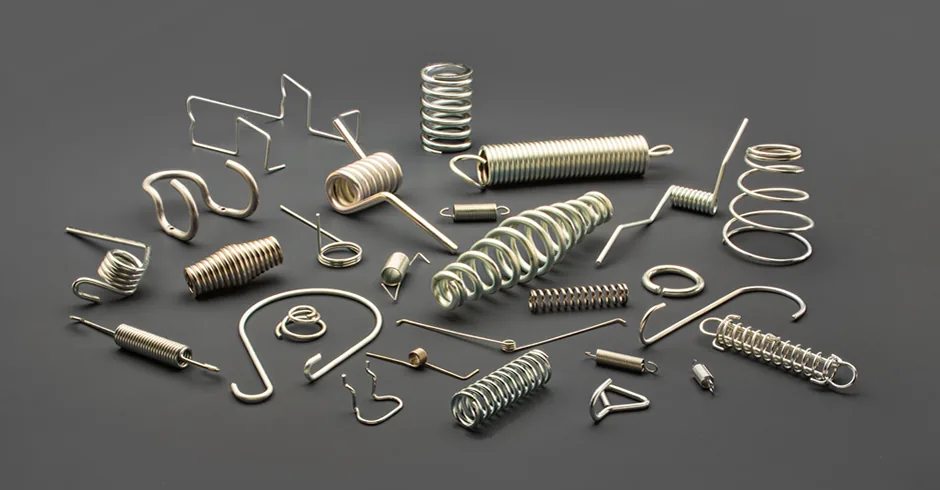
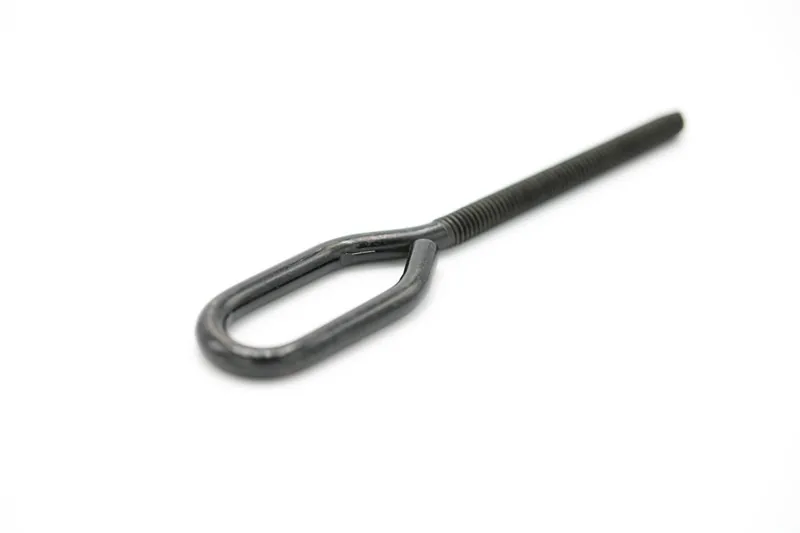
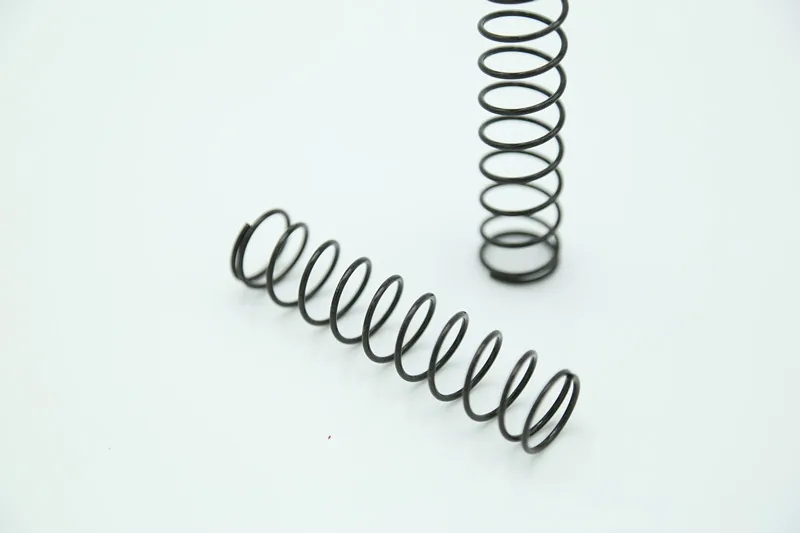
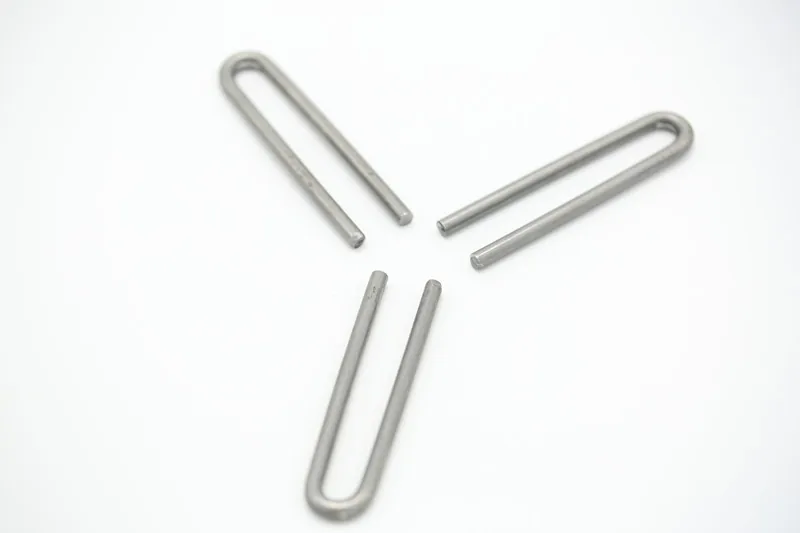
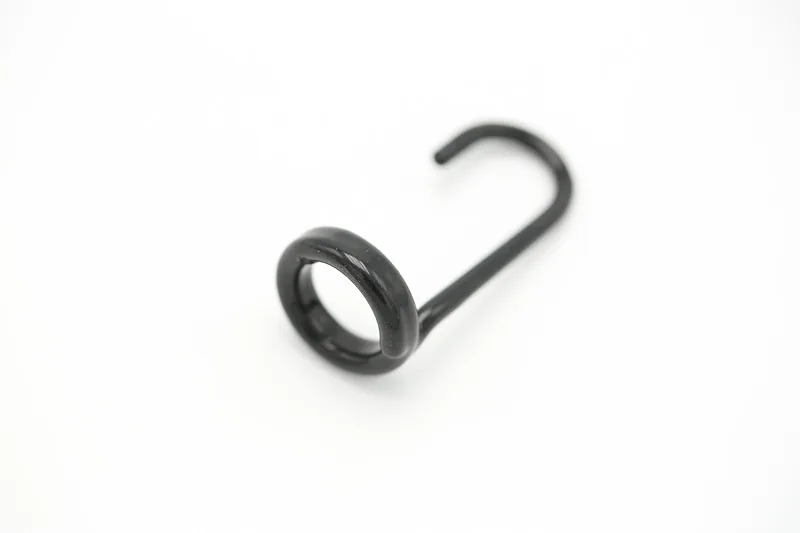
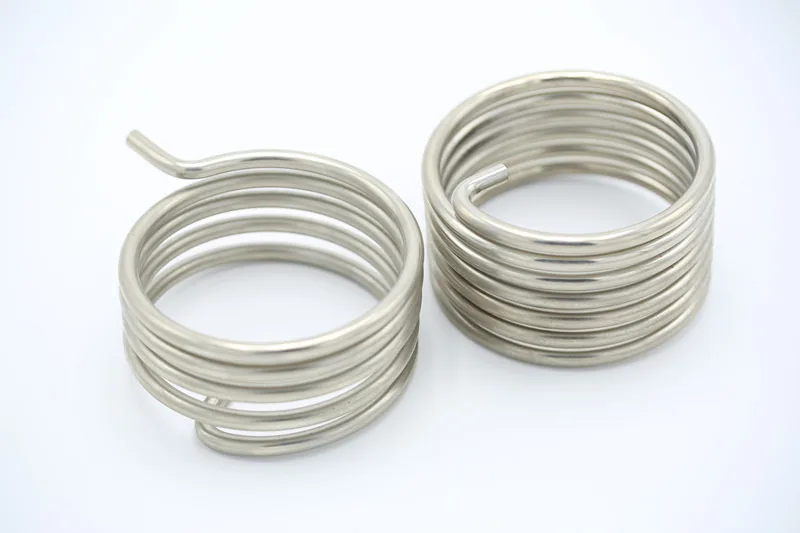
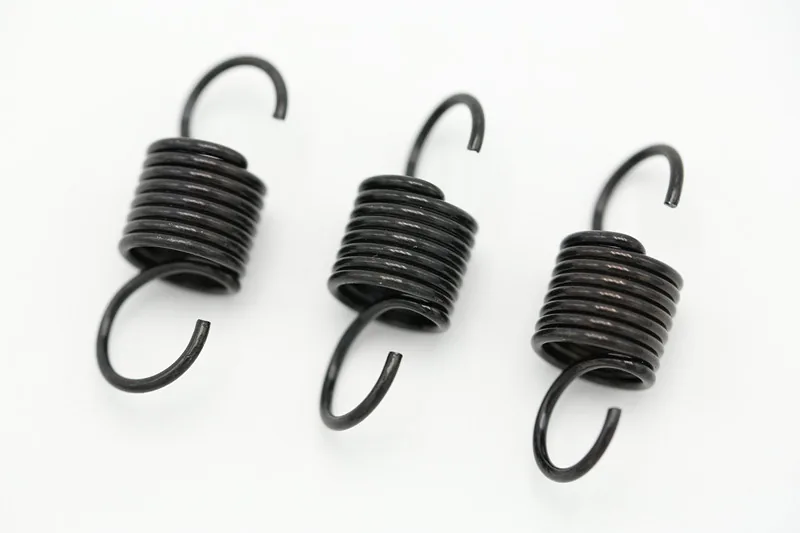
These are photographs of production parts, not renders. Each one can be reproduced to your dimensions, in your material and in your finish.
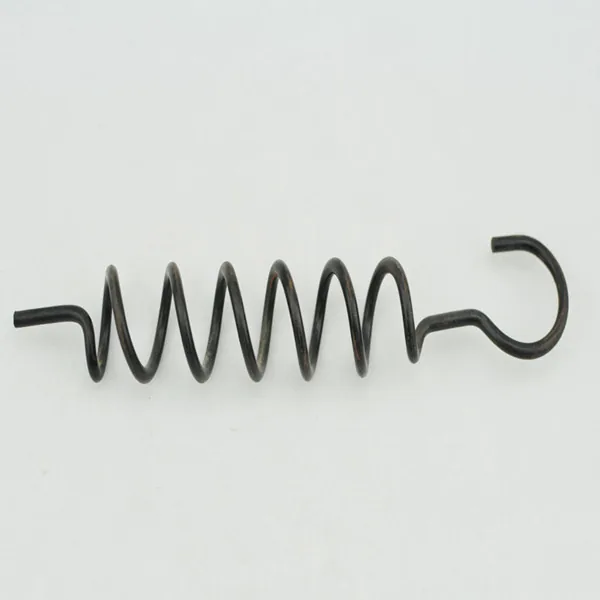
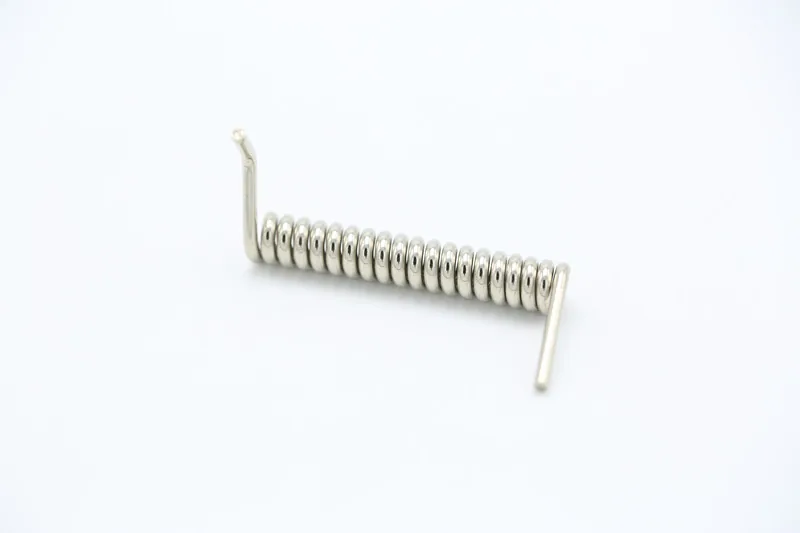
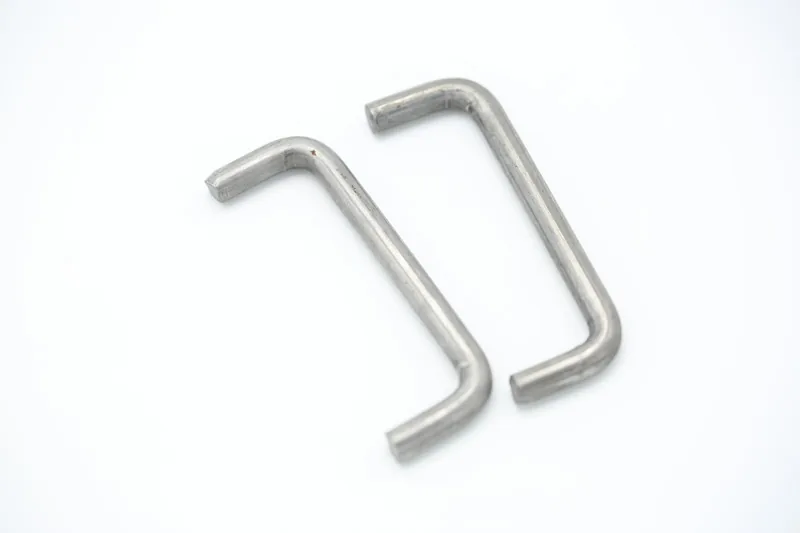
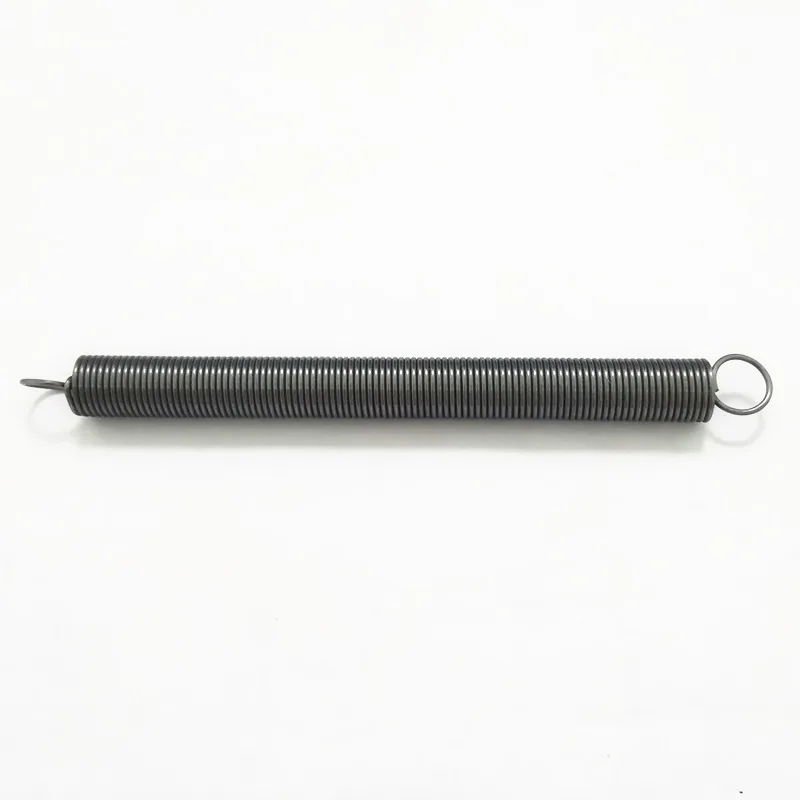
The industries below are where our production has concentrated since 2000, and the demands each one places on a spring are different.
Springs that survive ten years of daily cycling behind a panel
Miniature springs and contacts down to 0.1 mm wire
Interior, trim and accessory springs for tier suppliers
Extension springs and hooks that carry human load safely
Small springs for ribs, runners and opening mechanisms
Springs made for products that children handle
Precision springs for measuring and laboratory equipment
These are the four problems that bring most buyers to a dedicated spring manufacturer rather than to a general hardware supplier.
Springs are cheap parts that stop expensive lines. We run short and medium custom batches on dedicated CNC coilers instead of treating them as filler work, with parts shipping 7-15 days after the order is confirmed.
Torsion, tension, compression, flat and wire form parts are all made here, so a single drawing package, a single finish specification and a single inspection report cover the whole assembly.
Coiling is programmed on the machine rather than set by hand, and heat treatment and surface finishing follow a fixed route, so batch two behaves like the sample you approved.
Nine finishing routes are available in house, from zinc and nickel to dacromet, black oxide and phosphating, so the coating can be matched to the humidity and the contact material of your application.
Every batch follows the same route, and the inspection steps sit inside it rather than being bolted on at the end.
From a sketch, a drawing or the part in your hand to an approved production sample
Nine finishing routes chosen against the environment the spring works in
What gets tested before a batch is allowed to be packed
Written for buyers and design engineers who need to describe a spring precisely enough to be quoted accurately.
The six numbers a spring maker needs before anything can be quoted, and how to measure them from a part you already have.
Why most torsion spring failures happen at the leg, and how to get the handedness right the first time.
Zinc, nickel, dacromet, black oxide or stainless: a practical way to pick the finish before corrosion picks it for you.
Torsion, tension, compression and flat springs, plus wire forms, spring clips and spring hooks, in wire from 0.1 to 8 mm. All seven families are made on the same floor in Xiamen.
Yes. ISO standard, non-standard and OEM drawings are all normal work here, and we can also reproduce a part from a physical sample when no drawing exists.
Typical production is 7-15 days after the order is confirmed, with surface finishing included in that window.
Stainless steel, spring steel, carbon steel, 65Mn and music wire, with zinc, nickel, silver, gold, tin, galvanising, dacromet, black oxide and phosphating available in house.
Email the drawing, a photograph or the dimensions of your part, along with the load and the environment it works in, and we will come back with a quotation and any questions.
Tell us the load, the travel and the environment your spring works in. We will come back with a quotation and the questions that matter.