
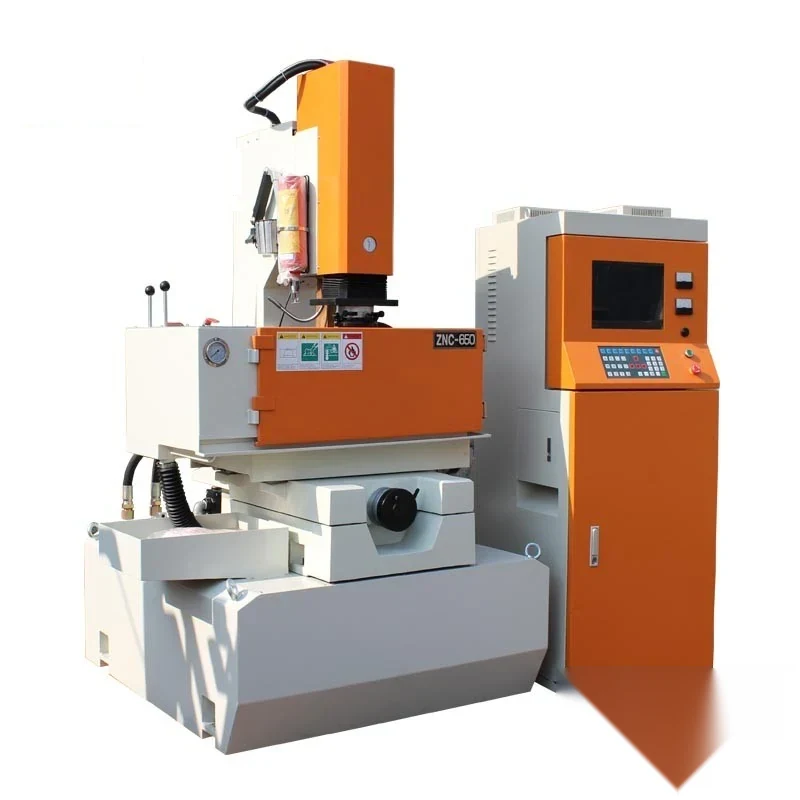
ZNC350 Spark Erosion Electric Discharge Die Sinking Machine
The ZNC350 is a die sinking electric discharge machine, the tool a mould shop uses to cut shapes into hardened steel that a cutter cannot reach or cannot survive. Its generator carries separate circuit designs for positive and negative polarity work, a dedicated deep hole circuit, a superfine finishing circuit and a se...
What This Machine Does
The ZNC350 is a die sinking electric discharge machine, the tool a mould shop uses to cut shapes into hardened steel that a cutter cannot reach or cannot survive. Its generator carries separate circuit designs for positive and negative polarity work, a dedicated deep hole circuit, a superfine finishing circuit and a servo stabilisation circuit for large electrode areas, so the same machine sinks a deep rib and then finishes a cavity surface. Electrode protection and separate high and low clearance circuits guard the electrode against the conditions that erode it fastest. Servo control is PWM with a DC servo motor, with AC servo available, and travel is arranged in two stages. Discharge parameters can be selected automatically or set by the operator for the material and finish required. XYZ positions are shown on digital readout. Fire detection with an extinguisher and low dielectric level protection are fitted, and PCB boards are moisture-proofed and anti-rust treated.
Why Buyers Choose This Machine
- Separate positive and negative processing circuits so the same machine handles both polarities
- Dedicated deep hole circuit keeps flushing and discharge stable in deep cavities and ribs
- Superfine processing circuit produces fine surface finishes without moving the job to another machine
- Large area electrode servo stabilisation prevents arcing when the discharge area is wide
- Electrode protection circuit reduces electrode wear and protects the shape you cut into it
- Automatic program discharge parameters shorten setup for operators new to EDM
- Fire detection with extinguisher and low liquid level protection built into the machine
Where ZNC350 Spark Erosion Electric Discharge Die Sink Earns Its Place
Problems It Solves
- Hardened steel cannot be machined economically with conventional cutters
- Deep cavities stop cutting cleanly when the discharge gap cannot be flushed
- Sharp internal corners are impossible to produce with a rotating cutter
- Electrode wear changes the cavity shape part-way through a long burn
- Large flat electrode faces arc and damage the workpiece without servo stabilisation
- Dielectric fires and low fluid levels are a real hazard on an unattended EDM
Who It Is For
- Mould and die shops working in hardened tool steel
- Toolrooms supporting injection moulding and press tool production
- Machine shops taking in EDM work as a subcontract service
- Distributors equipping toolrooms in export markets
Application Scenarios
- Sinking cavities and cores in hardened mould and die steel
- Cutting deep ribs slots and keyways that a milling cutter cannot reach
- Producing sharp internal corners that cannot be milled with a round cutter
- Removing broken taps and drills from finished workpieces
- Finishing mould surfaces where a superfine discharge setting is needed
Technical Detail
Technical Features
- Depth design for positive and negative processing
- Special circuit for deep hole processing
- Superfine processing circuit
- Large area electrode servo stabilisation circuit
- Electrode protection circuit
- Separate circuit design for high and low clearance
- PWM servo system with DC servo motor and AC servo optional
- Two stage travel
- High voltage overlap synchronous discharge system
- Square wave and equal energy posterior output
- Moisture-proof and anti-rust PCB board design
- Automatic program discharge parameters with selectable processing conditions
- DRO for XYZ
- Automatic fire detection with extinguisher and insufficient liquid level protection
Specifications
| Machine type | ZNC die sinking electric discharge machine |
|---|---|
| Models | ZNC350 ZNC450 ZNC550 ZNC650 |
| Workbench size | 600*300mm ZNC350 700*400mm ZNC450 800*480mm ZNC550 1000*600mm ZNC650 |
| Working slot size | 820*500*300mm ZNC350 1120*620*420mm ZNC450 1290*770*500mm ZNC550 |
| Servo system | PWM servo with DC servo motor AC servo optional |
| Travel | Two stage travel |
| Position display | DRO for X Y and Z |
| Discharge parameters | Automatic program with selectable processing conditions |
| Safety | Automatic fire detection with extinguisher and low liquid level protection |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Electrical discharge machining
- Die sinking
- Deep hole EDM
- Superfine surface finishing
Quality Control
- Generator circuits tested across positive negative deep hole and superfine settings
- Servo response checked with a large area electrode before despatch
- XYZ digital readout verified against the machine slides
- Fire detection and low liquid level protection function tested
- Test burn carried out on a sample workpiece before packing
Customisation Options
- Model chosen from ZNC350 to ZNC650 by workbench and working slot size
- AC servo specified in place of the standard DC servo motor
- Electrode holders and chucking specified for your electrode material
- Supply voltage phases and frequency built for your market
- Operating language for the control panel and manual
How It Compares With the Alternatives
| Conventional milling of hardened steel | Milling hardened tool steel wears cutters quickly and cannot form sharp internal corners; EDM erodes the shape regardless of material hardness |
|---|---|
| Wire cut EDM | Wire EDM cuts through profiles from edge to edge; the ZNC350 sinks blind cavities and pockets which wire cutting cannot do |
| Larger ZNC450 ZNC550 and ZNC650 models | The ZNC350 has a 600*300mm workbench and 820*500*300mm working slot; the larger models step up to 1000*600mm workbench on the ZNC650 for bigger mould blocks |
Running the Machine
Step 1
Mount the workpiece in the working slot and set it square to the machine axes
Step 2
Fit and align the electrode then zero the X Y and Z positions on the DRO
Step 3
Select the processing condition for the material electrode and finish required
Step 4
Use the deep hole circuit where the cavity depth restricts flushing
Step 5
Switch to the superfine circuit for the finishing passes on visible surfaces
Step 6
Check the dielectric level is above the low level protection point before running unattended
Step 7
Keep the dielectric filtered so debris does not cause secondary discharge
Other Machines in EDM
Questions About ZNC350 Spark Erosion Electric Discharge Die
Which ZNC model should I order?
Choose by the size of the work you sink. The ZNC350 has a 600*300mm workbench and 820*500*300mm working slot, rising to a 1000*600mm workbench on the ZNC650. Send us your largest mould block and we will confirm.
Can it cut hardened tool steel?
Yes. Electrical discharge machining removes material by spark erosion, so workpiece hardness does not limit the process the way it limits a cutter.
What electrode material should I use?
Copper and graphite are both used on die sinking machines, with the choice depending on cavity detail, wear and finish. Tell us the cavities you sink and we will advise on holders and chucking with the quotation.
Is AC servo available?
Yes. The standard machine uses a PWM servo system with a DC servo motor, and an AC servo motor is available as an option. State which you want on the order.
What safety features are fitted?
Automatic fire detection with an extinguisher and insufficient liquid level protection are fitted, and the PCB boards are moisture-proofed and anti-rust treated for the EDM environment.
What supply voltage is the machine built for?
Tell us your voltage, phases and frequency with the order and the machine will be wired and tested for that supply.
What are your trade and payment terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the ZNC350 Spark Erosion Electric Discharge Die
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.