
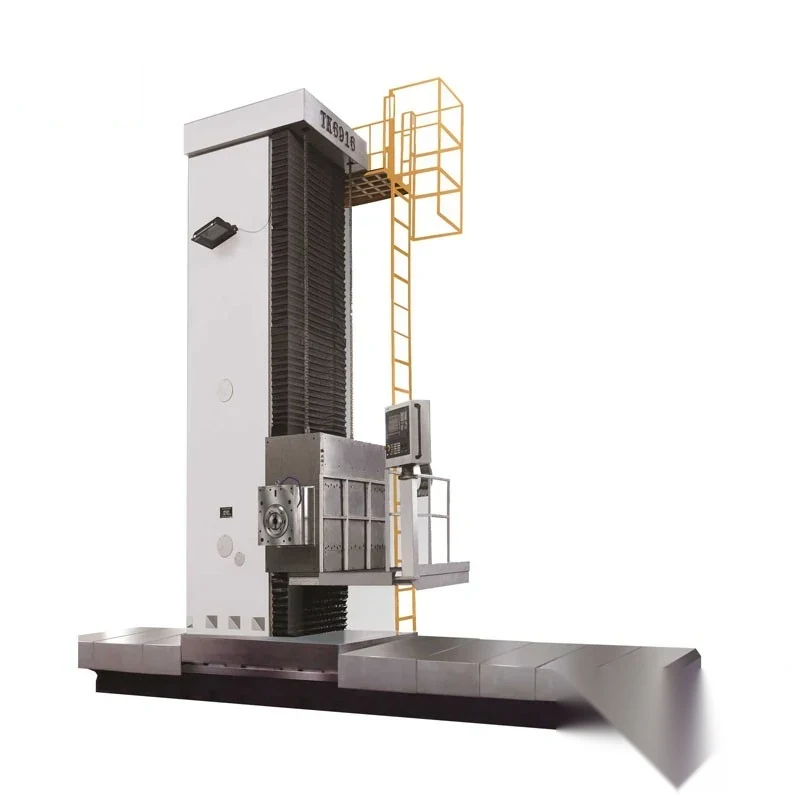
TX6213 CNC Horizontal Milling Boring Machine
The TX6213 is built for box-shaped work: gearbox housings, pump bodies, valve blocks and large brackets where a series of bores on different faces must end up in line with each other. Rough boring, fine boring and milling are done in the same setup, and the worktable carries a 4x90 degree optical positioning device, so...
What This Machine Does
The TX6213 is built for box-shaped work: gearbox housings, pump bodies, valve blocks and large brackets where a series of bores on different faces must end up in line with each other. Rough boring, fine boring and milling are done in the same setup, and the worktable carries a 4x90 degree optical positioning device, so a large part can be turned to the next face without being unclamped and re-indicated. Castings are produced by resin sand moulding and put through two stress relief treatments, which is what stops the machine moving in service after the first year. The X Y and Z axes are driven by servo motors turning ball screws through synchronous pulleys, a simple arrangement with few parts to wear, and the W axis is directly connected. The boring shaft carries a cutter cylinder so tools are loaded and unloaded quickly. An optional 4x90 degree positioning rotary table is available where turn-around machining is routine.
Why Buyers Choose This Machine
- Bores milled faces and drilled holes on several faces are produced in one setup so they stay in line
- 4x90 degree optical positioning on the worktable indexes a large part without unclamping and re-indicating
- Resin sand castings with two stress relief treatments hold alignment after the machine is in service
- Servo motors driving ball screws through synchronous pulleys on X Y and Z give a simple structure with few wear points
- Directly connected W axis removes a transmission stage from the boring feed
- Cutter cylinder on the boring shaft makes tool changes quick instead of a two-person job
- Optional 4x90 degree positioning rotary table for shops where turn-around machining is the norm
Where TX6213 CNC Horizontal Milling Boring Machine Earns Its Place
Problems It Solves
- Bores machined in separate setups on separate machines do not line up across the part
- Re-clamping and re-indicating a heavy box part between faces takes hours and adds error
- Untreated castings relax after installation and the machine loses its geometry
- Complicated multi-stage transmissions add backlash and wear points on the feed axes
- Slow tool changes on a boring bar stop a long job repeatedly
- Large and medium-sized parts exceed the capacity of general purpose milling machines
Who It Is For
- Heavy machinery and gearbox manufacturers
- Pump valve and compressor builders machining box-shaped bodies
- Subcontract shops taking in large part boring and milling work
- Overhaul workshops re-machining worn housings
- Plant engineering departments with their own large part machining capacity
Application Scenarios
- Machining gearbox and reduction housings with bores on opposite faces
- Boring and facing pump and compressor bodies
- Rough and fine boring of large and medium-sized castings
- Turn-around machining of box parts using the 4x90 degree positioning
- Milling mounting faces and bosses on fabricated frames
- Repair boring of worn housings in heavy machinery overhaul
Technical Detail
Technical Features
- Resin sand moulded castings with two stress relief treatments
- X Y and Z axes driven by servo motors and ball screws through synchronous pulleys
- W axis directly connected
- Boring shaft fitted with a cutter cylinder for fast tool loading and unloading
- Worktable with 4x90 degree optical positioning device
- Optional 4x90 degree positioning rotary table
- CNC control for rough and fine boring milling and related operations
Specifications
| Machine type | CNC horizontal milling and boring machine |
|---|---|
| Models | TX6213 / TK6213 |
| Castings | Resin sand moulded with two stress relief treatments |
| X Y Z drive | Servo motors driving ball screws through synchronous pulleys |
| W axis | Directly connected |
| Boring shaft | Fitted with cutter cylinder for tool loading and unloading |
| Worktable | 4x90° optical positioning device |
| Option | 4x90° positioning rotary table |
| Applications | Rough and fine boring milling and hole and plane machining of box-shaped parts |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Rough boring
- Fine boring
- Milling
- Drilling
- Face machining
Materials Handled
- Cast iron
- Steel
Quality Control
- Castings stress relieved twice before machining of guideways and mounting faces
- Spindle run-out and boring shaft alignment measured on assembly
- 4x90 degree table positioning checked for repeatability at each index position
- Axis positioning checked on X Y Z and W after servo commissioning
- Test boring and milling cut taken and measured before the machine is packed
Customisation Options
- 4x90 degree positioning rotary table specified where turn-around machining is routine
- Table and travels confirmed against your largest workpiece before the order is placed
- CNC system and operating language set for your shop
- Boring tooling and cutter holders specified for your bore diameters
- Supply voltage frequency and export packing arranged for your market
How It Compares With the Alternatives
| TPX611 horizontal CNC milling boring machine | Both work box-shaped parts, but the TX6213 is specified where the 4x90 degree optical worktable positioning and turn-around machining of larger parts drive the purchase |
|---|---|
| Manual horizontal boring machine | A manual machine depends on the operator dialling in each position; the CNC axes repeat the bore pattern part after part, which is what makes batch housing work viable |
| Machining the part on a vertical machining centre | A vertical centre reaches one face at a time and struggles with deep through bores; the horizontal boring machine bores through the part and indexes the table to reach the opposite face |
Running the Machine
Step 1
Clamp and level the workpiece on the table and set the datum for the first face
Step 2
Load the boring tooling into the boring shaft using the cutter cylinder
Step 3
Set and verify the CNC program for the bore pattern on the first face
Step 4
Take a roughing pass then measure before committing to the fine boring cut
Step 5
Index the table through 4x90 degree positioning to reach the next face without unclamping
Step 6
Re-check the bore alignment across faces on the first part of a batch
Step 7
Keep the guideways and ball screws lubricated on the schedule in the manual
Other Machines in Boring
Related Applications and Guides
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Heavy Equipment and Plant Maintenance
Mines quarries plantations and processing plants cannot wait for imported spares. XAIMC supplies the boring gear cutting turning and grinding machines
Questions About TX6213 CNC Horizontal Milling Boring Machine
What size of part will the TX6213 take?
Send us the workpiece dimensions weight and the bore pattern you machine and we will confirm the table size and axis travels against them before quoting.
Can I machine opposite faces without re-clamping?
Yes. The worktable has a 4x90 degree optical positioning device, so the part is indexed to the next face and the bores stay related to the same datum.
Why are the castings stress relieved twice?
Resin sand castings carry internal stress from solidification. Two stress relief treatments release it before machining so the machine holds its geometry in service.
How are tools changed in the boring shaft?
The boring shaft is equipped with a cutter cylinder, which makes loading and unloading tools convenient and fast.
Is a rotary table available?
Yes. A 4x90 degree positioning rotary table is offered as an option for turn-around processing of large parts.
What CNC system is fitted and can I specify a different one?
Tell us the control system your operators already work with and the voltage and frequency of your supply, and we will confirm what we can build.
What are your trade and payment terms and how is the machine shipped?
We quote FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight. Tell us your port and we will confirm packing and shipping dimensions.
Request a Quote on the TX6213 CNC Horizontal Milling Boring Machine
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.