
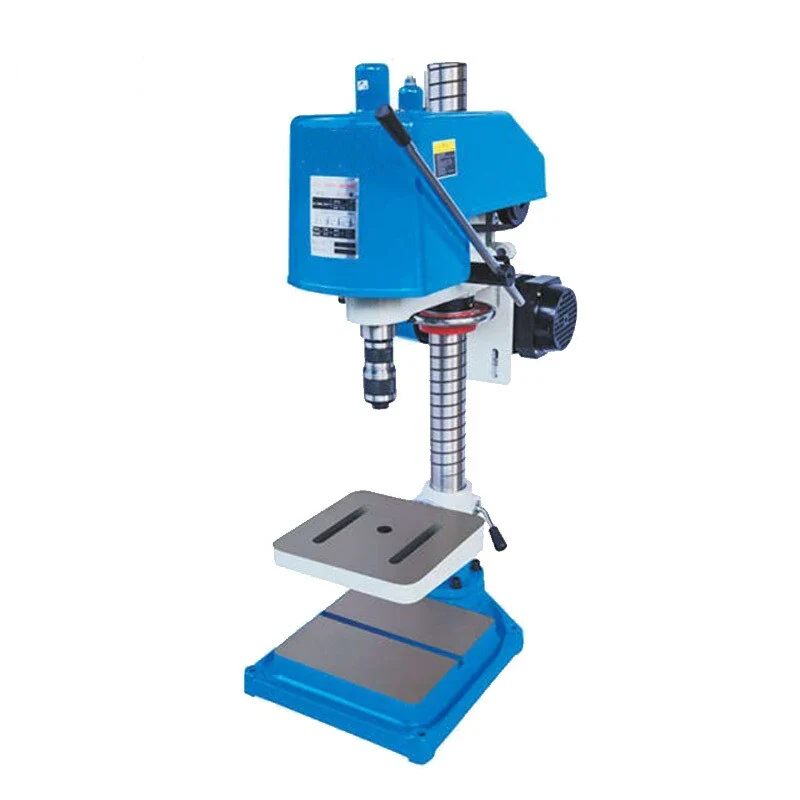
Tapping Machine SWJ-10B SWJ-6 SWJ-12 SWJ-16 & SWJ-24
The SWJ range is built to do one job properly: cutting threads in drilled holes. Five sizes cover M6 to M24 in cast iron and M5 to M20 in steel, so a shop can put the right machine at the right station rather than tapping everything on a drill press. The structure is simple and the machine is easy to operate, and the p...
What This Machine Does
The SWJ range is built to do one job properly: cutting threads in drilled holes. Five sizes cover M6 to M24 in cast iron and M5 to M20 in steel, so a shop can put the right machine at the right station rather than tapping everything on a drill press. The structure is simple and the machine is easy to operate, and the part that matters most is the friction clutch. It drives the tap through the cut and slips when the load rises, which gives overload protection, keeps the motor from being stalled and hammered, and extends its life. Running is stable and noise is low. Spindle speeds are stepped rather than variable: 480 and 850 r/min on the SWJ-6, three speeds on the others down to 230, 350 and 500 r/min on the SWJ-24, which is the right pattern since larger taps need lower speeds. Spindle travel is 40mm or 50mm and spindle tapers run from B10 to B22.
Why Buyers Choose This Machine
- Friction clutch slips under overload so a bound tap does not stall the motor or snap in the hole
- Five capacities from M6 to M24 in cast iron so each station gets the right size machine
- Speed steps fall as capacity rises which is exactly what larger taps need
- Dedicated tapping station frees the drilling machine for drilling
- Simple structure with easy operation so operators are productive quickly
- Stable running and low noise on a machine used all shift
- SWJ-16 and SWJ-24 give 485mm and 545mm spindle nose to worktable for taller parts
Where Tapping Machine SWJ-10B SWJ-6 SWJ-12 SWJ-16 & SW Earns Its Place
Problems It Solves
- Taps snap in the hole when a machine has no clutch to slip under overload
- Stalling a motor on a bound tap shortens its life and risks the drive
- Tapping on a drilling machine ties up drilling capacity and is rarely the right speed
- Hand tapping large threads in cast iron is slow and produces crooked threads
- Running a tap too fast for its size burns the tap and tears the thread
- Tall workpieces do not fit under machines with limited spindle nose to table distance
Who It Is For
- Fabrication shops with repeat tapped hole patterns
- Casting machine shops tapping cast iron components
- Assembly plants preparing threaded holes in house
- Maintenance workshops repairing and recutting threads
- Distributors supplying small and medium engineering shops
Application Scenarios
- Production tapping of drilled hole patterns in plate and castings
- Tapping M20 and M24 threads in cast iron on the SWJ-24
- Small thread work at M6 and M5 on the SWJ-6
- Second-operation tapping alongside a drilling line
- Tapping tall workpieces on the SWJ-16 and SWJ-24 columns
- Repair shop thread cutting in cast iron and steel components
Technical Detail
Technical Features
- Machine friction clutch drive with overload protection
- Maximum tapping capacity M6/M5 to M24/M20 in cast iron and steel
- Spindle speeds in two or three steps by model from 230 r/min to 850 r/min
- Spindle travel 40mm or 50mm
- Spindle tapers B10 B16 B18 and B22
- Column diameters from 50mm to 73mm
- Worktable sizes from 196 x 196mm to 280 x 280mm
- Overall heights from 767mm to 1220mm
- Stable low noise running with simple operation
Specifications
| Machine type | Tapping machine |
|---|---|
| Models | SWJ-6 SWJ-10B SWJ-12 SWJ-16 SWJ-24 |
| Max tapping capacity cast iron and steel | M6/M5 / M12/M10 / M12/M8 / M16/M12 / M24/M20 |
| Diameter of column | 60mm / 50mm / 60mm / 73mm / 70mm |
| Spindle travel | 40mm / 50mm / 40mm / 50mm / 50mm |
| Spindle axis to column generating line | 127mm / 140mm / 127mm / 183mm / 198mm |
| Max distance spindle nose to worktable | 245mm / 310mm / 240mm / 485mm / 545mm |
| Max distance spindle nose to base | 375mm / 370mm / 660mm / 760mm |
| Spindle taper | B10 / B16 / B16 / B18 / B22 |
| Spindle speeds | 480 850 / 250 480 800 / 260 440 750 / 240 380 570 / 230 350 500 r/min |
| Spindle speed steps | 2 on SWJ-6 and 3 on the others |
| Worktable size | 196 x 196mm / 200 x 200mm / 235 x 235mm / 270 x 280mm / 280 x 280mm |
| Dimension of base | 385 x 215mm / 365 x 254mm / 400 x 250mm / 520 x 310mm / 495 x 375mm |
| Overall height | 800mm / 767mm / 810mm / 1220mm / 1075mm |
| Drive | Machine friction clutch with overload protection |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Tapping
- Thread recutting
Quality Control
- Friction clutch set and tested to slip under overload before shipment
- Spindle run-out checked at the B10 B16 B18 or B22 taper
- All spindle speed steps run and checked against the model plate
- Table squareness to the spindle axis verified
- Sample thread tapped in cast iron and checked with a gauge
Customisation Options
- Model selected by the largest thread you cut in cast iron or steel
- Tapping chucks and tap holders supplied to match the spindle taper
- Supply voltage frequency and phase built for your market
- Worktable and fixture arrangement discussed for repeat hole patterns
- Manual and machine plates prepared in your working language
How It Compares With the Alternatives
| Tapping on a drilling machine | A drilling machine is geared for drilling speeds and usually has no slipping clutch, so taps break and drilling capacity is tied up |
|---|---|
| Hand tapping with a wrench | Hand tapping large threads in cast iron is slow and the thread is rarely square to the face |
| Auto-Feed Drilling Machine ZB4116G ZB4120G ZB4132G | Those machines drill and tap at one station; the SWJ machines are dedicated tappers for shops running tapping as a separate production operation |
| Machines without overload protection | The friction clutch is what protects both the tap and the motor when a tap binds in a blind or dirty hole |
Running the Machine
Step 1
Choose the model whose cast iron and steel capacity covers your largest thread
Step 2
Clamp the workpiece on the table so the drilled hole is square to the spindle
Step 3
Fit the tap in a holder matched to the B10 B16 B18 or B22 spindle taper
Step 4
Select the lowest speed step for large taps and the higher steps for small ones
Step 5
Check the clutch slips before running production so a bound tap is protected
Step 6
Use tapping fluid suited to cast iron or steel and clear chips from blind holes
Step 7
Gauge the first thread of a batch before continuing
Other Machines in Tapping
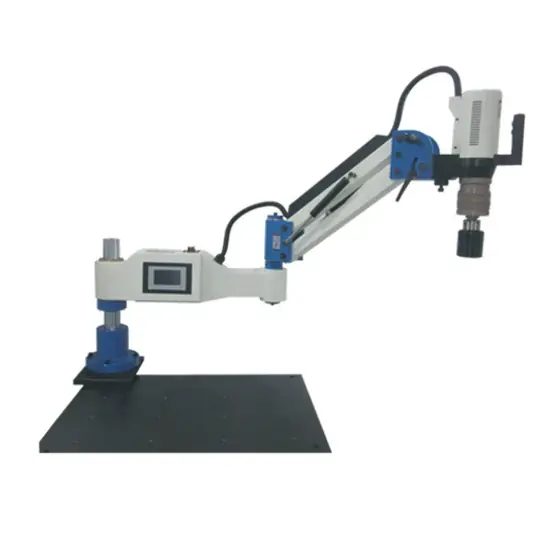
Pneumatic and Electric Threading Machine SRAM12 SRM-M16W SRM-M24 SRM-M42W
View Machine →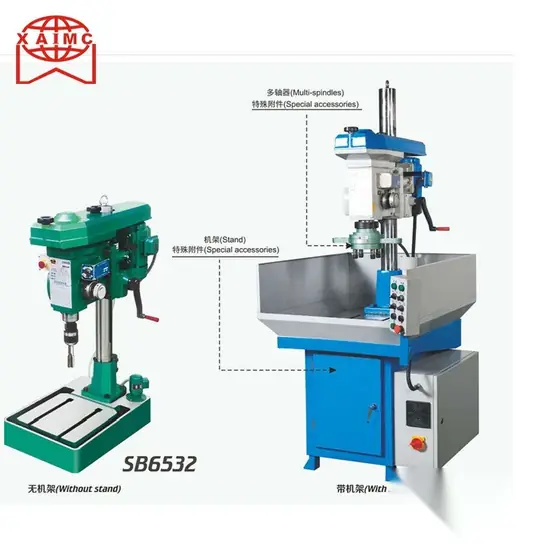
Gear Type Teeth Distance Tapping Machine SB6516 SB6532 and SB6532A
View Machine →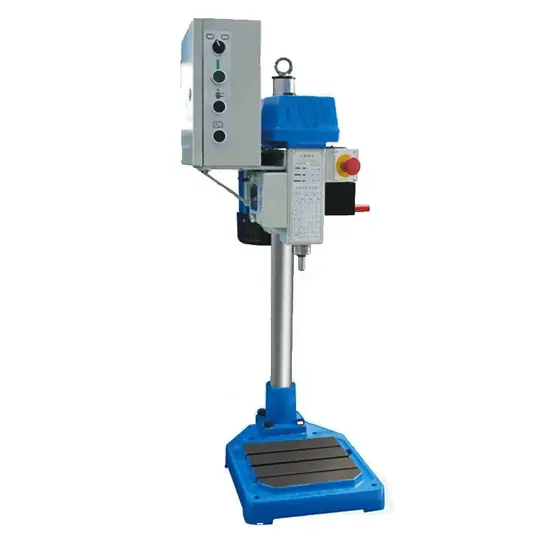
Gear Type Teeth Distance Tapping Machine SB408G SB4516G and SB4516A
View Machine →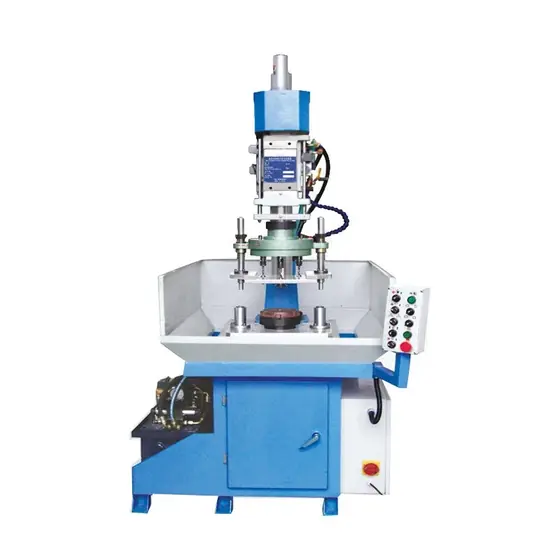
Lead-Screw Automatic Tapping Machine SB8030
View Machine →Questions About Tapping Machine SWJ-10B SWJ-6 SWJ-12 SWJ-16
Which model do I need?
Capacity in cast iron and steel is M6/M5 on the SWJ-6, M12/M10 on the SWJ-10B, M12/M8 on the SWJ-12, M16/M12 on the SWJ-16 and M24/M20 on the SWJ-24. Choose by your largest thread.
What stops the tap breaking?
A machine friction clutch drives the spindle and slips under overload. That protects the tap and keeps the motor from being stalled, which is also why motor life is longer.
What spindle speeds are available?
Two steps on the SWJ-6 at 480 and 850 r/min, three steps on the others, down to 230, 350 and 500 r/min on the SWJ-24 where bigger taps need lower speeds.
Will it take a tall workpiece?
The SWJ-16 gives 485mm and the SWJ-24 545mm from spindle nose to worktable. The smaller models give 240mm to 310mm.
What tap holders do I need?
Match the spindle taper: B10 on the SWJ-6, B16 on the SWJ-10B and SWJ-12, B18 on the SWJ-16 and B22 on the SWJ-24. We can supply holders with the machine.
What voltage and how are they packed?
Wired for the voltage frequency and phase you state on the order, packed for export from Xi'an and shipped FOB CFR or CIF.
What are your payment terms?
30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the Tapping Machine SWJ-10B SWJ-6 SWJ-12 SWJ-16
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.