
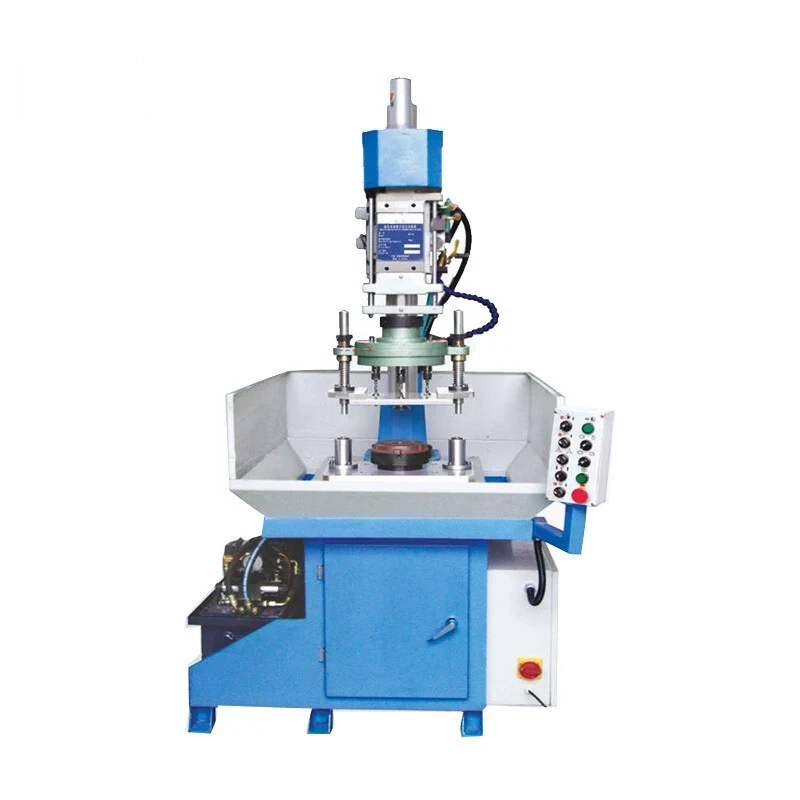
Lead-Screw Automatic Tapping Machine SB8030
The SB8030 drives the tapping feed from a lead screw rather than from a change gear train, so the feed rate is tied mechanically to the screw and holds through the whole stroke. That steady feed is what allows the tap to be extruded into the hole and brings hole precision and thread cleanliness to the required standard...
What This Machine Does
The SB8030 drives the tapping feed from a lead screw rather than from a change gear train, so the feed rate is tied mechanically to the screw and holds through the whole stroke. That steady feed is what allows the tap to be extruded into the hole and brings hole precision and thread cleanliness to the required standard. Capacity is 35 mm maximum drilling diameter on a 95 mm column, with 140 mm of spindle travel and 282.5 mm from the spindle axis to the column generating line, giving 700 mm maximum from spindle nose to base. The spindle is MT4 or ER40, so standard taper tooling or an ER collet chuck can both be used. Spindle speeds are specified by the customer rather than being fixed at the factory, which means the machine arrives set for the thread sizes and material you actually run. Working pressure is 20 to 35 kgf/cm2. The main motor is 2.2 kW with a 40 W coolant motor. The machine weighs 600 kg net on a 690 x 500 mm base at 1165 mm overall height.
Why Buyers Choose This Machine
- Lead screw feed holds a steady rate through the stroke instead of depending on gear train backlash
- Tap extrusion under controlled feed gives hole precision and a clean thread
- Spindle speeds specified by the customer so the machine arrives suited to your threads and material
- MT4 or ER40 spindle accepts taper tooling or ER collet chucks already in your shop
- 35 mm capacity and 140 mm spindle travel handle deep threads in heavy parts
- Coolant motor fitted so thread quality and tap life do not depend on hand oiling
- 600 kg net on a 690 x 500 mm base gives the stability that heavy tapping needs
Where Lead-Screw Automatic Tapping Machine SB8030 Earns Its Place
Problems It Solves
- Gear driven feed with backlash lets the tap wander off pitch in deep holes
- Hand feeding a large tap gives inconsistent thread depth and form
- Dry tapping picks up and tears the thread in ductile material
- A fixed factory speed set does not match every shop's thread and material mix
- Light machines flex under the torque of tapping at 35 mm capacity
Who It Is For
- Production machine shops tapping heavy components
- Valve flange and hydraulic block manufacturers
- Subcontract shops standardised on ER40 tooling
- Heavy equipment component manufacturers
- Distributors supplying automatic tapping machines
Application Scenarios
- Tapping deep threads in thick machined parts and flanges
- Repeat tapping of heavy components where feed consistency matters
- Thread forming by extrusion on ductile material
- Tapping large diameter threads up to the 35 mm capacity of the machine
- Production tapping stations where an ER40 collet chuck standardises tooling
Technical Detail
Technical Features
- Lead screw driven tapping feed
- Tap extrusion feed for hole precision and thread cleanliness
- Maximum drilling diameter 35 mm
- Column diameter 95 mm
- Spindle travel 140 mm
- Spindle taper MT4 or ER40
- Spindle speeds specified by the customer
- Working pressure 20 to 35 kgf/cm2
- Main motor 2.2 kW with 40 W coolant motor
- Base 690 x 500 mm at 1165 mm overall height
Specifications
| Machine type | Lead-screw automatic tapping machine |
|---|---|
| Models | SB8030 (OD-35) |
| Max drilling diameter | 35 mm |
| Column diameter | 95 mm |
| Spindle travel | 140 mm |
| Distance spindle axis to column generating line | 282.5 mm |
| Max distance spindle nose to base | 700 mm |
| Spindle taper | MT4 or ER40 |
| Spindle speed range | Customer specified |
| Working pressure | 20-35 kgf/cm2 |
| Base dimensions | 690 x 500 mm |
| Overall height | 1165 mm |
| Main motor power | 2.2 kW |
| Coolant motor | 40 W |
| Gross / net weight | 630 / 600 kg |
| Packing dimensions | 152 x 112 x 230 cm |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Tapping
- Thread cutting
- Extrusion
Quality Control
- Lead screw feed rate checked against the specified thread pitch
- Spindle run-out checked at the MT4 or ER40 nose
- Customer specified spindle speeds set and run under power before shipment
- Working pressure checked within the 20 to 35 kgf/cm2 range
- Coolant circuit tested and sample threads cut and gauged before packing
Customisation Options
- Spindle speed range specified by the customer for the threads and material you run
- MT4 taper or ER40 collet spindle selected to match your tooling
- Lead screw and feed setup specified for your thread pitch
- Supply voltage frequency and phase built for your market
- Operating language manual and control plate text prepared for your workshop
How It Compares With the Alternatives
| Gear type tapping machine SB408G and SB4516G | The gear machines change pitch by swapping gears which suits a varied pitch mix; the lead screw drive here gives a steadier feed through long strokes in heavy parts |
|---|---|
| Gear type tapping machine SB6532 | SB6532 is a bench and column machine to M32 on an MT3 spindle; the SB8030 is a heavier 600 kg machine with 140 mm spindle travel MT4 or ER40 tooling and a coolant system |
| Tapping on a drilling machine | A drilling machine has no lead screw feed and no customer set speed range, so deep threads in heavy parts depend entirely on the operator |
Running the Machine
Step 1
Level and anchor the machine on its 690 x 500 mm base and connect power and coolant
Step 2
Fit the tap in the MT4 taper or the ER40 collet chuck
Step 3
Confirm the spindle speed setting matches the thread size and material
Step 4
Set the working pressure within the 20 to 35 kgf/cm2 range
Step 5
Clamp the part and align the pre-drilled hole under the spindle
Step 6
Run coolant and let the lead screw feed drive the tap through the 140 mm stroke
Step 7
Gauge the first thread of each batch before running the rest
Other Machines in Tapping
Gear Type Teeth Distance Tapping Machine SB6516 SB6532 and SB6532A
View Machine →
Gear Type Teeth Distance Tapping Machine SB408G SB4516G and SB4516A
View Machine →
Tapping Machine SWJ-10B SWJ-6 SWJ-12 SWJ-16 & SWJ-24
View Machine →
Pneumatic and Electric Threading Machine SRAM12 SRM-M16W SRM-M24 SRM-M42W
View Machine →Questions About Lead-Screw Automatic Tapping Machine SB8030
What spindle speeds does the machine come with?
Spindle speeds are customer specified. Send us your thread sizes and the material you tap and we will set the speed range before the machine is built.
What is the tapping capacity?
Maximum drilling diameter is 35 mm with 140 mm of spindle travel and 700 mm maximum from spindle nose to base.
What tooling does the spindle take?
MT4 taper or ER40 collet. Tell us which you use and we will supply the machine with that spindle.
Does the machine have coolant?
Yes. A 40 W coolant motor is fitted alongside the 2.2 kW main motor.
What are the shipping weight and case size?
630 kg gross and 600 kg net, packed at 152 x 112 x 230 cm. We confirm the figures on the proforma invoice.
How does this compare with a gear feed tapping machine?
The lead screw drives the feed directly, which gives a steadier rate through a long stroke. A change gear machine such as SB4516G suits a shop that changes pitch frequently. Tell us your thread mix and we will advise.
What are your trade and payment terms?
We quote FOB CFR and CIF. Payment is 30 percent by T/T with the order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the Lead-Screw Automatic Tapping Machine SB8030
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.