
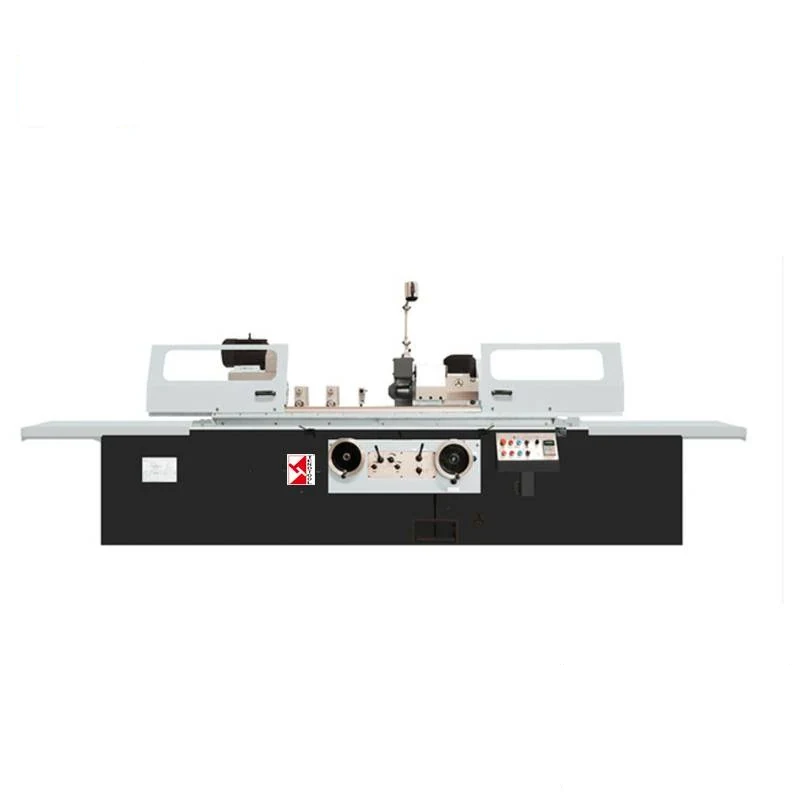
External Cylindrical Grinder M1320/M1332/M1350
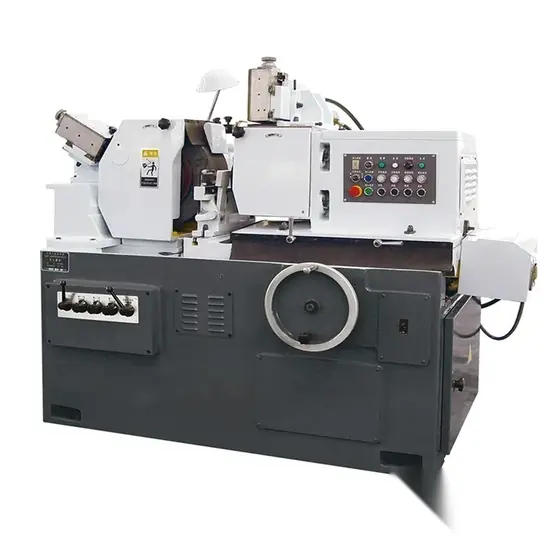
The M1320, M1332 and M1350 grind external diameters on shafts, spindles, pins and rolls to the finish and roundness a turned surface cannot reach. Wheel head cross feed is hydraulic, giving automatic periodical feed and rapid feed to and from the work, and the same feed can be taken by hand wheel for rough and fine pas...
What This Machine Does
The M1320, M1332 and M1350 grind external diameters on shafts, spindles, pins and rolls to the finish and roundness a turned surface cannot reach. Wheel head cross feed is hydraulic, giving automatic periodical feed and rapid feed to and from the work, and the same feed can be taken by hand wheel for rough and fine passes when the operator wants to control the last few microns. The work head spindle, wheel head spindle, internal grinding spindle, coolant pump and the hydrodynamic and hydrostatic oil pumps each run from a separate motor, so one load does not drag on another and the wheel holds its speed through a cut. Longitudinal table movement is hydraulic or by hand wheel, and the table swivels so tapers can be ground without special tooling. An internal grinding spindle is fitted, which means bores can be finished in the same setup as the outside diameter. Electric hydraulic and mechanical interlocks tie the moving parts together and all control levers are grouped on one panel.
Why Buyers Choose This Machine
- Hydraulic cross feed gives automatic periodical feed and rapid approach so cycle time is not lost winding the wheel in
- Hand wheel rough and fine feed lets the operator take the last passes by feel where the size is critical
- Separate motors on work head wheel head internal spindle coolant and oil pumps so loads do not interact
- Swivelling worktable grinds tapers without dedicated tooling
- Internal grinding spindle finishes bores in the same setup as the outside diameter
- Electric hydraulic and mechanical interlocks on the moving parts prevent conflicting movements
- All control levers grouped on one panel which shortens operator training
Where External Cylindrical Grinder M1320 Earns Its Place
Problems It Solves
- Turned diameters cannot hold the roundness and finish a bearing fit needs
- Hardened parts cannot be sized with a single point tool after heat treatment
- Tapers ground on fixed-table machines need special attachments
- A shared drive lets a heavy cut on one spindle pull speed off another
- Grinding the bore on a second machine loses the concentricity to the outside diameter
- Scattered controls slow down a new operator and invite wrong-lever errors
Who It Is For
- Machine shops finishing hardened shafts and spindles
- Engine and machinery repair shops regrinding worn journals
- Toolrooms producing precision pins bushes and arbors
- Bearing and hydraulic component manufacturers
- Distributors supplying conventional grinding machines to general engineering
Application Scenarios
- Finish grinding shaft and spindle diameters after turning and heat treatment
- Grinding tapered seats and cone surfaces using the swivelled table
- Bore grinding on the internal spindle in the same setup as the outside diameter
- Regrinding worn shafts and journals in a repair shop
- Sizing hardened pins and bushes that cannot be finished on a lathe
- Roll and roller finishing in a maintenance workshop
Technical Detail
Technical Features
- Hydraulic wheel head cross feed with automatic periodical feed and rapid feed
- Hand wheel rough and fine cross feed
- Separate drive motors for work head wheel head internal grinding spindle coolant pump and oil pumps
- Hydrodynamic and hydrostatic spindle bearing system
- Hydraulic or hand wheel longitudinal table movement
- Swivelling worktable for taper grinding
- Wheel dresser mountable on the worktable or on the tailstock
- Electric hydraulic and mechanical interlocks on moving parts
- Centralised control panel
Specifications
| Machine type | External cylindrical grinding machine with internal grinding spindle |
|---|---|
| Models | M1320 / M1332 / M1350 |
| Cross feed | Hydraulic automatic periodical and rapid feed, plus hand wheel |
| Table movement | Hydraulic or hand wheel, swivelling for taper |
| Spindle bearings | Hydrodynamic and hydrostatic |
| Drives | Separate motors for work head wheel head internal spindle coolant and oil pumps |
| Wheel dressing | Dresser mounts on worktable or tailstock |
| Interlocks | Electric hydraulic and mechanical on moving parts |
| Operations | External cylindrical grinding, taper grinding, internal grinding |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- External cylindrical grinding
- Taper grinding
- Internal grinding
- Wheel dressing
Quality Control
- Wheel head and work head spindle run-out measured on the assembled machine
- Table swivel scale checked against a ground taper test piece
- Hydraulic feed circuit pressure tested and periodical feed increments verified
- Interlock functions triggered and confirmed before shipment
- Test grinding run on a sample workpiece with roundness and finish checked before packing
Customisation Options
- Model selected from M1320 M1332 or M1350 against your workpiece diameter and length
- Supply voltage phase and frequency built for your market
- Grinding wheel specification and internal spindle wheels chosen for your material
- Steady rests and workholding specified for your shaft sizes
- Manual and control panel markings prepared in your working language
How It Compares With the Alternatives
| Finishing on a lathe | A lathe cannot hold roundness and surface finish on hardened material; the grinder is the machine that sizes a part after heat treatment |
|---|---|
| XAIMC surface grinding machines M71 series | The M71 machines grind flat faces; these grind round external and internal surfaces. They are complementary machines rather than alternatives |
| M1420 universal cylindrical grinding machine | The M1420 series is built around swivelled conical grinding with sliding bearing spindles; the M13 series leads on hydraulic periodical cross feed and separate drive motors |
| Grinding the bore on a separate machine | The fitted internal grinding spindle keeps bore and outside diameter concentric because neither is re-clamped |
Running the Machine
Step 1
Mount the work between centres or in the chuck and check run-out before starting
Step 2
Dress the wheel with the dresser on the table or the tailstock
Step 3
Swivel the table and set it against the scale if the part is tapered
Step 4
Select hydraulic longitudinal traverse or hand wheel for the pass you are taking
Step 5
Use automatic periodical cross feed for roughing and take the last passes on the hand wheel
Step 6
Keep coolant flowing to the wheel contact through the whole cut
Step 7
Measure the part after spark out and dress the wheel again before the next component
Related Applications and Guides
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Heavy Equipment and Plant Maintenance
Mines quarries plantations and processing plants cannot wait for imported spares. XAIMC supplies the boring gear cutting turning and grinding machines
Surface Grinder vs Cylindrical Grinder - Selecting the Right Machine
A surface grinder finishes flat faces held on a table, while a cylindrical grinder finishes round diameters held between centres or in a chuck. This c
Questions About External Cylindrical Grinder M1320
What is the difference between M1320 M1332 and M1350?
Working capacity. Send us the diameter and length of your largest workpiece and we will confirm which model covers it.
Can it grind tapers?
Yes. The worktable rotates and is positioned against a scale, so conical surfaces are ground without special attachments.
Does it do internal grinding as well?
Yes. There is an internal grinding spindle with its own motor, so a bore can be finished in the same setup and stays concentric with the outside diameter.
What accuracy can we expect?
That depends on your material, workholding, wheel and coolant. Send us a drawing of the part with the tolerance you need and we will tell you whether the machine holds it before you order.
What supply voltage is it built for?
Tell us your voltage phase and frequency with the enquiry and the machine is wired for your market before it ships.
What grinding wheels are supplied?
Wheel specification is chosen against your material and finish requirement. Tell us what you grind and we will quote the wheels and the dresser with the machine.
What are your trade and payment terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order with 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the External Cylindrical Grinder M1320
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.