
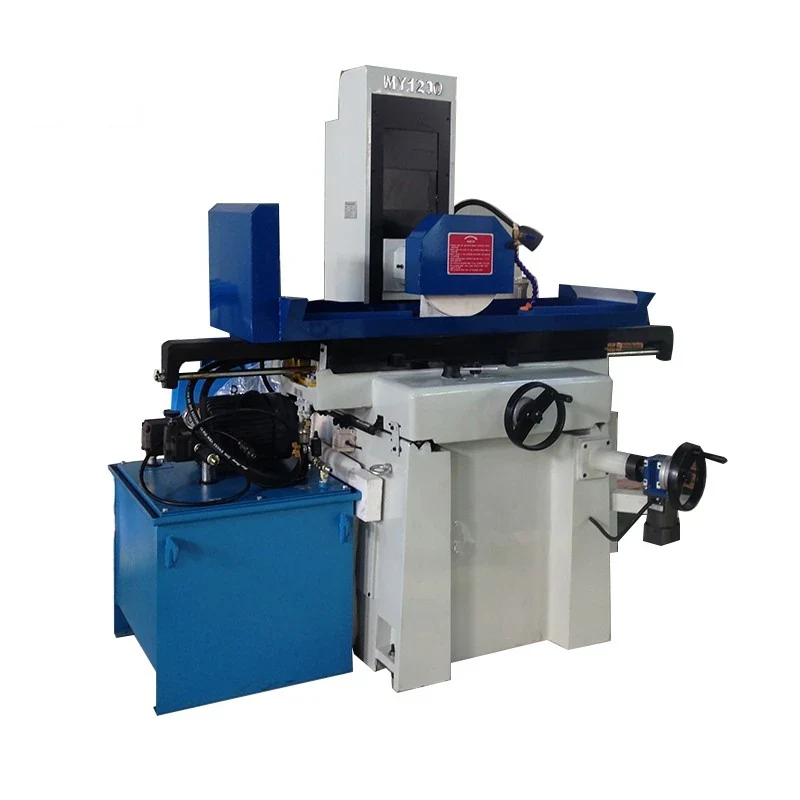
M1230 Surface Grinder Grinding Machine
The MY1230 takes workpieces up to 630x310x390mm, grinding to a maximum length of 630mm and width of 320mm, with 530mm from table surface to spindle centre so tall parts and fixtures clear the wheel. Slideways use precision plastic guide surfaces finished by precision scraping, which is the detail that decides how a man...
What This Machine Does
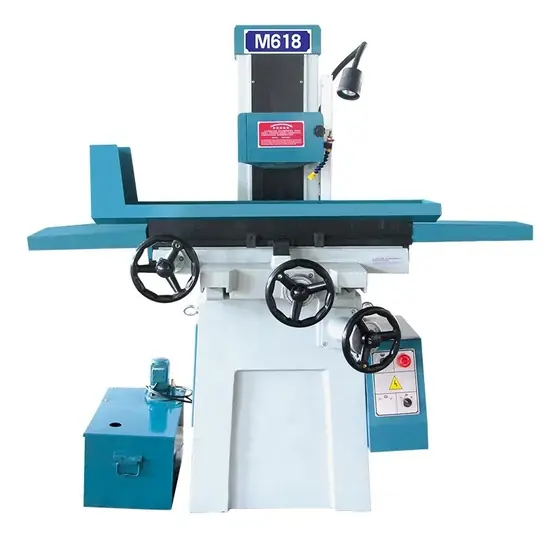
The MY1230 takes workpieces up to 630x310x390mm, grinding to a maximum length of 630mm and width of 320mm, with 530mm from table surface to spindle centre so tall parts and fixtures clear the wheel. Slideways use precision plastic guide surfaces finished by precision scraping, which is the detail that decides how a manual grinder feels and how long it holds accuracy: a scraped plastic way moves smoothly at low feed and does not stick-slip at the point where you are taking off the last few microns. Hydraulic transmission is imported and the drive is synchronous. The main mechanical valve is a purpose-built grinder valve split into two parts, mechanical commutation control and throttle control, and the throttle section carries an unloading function so the table can be started and stopped at station. The machine grinds flat surfaces and complex shaped surfaces, and takes either a permanent magnet chuck or an electromagnetic chuck depending on what the user needs to hold.
Why Buyers Choose This Machine
- 630x310x390mm workpiece capacity with 630mm grinding length covers medium plate and fixture work
- 530mm from table surface to spindle centre so tall parts and fixtures clear the wheel
- Precision plastic guide surfaces finished by precision scraping move smoothly at the low feed rates that matter on a finishing pass
- Purpose-built grinder valve splits mechanical commutation from throttle control so table reversal and feed rate are set independently
- Unloading function in the throttle section lets the table be started and stopped at station
- Grinds complex shaped surfaces as well as plain flat faces
- Permanent magnet or electromagnetic chuck fitted to suit the parts you hold
Where M1230 Surface Grinder Grinding Machine Earns Its Place
Problems It Solves
- Stick-slip on a poorly finished slideway ruins the finishing pass on a manual grinder
- A low spindle centre height means tall parts and fixtures will not pass under the wheel
- A general hydraulic valve does not give the clean table reversal a grinder needs
- Without an unloading function the table cannot be stopped cleanly at station
- Formed surfaces have to be filed or spark eroded when the grinder only does plain flats
- A fixed chuck type does not suit shops that hold both magnetic and non-standard parts
Who It Is For
- Toolrooms grinding plates blocks and formed surfaces
- Die and mould shops working within a 630mm part length
- Machine repair workshops restoring flat reference faces
- General machine shops adding surface grinding capacity
- Distributors supplying manual surface grinding machines
Application Scenarios
- Flat grinding of plates and die blocks within 630mm length
- Grinding formed and complex shaped surfaces with a dressed wheel profile
- Finishing hardened toolroom parts after heat treatment
- Machine repair work on worn flat faces
- Grinding tall fixtures that need the 530mm spindle centre height
- Small batch work where the operator controls each pass
Technical Detail
Technical Features
- Precision plastic guide surfaces with precision scraping
- Imported hydraulic transmission
- Synchronous drive
- Special grinder valve with mechanical commutation control and throttle control sections
- Unloading function for start and stop at station
- Permanent magnet or electromagnetic chuck option
- Grinding of flat and complex shaped surfaces
- Rigid structure with convenient operator access
Specifications
| Machine type | Manual surface grinding machine |
|---|---|
| Models | M1230 / MY1230 |
| Max workpiece to be ground (L x W x H) | 630x310x390mm |
| Max grinding length | 630mm |
| Max grinding width | 320mm |
| Distance from table surface to spindle centre | 530mm |
| Guideways | Precision plastic guide surfaces, precision scraped |
| Transmission | Imported hydraulic, synchronous drive |
| Workholding | Permanent magnet chuck or electromagnetic chuck |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Surface grinding
- Flat face grinding
- Form and shaped surface grinding
Quality Control
- Guideway scraping contact checked with blue before the machine is assembled
- Hydraulic circuit pressure tested and the grinder valve commutation verified through repeated reversals
- Unloading function confirmed to stop the table cleanly at station
- Grinding length and width travel measured against the 630mm and 320mm figures
- Test grind run with flatness and finish checked before packing
Customisation Options
- Permanent magnet or electromagnetic chuck specified for your parts
- Supply voltage phase and frequency built for your market
- Grinding wheel specification chosen for your material and finish
- Wheel dressing arrangement specified where you grind formed surfaces
- Manual and machine markings prepared in your working language
How It Compares With the Alternatives
| M7120 to M7140 surface grinders | Those machines run hydraulic lateral feed and a built-in motor head; the M1230 leads on its scraped plastic guideways and the purpose-built grinder valve, which is what a manual operator notices on a finishing pass |
|---|---|
| M7232 and M7240 large table grinders | The M7232 and M7240 take far longer and heavier parts; the M1230 is the machine for a 630mm part where you want the operator in control of every pass |
| Metal-on-metal slideways | The precision plastic guide surface moves without stick-slip at the low feed rates a grinder finishes on, which is where a metal way tends to grab |
| Spark eroding a formed surface | Grinding a dressed wheel profile into the part is faster and leaves a ground finish rather than an eroded skin |
Running the Machine
Step 1
Fit the chuck type suited to the part and clean the chuck face before seating the work
Step 2
Check the part clears within 630x310x390mm and under the 530mm spindle centre height
Step 3
Let the hydraulics reach working temperature before cutting to size
Step 4
Dress the wheel, profiling it first if you are grinding a shaped surface
Step 5
Set the throttle control for table feed rate independently of the commutation setting
Step 6
Take light passes with coolant and use the unloading function to stop at station between parts
Step 7
Spark out on the final pass and measure the part off the machine
Related Applications and Guides
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
Heavy Equipment and Plant Maintenance
Mines quarries plantations and processing plants cannot wait for imported spares. XAIMC supplies the boring gear cutting turning and grinding machines
Surface Grinder vs Cylindrical Grinder - Selecting the Right Machine
A surface grinder finishes flat faces held on a table, while a cylindrical grinder finishes round diameters held between centres or in a chuck. This c
Questions About M1230 Surface Grinder Grinding Machine
What is the largest part it will grind?
630x310x390mm, with a maximum grinding length of 630mm and width of 320mm. Distance from table surface to spindle centre is 530mm, so check your fixture height against that too.
Which chuck is supplied?
Either a permanent magnet or an electromagnetic chuck, fitted according to what you need to hold. Tell us your part material and size and we will advise which one suits.
Can it grind shaped surfaces or only flats?
Both. It grinds plain planes and complex shaped surfaces, working from a dressed wheel profile.
What accuracy will we get?
That depends on your material, fixturing, wheel and how the part was heat treated. Send us the drawing with your flatness and finish requirement and we will confirm before you order.
Why plastic guideways?
The guide surfaces are precision plastic finished by precision scraping. They move smoothly at the very low feed rates used on a finishing pass, where a plain metal way tends to stick and then jump.
Can it be built for our supply voltage?
Yes. Confirm your voltage phase and frequency at enquiry and the machine is wired for your market.
What are your payment and trade terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the M1230 Surface Grinder Grinding Machine
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.