
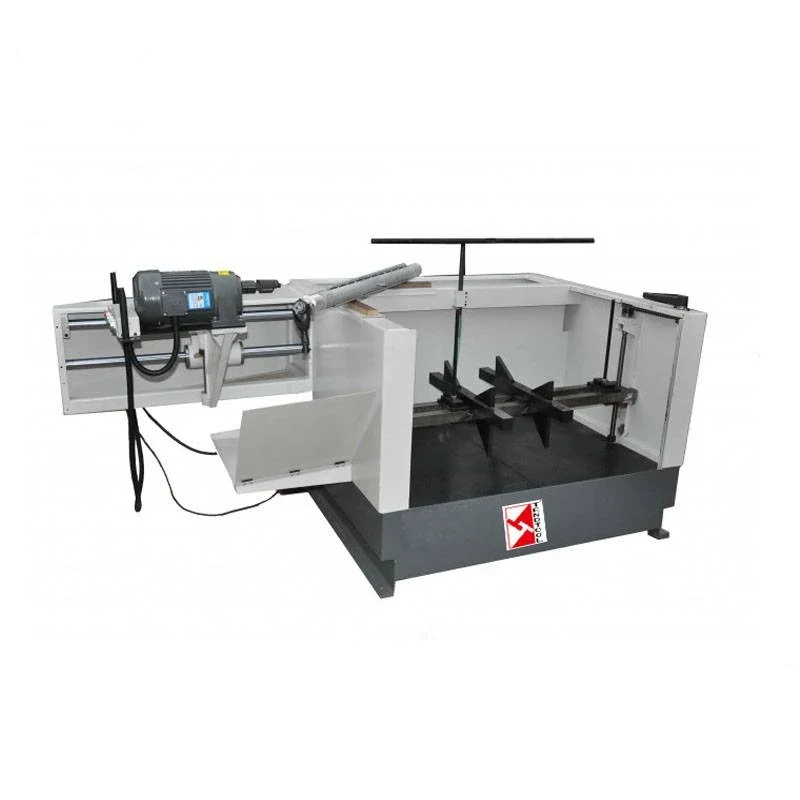
Line Honing Machine LH100
The LH100 hones the main bearing bore line of an engine block back into alignment instead of boring it. Once a block has been run hard the main bore line distorts through warpage and cap stretch, and the caps have to be brought back to a true, round, correctly sized line before new bearings will carry load evenly. Line...
What This Machine Does
The LH100 hones the main bearing bore line of an engine block back into alignment instead of boring it. Once a block has been run hard the main bore line distorts through warpage and cap stretch, and the caps have to be brought back to a true, round, correctly sized line before new bearings will carry load evenly. Line honing takes off the minimum stock needed, usually less than .003 inch (.076 mm) from the caps against as much as .010 inch (.254 mm) when the same job is bored, so the block keeps more of its original material and the crank centreline barely moves. The machine covers main bearing bores from 46 to 178 mm, with special tooling for the 127 to 178 mm range, and takes 90 and 60 degree V blocks as well as overhead and L-head in-line blocks up to 1140 mm long and 710 mm from head deck to main bearing centreline. Setup is quick and the machine does not need specially trained operators.
Why Buyers Choose This Machine
- Minimum stock removal usually under .003 inch (.076 mm) off the caps against as much as .010 inch (.254 mm) with boring
- Corrects main bore distortion from warpage and cap stretch rather than just resizing a bent line
- Meets or exceeds original factory accuracy for alignment roundness and size
- Covers main bearing bores from 46 to 178 mm so one machine handles car through heavy-duty blocks
- Takes 90 and 60 degree V blocks plus overhead and L-head in-line blocks up to 1140 mm long
- Fast easy setup with no special operator training required
- Turns main bore work into a chargeable in-house service instead of an outside job
Where Line Honing Machine LH100 Earns Its Place
Problems It Solves
- A distorted main bore line wipes new bearings out soon after the engine goes back together
- Line boring removes far more cap material than the repair actually needs
- Cap stretch leaves the bore out of round in a way that new bearings cannot compensate for
- Sending blocks out for main bore work adds a transport leg and days of delay to every rebuild
- Hand-fitting caps cannot hold alignment roundness and size across a bore line
Who It Is For
- Engine rebuilders who currently send main bore work out to a subcontractor
- Truck bus and plant fleet workshops reconditioning their own blocks
- Performance and race engine builders correcting cap stretch
- Machine shops adding main bore reconditioning to an existing service list
- Distributors equipping engine rebuild workshops in export markets
Application Scenarios
- Restoring main bearing bore alignment on a block that has been run with a spun bearing
- Correcting cap stretch after high-load or performance engine service
- Preparing 90 and 60 degree V blocks for main bearing fitting in a rebuild line
- Line honing in-line overhead and L-head blocks up to 1140 mm long
- Sizing main bores after caps have been ground and refitted
- Offering main bore reconditioning as a subcontract service to other shops
Technical Detail
Technical Features
- Main bearing bore diameter range 46 to 178 mm (1.800 to 7.000 in)
- Special tooling available for the 127 to 178 mm (5.000 to 7.000 in) range
- Capacity for 90 and 60 degree V blocks and overhead and L-head in-line blocks
- Block capacity up to 1140 mm (45 in) long
- Up to 710 mm (28 in) from head deck to main bearing centreline
- Honing process holds alignment roundness and size together in one operation
- Setup arranged for quick changeover between block types
Specifications
| Machine type | Line honing machine for engine main bearing bores |
|---|---|
| Models | LH100 |
| Main bearing bore diameter range | 46 - 178 mm (1.800 - 7.000 in) |
| Special tooling range | 127 - 178 mm (5.000 to 7.000 in) |
| Block capacity | V blocks both 90 and 60 degree; overhead and L-head in-line blocks |
| Max block length | 1140 mm (45 in) |
| Head deck to main bearing centreline | 710 mm (28 in) |
| Typical stock removal | Usually less than .003 in (.076 mm) off the caps |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Line honing
- Main bearing bore alignment
- Bore sizing
Quality Control
- Main bore alignment checked along the full bore line on a test block
- Bore roundness and size verified against the target bearing dimension
- Stock removal checked to confirm it stays within the expected .076 mm band
- Tooling run-out inspected on assembly before the machine is run in
- Full function test through a complete honing cycle before packing
Customisation Options
- Tooling specified for your main bearing bore range including the 127 to 178 mm special tooling if needed
- Fixturing arranged for the V and in-line block types you actually run
- Supply voltage and frequency set for your market
- Stone grades selected for the block and cap material you work with
- Manual and machine labelling prepared in the language your shop needs
How It Compares With the Alternatives
| Line boring machine LB100 | Boring removes as much as .010 in (.254 mm) from the caps; line honing usually takes under .003 in (.076 mm) and leaves the block with more material for a future rebuild |
|---|---|
| Replacing the block | A distorted main bore line is repairable on the LH100; replacing the block is a far larger cost for a fault the machine corrects |
| Hand scraping and fitting caps | Hand work cannot hold alignment roundness and size together across the bore line; the LH100 works all three in one honing pass |
Running the Machine
Step 1
Grind and refit the main caps so the bore is slightly undersize before honing
Step 2
Mount the block on the machine and set it square to the bore line
Step 3
Select tooling for the main bearing bore diameter using the special tooling above 127 mm
Step 4
Set the stones and take a light first pass
Step 5
Measure alignment roundness and size along the line before continuing
Step 6
Hone to final size checking the bore against the bearing dimension
Step 7
Clean the block thoroughly so no abrasive is left in the oil galleries
Other Machines in Engine Rebuilding Machine
Cylinder Block Grinding-Milling Machine 3M9735B
View Machine →
Line Boring Machine LB100
View Machine →
Line Boring Machine T8120*20/T8120SF/LB2300
View Machine →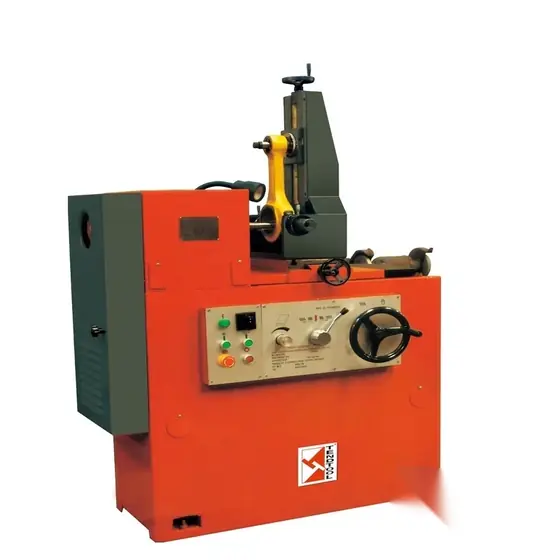
Con-Rod Bushing Boring Machine T8216/T8210D
View Machine →Related Applications and Guides
Engine Rebuilding Workshops
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies
Automotive Service and Fleet Workshops
Service centres and fleet depots keep vehicles moving. XAIMC supplies the lifting tyre wheel and fluid handling equipment those workshops use, includi
Cylinder Boring vs Honing - What Each Operation Does
Boring removes metal to bring a worn cylinder back to a round straight bore at a new oversize, while honing produces the final diameter, geometry and
How to Choose a Valve Seat Cutting Machine
A valve seat cutting machine machines the seat angles and the valve guide bore in a cylinder head so that the valve seals concentrically against the s
Questions About Line Honing Machine LH100
What main bearing bore sizes does the LH100 cover?
46 to 178 mm (1.800 to 7.000 in). Special tooling is required for the 127 to 178 mm (5.000 to 7.000 in) range, so tell us your largest bore when you enquire.
How much material does line honing take off the caps?
Usually less than .003 in (.076 mm), compared with as much as .010 in (.254 mm) when the same line is bored.
What size blocks will it take?
V blocks in both 90 and 60 degree, plus overhead and L-head in-line blocks, up to 1140 mm (45 in) long and 710 mm (28 in) from head deck to main bearing centreline.
Does my operator need special training?
No special training is required. Setup is straightforward and the machine is designed to be operated by an ordinary rebuild technician.
Can it correct distortion or only resize the bore?
It corrects distortion caused by warpage and cap stretch, and works to meet or exceed original factory accuracy for alignment roundness and size.
What are your trade and payment terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
What is the lead time?
Lead time depends on the tooling package and voltage specified. Send us your bore range and market voltage and we will confirm a date with the quotation.
Request a Quote on the Line Honing Machine LH100
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.