
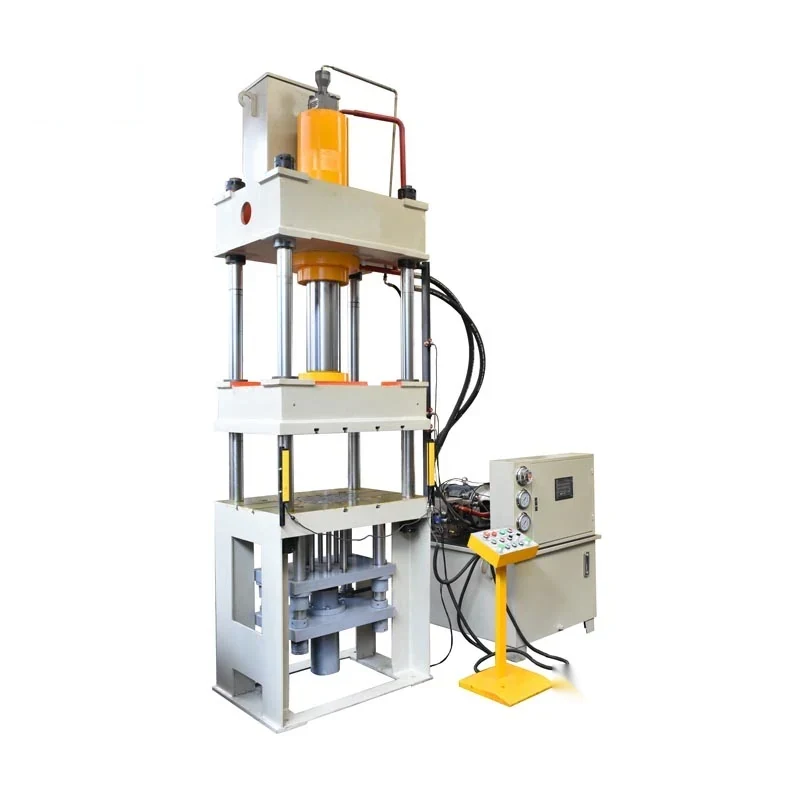
Y32 Four Column Hydraulic Press Machine
The Y32 is a four-column hydraulic press for deep drawing and forming metal products, built in double-action form so the blank holder and the drawing ram work separately. Two electrical control systems are offered, conventional relay control and PLC control, and the press runs in adjustment, manual or semi-automatic mo...
What This Machine Does
The Y32 is a four-column hydraulic press for deep drawing and forming metal products, built in double-action form so the blank holder and the drawing ram work separately. Two electrical control systems are offered, conventional relay control and PLC control, and the press runs in adjustment, manual or semi-automatic mode. It can be set for constant-pressure forming, where the press holds pressure after the stroke and then returns automatically, or for fixed-distance working where the stroke is set and repeated. The worktable carries an ejector, so formed parts are pushed out of the die instead of being levered free. The same ejector can be used as a hydraulic die cushion to support the drawing operation, with working pressure and travel adjustable within the machine range to suit the part. The hydraulic system comprises motors, oil pumps, control valve manifolds, tanks and connecting pipework. The Y32 range covers presses from 63T to 2000T.
Why Buyers Choose This Machine
- Double-action layout holds the blank while the punch draws so deep parts do not wrinkle or tear
- Constant-pressure mode holds the part at pressure then returns the ram automatically
- PLC or conventional relay control offered so the shop can match its own maintenance skills
- Adjustment manual and semi-automatic modes cover die setting and production on one press
- Table ejector pushes formed parts out of the die instead of the operator levering them free
- Ejector doubles as a hydraulic die cushion for drawing work with adjustable pressure and travel
- Four-column frame guides the ram squarely so die halves stay in alignment
Where Y32 Four Column Hydraulic Press Machine Earns Its Place
Problems It Solves
- Drawn parts wrinkle or split when the blank is not held while the punch descends
- Single-mode presses cannot be slowed for die setting without stopping production settings
- Formed parts stick in the die and are damaged when levered out by hand
- Pressure and stroke that cannot be adjusted force a die change for every new part
- Ram misalignment on two-column frames wears die guides and punches
Who It Is For
- Metal-forming factories running drawn and pressed steel parts
- Toolrooms and die shops needing a press with adjustable pressure and stroke
- Appliance and hardware manufacturers forming sheet components
- Machinery importers supplying forming presses to fabrication plants
Application Scenarios
- Deep drawing cookware tanks covers and pressed steel housings
- Forming and bending sheet metal components in medium and large batches
- Powder and plastic moulding work where a controlled pressure dwell is needed
- Straightening and pressing assembly work on heavy fabricated parts
- Die trials and die proving in a toolroom before production runs
Technical Detail
Technical Features
- Four-column frame with double-action deep drawing arrangement
- Two electrical control systems offered conventional and PLC
- Adjustment manual and semi-automatic operating modes
- Constant-pressure forming with automatic return after pressure dwell
- Fixed-distance stroke setting for repeat production
- Worktable ejector usable as a hydraulic die cushion
- Working pressure and stroke travel adjustable within the machine range
- Hydraulic system with motors oil pumps control valve manifolds and oil tank
Specifications
| Machine type | Four column double-action deep drawing hydraulic press |
|---|---|
| Models | Y32 series 63T 100T 160T 200T 315T 630T 1000T 2000T |
| Frame | Four column construction |
| Control | Conventional electrical control or PLC control |
| Operating modes | Adjustment manual and semi-automatic |
| Working modes | Constant pressure forming and fixed distance stroke |
| Worktable | Ejector fitted usable as hydraulic die cushion |
| Hydraulic system | Motors oil pumps control valve manifolds and oil tank |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Deep drawing
- Forming
- Bending
- Stamping
- Straightening
Quality Control
- Hydraulic system pressure tested and checked for leaks before despatch
- Ram squareness and parallelism to the table checked on the assembled press
- Control system run through adjustment manual and semi-automatic modes
- Ejector travel and die cushion pressure verified through full stroke
- Press run in under load before packing
Customisation Options
- Tonnage selected from the Y32 range between 63T and 2000T for your part
- Conventional or PLC electrical control specified with the order
- Table size and die space matched to the tooling you already run
- Supply voltage and frequency set to your market
- Operating language for control labels and manual
How It Compares With the Alternatives
| Single-action hydraulic press | A single-action press has no separate blank holder, so deep drawn parts wrinkle at the flange; the double-action Y32 holds the blank through the draw |
|---|---|
| Mechanical crank press | A crank press gives a fixed stroke and fixed force curve; the Y32 lets you set working pressure and stroke travel within the machine range for the part |
| Operated hydraulic press MDY100/35 | The MDY100/35 is a hand-controlled workshop press for repair and light forming; the Y32 is a production forming press with die cushion and programmable modes |
Running the Machine
Step 1
Mount the die and set the ram stroke in adjustment mode before running production
Step 2
Choose constant-pressure or fixed-distance working according to the part
Step 3
Set the blank holder force and the die cushion pressure within the machine range
Step 4
Run the first part in manual mode and check the draw for wrinkles and thinning
Step 5
Switch to semi-automatic once the setting is proved and check parts at intervals
Step 6
Check the oil level filters and pipework for leaks as part of routine maintenance
Other Machines in Press Machine
Related Applications and Guides
Sheet Metal Fabrication
Sheet metal shops cut, bend, roll and form. XAIMC supplies shears press brakes plate rolls tube benders and fibre laser cutting across the manual to C
Questions About Y32 Four Column Hydraulic Press Machine
Which tonnage should I order?
The Y32 range runs from 63T to 2000T. Send us a drawing of the part, the material and thickness and the draw depth, and we will recommend the tonnage in writing.
What is the difference between constant pressure and fixed distance working?
In constant-pressure working the press holds pressure after the stroke and then returns automatically. In fixed-distance working the stroke is set and repeated, which suits parts controlled by depth rather than by force.
Can I have PLC control?
Yes. The press is offered with conventional electrical control or with PLC control. State which you want on the order, as it changes the electrical build.
Can the press be used for die cushion work?
Yes. The ejector in the worktable can be used as a hydraulic die cushion to support the drawing operation, and its pressure and travel are adjustable within the machine range.
What voltage will the machine be supplied for?
Tell us your supply voltage, phases and frequency with the order and the machine will be built and tested to that supply.
What are your trade and payment terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
How are spare parts handled after delivery?
Send us the machine model and the part you need from the hydraulic or electrical system and we will quote spares against your machine record.
Request a Quote on the Y32 Four Column Hydraulic Press Machine
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.