
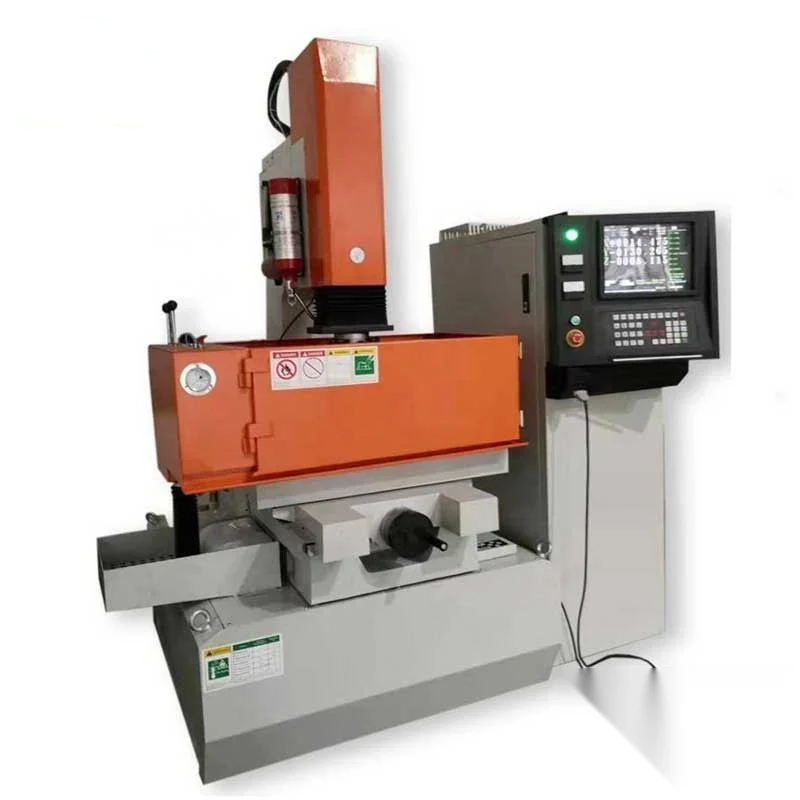
D7135 CNC Electric Discharge
The D7135 is a CNC sinker EDM for cavities, holes and special shaped parts in copper, plumbago and steel, the work a cutting tool cannot reach because the form is internal, sharp-cornered or in material too hard to mill. The machine was laid out using special CAD software, and the structure includes a properly arranged...
What This Machine Does
The D7135 is a CNC sinker EDM for cavities, holes and special shaped parts in copper, plumbago and steel, the work a cutting tool cannot reach because the form is internal, sharp-cornered or in material too hard to mill. The machine was laid out using special CAD software, and the structure includes a properly arranged back-oil groove so the working oil returns cleanly instead of pooling on the machine. The principal axis is driven by a high precision DC servomotor working through a precision screw made in Taiwan, with spindle box lubrication, so the axis runs without noise, without heating and with low friction, which is what holds accuracy through a long burn. X and Y axes use high precision preloaded bearings on high precision ball screws, giving the rigidity the electrode needs while keeping the axes easy to drive. Scrap removal is selectable: sweeping oil, sucking oil, or a process where the workpiece is not submerged in oil at all, so the flushing method is matched to the cavity rather than fixed by the machine.
Why Buyers Choose This Machine
- Machines cavities holes and special shaped parts that a cutting tool cannot produce
- Works in copper plumbago and steel including material too hard to mill
- High precision DC servomotor on the principal axis for controlled electrode feed through a long burn
- Precision screw made in Taiwan with spindle box lubrication runs quietly without heating and with low friction
- High precision preloaded bearings on ball screws for X and Y give rigidity without making the axes heavy to drive
- Choice of sweeping oil sucking oil or non-submerged processing so flushing is matched to the cavity
- Back-oil groove designed into the structure so working oil returns cleanly and the machine stays clean
Where D7135 CNC Electric Discharge Earns Its Place
Problems It Solves
- A milling cutter cannot produce a sharp internal corner because it has a radius
- Hardened tool steel cannot be cut with a conventional tool after heat treatment
- Deep cavities trap debris and the burn stalls without the right flushing method
- A screw that heats up under a long burn takes the accuracy of the cavity with it
- Fixed flushing means the machine dictates the process rather than the part
- Working oil pooling on the machine makes a mess and makes maintenance harder
Who It Is For
- Mould and die shops producing injection and press tooling
- Toolrooms machining hardened steel after heat treatment
- Manufacturers of parts with internal forms and sharp corners
- Workshops machining copper and graphite components
- Distributors supplying CNC sinker EDM to tooling industries
Application Scenarios
- Sinking cavities into hardened mould and die steel
- Producing sharp internal corners a milling cutter cannot reach
- Machining graphite and copper electrodes and components
- Burning holes in hardened parts after heat treatment
- Special shaped detail work on plastic injection mould cores and cavities
- Work where the part cannot be submerged and needs a non-submerged process
Technical Detail
Technical Features
- Designed with special CAD software
- Structure with back-oil groove for clean oil return
- Principal axis on high precision DC servomotor
- Precision screw made in Taiwan on the principal axis
- Spindle box lubrication without noise or high temperature
- X and Y axes on high precision preloaded bearings
- High precision ball screws on X and Y
- Selectable scrap removal by sweeping oil or sucking oil
- Non-submerged processing option
- Processes copper plumbago and steel
Specifications
| Machine type | CNC electric discharge machine, sinker EDM |
|---|---|
| Models | D7135 |
| Principal axis drive | High precision DC servomotor |
| Principal axis screw | Precision screw made in Taiwan |
| Principal axis lubrication | Spindle box lubrication |
| X and Y axes | High precision preloaded bearings on high precision ball screws |
| Scrap removal | Sweeping oil, sucking oil, or non-submerged process |
| Workpiece materials | Copper, plumbago, steel |
| Typical work | Cavity, hole and special shape parts |
| Design | Laid out with special CAD software, back-oil groove in the structure |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Electrical discharge machining
- Cavity sinking
- Hole burning
- Special shape machining
Materials Handled
- Copper
- Plumbago
- Steel
Quality Control
- Principal axis servo feed tested through a full burn cycle for stable electrode control
- Ball screw and preloaded bearing backlash measured on X and Y before release
- Spindle box lubrication verified and axis running temperature checked under load
- All three flushing methods run and confirmed before shipment
- Test burn made on a sample cavity with form and finish inspected before packing
Customisation Options
- Flushing arrangement specified as sweeping oil sucking oil or non-submerged for your typical part
- Supply voltage phase and frequency built for your market
- Electrode holding and tooling specified for the cavities you produce
- Dielectric tank and filtration arrangement specified with the machine
- Control language and manual prepared for your shop
How It Compares With the Alternatives
| Milling a cavity | Milling is faster where it can reach, but it leaves a corner radius and cannot cut hardened steel; EDM produces sharp internal corners in material after heat treatment |
|---|---|
| Submerged only EDM machines | The D7135 can also run a process where the workpiece is not submerged in oil, which is an option a fixed submerged machine does not give you |
| Manual sinker EDM | A manual machine depends on the operator watching and adjusting the burn; the DC servo principal axis under CNC control holds electrode feed itself |
| Grinding a form into hardened steel | Grinding needs access to the surface with a wheel; EDM reaches internal cavities and blind holes that a wheel cannot get into |
Running the Machine
Step 1
Set the workpiece and check the cavity form against the electrode before starting
Step 2
Choose the scrap removal method that suits the cavity, sweeping oil, sucking oil or non-submerged
Step 3
Set the electrode and reference the axes on the CNC control
Step 4
Start the burn at a conservative setting and confirm the discharge is stable
Step 5
Watch that flushing is clearing debris, particularly on a deep cavity
Step 6
Finish with a lighter setting to bring the surface to the finish the tool needs
Step 7
Keep the back-oil groove and dielectric filtration clean as part of routine maintenance
Other Machines in EDM
Questions About D7135 CNC Electric Discharge
What materials can it machine?
Copper, plumbago and steel, including hardened steel that cannot be cut with a conventional tool. Tell us the material and hardness of your work and we will advise on electrode material and settings.
Does the workpiece have to be submerged in oil?
No. You can choose sweeping oil or sucking oil for scrap removal, or run a process where the workpiece is not submerged. The right choice depends on the cavity, and we can advise from your drawing.
What accuracy and surface finish can we expect?
That depends on the electrode, the material and the settings you run. Send us the cavity drawing with the tolerance and surface finish you need and we will confirm before you order.
Why does the screw matter?
The principal axis uses a precision screw made in Taiwan with spindle box lubrication, so the axis runs without noise or high temperature and with low friction. A screw that heats up during a long burn moves and takes the cavity accuracy with it.
Can it be supplied for our supply voltage?
Yes. Give us your voltage phase and frequency at enquiry and the machine is built for your market.
Are electrodes and tooling supplied?
Electrode holding and tooling are specified against the cavities you produce. Send us a typical part and we will quote the tooling with the machine.
What are your payment and trade terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the D7135 CNC Electric Discharge
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.