
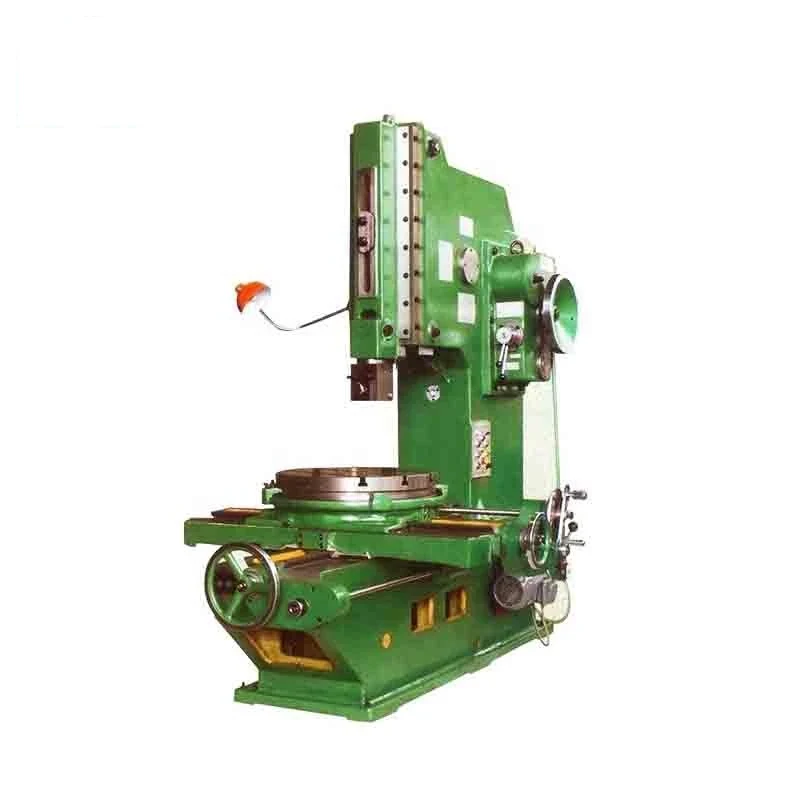
B5020/B5032/B5040/B5050 Vertical Slotting Machine
A vertical slotting machine cuts with a downward stroke, which is what makes it the practical way to produce internal keyways splines and square or profiled holes inside a bore that a milling cutter cannot reach. The B5020 B5032 B5040 and B5050 cover that work across four sizes, from single parts to small batch runs in...
What This Machine Does
A vertical slotting machine cuts with a downward stroke, which is what makes it the practical way to produce internal keyways splines and square or profiled holes inside a bore that a milling cutter cannot reach. The B5020 B5032 B5040 and B5050 cover that work across four sizes, from single parts to small batch runs in a general workshop. The main motion comes from a rotary variable handle gear mechanism which also drives longitudinal feed, and hydraulic transmission gives the sliding pillow its reciprocating stroke together with hydraulic feed at the table. The table itself feeds in three directions, longitudinal horizontal and rotary, so a part clamped once can have several surfaces machined without being disturbed and losing its reference. The machines run on a three-phase AC supply at 380 volts 50 Hz. Panels and covers are laid out for straightforward maintenance so routine servicing does not need the machine stripped.
Why Buyers Choose This Machine
- Vertical stroke reaches internal keyways and splines inside bores that milling cutters cannot enter
- Three feed directions at the table machine several surfaces from one clamping
- Hydraulic drive to the sliding pillow gives a smooth reciprocating stroke without gear shock
- Hydraulic table feed keeps feed pressure steady through the cut
- Rotary feed with the variable handle gear mechanism suits circular and indexed work
- Four sizes from B5020 to B5050 match the machine to the stroke and part size you need
- Standard 380 V 50 Hz three-phase supply and an accessible layout for maintenance
Where B5020 Earns Its Place
Problems It Solves
- Internal keyways cannot be cut on a mill without broaching tooling that is expensive for one part
- Broach sets only fit one size so odd keyway sizes wait for tooling that never arrives
- Re-clamping to reach another face loses the original reference and adds error
- Mechanical stroke drives shock the tool at the reversal point and mark the cut
- Hand feeding through a deep slot gives uneven pressure and a stepped wall
- Spaced internal forms around a bore need a rotary feed that hand setups cannot repeat
Who It Is For
- Gear and transmission repair shops cutting internal keyways
- Plant maintenance workshops making and repairing drive components
- Jobbing machine shops handling single and small batch orders
- Toolrooms producing dies and profiled internal forms
- Distributors supplying conventional machine tools to industrial buyers
Application Scenarios
- Cutting internal keyways in gears sprockets pulleys and couplings
- Producing square hexagonal and profiled internal holes
- Machining internal splines and serrations on hubs
- Cutting slots and flat faces on single parts in a maintenance workshop
- Small batch slotting work in a jobbing shop
- Machining several surfaces of a housing from one clamping using the three feed directions
Technical Detail
Technical Features
- Vertical slotting stroke with sliding pillow driven by hydraulic transmission
- Hydraulic feed device for the worktable
- Rotary variable handle gear mechanism as the main turning motion with longitudinal feed
- Worktable feed in three directions longitudinal horizontal and rotary
- Four model sizes B5020 B5032 B5040 and B5050
- Three-phase AC supply 380 volts 50 Hz
- Layout arranged for easy maintenance access
Specifications
| Machine type | Vertical slotting machine heavy duty |
|---|---|
| Models | B5020 / B5032 / B5040 / B5050 |
| Main motion | Rotary variable handle gear mechanism |
| Ram drive | Hydraulic transmission to the sliding pillow |
| Table feed | Hydraulic feed in longitudinal horizontal and rotary directions |
| Power supply | Three-phase AC 380 V 50 Hz |
| Applications | Planes forms and keyways including internal keyways in bores |
| Production type | Single piece and small batch production |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Slotting
- Internal keyway cutting
- Spline cutting
- Profiled hole machining
- Flat surface machining
Quality Control
- Sliding pillow guideways checked for straightness and bearing contact during assembly
- Hydraulic system pressure tested and checked for leaks before running
- Stroke reciprocation and table feed run through the full range in all three directions
- Rotary feed checked for repeat position
- Machine run in and test cut on a sample workpiece before painting and packing
Customisation Options
- B5020 B5032 B5040 or B5050 selected against your stroke length and part size
- Supply voltage and frequency changed from 380 V 50 Hz where your market requires it
- Slotting tool holders specified for the keyway widths and depths you cut
- Machine plates and operating manual prepared in your working language
- Export packing specified for your shipping route and port
How It Compares With the Alternatives
| B6050 horizontal metal shaper | The shaper strokes horizontally and suits external flats and long faces; the slotting machine strokes vertically and is the machine that reaches internal keyways inside a bore |
|---|---|
| Keyway broaching with a press and broach set | Broaching is fast once you own the broach for that size; the slotting machine cuts any keyway width and depth with a ground tool and no size-specific tooling |
| Mechanically driven slotting machines | Hydraulic transmission to the sliding pillow and hydraulic table feed give a smoother stroke and steadier feed pressure than a purely mechanical drive |
Running the Machine
Step 1
Clamp the part on the table and set the internal reference against the bore
Step 2
Set the stroke length and stroke position so the tool clears the work at the top of travel
Step 3
Fit and set the slotting tool for the keyway width and rake required
Step 4
Select the feed direction longitudinal horizontal or rotary and set the feed amount
Step 5
Check hydraulic oil level and let the system reach working temperature before cutting
Step 6
Take a trial pass and measure the slot before working down to full depth
Step 7
Work to depth in successive passes rather than forcing a single deep cut
Other Machines in Slotting
Related Applications and Guides
Heavy Equipment and Plant Maintenance
Mines quarries plantations and processing plants cannot wait for imported spares. XAIMC supplies the boring gear cutting turning and grinding machines
Questions About B5020
Which model should I choose?
The four models B5020 B5032 B5040 and B5050 differ in working size. Send us the bore diameter keyway width and slot depth you cut most often and we will confirm the model.
Can it cut internal keyways in a blind bore?
A slotting machine cuts on a downward stroke and needs tool run-out clearance at the bottom of the slot. Send us the part drawing and we will confirm whether your blind bore leaves enough clearance.
What power supply does the machine need?
Standard supply is three-phase AC 380 volts 50 Hz. Tell us your local voltage and frequency and we will build the machine accordingly.
Is the table feed automatic?
Yes. The worktable has a hydraulic feed device and feeds in three directions, longitudinal horizontal and rotary, so several surfaces can be machined from one clamping.
Are slotting tools included?
Tooling is quoted against the keyway sizes you cut. Send us your keyway widths and depths and we will specify the tool holders and tools with the machine.
What are your trade and payment terms?
We quote FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
How long does maintenance take on these machines?
The machine is laid out for easy maintenance access. Routine work is limited to lubrication hydraulic oil checks and guideway cleaning, which does not require the machine to be stripped.
Request a Quote on the B5020
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.