Cap Visual Inspection
Reliable Cap Visual Inspection System with 6-Camera High-Speed AI Full-Area Defect Detection
Inspection Speed: 300pcs/min~2500pcs/min
View specification →
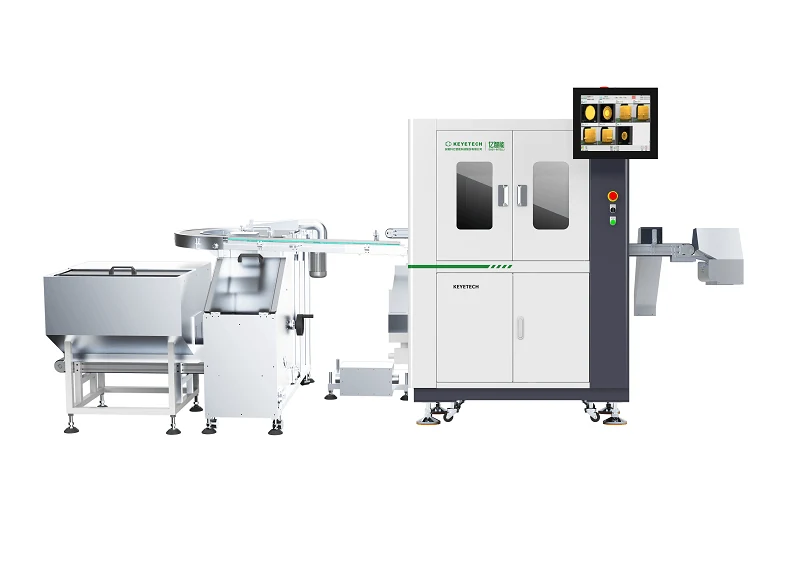
The largest family in our range. These systems inspect plastic closures for water, beverage, dairy, daily chemical and pharmaceutical packaging at production speed, and remove the failures without stopping the line.
A cap is a hard part to inspect because the defects hide in three different places. The top face shows colour difference, black spots and stains. The sidewall shows flashing, notches and knurl damage. The inside shows thread defects, compression and broken rings, double or reversed gaskets, inner plugs and mould numbers. Covering all three needs more than one camera and more than one lighting geometry.
Our cap systems use six to sixteen industrial cameras with self-developed strobe LED light sources. An integrated cavity light source gives even illumination on the sidewall, which is where most single-camera systems produce false rejects. Detection precision is 0.1 mm and inspection speed runs from 300 to 2500 pieces per minute depending on the camera count and how tight your tolerance is.
Rejection is by high-speed air valve, so throughput is not limited by a mechanical pusher. Good caps are counted and divided into boxes automatically, which removes a second manual operation.
Each entry carries the specification table and FAQ published for that configuration.
Inspection Speed: 300pcs/min~2500pcs/min
View specification →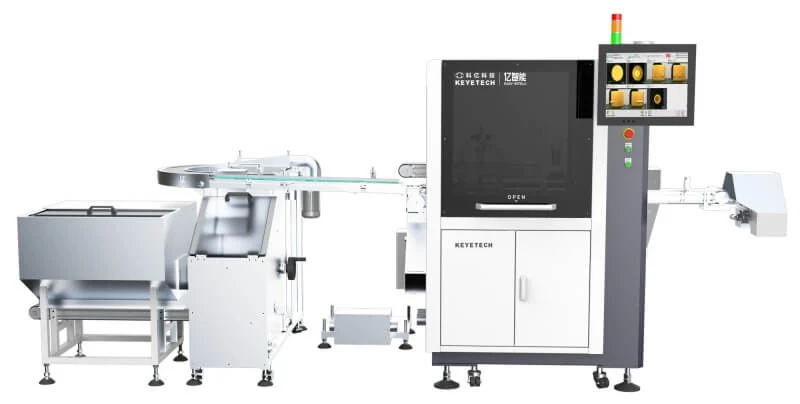
Inspection Speed: 300~2500pcs/min
View specification →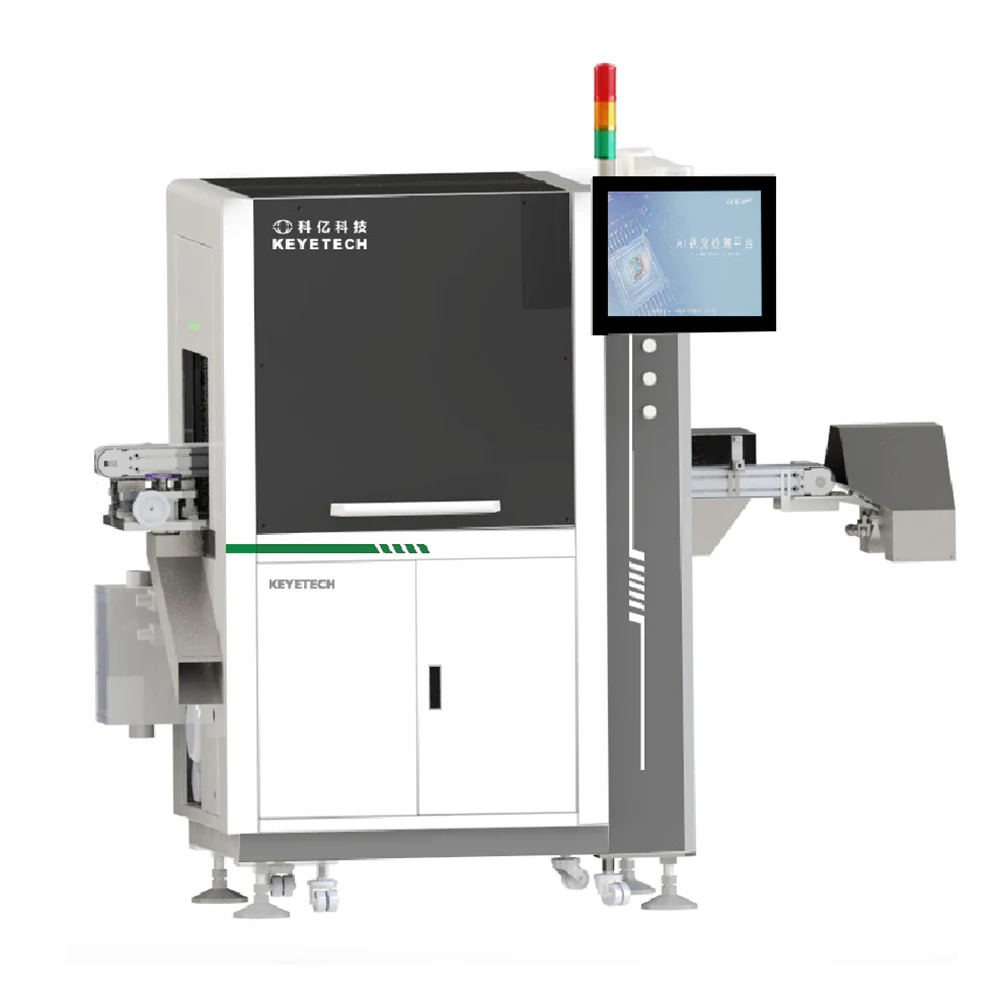
Inspection Speed: 300~2500pcs/min
View specification →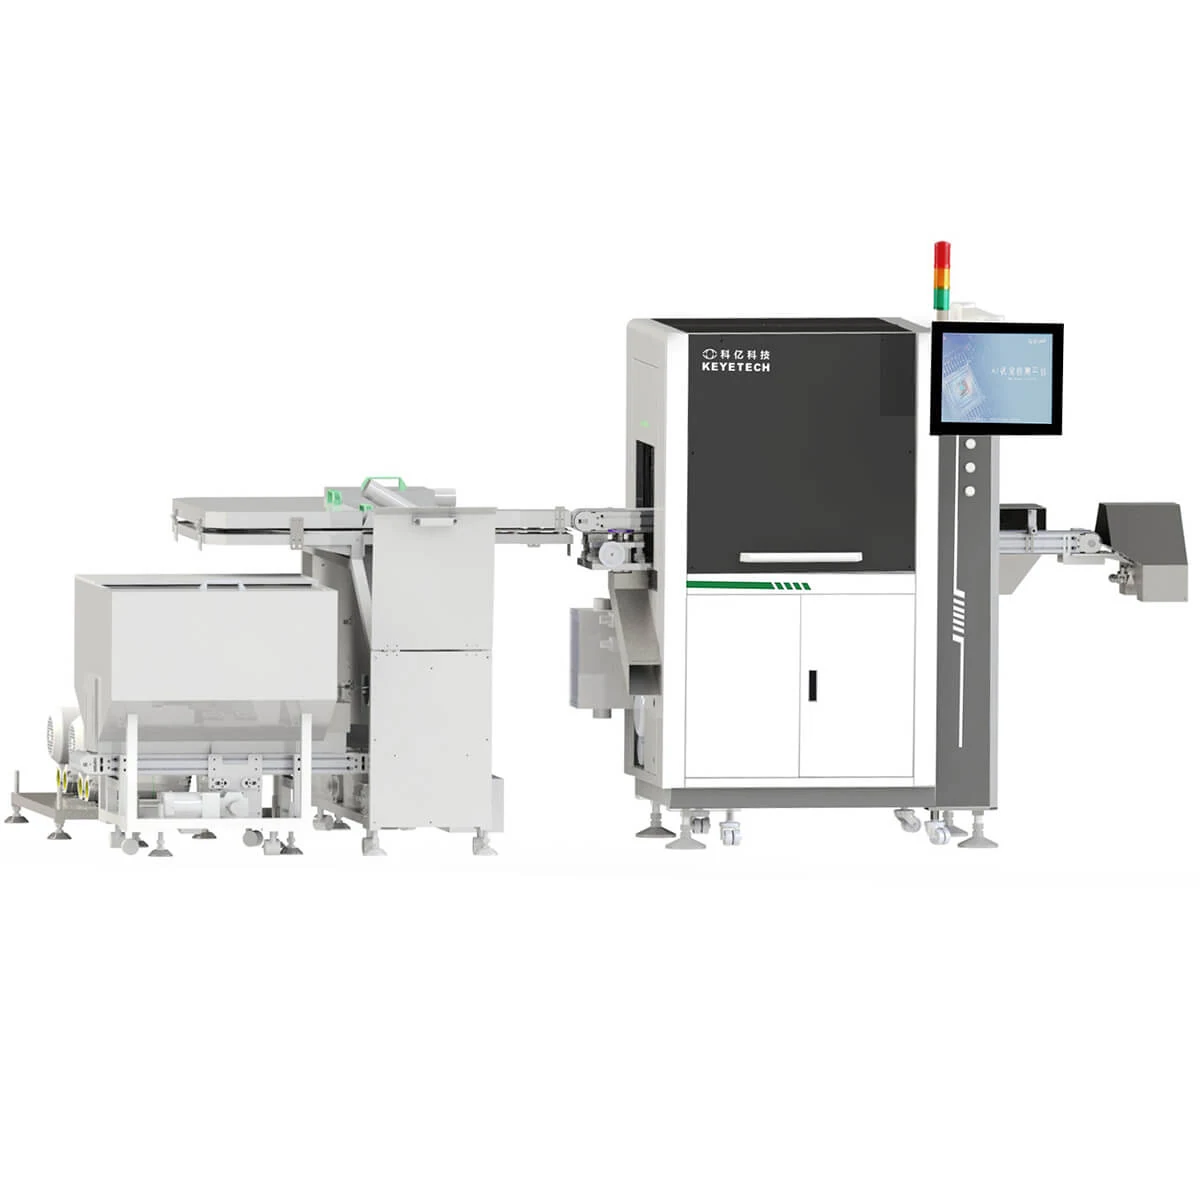
Inspection Speed: 300~2500pcs/min
View specification →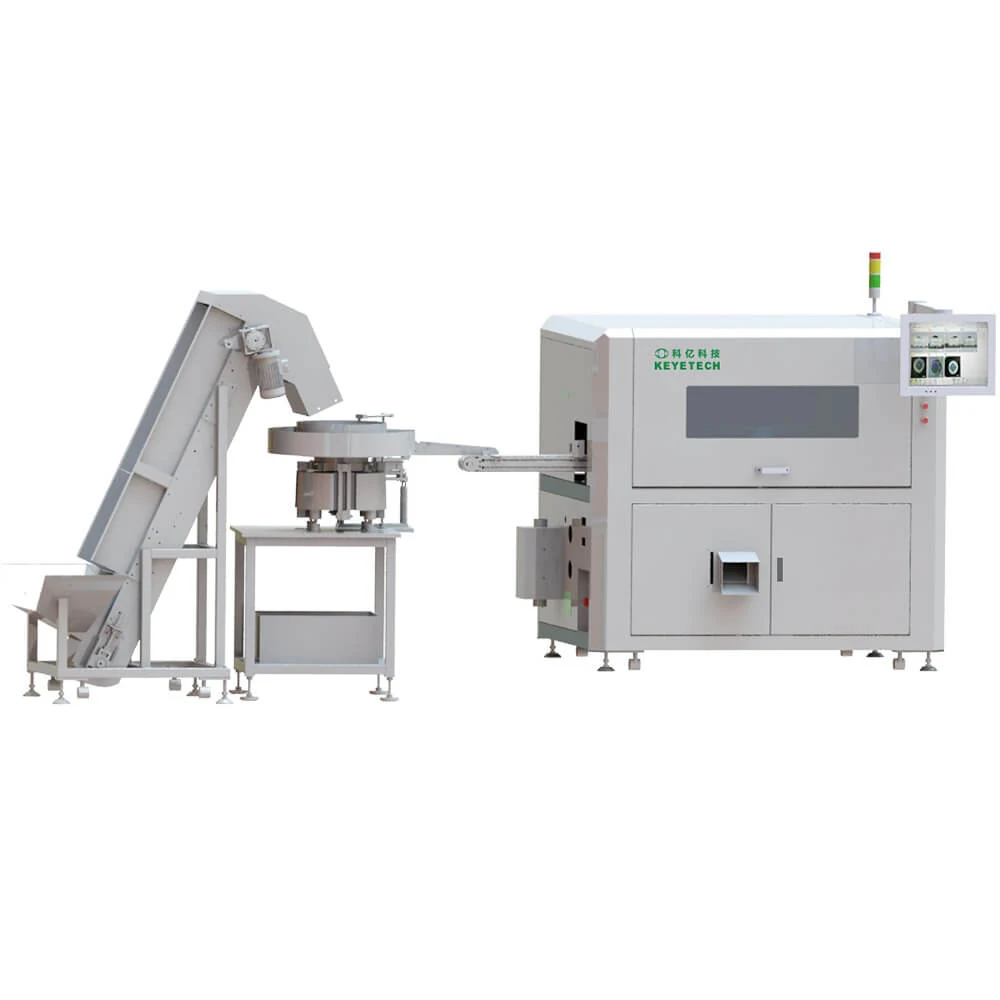
Inspection Speed: 300~2500pcs/min
View specification →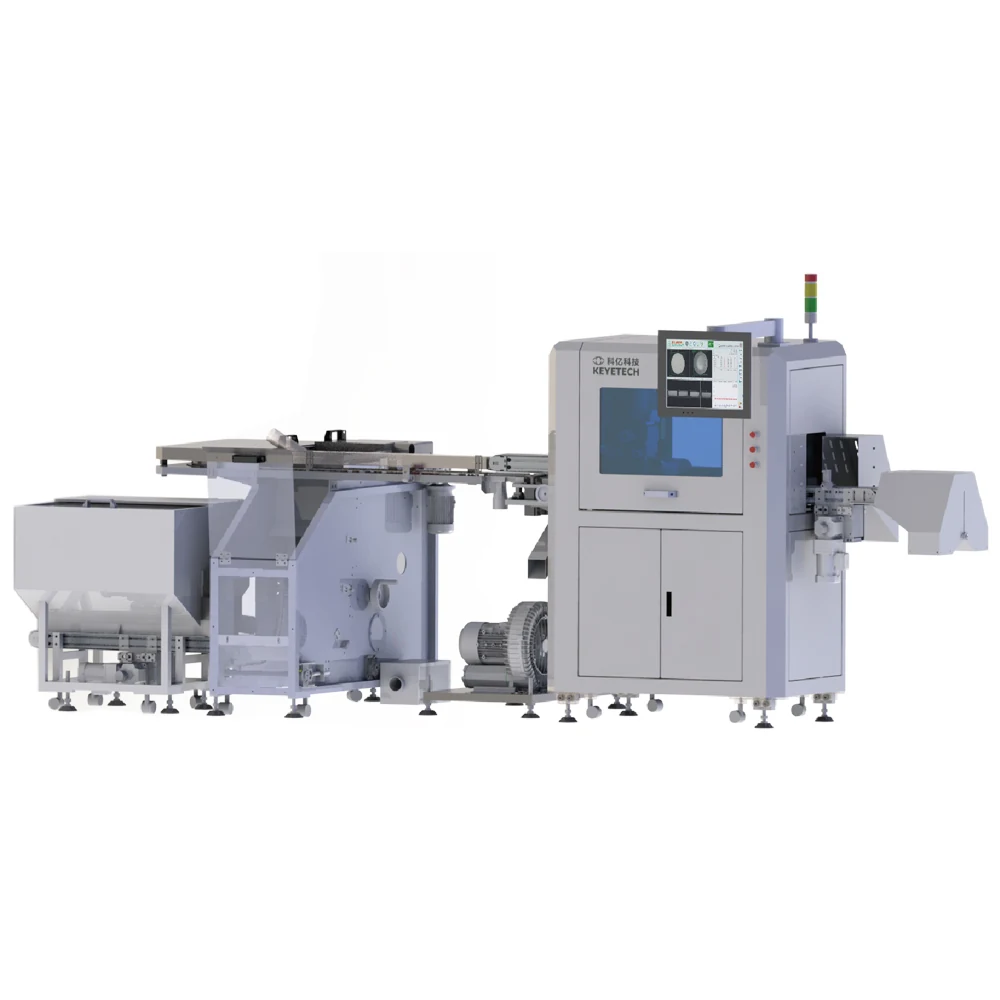
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →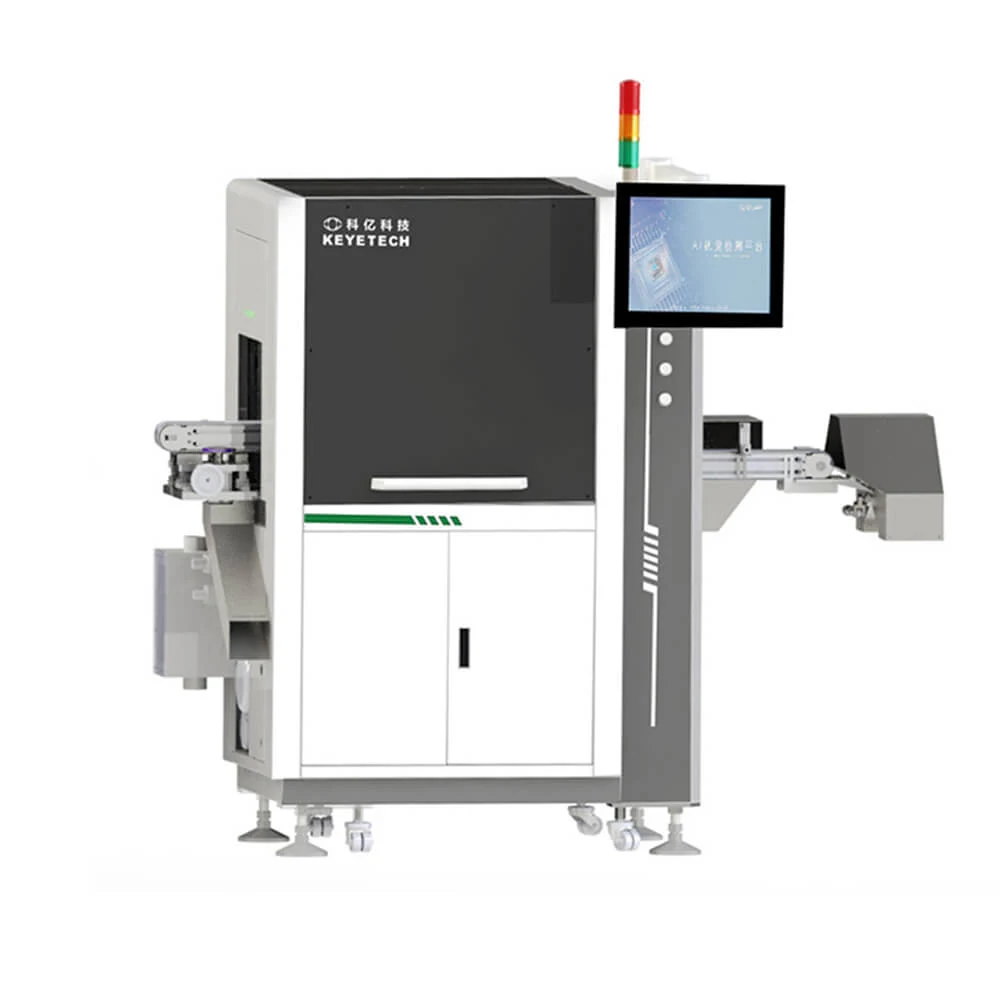
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →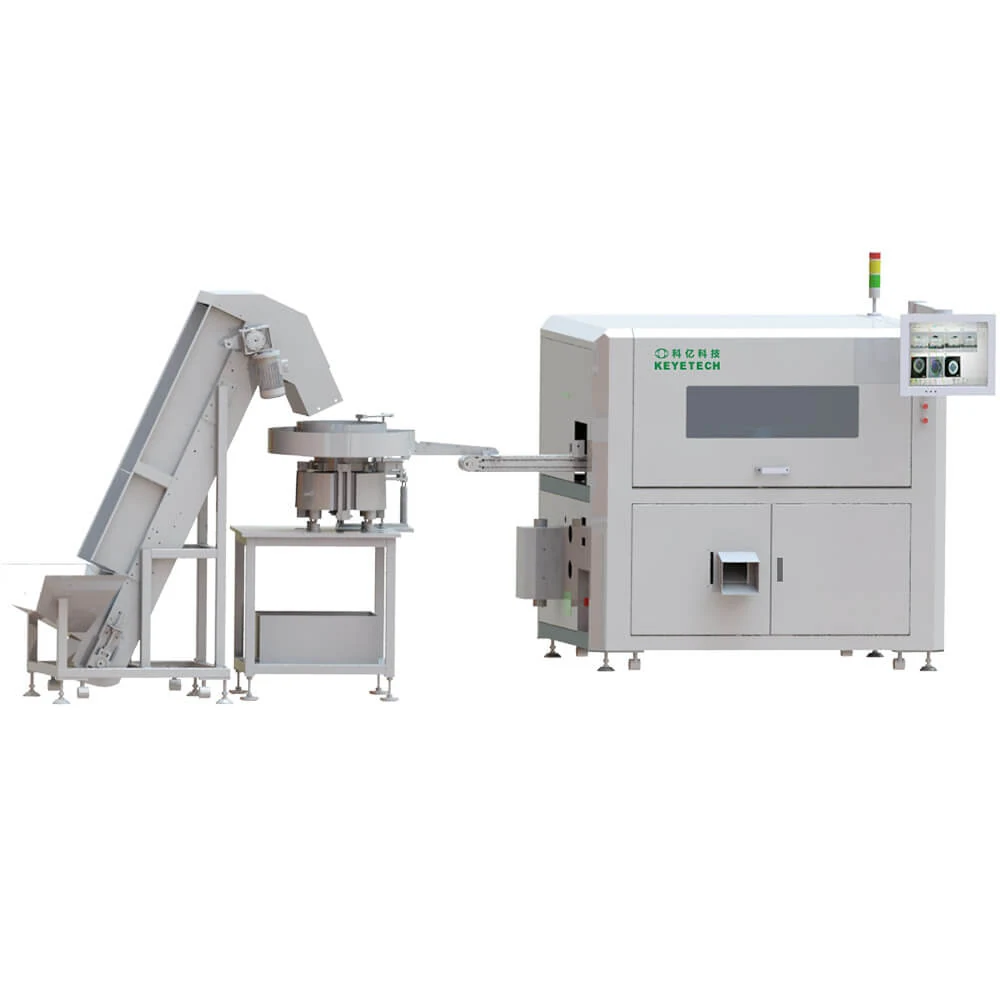
Inspection Speed: 300~2500pcs/min
View specification →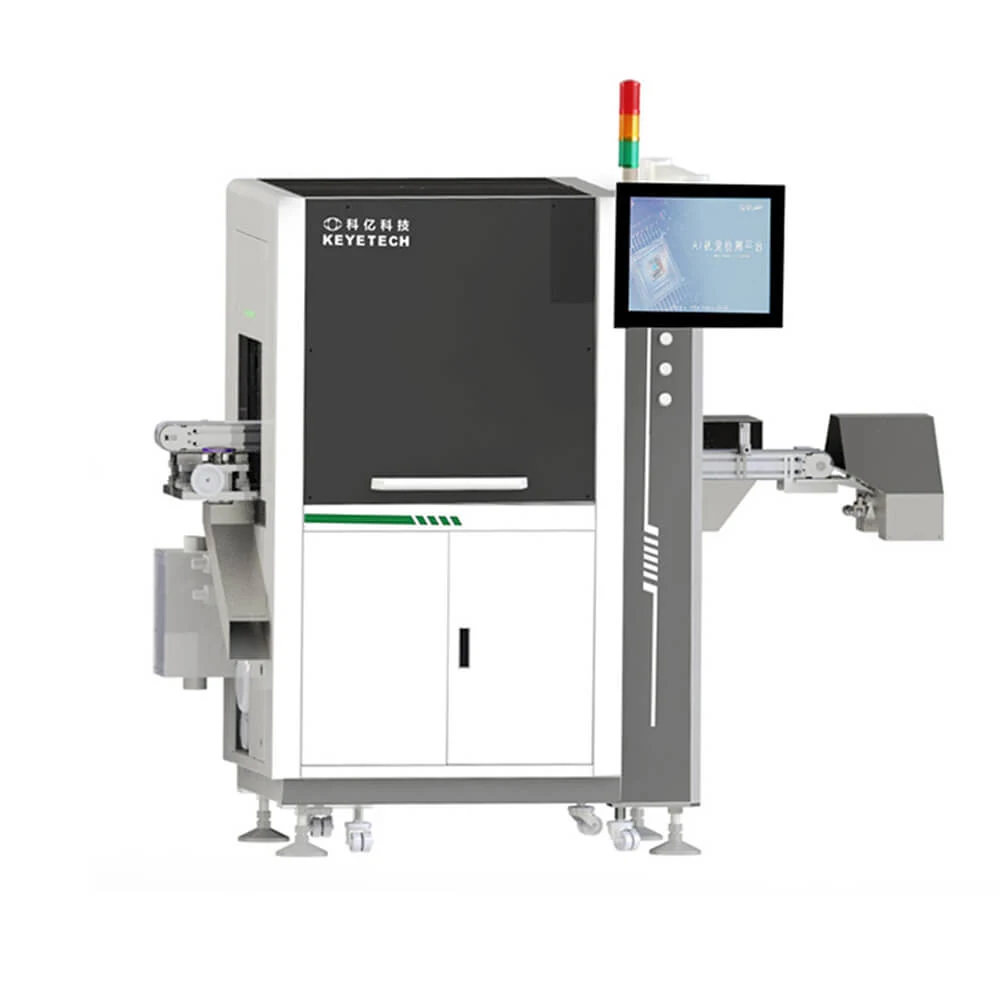
Inspection Speed: 300~2500pcs/min
View specification →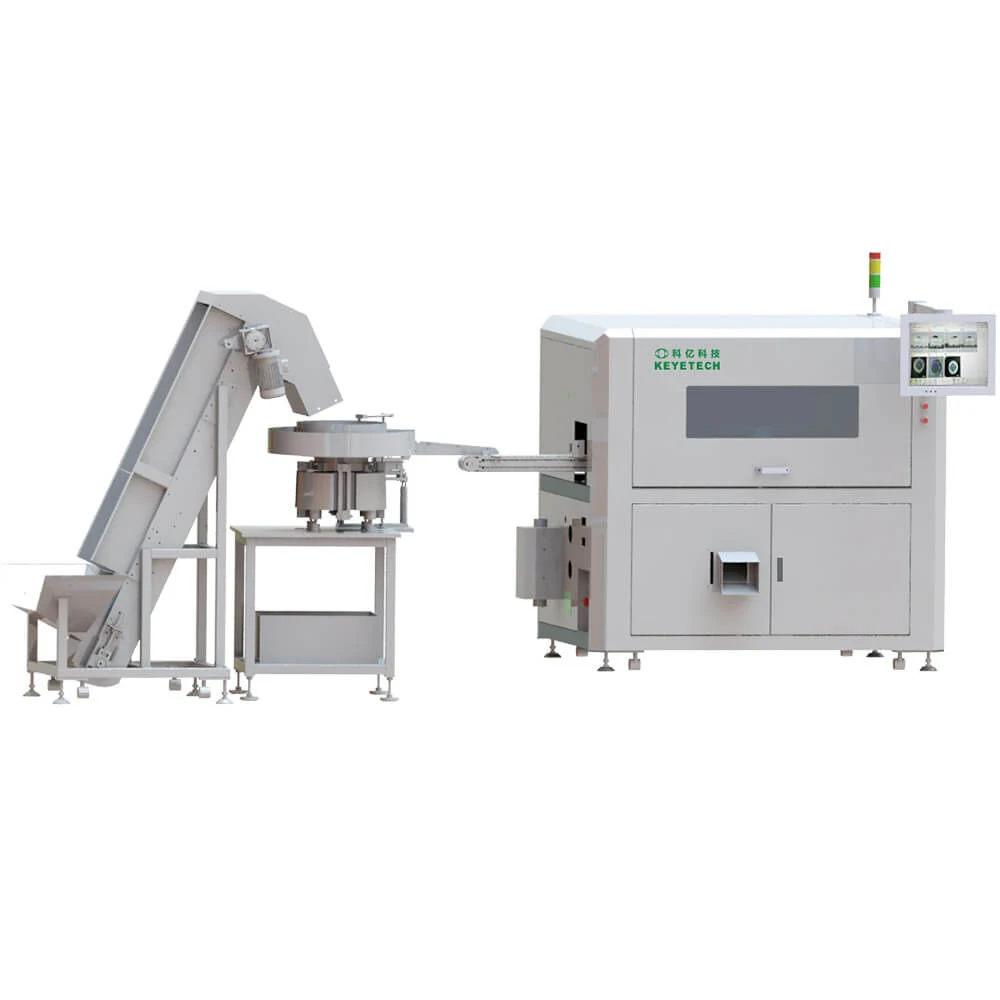
Inspection Speed: 300~2500pcs/min
View specification →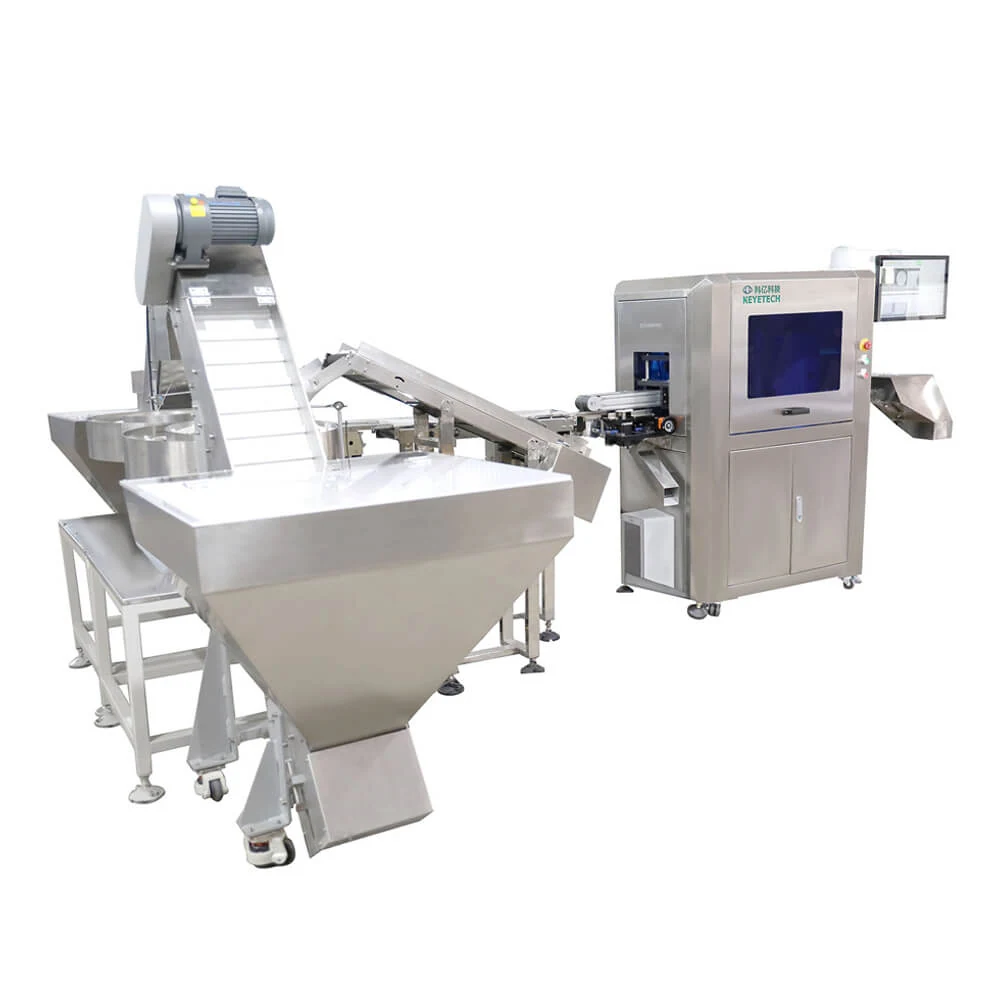
Inspection Speed: 300~2500pcs/min
View specification →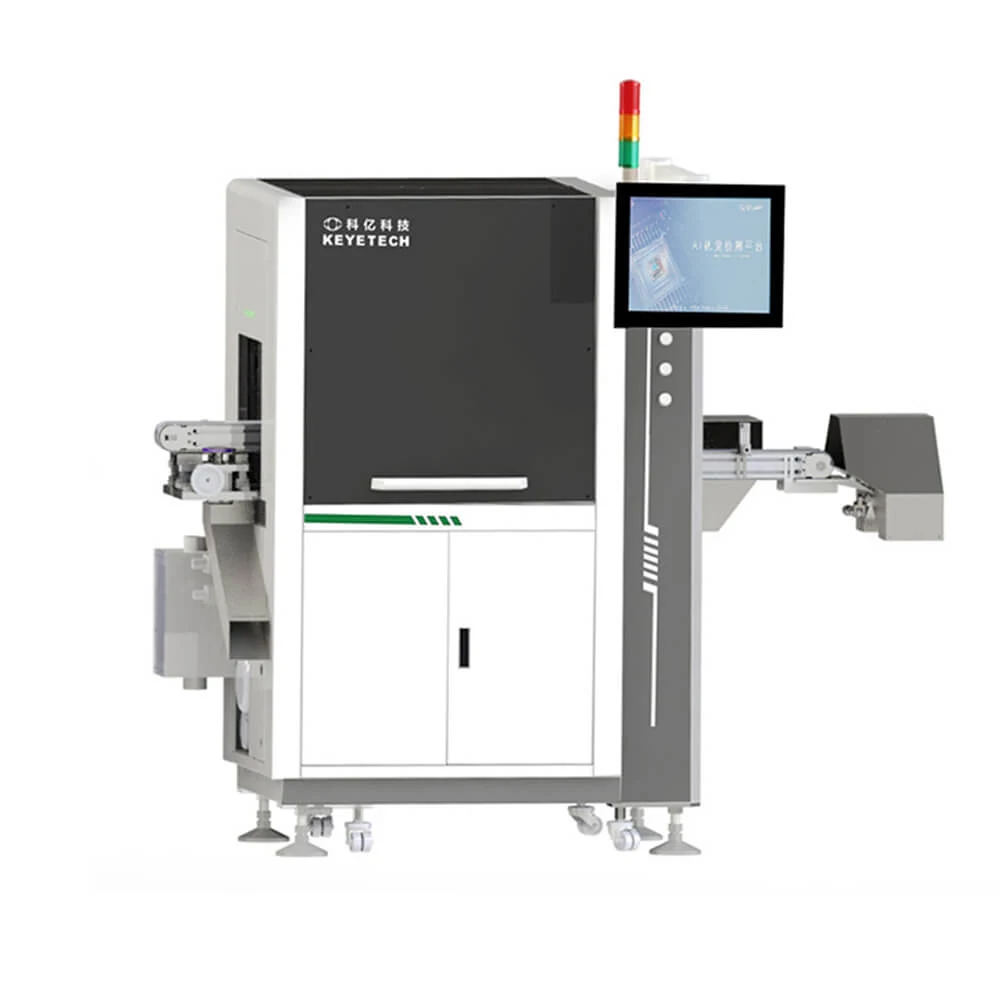
Inspection Speed: 300~2500pcs/min
View specification →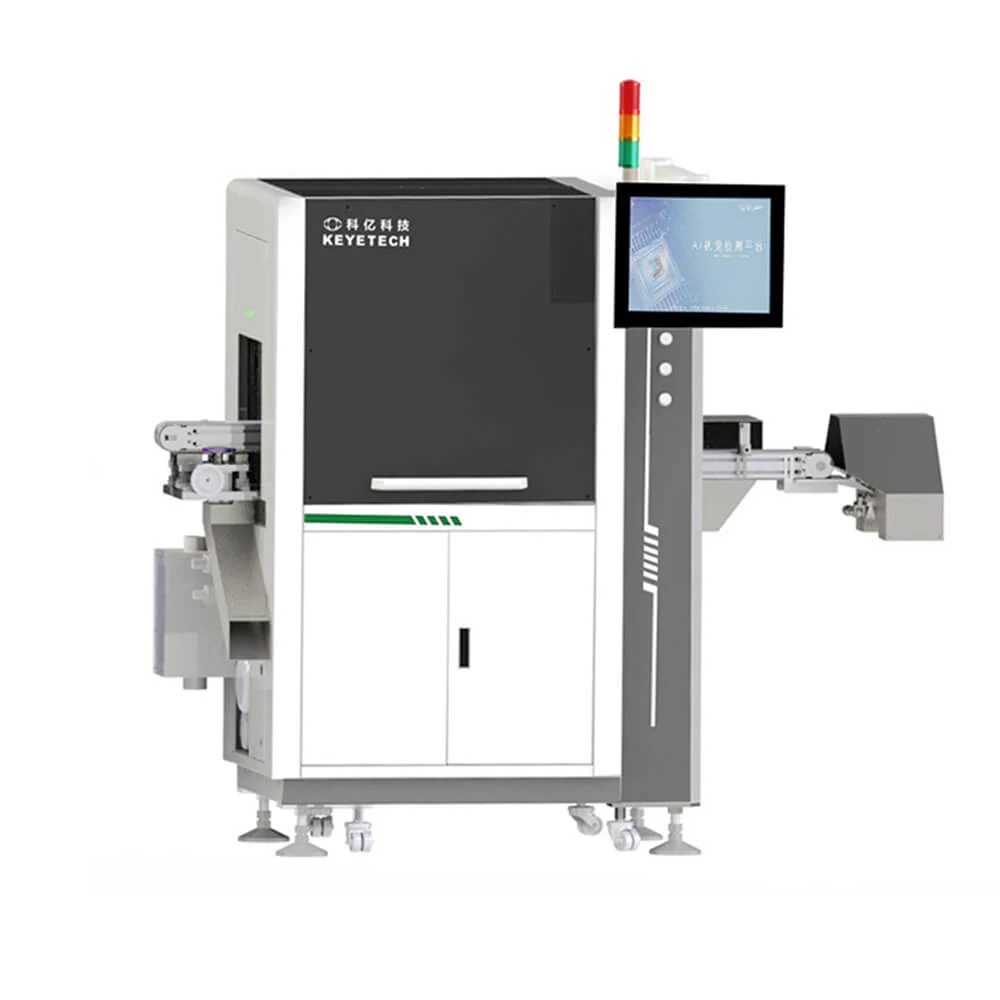
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →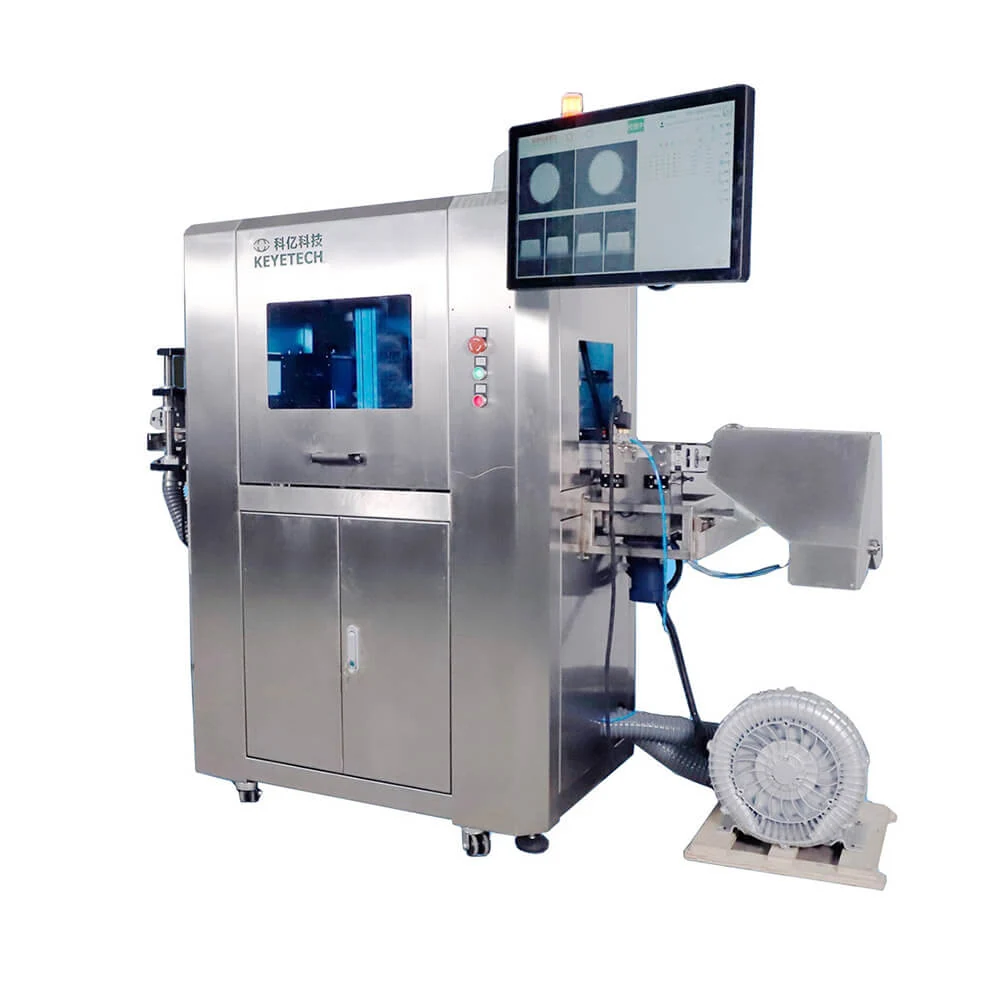
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →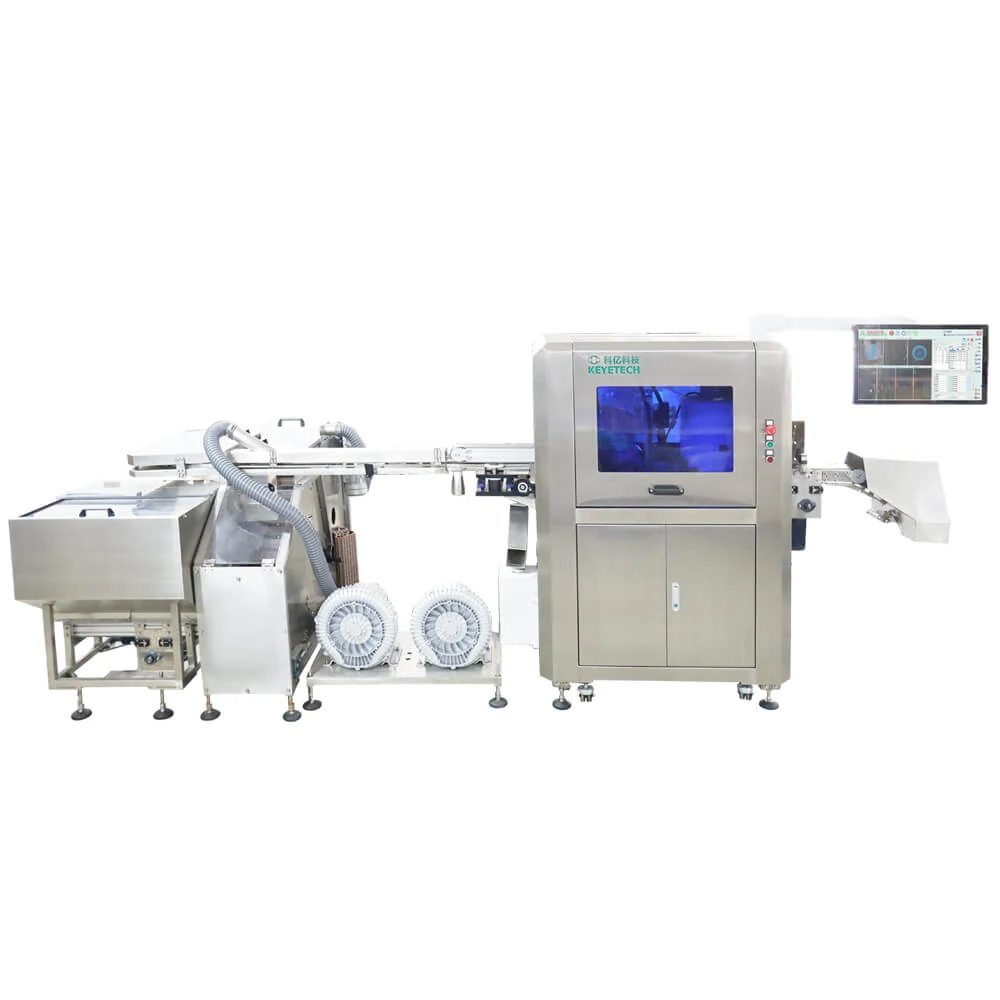
Inspection Speed: 300~2500pcs/min
View specification →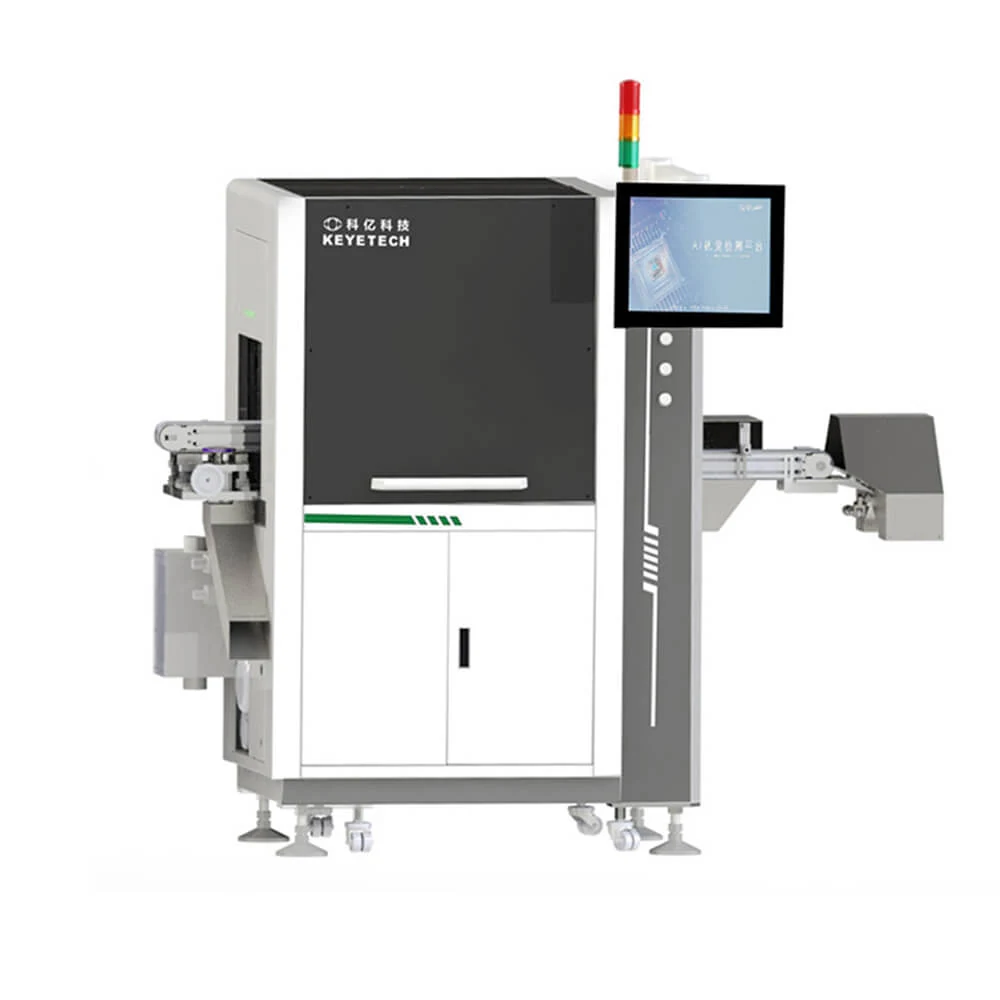
Inspection Speed: 300~2500pcs/min
View specification →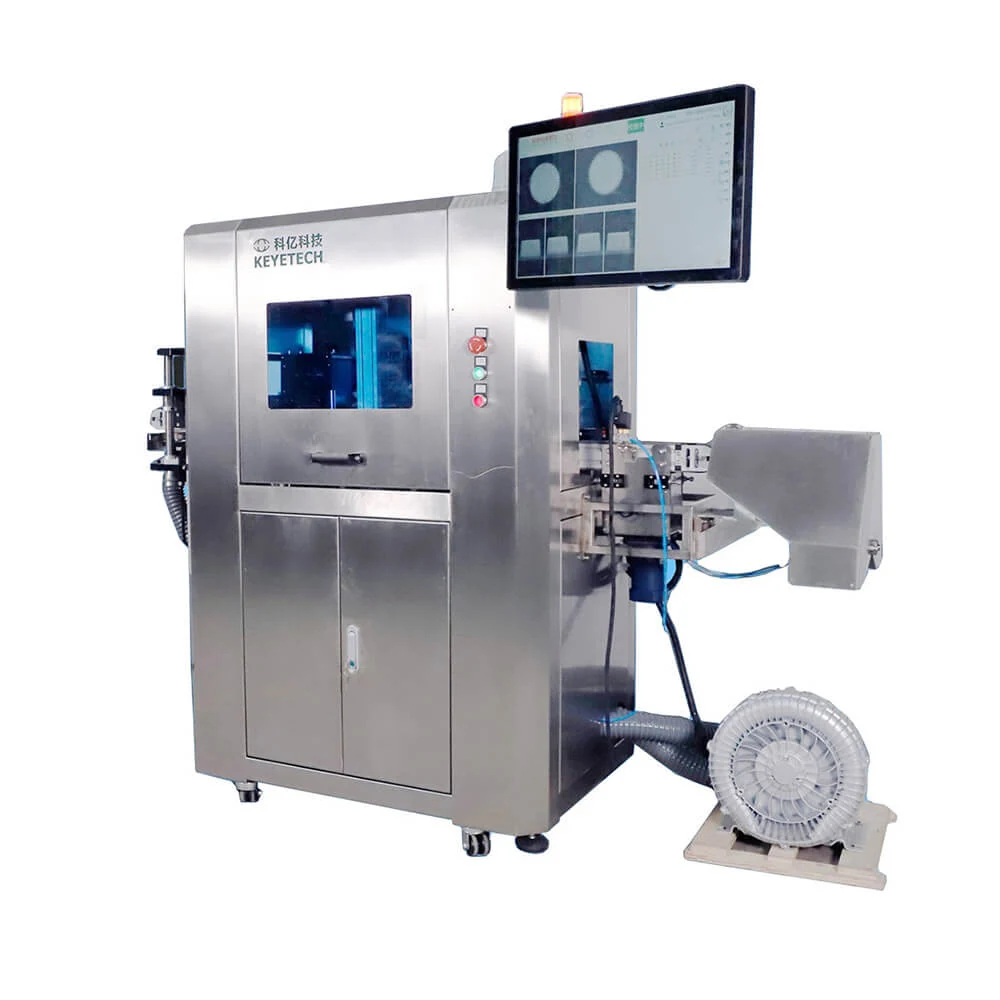
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →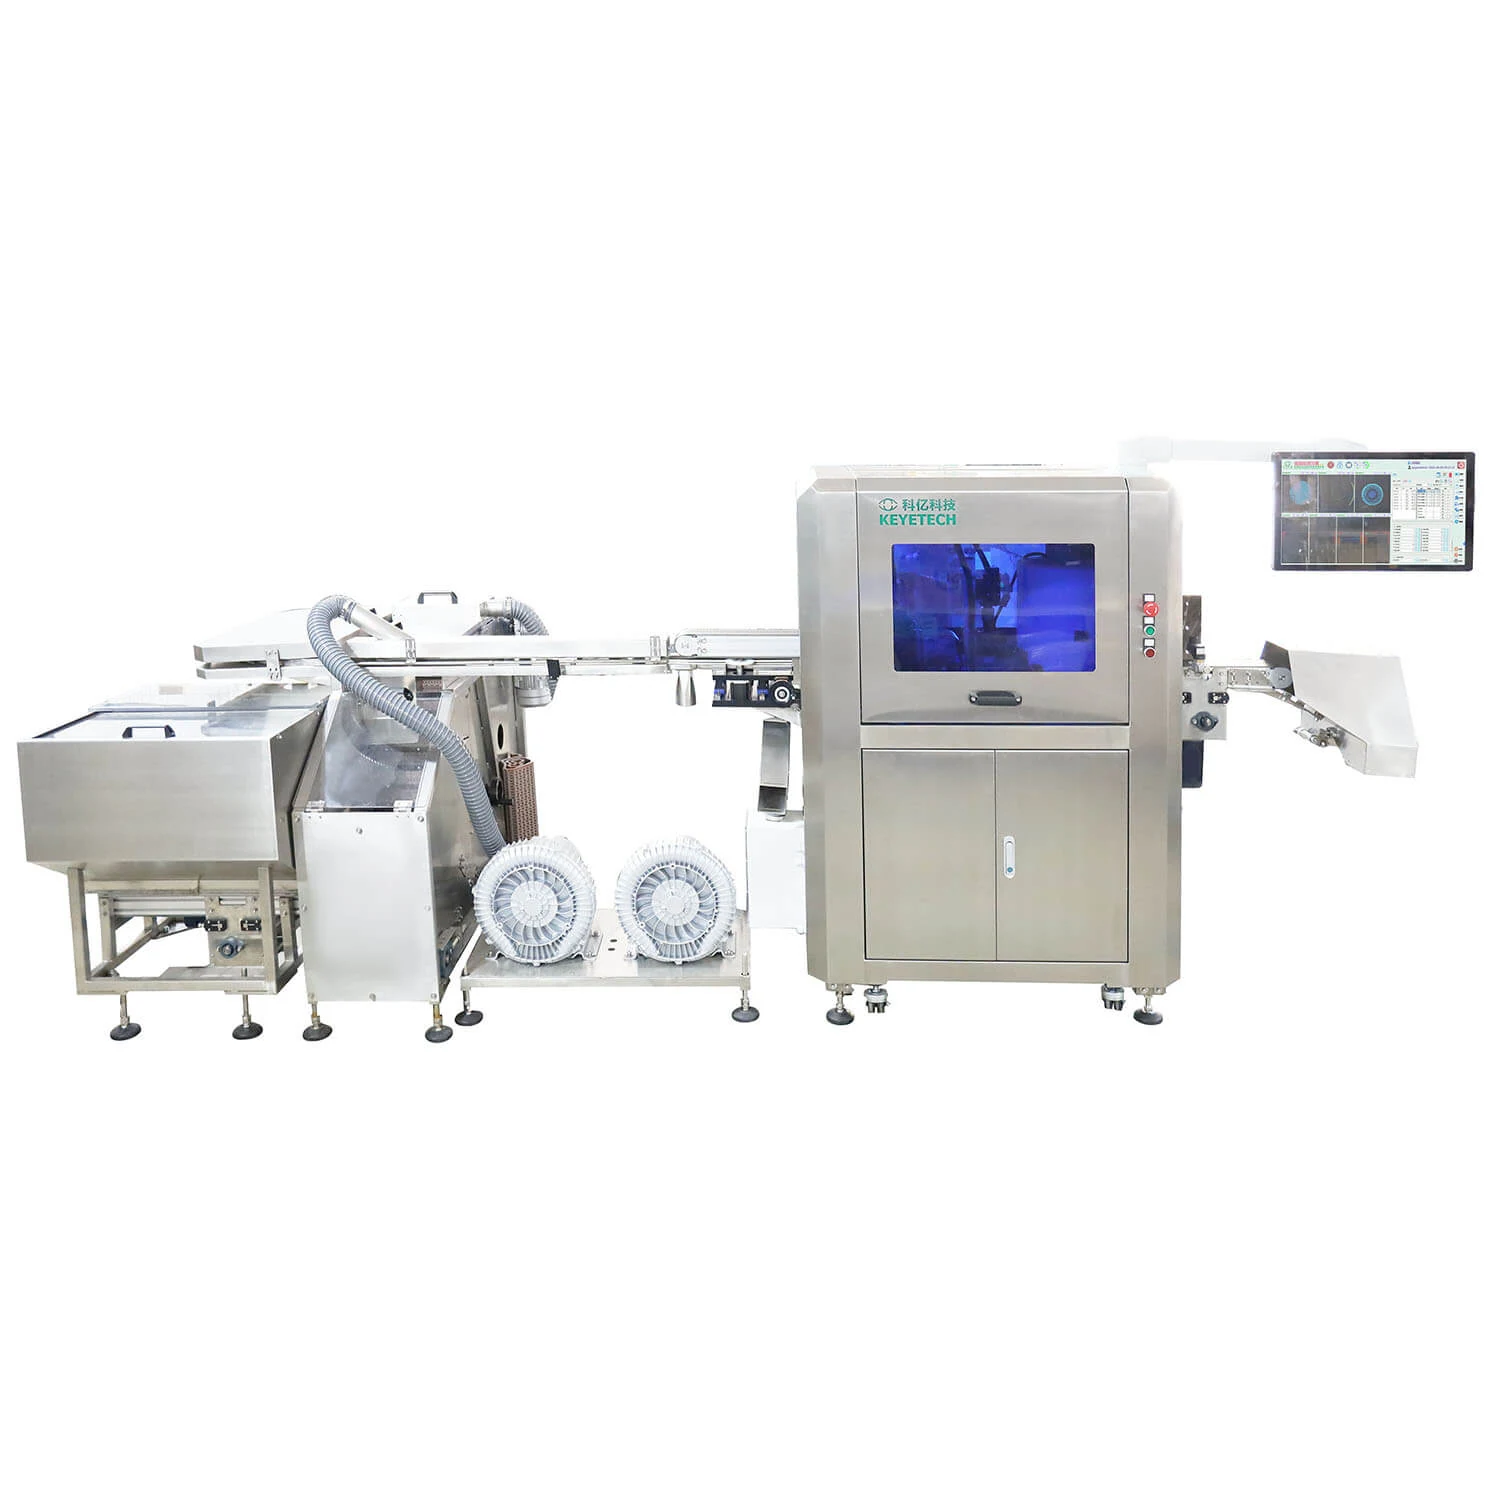
Inspection Speed: 300~2500pcs/min
View specification →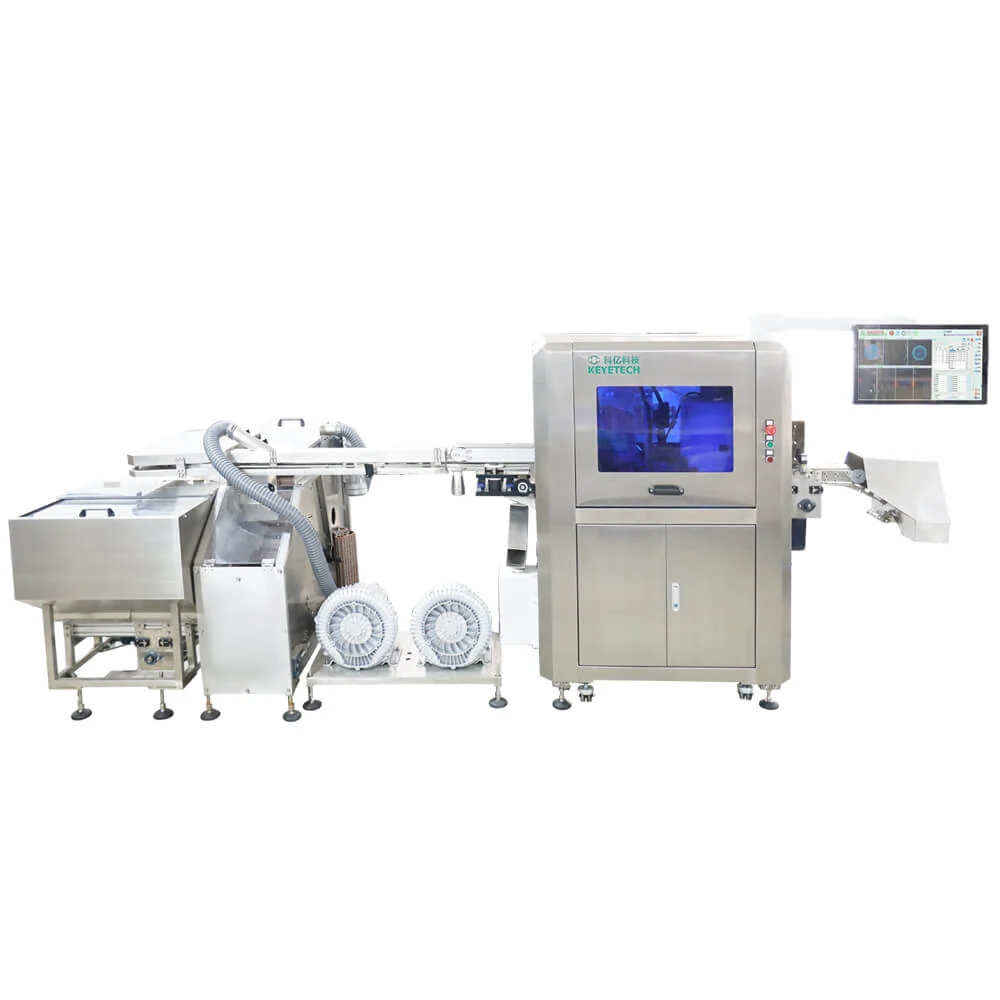
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →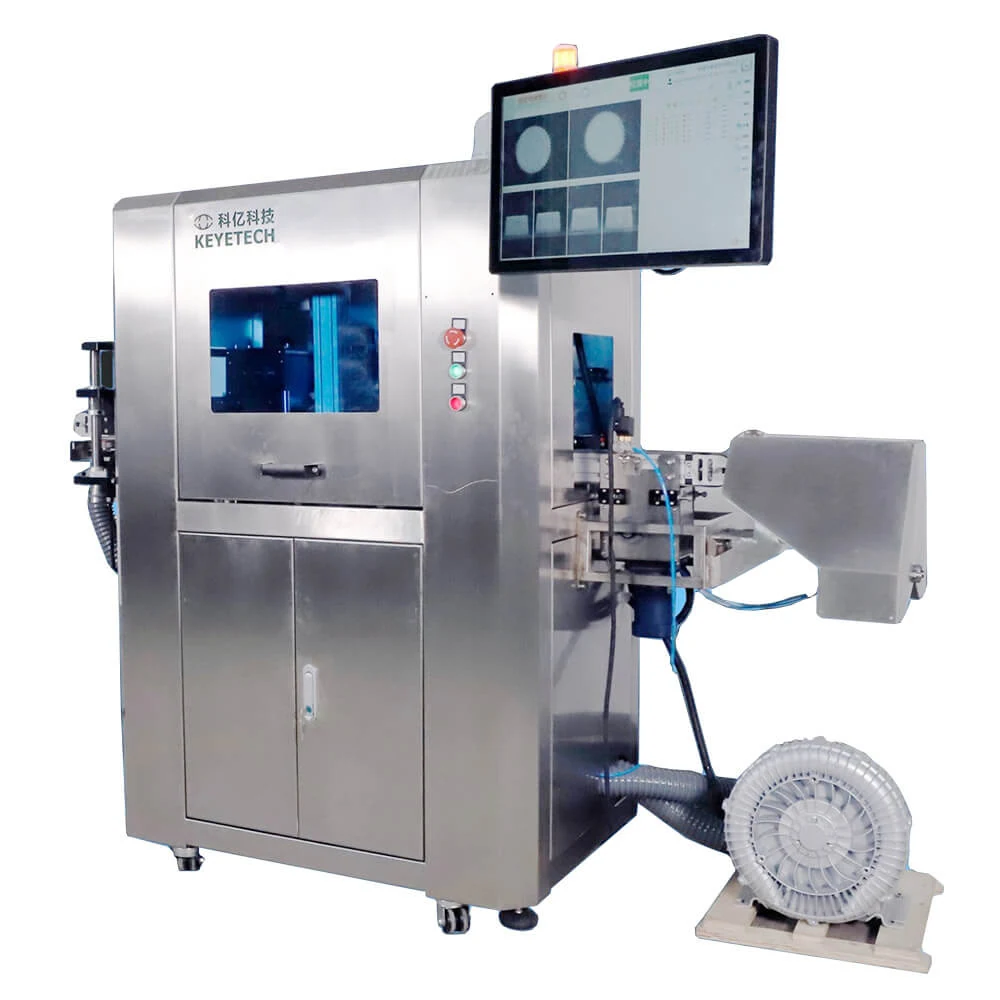
Inspection Speed: 300~2500pcs/min
View specification →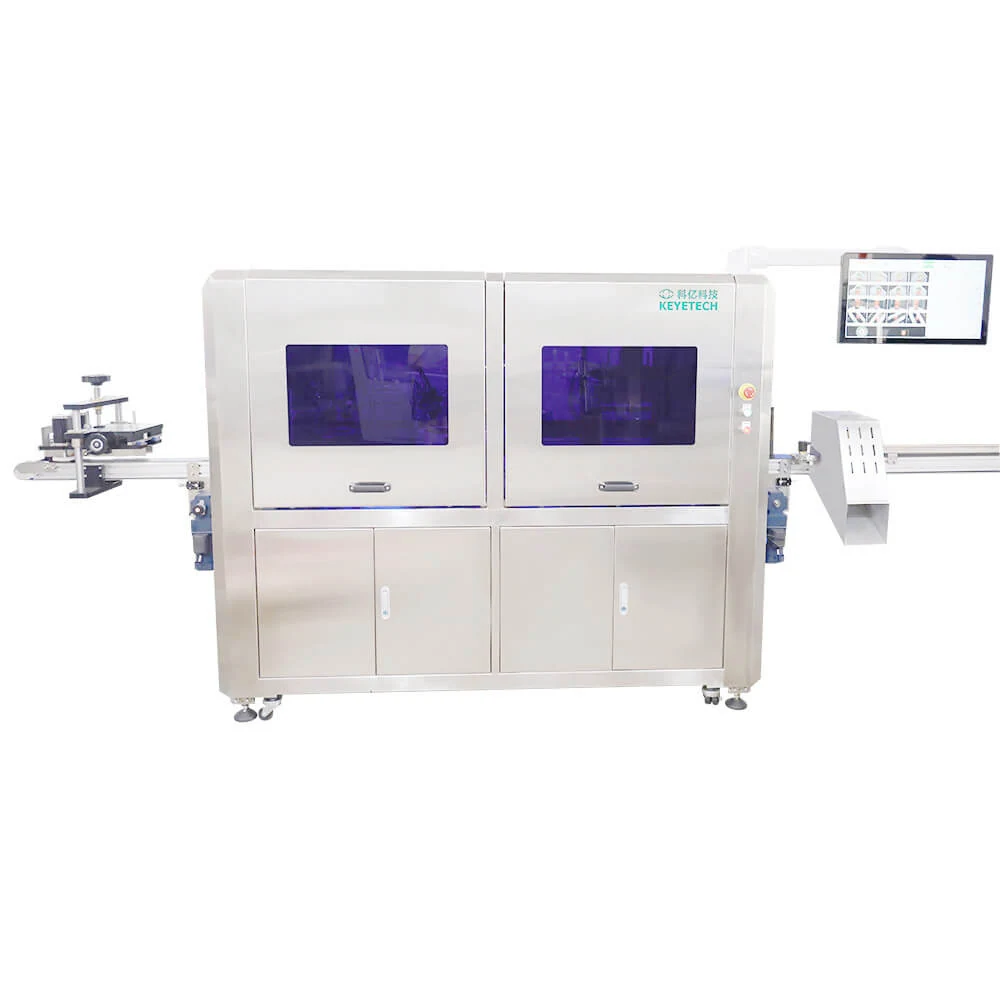
Inspection Speed: 300~2500pcs/min
View specification →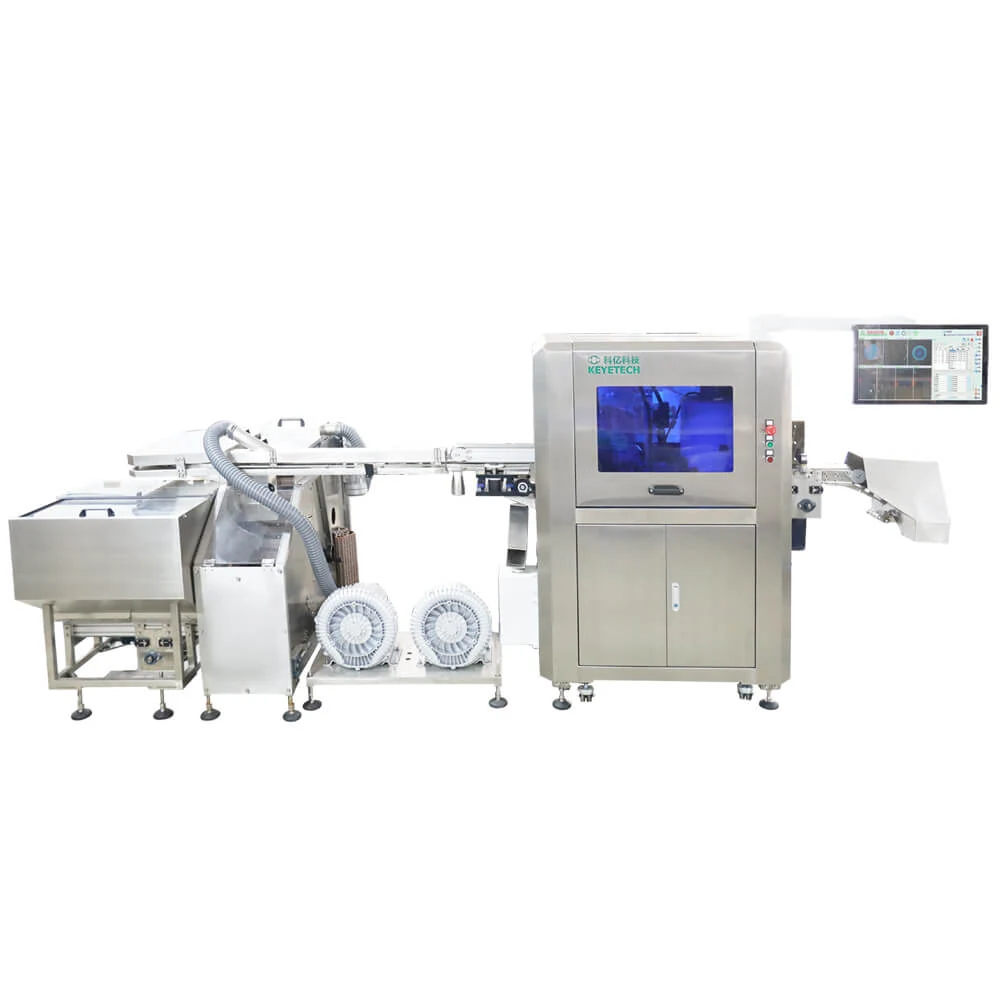
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →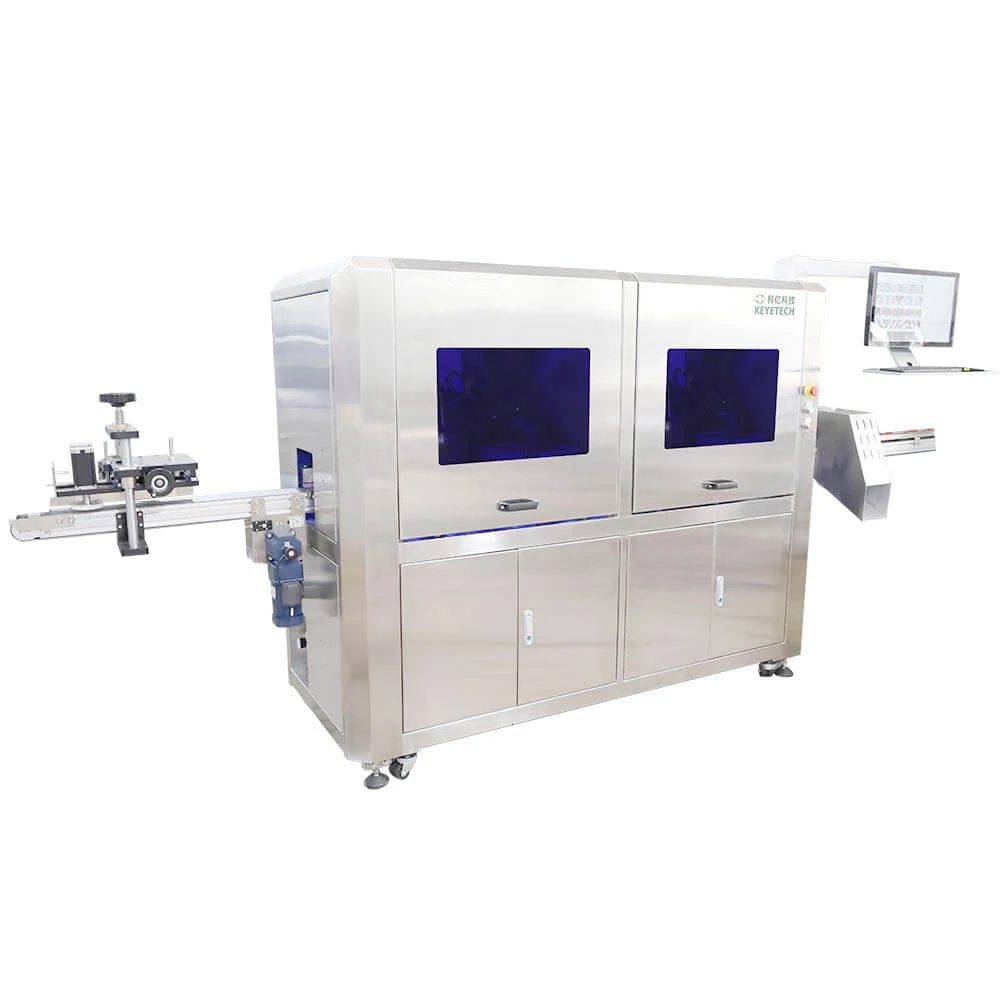
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →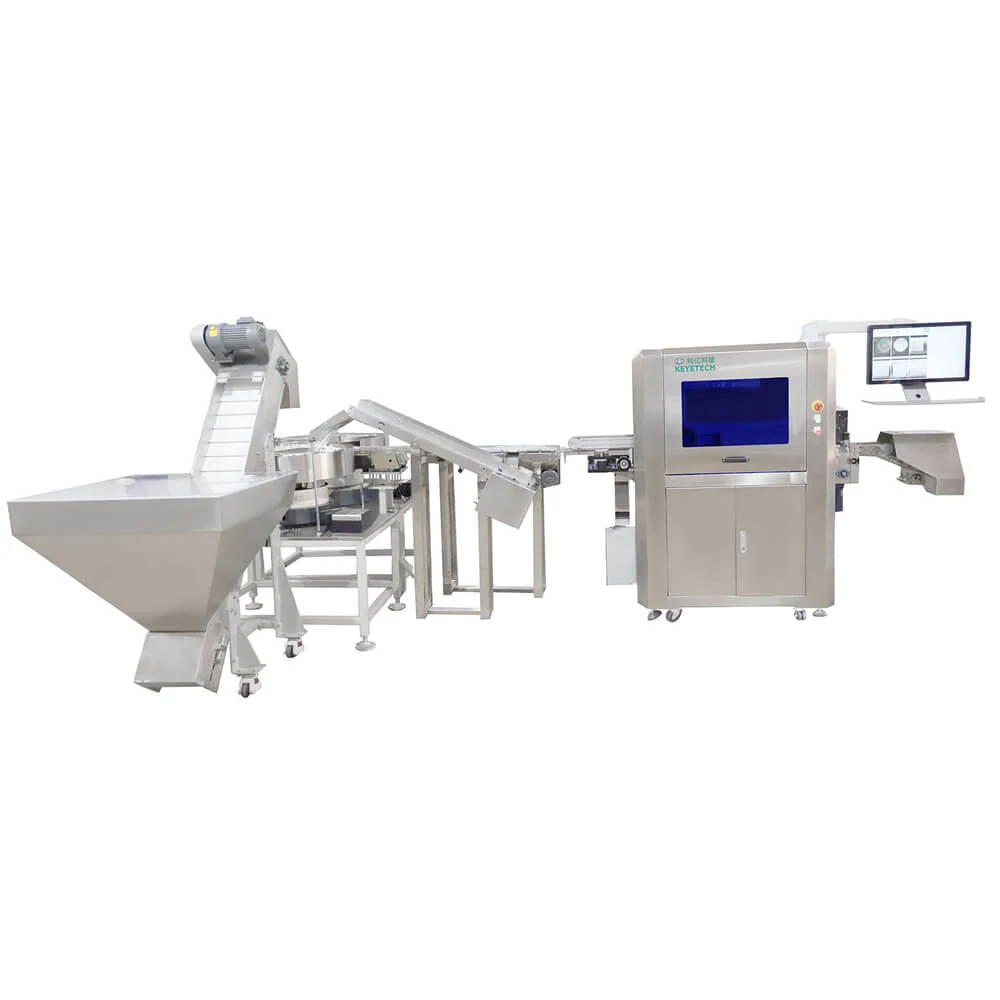
Inspection Speed: 300~2500pcs/min
View specification →
Inspection Speed: 300~2500pcs/min
View specification →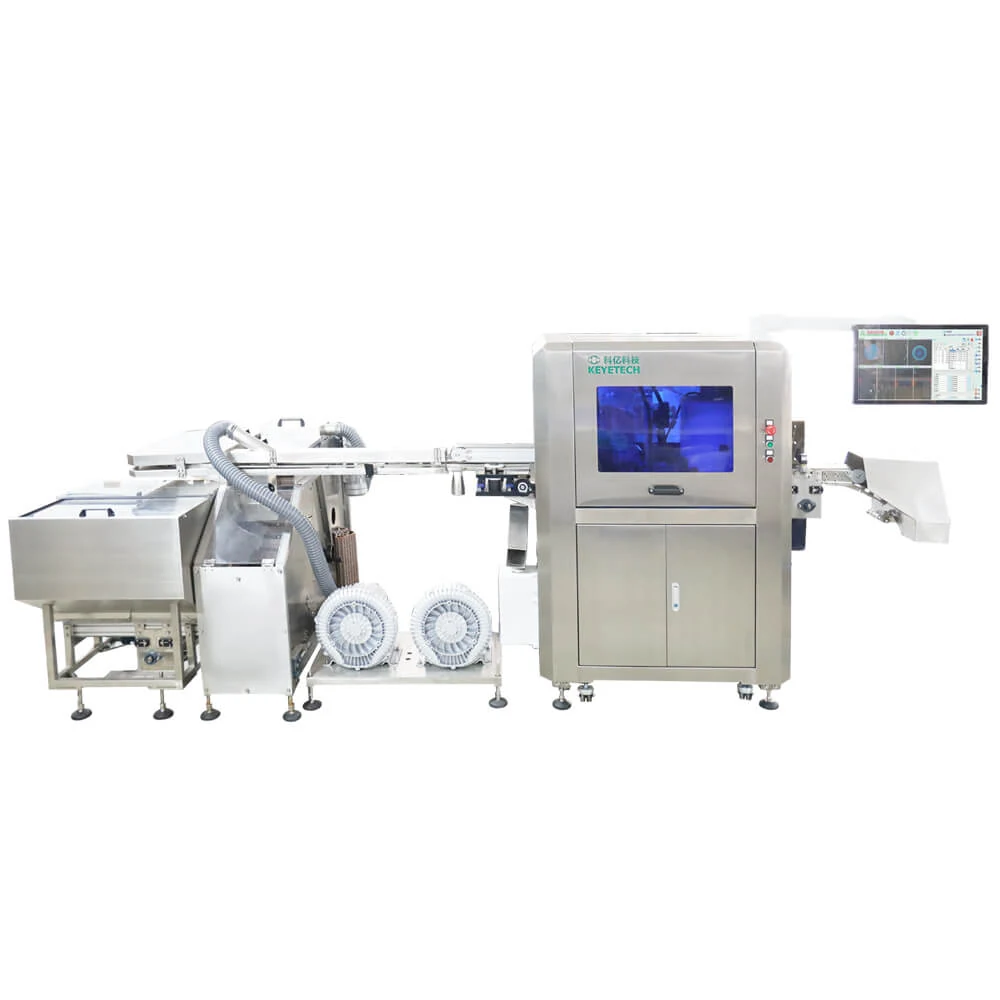
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →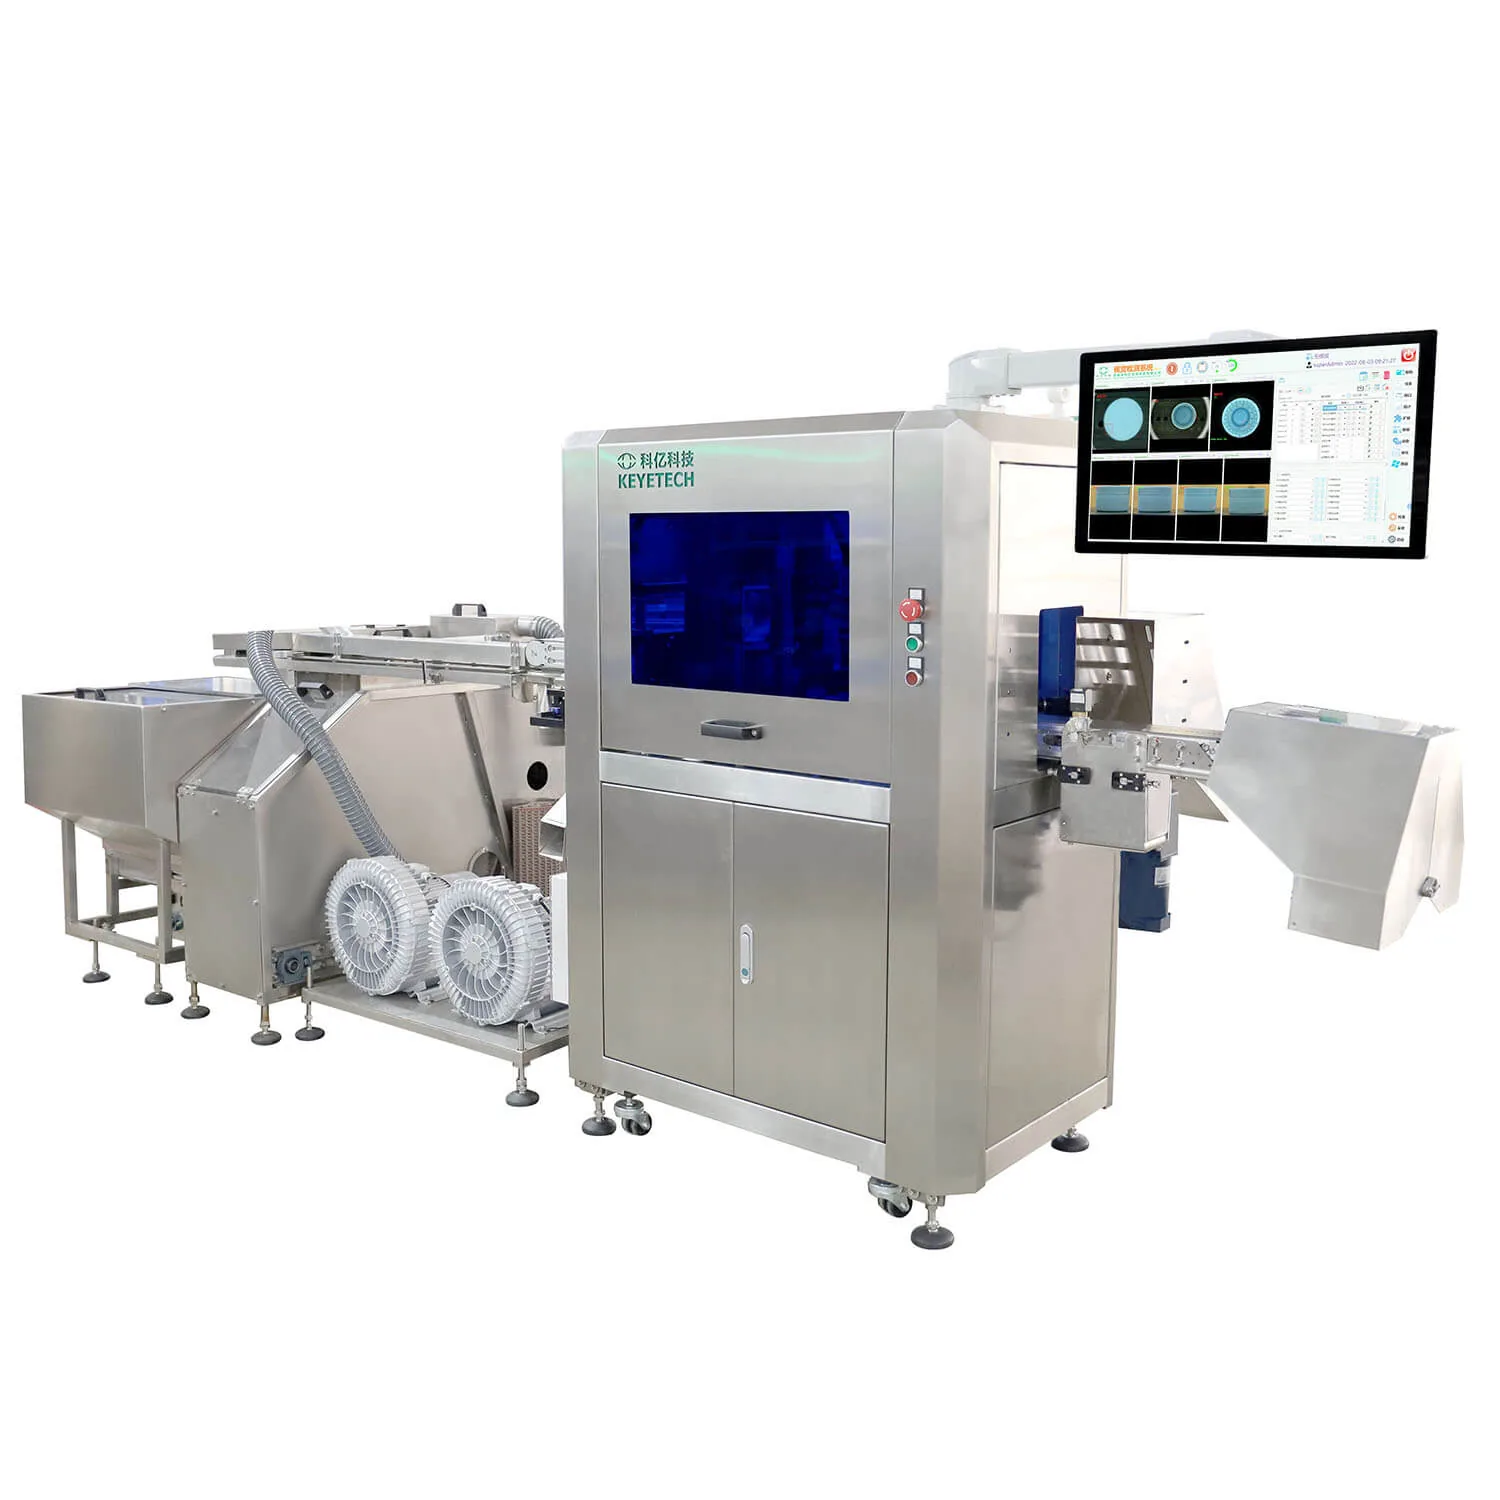
Inspection Speed: 300~2500pcs/min
View specification →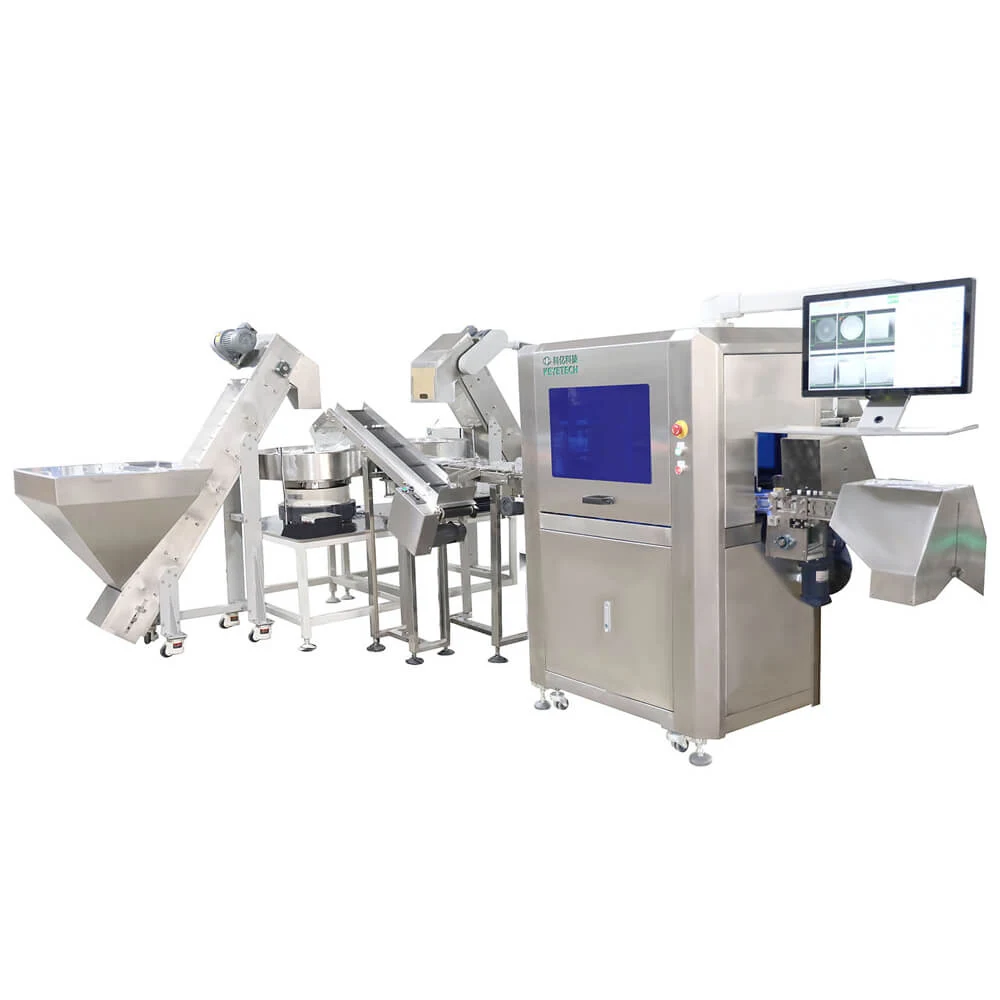
Inspection Speed: 300~2500pcs/min
View specification →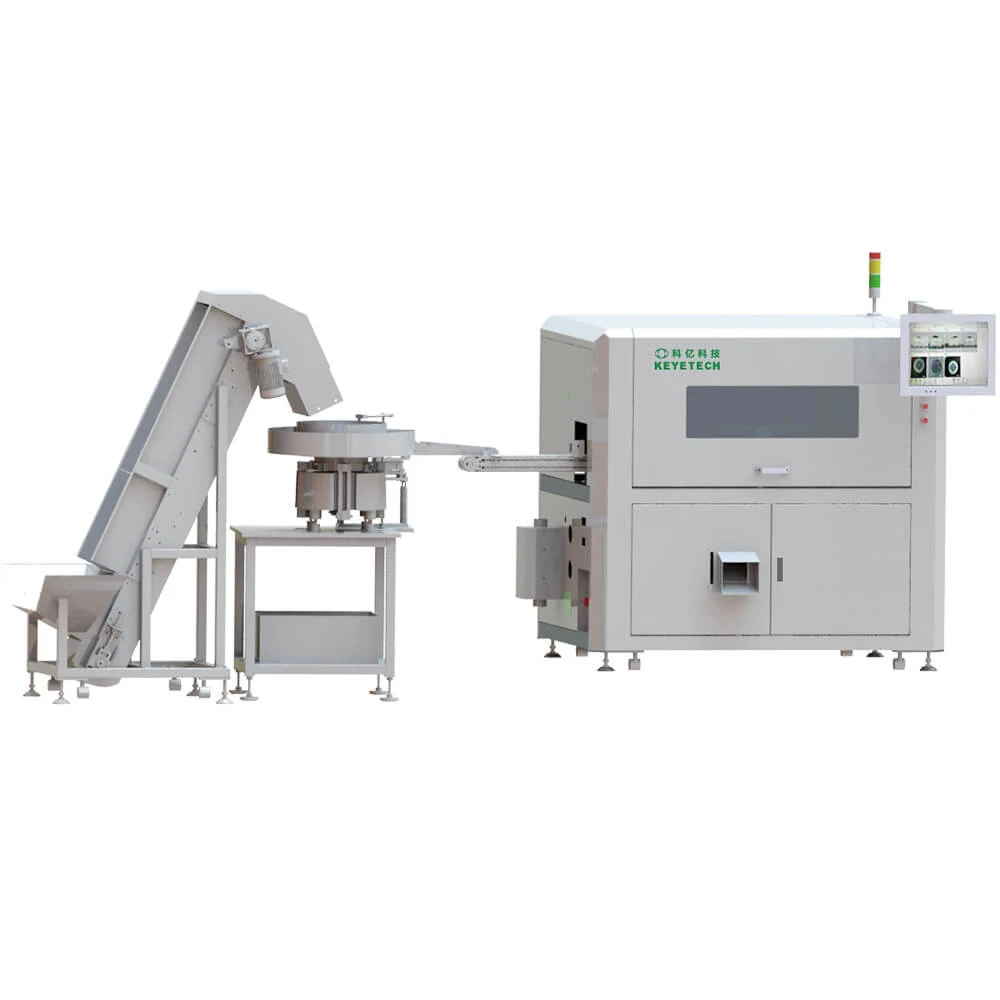
Inspection Speed: 300~2500pcs/min
View specification →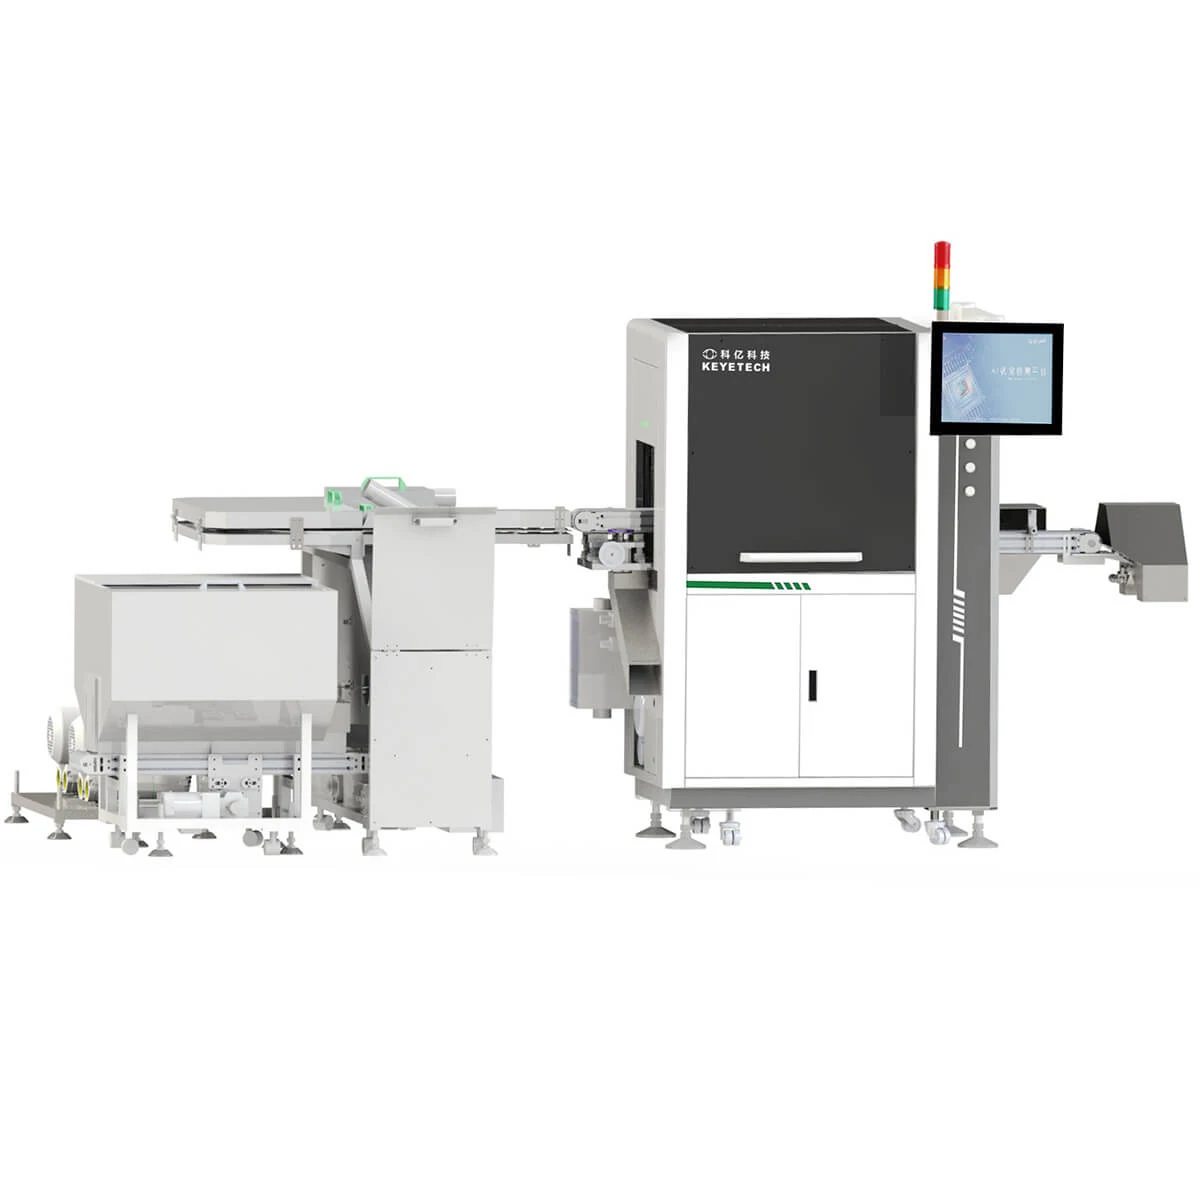
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →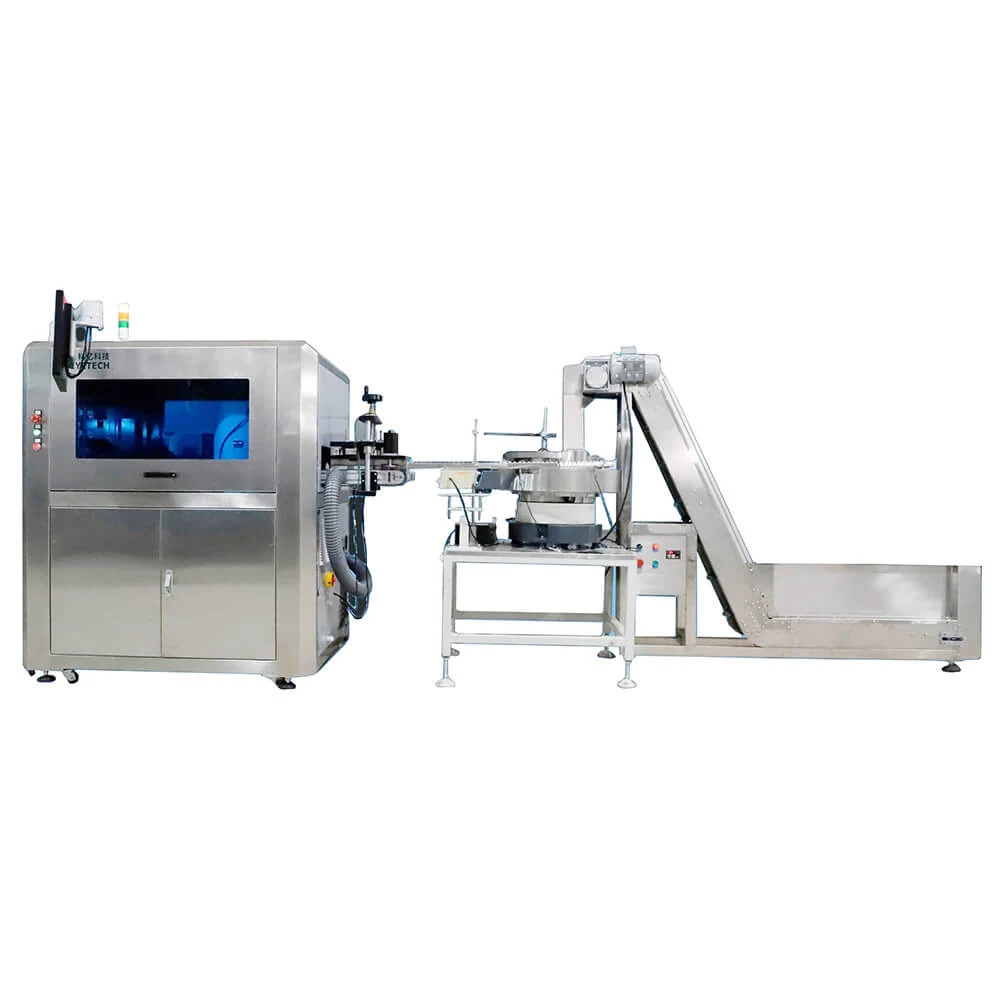
Inspection Speed: 300~2500pcs/min
View specification →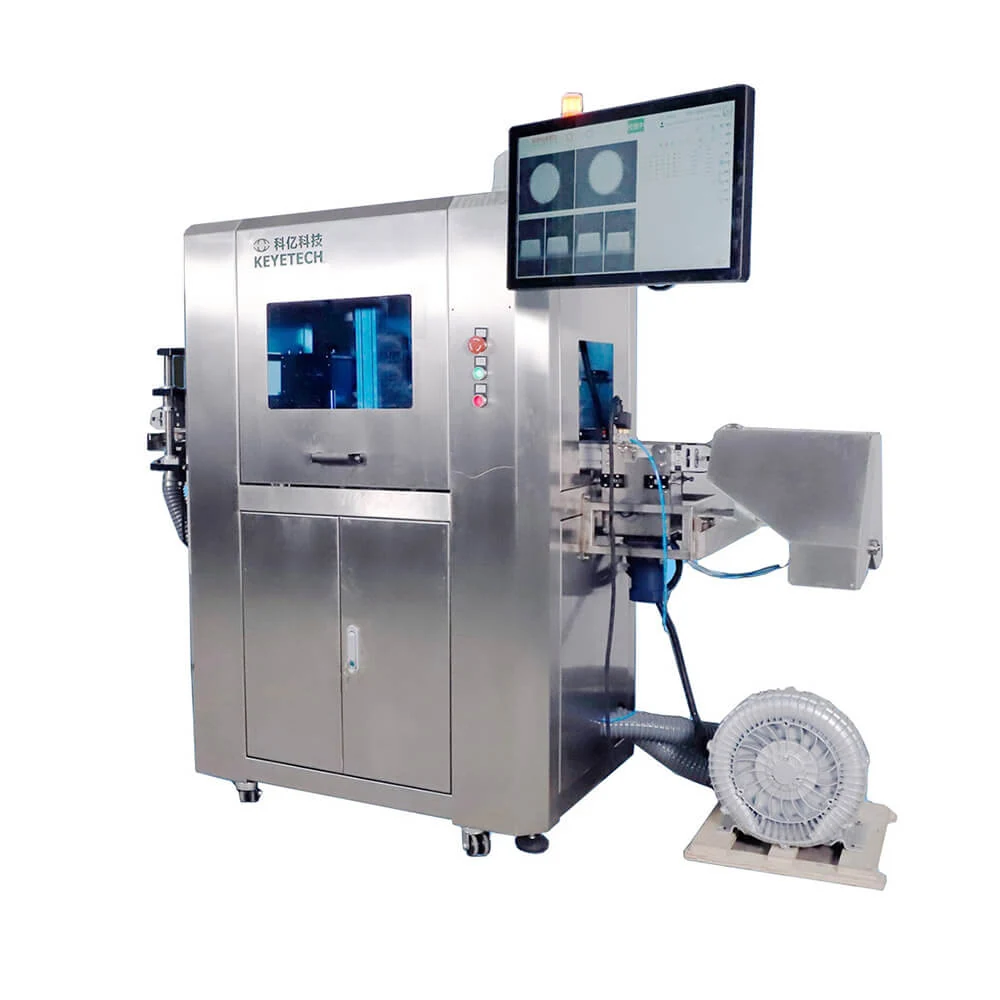
Inspection Speed: 300~2500pcs/min
View specification →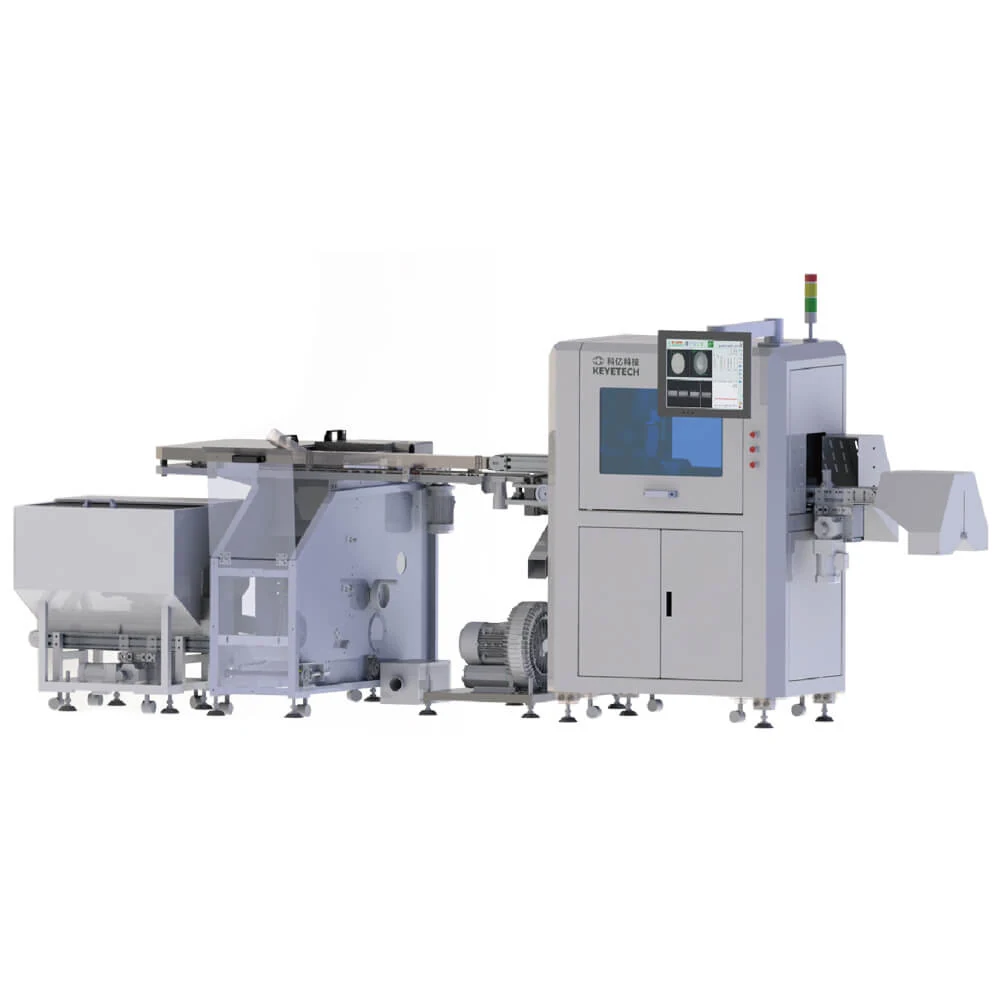
Inspection Speed: 300~2500pcs/min
View specification →Inspection Speed: 300~2500pcs/min
View specification →All plastic closures for water and beverage, daily products, daily chemicals and pharmaceutical packaging. Metal-look and printed closures are handled by changing the lighting design, not the machine.
Camera count follows the inspection area, the defect types and the tolerance. A cap top and sidewall check is usually six cameras; adding inner thread, gasket and mould number pushes it to twelve or more.
Resolution is selected from your precision requirement. A 0.2 mm x 0.2 mm defect and a 0.5 mm x 0.5 mm defect do not need the same sensor, so we size it against your smallest real defect.
Yes. Inline installation connects to your existing cap moulding machine. Offline installation uses our material feeder so the machine runs independently of the moulder.
Standard configurations are built from semi-finished stock in two to three weeks. Heavily customised systems can take eight weeks or more; the exact date comes with the quotation.
Total cap types and quantity, cap colour and size with samples or drawings, the list of defects to detect with samples, target or 360-degree inspection, required speed and precision, and inline or offline.
Send the part, the defect list, the speed and the precision. We image your real samples before we quote.