IML Visual Inspection
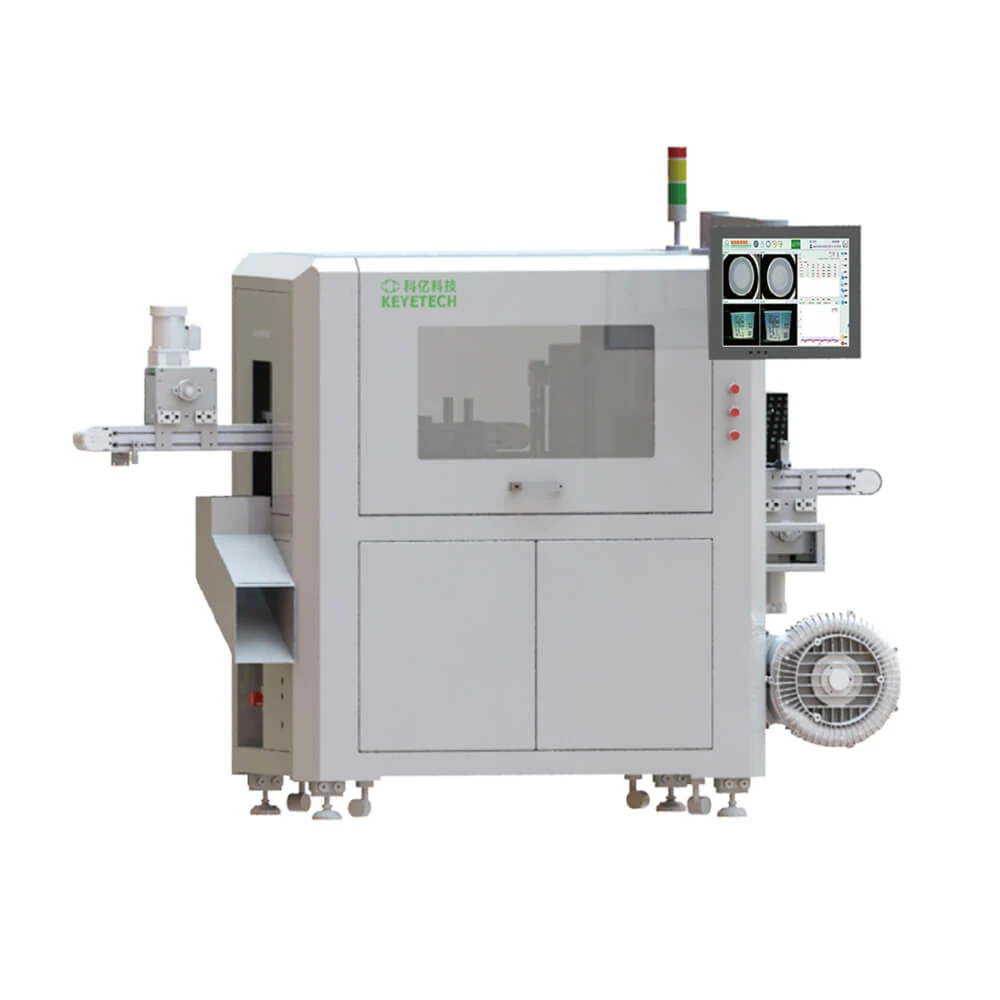
AI-driven 10 Cameras All-round IML Inspection Machine in Any Rotational Position
Inspection Speed: 100~300pcs/min
View specification →
In-mould labelling puts the print inside the wall, so a label fault is a scrapped container, not a re-labelling job. These systems catch it at the moulder.
IML containers fail in ways that a plain container does not. The label can sit off position or skewed, wrinkle, trap air as a bubble, lift at the seam, print out of register, or drift in colour between shots. Any of those makes the whole moulded part unusable because the decoration cannot be removed.
Our IML systems image the container body and the label together, using customised lighting that reads print contrast without blowing out the highlights on glossy film. The AI system compares each part against the accepted appearance standard and rejects the failures online, with 360-degree coverage across the full container surface.
Because the same machine family covers cups, bowls, tubs and pails, a converter running several IML formats can standardise on one inspection platform and one operator interface rather than one machine per format.
Each entry carries the specification table and FAQ published for that configuration.
Inspection Speed: 100~300pcs/min
View specification →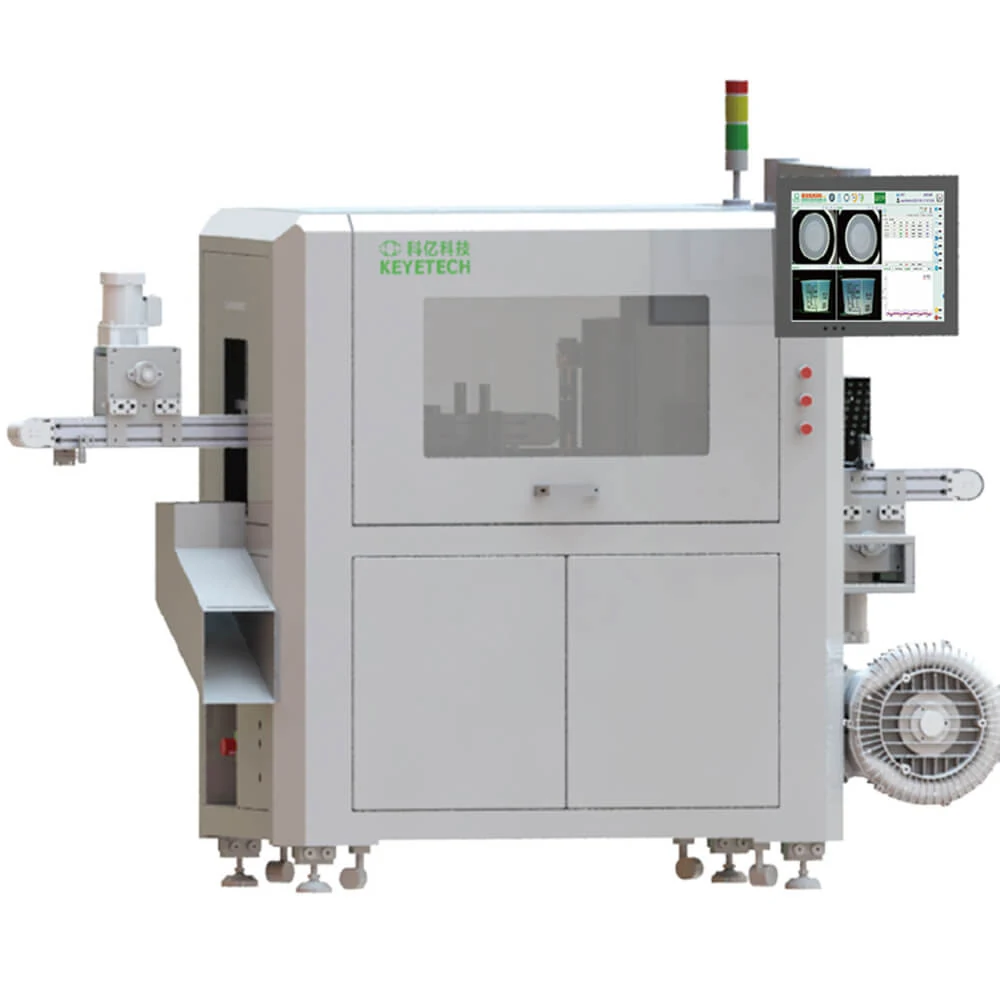
Inspection Speed: 100~300pcs/min
View specification →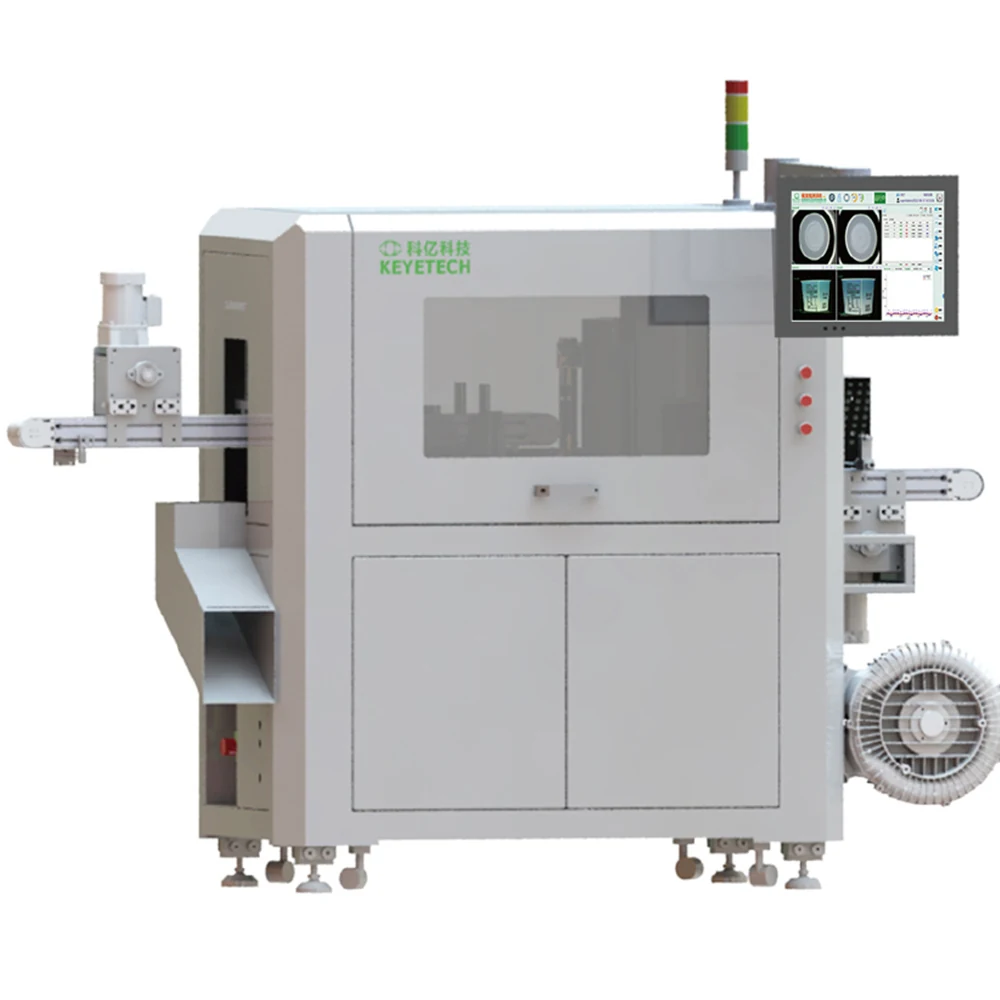
Inspection Speed: 100~300pcs/min
View specification →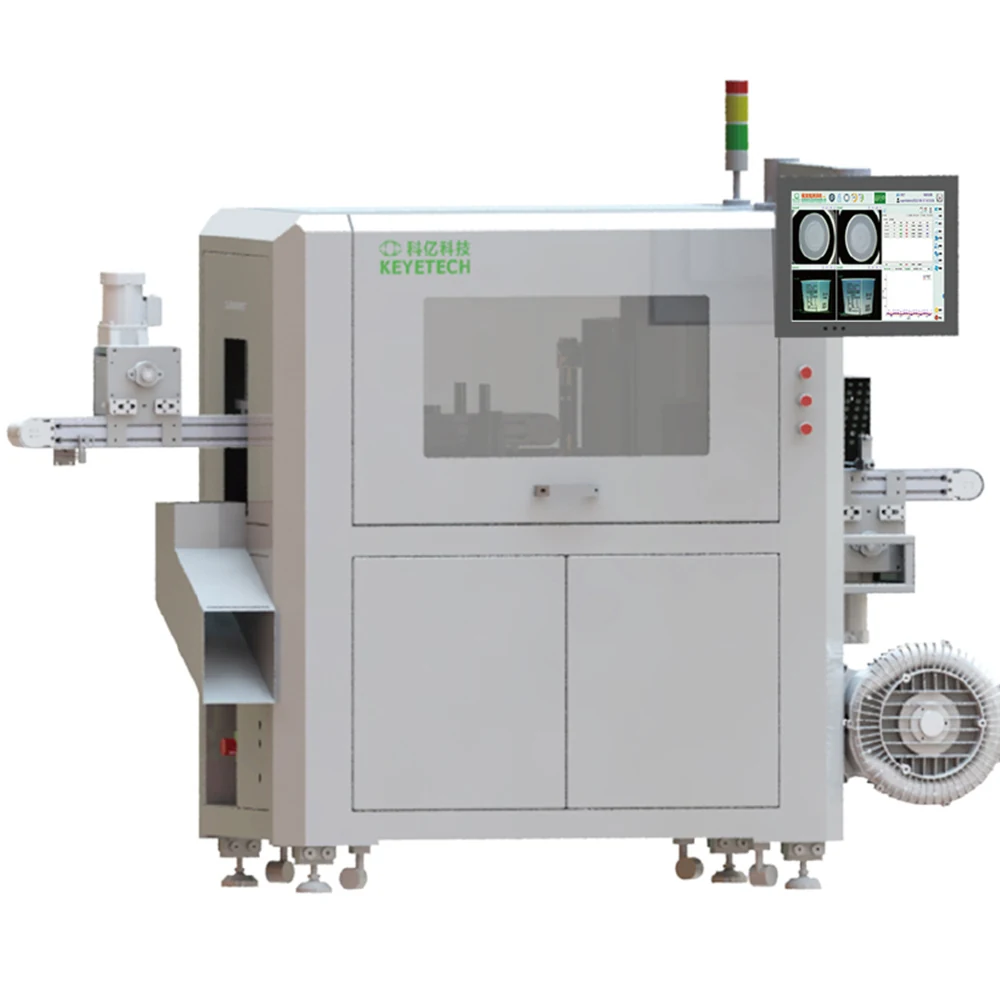
Inspection Speed: 100~300pcs/min
View specification →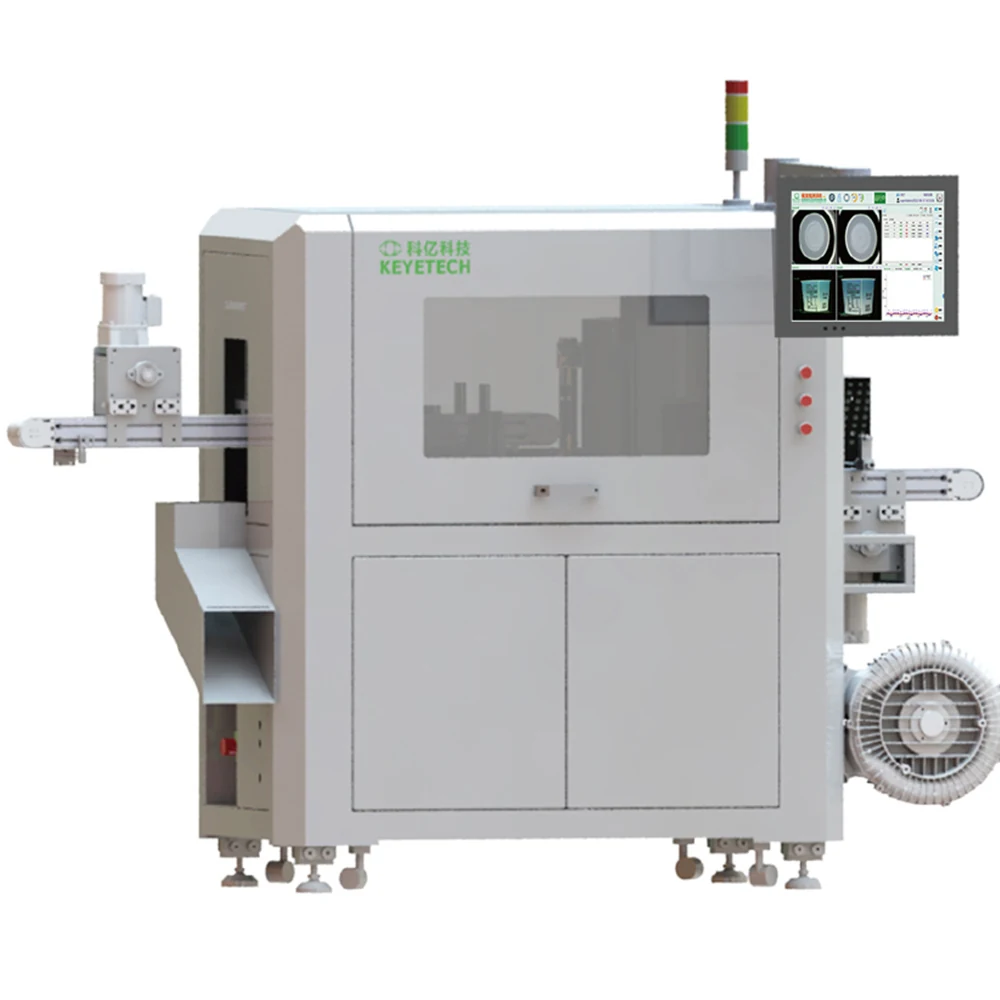
Inspection Speed: 100~300pcs/min
View specification →
Inspection Speed: 100~300pcs/min
View specification →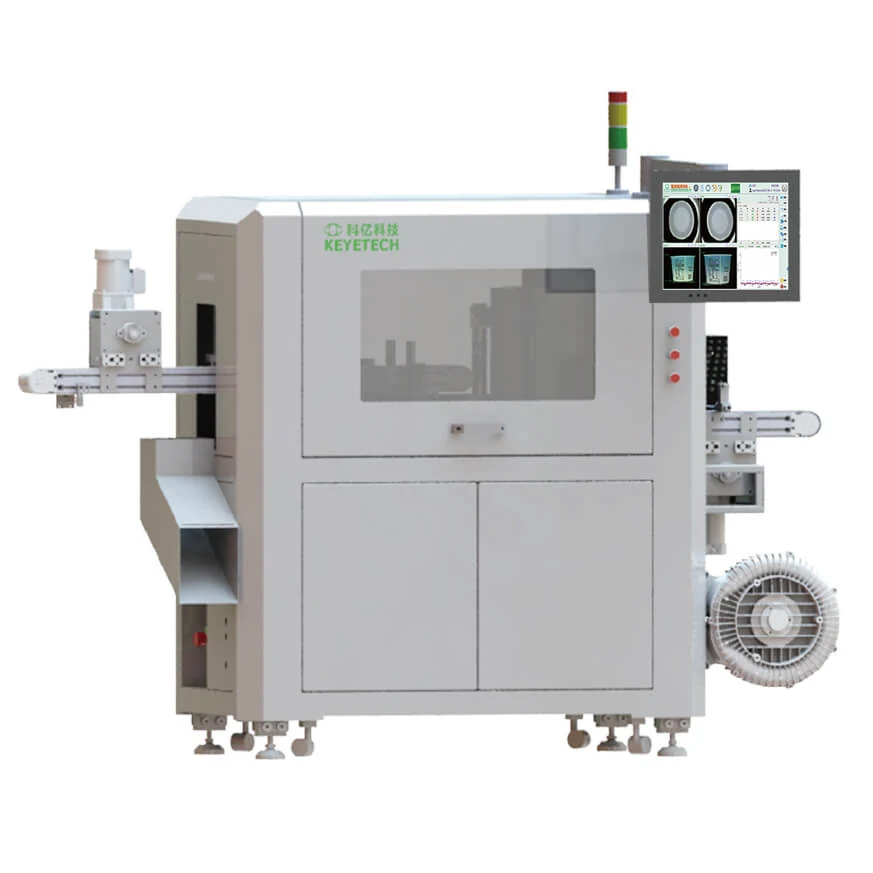
Inspection Speed: 100~300pcs/min
View specification →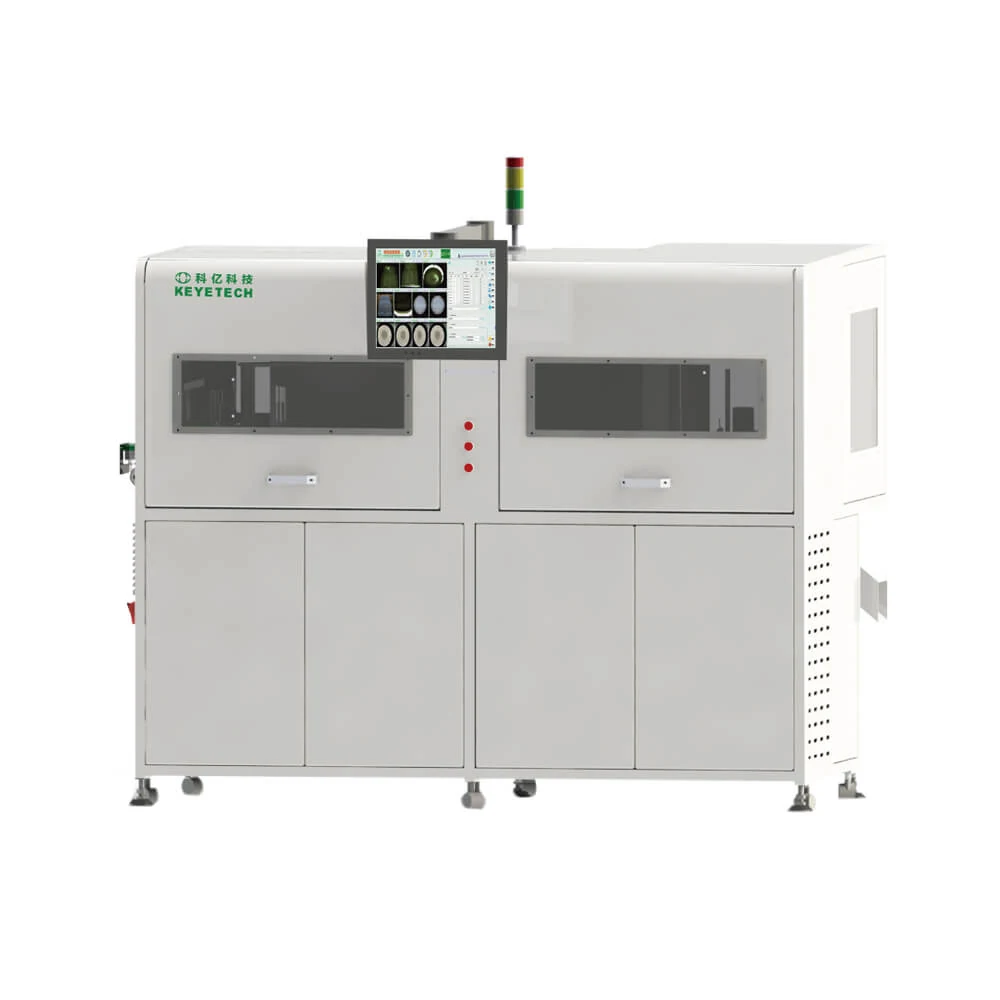
Inspection Speed: 100~300pcs/min
View specification →
Inspection Speed: 100~300pcs/min
View specification →
Inspection Speed: 100~300pcs/min
View specification →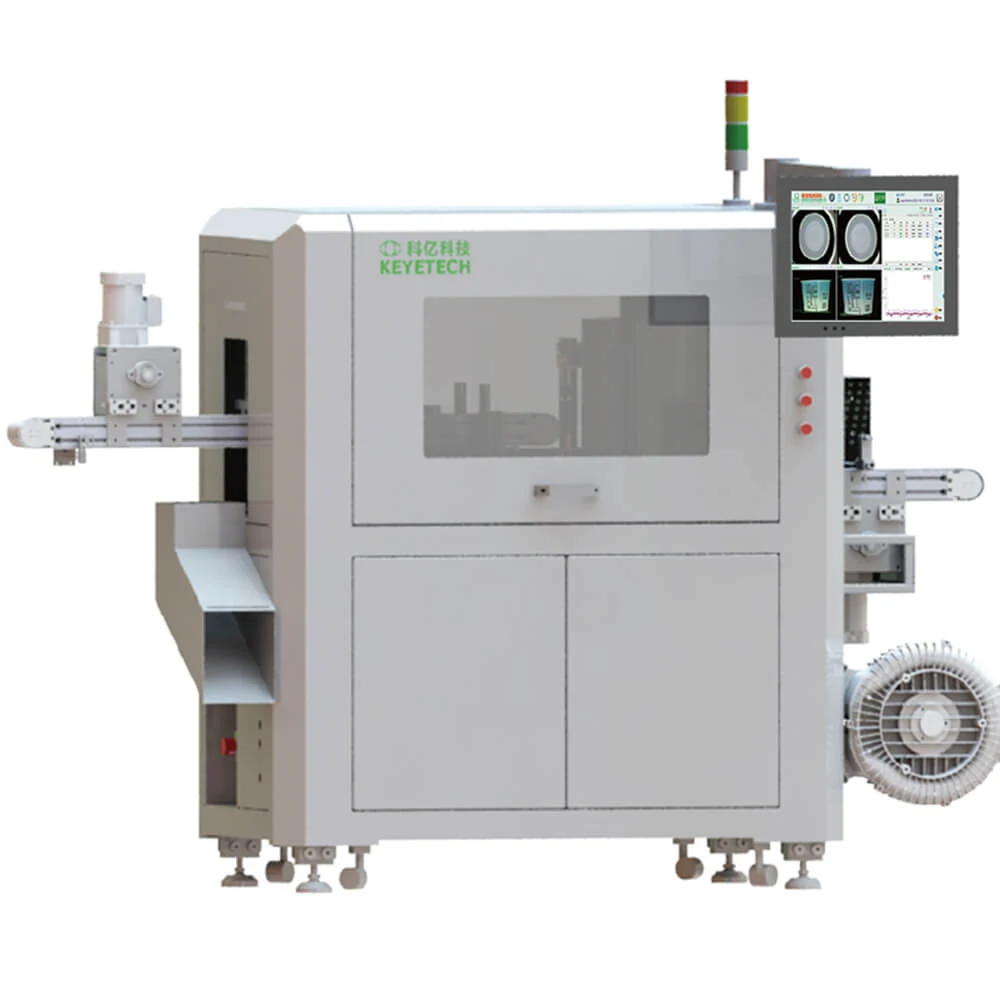
Inspection Speed: 100~300pcs/min
View specification →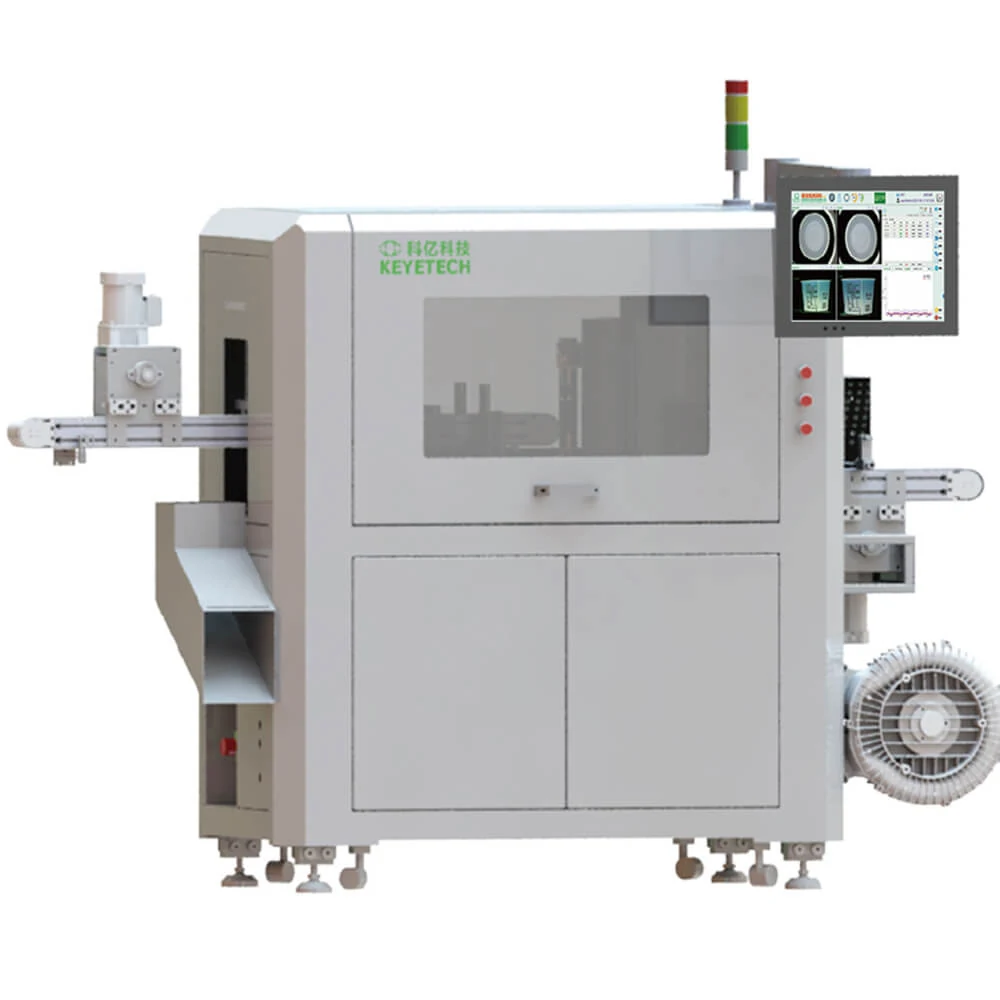
Inspection Speed: 100~300pcs/min
View specification →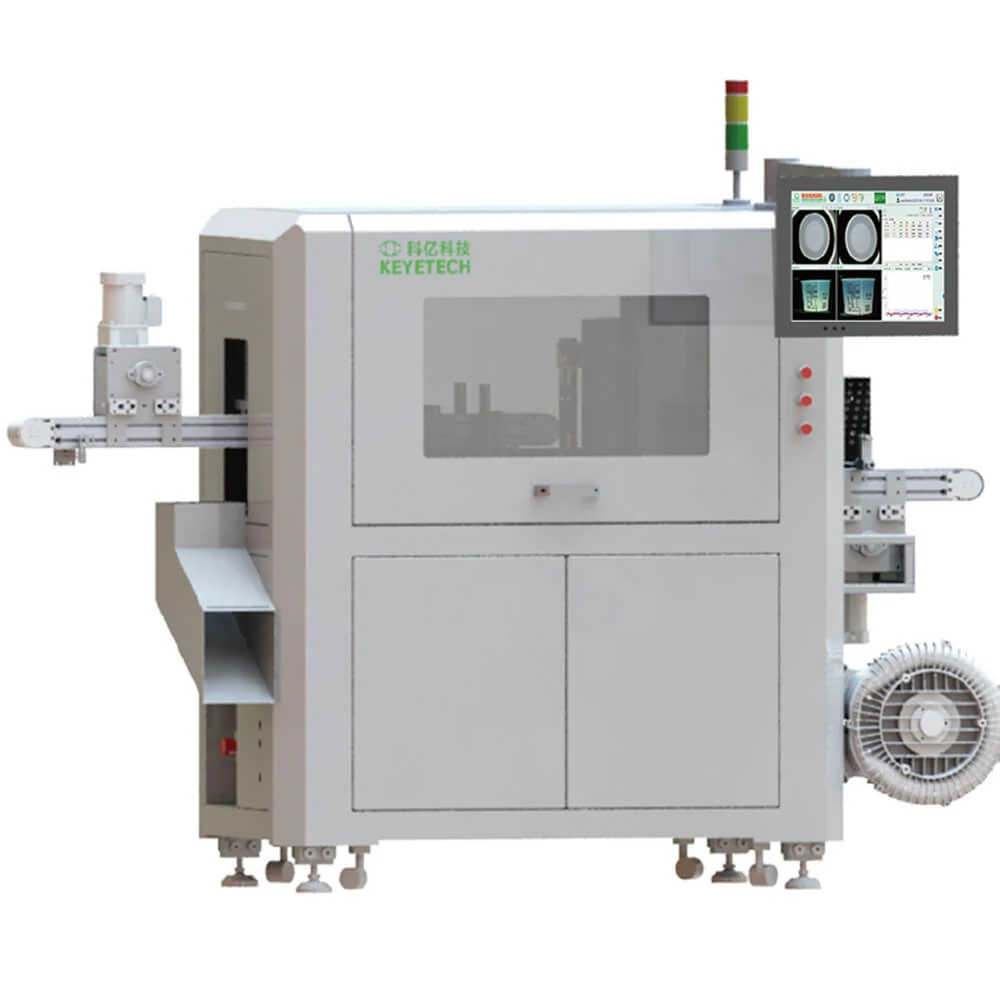
Inspection Speed: 100~300pcs/min
View specification →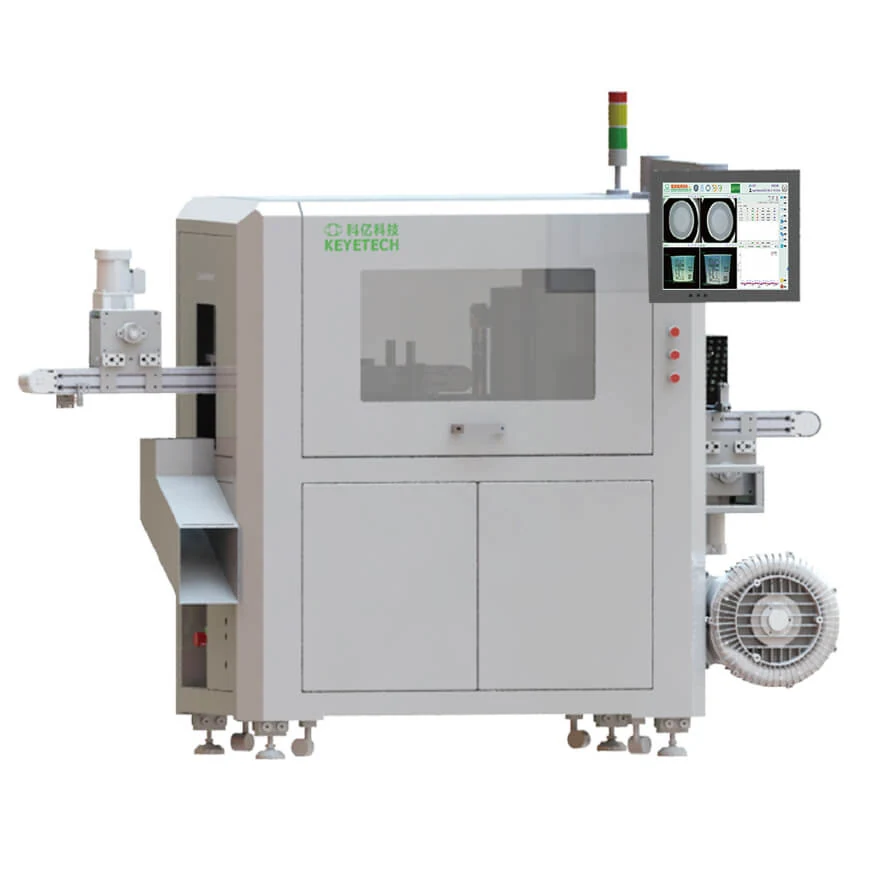
Inspection Speed: 100~300pcs/min
View specification →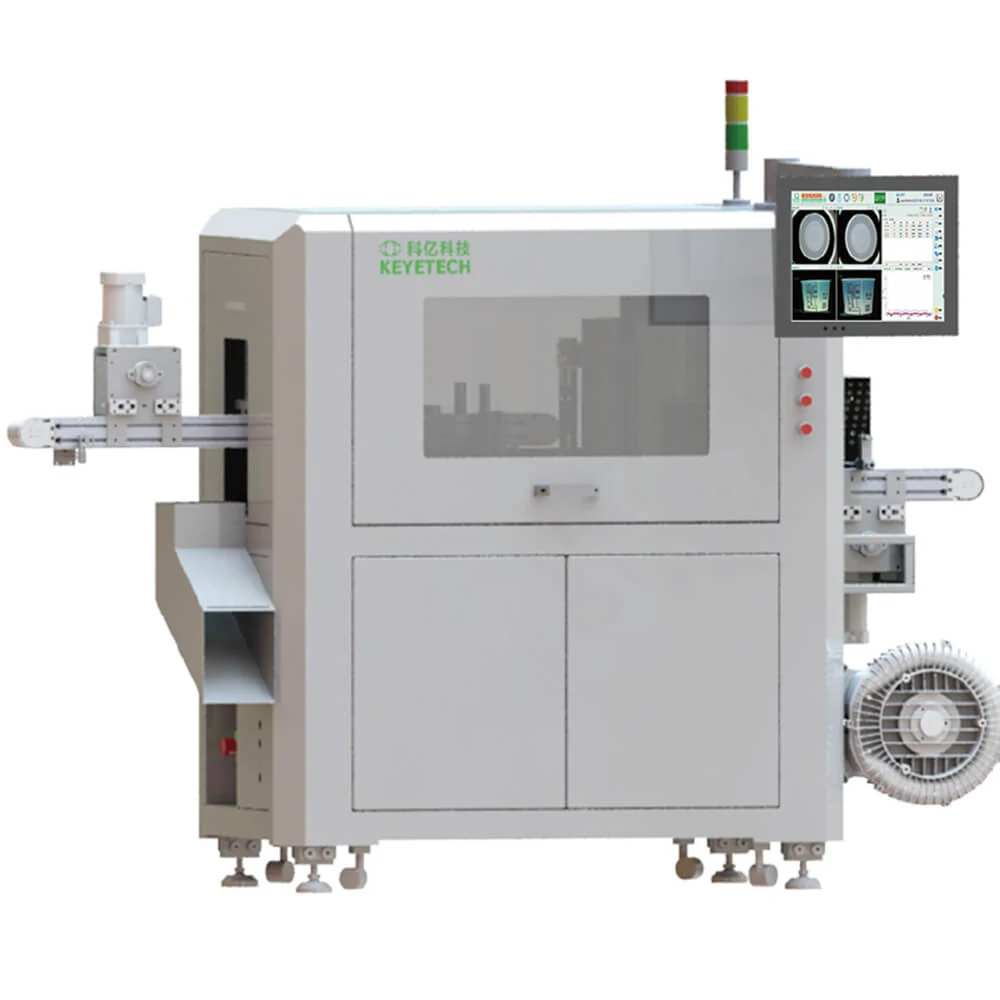
Inspection Speed: 100~300pcs/min
View specification →Inspection Speed: 100~300pcs/min
View specification →Inspection Speed: 100~300pcs/min
View specification →Inspection Speed: 100~300pcs/min
View specification →Cups, bowls, tubs, containers and pails. Format affects handling and camera placement; the inspection principle and software are the same.
Yes. The model is trained on your accepted appearance, so a wrinkle in the film, a black spot in the resin and a colour drift are all anomalies against that standard and can be classified separately.
Colour difference is one of the standard detected defect types. If you need per-cavity traceability, tell us at the enquiry stage so cavity identification is designed into the handling.
Inline with the take-out and conveyor of your IML moulding cell, or offline as a standalone station fed by our material feeder.
Typically 100 to 300 pieces per minute for IML containers, depending on part size, how many views are needed and the precision setting.
Container drawings or samples, the label artwork, the defect list with physical defect samples, required speed and precision, and whether the installation is inline at the moulder or offline.
Send the part, the defect list, the speed and the precision. We image your real samples before we quote.