Manganese Steel Castings
Jaw Crusher Plates and Wear Parts
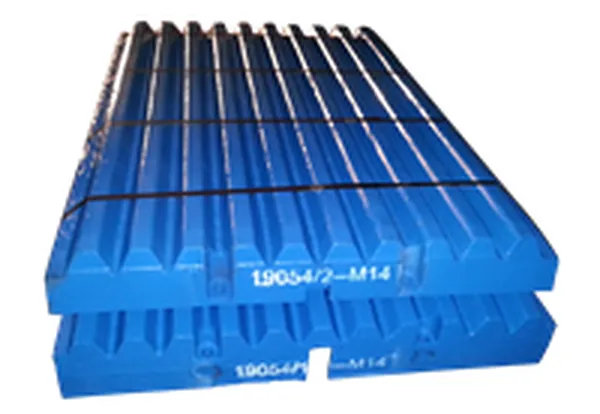
Jaw plates are the highest volume wear part in most aggregate plants. Tooth profile, alloy and seating decide how many tonnes you get before the change out.
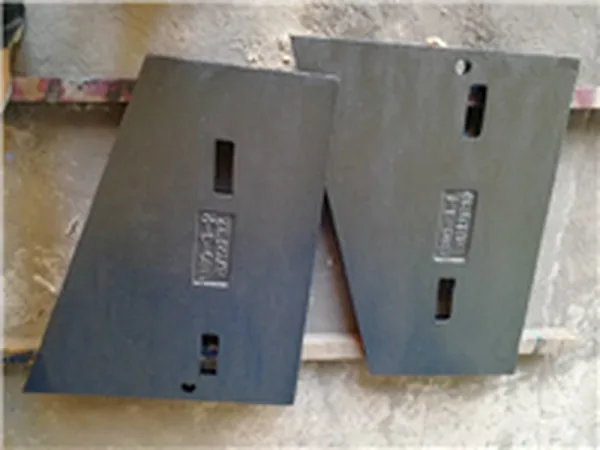
- Fixed and swing jaw plates, cheek plates and toggle plates
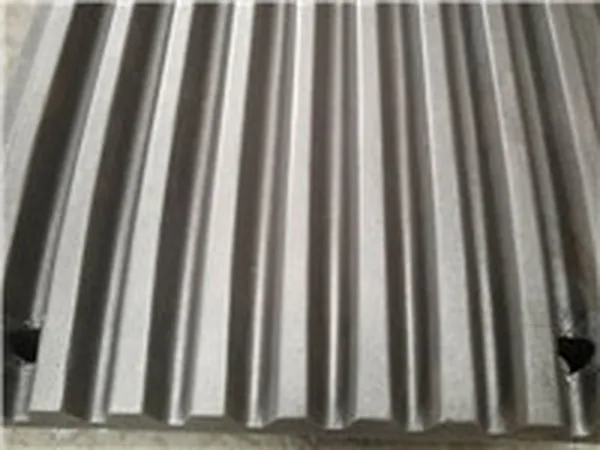
- Corrugated and custom tooth profiles to drawing
- Cast, heat treated and dimensionally checked
- Repeat batches from held tooling
Product Overview
About This Programme
Typical products are jaws, check plates, wear plates, toggle plates and others. We produce them in austenitic manganese steel with a written technical specification covering smelting, moulding, pouring and heat treatment so that batch quality stays stable.
The tooth profile matters as much as the alloy. A coarse profile grips large feed but reduces the effective contact area, and a fine profile gives a better product shape but wears the tips faster. If you send us the feed size and the product you need, we can advise which of your existing profiles is worth keeping.
Key Benefits
Key Benefits
Why buyers move this part to us, in their words rather than ours.
Stable batch hardness
Every batch is hardness tested and reported, so plate life is predictable across a delivery.
Correct seating
Back face flatness and bolt geometry checked, because a plate that does not seat will crack at the wedges.
Tooling held for reorders
After the first article your tooling stays with us, which shortens repeat lead times.
Application Scenarios
Application Scenarios
- Primary jaw crushers in quarrying and mining
- Recycling and demolition crushing lines
- Coal and limestone sizing plants
- Mobile jaw crusher spreads
Who It Is For
Who It Is For
Quarry and aggregate producers
Buying plates on a fixed maintenance interval.
Recycling operators
Crushing concrete and demolition rubble where feed is unpredictable.
Crusher dealers
Holding stock of common plate sizes against seasonal demand.
Problems It Solves
Problems It Solves
If one of these is happening on your plant, send us the part and the current life figures.
- Plates cracking at the wedge or bolt line instead of wearing out
- Back faces out of flat so the plate rocks in the frame
- Tooth profile that does not match the feed, giving poor throughput
- Hardness variation across a delivery making life unpredictable
- Stock outs on the fastest moving plate size
Technical Features
Technical Features and Materials
Alloy
Austenitic manganese steel, grade selected against feed hardness and impact level.
Profile
Corrugated, coarse, fine or custom tooth profiles cast to drawing.
Back face
Checked for flatness and bolt geometry so the plate seats correctly.
Heat treatment
Solution treatment and quench to a fixed cycle, with hardness reported per batch.
Manufacturing Process
Manufacturing Process
The moulding route is chosen for the part. It is confirmed in writing with the quotation, together with the tolerance class and the machining allowance.
| Process | Best Suited For | Tolerance | Piece Weight |
|---|---|---|---|
| Green sand process | Small and medium parts with low dimensional requirement | CT11–CT14 | 0.2–200 kg |
| Resin sand process | Medium and large parts with high dimensional requirement | CT10–CT11 | 100–3000 kg |
| Shell molding process | Small and medium parts with strict dimensional requirement | CT7–CT9 | ≤50 kg |
| Lost foam process | Small and medium parts with complex structure | CT7–CT9 | ≤100 kg |
| Vacuum process | Medium and large parts needing good surface roughness | CT7–CT9 | ≤10000 kg |
Quality Control
Quality Control and Certification
Inspection is planned at the stages where a problem is still cheap to fix.
- Chemical composition by optical emission and handheld spectrometer
- Hardness tested and reported on every batch
- Dimensions checked against your drawing or the master sample
- Non destructive testing by magnetic particle, penetrant or ultrasonic method where the drawing requires it
Certification documents are issued by the producing factory for the specific order. Ask for the certificate package that applies to your part before you place the order.
Customization
Customization Options
Material and grade
Any grade in the programme, or a grade you nominate with the local equivalent confirmed before production.
Geometry and fixing
Produced to your drawing or reverse engineered from a worn sample, including bolt and seat geometry.
Marking and packing
Part number marking, position marking for sets, and export packing agreed before production.
Use Guide
How to Order
STEP 01
Send the drawing or the worn part
A drawing, a 3D file, or photographs with overall dimensions and the machine details. Add the annual quantity.
STEP 02
Confirm material and construction
We propose the grade and, where relevant, the construction, and explain the trade off against your current part.
STEP 03
First article
Tooling is made and the first article is measured and tested before the batch is released.
STEP 04
Batch and inspection
Stage inspections during production and a final inspection to the agreed standard with the reports you need.
STEP 05
Packing and shipment
Export packing marked with your part numbers, with the shipping documents you require.
FAQ
Questions About Jaw Crusher Plates and Wear Parts
Can you copy our existing jaw plate?
Which tooth profile should I order?
Why do plates crack rather than wear?
Do you supply the wedges and fixings?
What quantity do you normally ship?
Send the Part and We Will Quote It
Photographs of the worn part with dimensions and the machine details are usually enough to start. Our engineers reply with the material, the construction and a price.