Casting Material
High Chrome Iron Castings
High chrome iron is the answer when abrasion, not impact, is destroying your parts. It outlasts alloy steel by a wide margin while staying tougher than ordinary white iron.
- BTMCr2 to BTMCr26 and ISO 21988 equivalents
- Hardness typically 55 HRC and above after heat treatment
- Good resistance to hot and corrosive service
- Supplied cast, heat treated and machined
Product Overview
What High Chrome Iron Castings Are Good For
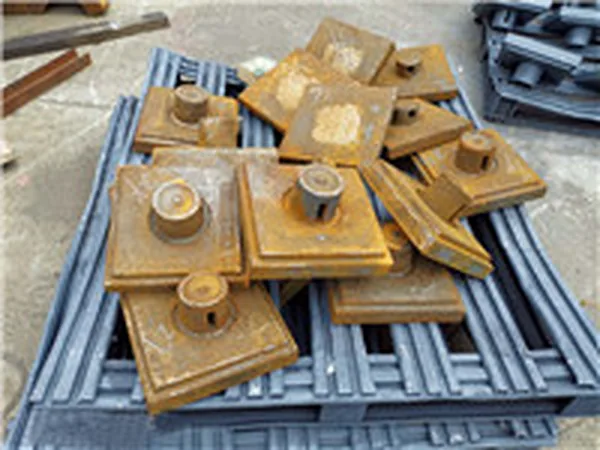
High chrome iron is an anti wear material with excellent performance. It has much higher wear resistance than alloy steel, much higher toughness and strength than ordinary white cast iron, and it also holds up well against high temperature and corrosion. We supply these castings to mining, cement, power plants and other industries.
The mechanism is simple. Chromium forms hard M7C3 carbides inside a martensitic matrix. The carbides resist the sliding abrasion of rock, slurry and clinker, and the matrix holds them in place. The higher the chromium, the more carbide volume, so a BTMCr26 liner lasts longer in sliding abrasion but tolerates less impact than a BTMCr15 one.
Who It Is For
Who Buys These Castings
The same material serves very different buyers. These are the four groups that make up most of our enquiries for this range.
Crushing plant operators
Wear plates, blow bars and liners that decide the change out interval.
Slurry pump builders
Pump shells and rotors handling abrasive slurries.
Cement and coal plants
Vertical mill shells and grinding elements exposed to constant sliding abrasion.
Agricultural equipment makers
Ground engaging and wear resistant parts.
Problems It Solves
Problems These Castings Solve
Buyers come to us when one of these is happening. If you recognise your situation here, send the drawing and the current part life.
- Wear parts changed far more often than the maintenance plan allows
- Alloy steel parts that deform instead of wearing evenly
- Cracking when a wear part is over specified in chromium for an impact duty
- Hardness that varies from piece to piece across a delivery
- Long lead times on liners that stop the plant when they run out
Manufacturing Process
Manufacturing Process and Piece Weight
We choose the route from the part, not from what one factory happens to own. The route is confirmed in writing with the quotation.
| Process | Best Suited For | Tolerance | Piece Weight |
|---|---|---|---|
| Green sand process | Small and medium parts with low dimensional requirement | CT11–CT14 | 0.2–200 kg |
| Resin sand process | Medium and large parts with high dimensional requirement | CT10–CT11 | 100–3000 kg |
| Shell molding process | Small and medium parts with strict dimensional requirement | CT7–CT9 | ≤50 kg |
| Lost foam process | Small and medium parts with complex structure | CT7–CT9 | ≤100 kg |
| Vacuum process | Medium and large parts needing good surface roughness | CT7–CT9 | ≤10000 kg |
Specifications
Material Standards and Grades
We apply the industry specifications of the country you sell into, so that the metal parts we supply meet your local standard.
| Standard | Grades We Supply |
|---|---|
| GB/T 8263 | BTMNiCr2, BTCr9Ni5, BTMCr2, BTMCr8, BTMCr12, BTMCr15, BTMCr26 |
| DIN 1695 | 0.9610, 0.9620, 0.9625, 0.9630, 0.9635, 0.9640, 0.9645, 0.9650, 0.9655 |
| ISO 21988 | HBW555XCr13, HBW555XCr16, HBW555XCr21, HBW555XCr27, HBW600XCr20Mo2Cu |
Application Scenarios
Typical Products and Applications
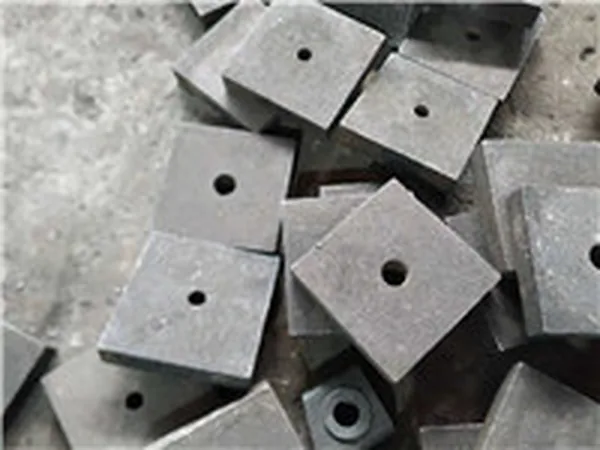
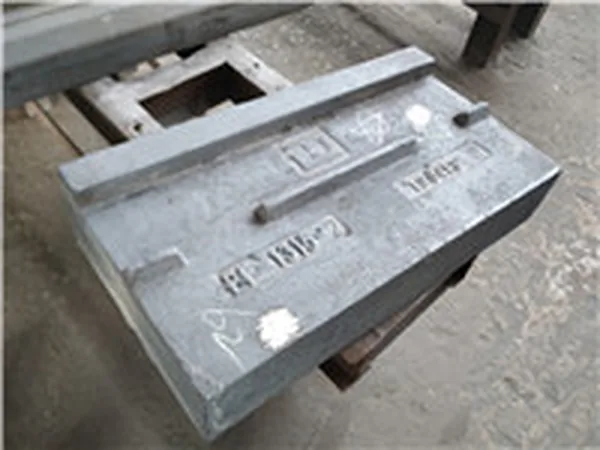
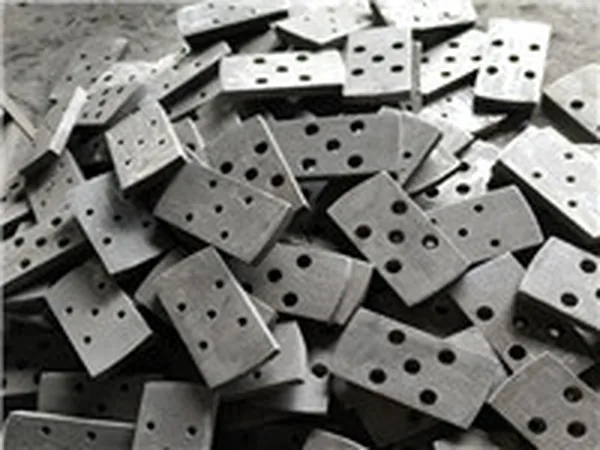
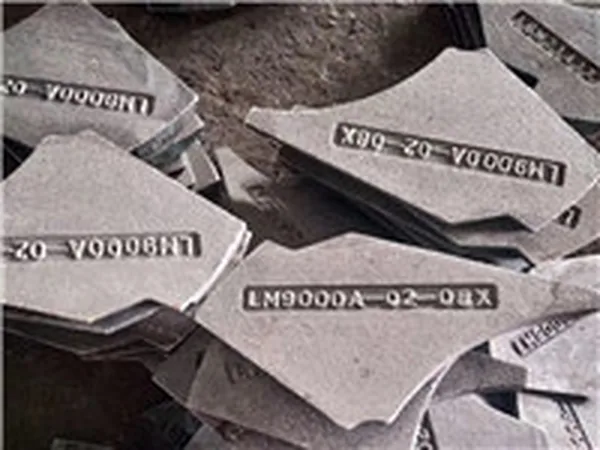
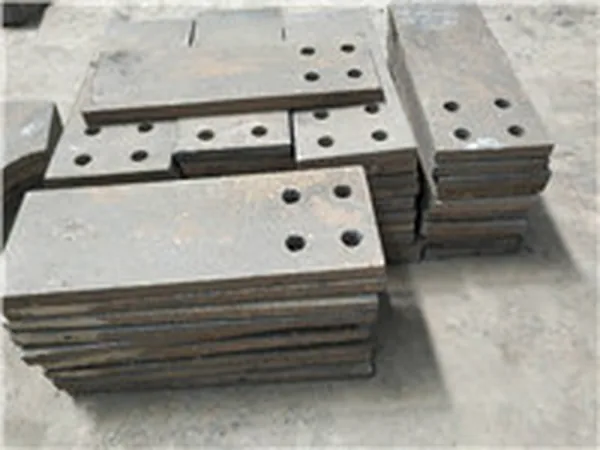
Every image below is a part actually produced through our supply chain.
- Wear plate for crusher
- Pump shell and rotor
- Blow bars from impact crusher
- Pipe fitting
- Milling balls
- Milling shell for vertical miller
- Agriculture wear resistant parts
Quality Control
Quality Control and Certification
Inspection is planned at the stages where a problem is still cheap to fix, not only at final inspection.
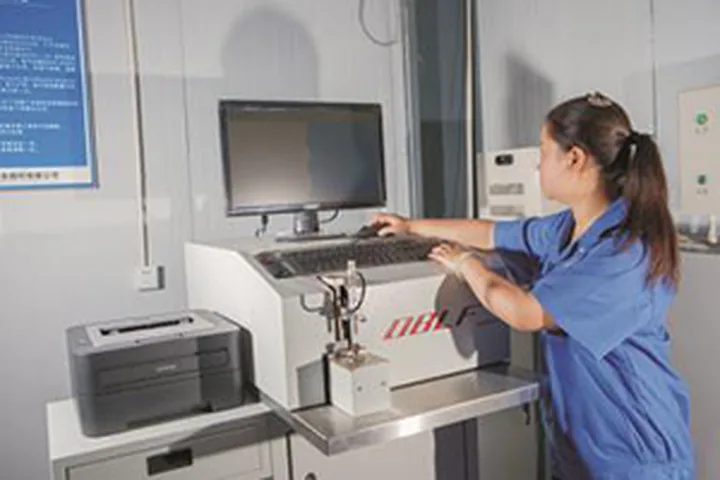
- Chemical composition by optical emission spectrometer, handheld spectrometer and carbon sulphur analyser
- Dimensions by manual gauging, gantry and mid size CMM and 3D scanning
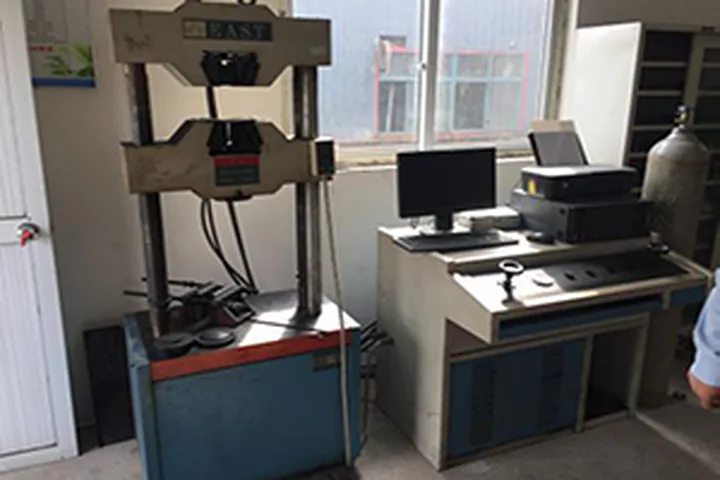
- Mechanical properties by tensile, impact and hardness testing
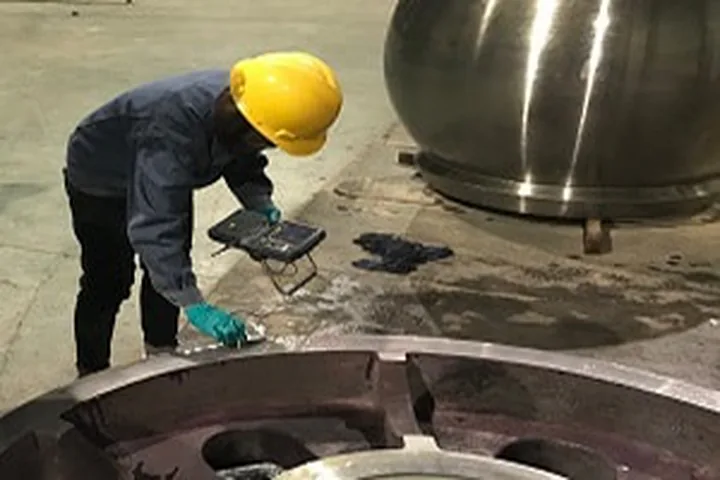
- Non destructive testing by magnetic particle, penetrant, ultrasonic and X-ray methods
Third party certification documents are issued by the producing factory for the specific order. Ask for the certificate package that applies to your part before you place the order.
Customization
Customization Options
Almost everything on this page can be adapted to your drawing.
Material and grade
Any of the grades listed above, or a grade you nominate. Where a local equivalent is required we confirm the cross reference before production.
Machining and tolerance
As cast, semi machined or finish machined. Mark the critical dimensions on the drawing and we confirm which faces are machined.
Surface and marking
Painting, powder coating, plating, galvanizing and part number marking, agreed at enquiry stage and priced into the piece price.
Comparison
Comparison With Other Options
A short answer to the question buyers ask most often before they place an order.
| Option | What You Gain and Give Up | Typical Use |
|---|---|---|
| High chrome iron | Highest abrasion resistance, low impact tolerance | Sliding abrasion duty |
| Manganese steel | Work hardens under impact, tougher | High impact duty |
| Alloy steel | Weldable and machinable, wears faster | Moderate wear duty |
Use Guide
How to Order and Use This Range
STEP 01
Send the drawing or the sample
A 2D drawing, a 3D file or clear photographs of the worn part with overall dimensions. Add the annual quantity and the target delivery date.
STEP 02
Agree material and process
We propose the grade and the moulding route, confirm tolerance class and machining allowance, and flag anything in the geometry that will add cost.
STEP 03
Tooling and first article
Pattern or die tooling is quoted separately. The first article is measured and tested before batch release.
STEP 04
Batch production and inspection
Stage inspections during production, then final inspection to the agreed standard with the test reports you require.
STEP 05
Packing and shipment
Export packing on fumigated pallets or in steel frames, marked with your part numbers, with the shipping documents you need.
FAQ
Questions About High Chrome Iron Castings
The answers buyers ask for before they place a first order.
BTMCr15 or BTMCr26, which should I use?
What hardness will the parts reach?
Can you match parts to my crusher brand?
Do you supply bimetal or insert reinforced wear parts?
How are these castings packed for export?
Send Your Drawing and Get a Quote
Send a 2D drawing, a 3D file or photographs of the worn part with the annual quantity. Our engineers reply with the process route, the material grade and a price.