Casting Material
Gray Iron Castings
Gray iron is the low cost route to rigid, vibration damping housings, frames and beds. We pour it in HT150 to HT300 and the matching ISO, EN, DIN, BS, JIS and ASTM grades, and machine it in house.
- 0.2 kg to 10 000 kg per piece
- CT7 to CT14 depending on moulding route
- Machined and painted to drawing
- ISO, EN, DIN, BS, JIS and ASTM grades
Product Overview
What Gray Iron Castings Are Good For
Gray cast iron is a relatively inexpensive cast iron with good casting properties and good machinability. It is widely used for frames, boxes, beds and shells. The graphite inside gray cast iron is distributed in flakes, and because graphite is prone to stress concentration, gray iron has low strength, plasticity and toughness compared with ductile iron. In return it gives excellent vibration damping, low notch sensitivity and good wear resistance.
Those properties decide where gray iron belongs. If your part carries impact or needs elongation, ductile iron is the better answer. If your part needs to stay dimensionally stable, absorb machine vibration and be cut quickly on a machining centre, gray iron is usually both the cheaper and the better engineering choice.
Who It Is For
Who Buys These Castings
The same material serves very different buyers. These are the four groups that make up most of our enquiries for this range.
Machine tool builders
Beds, columns, saddles and tables where damping and dimensional stability drive accuracy.
Pump and compressor makers
Bodies, covers and bearing housings poured in HT250 and HT300.
Municipal and construction suppliers
Covers, gratings, frames and architectural castings produced in repeat batches.
Agricultural and energy equipment
Gearbox housings, brackets and counterweights where cost per kilogram decides the project.
Problems It Solves
Problems These Castings Solve
Buyers come to us when one of these is happening. If you recognise your situation here, send the drawing and the current part life.
- Machine frames that ring or chatter and spoil surface finish
- Fabricated weldments that distort after stress relief and cost too much labour
- Suppliers who cannot hold a repeatable wall thickness across a batch
- Long lead times on medium volume housings and covers
- Porosity found only after machining, when the value added is already lost
Manufacturing Process
Manufacturing Process and Piece Weight
We choose the route from the part, not from what one factory happens to own. The route is confirmed in writing with the quotation.
| Process | Best Suited For | Tolerance | Piece Weight |
|---|---|---|---|
| Green sand process | Small and medium parts with low dimensional requirement | CT11–CT14 | 0.2–200 kg |
| Resin sand process | Medium and large parts with high dimensional requirement | CT10–CT11 | 100–3000 kg |
| Shell molding process | Small and medium parts with strict dimensional requirement | CT7–CT9 | ≤50 kg |
| Lost foam process | Small and medium parts with complex structure | CT7–CT9 | ≤100 kg |
| Vacuum process | Medium and large parts needing good surface roughness | CT7–CT9 | ≤10000 kg |
Specifications
Material Standards and Grades
We apply the industry specifications of the country you sell into, so that the metal parts we supply meet your local standard.
| Standard | Grades We Supply |
|---|---|
| ISO 185 | 185/JL/150, 185/JL/200, 185/JL/225, 185/JL/250, 185/JL/275, 185/JL/300 |
| GB/T 9439 | HT150, HT200, HT225, HT250, HT275, HT300 |
| EN 1561 | EN-GJL-150, EN-GJL-200, EN-GJL-250, EN-GJL-300 |
| DIN 1691 | GG-15, GG-20, GG-25, GG-30 |
| BS 1452 | 150, 180, 200, 220, 250, 300 |
| JIS G5501 | FC150, FC200, FC250, FC300 |
| ASTM A48 | No.20, No.25, No.30, No.35, No.40, No.45, No.50 |
Application Scenarios
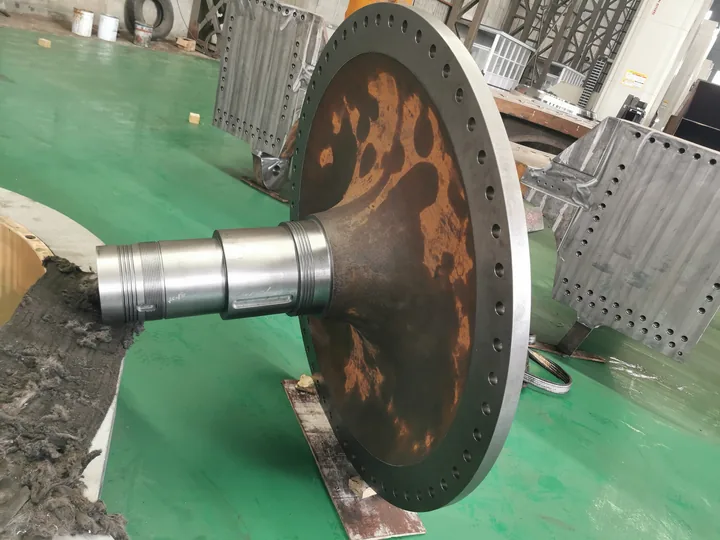
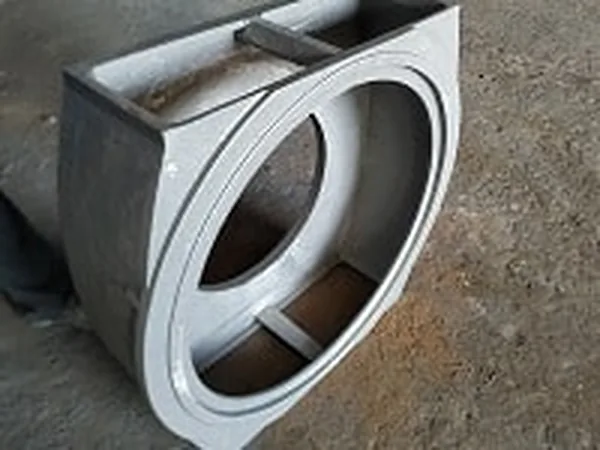
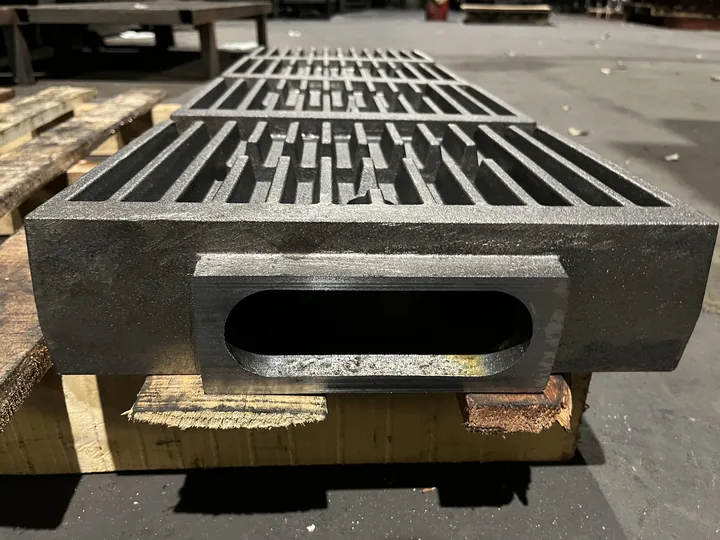
Typical Products and Applications
Every image below is a part actually produced through our supply chain.
- Municipal products
- Mechanical parts
- Agricultural machinery
- Architecture
- Energy field
- Cookware
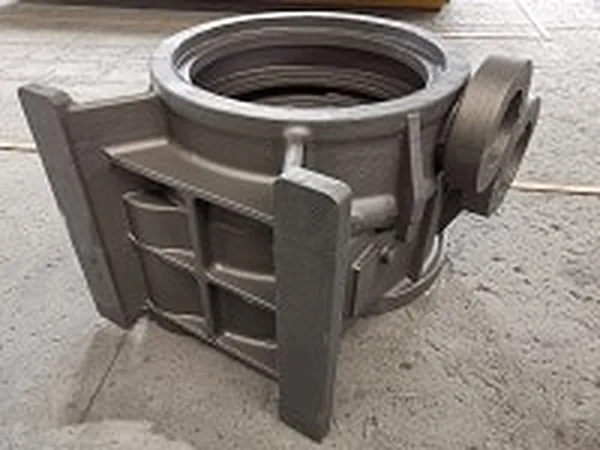
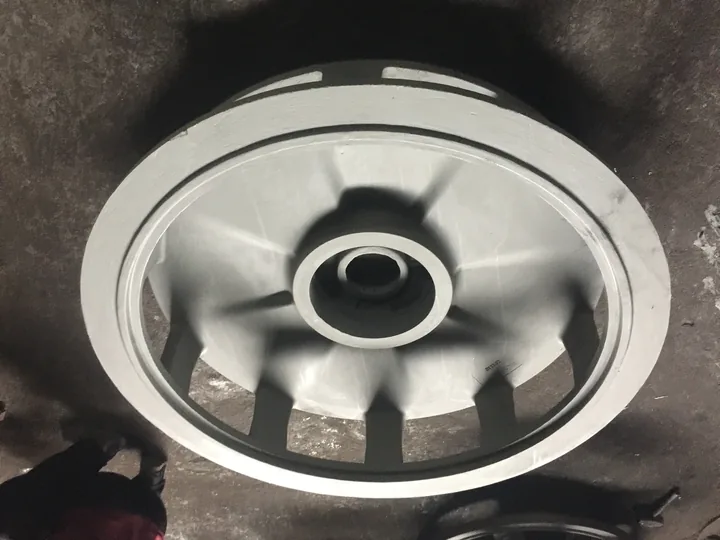
Quality Control
Quality Control and Certification
Inspection is planned at the stages where a problem is still cheap to fix, not only at final inspection.
- Chemical composition by optical emission spectrometer, handheld spectrometer and carbon sulphur analyser
- Dimensions by manual gauging, gantry and mid size CMM and 3D scanning
- Mechanical properties by tensile, impact and hardness testing
- Non destructive testing by magnetic particle, penetrant, ultrasonic and X-ray methods
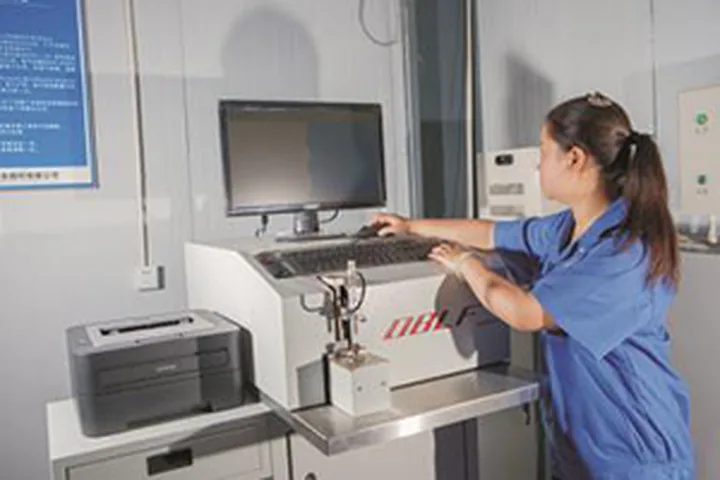
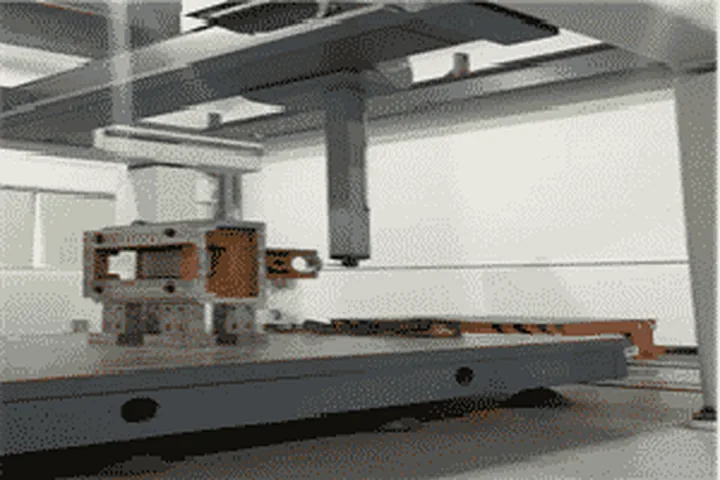
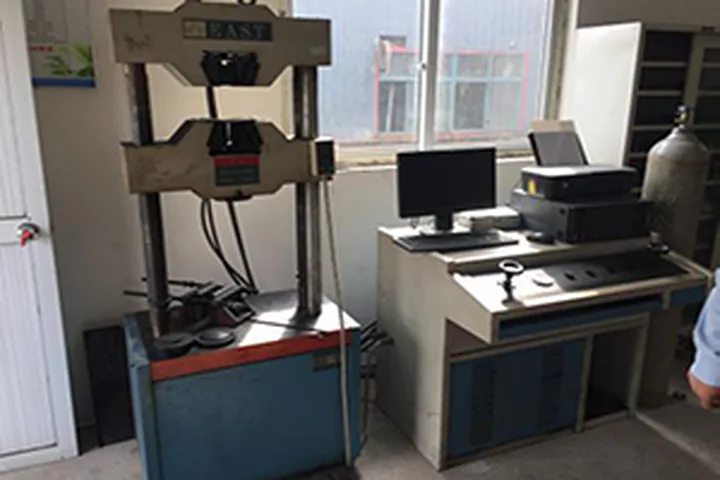
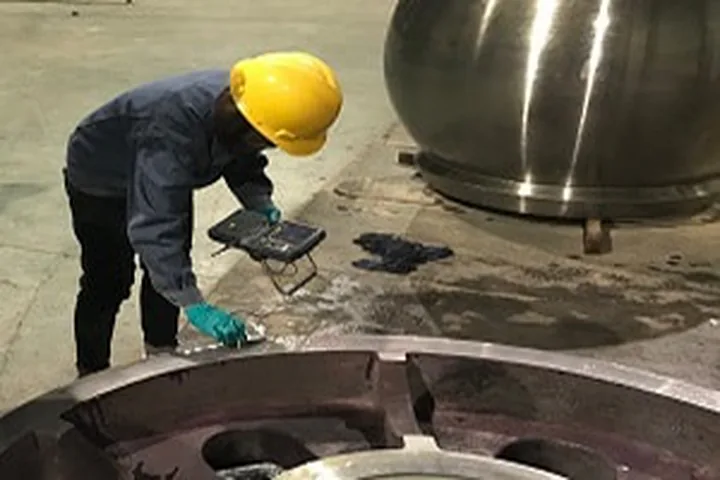
Third party certification documents are issued by the producing factory for the specific order. Ask for the certificate package that applies to your part before you place the order.
Customization
Customization Options
Almost everything on this page can be adapted to your drawing.
Material and grade
Any of the grades listed above, or a grade you nominate. Where a local equivalent is required we confirm the cross reference before production.
Machining and tolerance
As cast, semi machined or finish machined. Mark the critical dimensions on the drawing and we confirm which faces are machined.
Surface and marking
Painting, powder coating, plating, galvanizing and part number marking, agreed at enquiry stage and priced into the piece price.
Comparison
Comparison With Other Options
A short answer to the question buyers ask most often before they place an order.
| Option | What You Gain and Give Up | Typical Use |
|---|---|---|
| Gray iron | Best damping, lowest cost, low elongation | Frames, beds, housings |
| Ductile iron | Higher strength and elongation, higher cost | Load carrying parts |
| Cast steel | Highest strength and weldability, highest cost | Impact and structural parts |
Use Guide
How to Order and Use This Range
STEP 01
Send the drawing or the sample
A 2D drawing, a 3D file or clear photographs of the worn part with overall dimensions. Add the annual quantity and the target delivery date.
STEP 02
Agree material and process
We propose the grade and the moulding route, confirm tolerance class and machining allowance, and flag anything in the geometry that will add cost.
STEP 03
Tooling and first article
Pattern or die tooling is quoted separately. The first article is measured and tested before batch release.
STEP 04
Batch production and inspection
Stage inspections during production, then final inspection to the agreed standard with the test reports you require.
STEP 05
Packing and shipment
Export packing on fumigated pallets or in steel frames, marked with your part numbers, with the shipping documents you need.
FAQ
Questions About Gray Iron Castings
The answers buyers ask for before they place a first order.
Which gray iron grade should I specify?
What is the largest gray iron casting you can pour?
Can you machine the castings as well?
Do you supply painted or primed castings?
How do you control porosity and hardness?
Send Your Drawing and Get a Quote
Send a 2D drawing, a 3D file or photographs of the worn part with the annual quantity. Our engineers reply with the process route, the material grade and a price.