
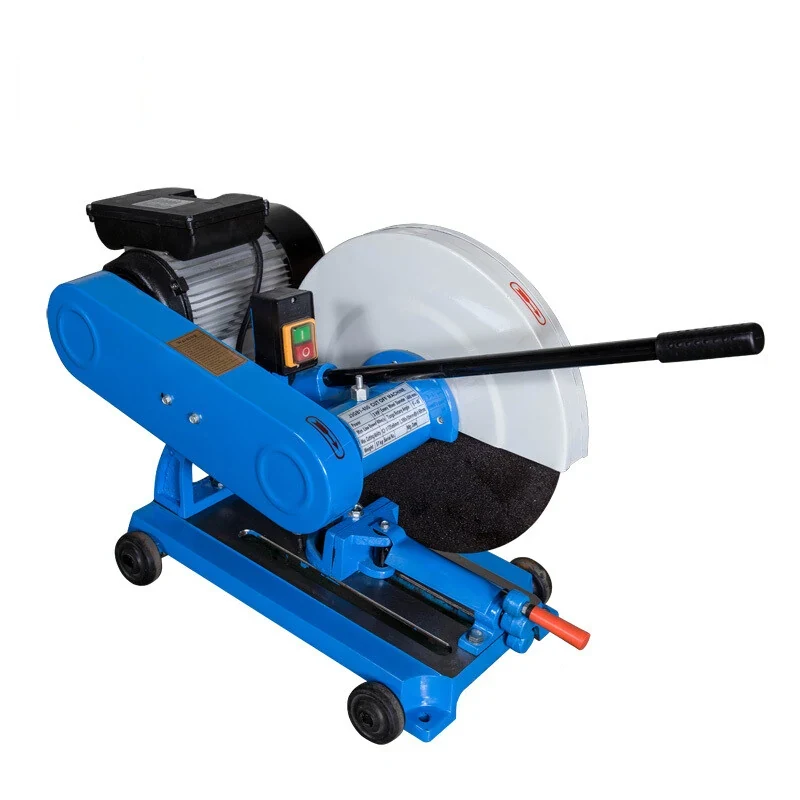
Shape Cutter J3GA-400
The J3GA-400 is an abrasive cut-off machine for the fabrication shop: a 400 mm fibre-reinforced cutting wheel driven by a 3 kW motor takes steel tube up to 135 mm diameter with 6 mm wall, angle iron up to 100 x 10 mm, channel steel up to 126 x 53 mm and round bar up to 50 mm diameter. Spindle no-load speed is 2280 rpm,...
What This Machine Does
The J3GA-400 is an abrasive cut-off machine for the fabrication shop: a 400 mm fibre-reinforced cutting wheel driven by a 3 kW motor takes steel tube up to 135 mm diameter with 6 mm wall, angle iron up to 100 x 10 mm, channel steel up to 126 x 53 mm and round bar up to 50 mm diameter. Spindle no-load speed is 2280 rpm, giving a wheel line speed of 48 m/s against a wheel safety line speed of 60 m/s, so the machine runs inside the wheel rating rather than at its limit. Both the body and the base are cast iron, which gives the machine the mass to hold the cut steady and the durability to stay in a working shop for years. The tongs rotate plus or minus 45 degrees for mitre cuts. The handle can be matched with a special switch for safe and reliable control. The base measures 540 x 320 mm and the machine weighs 80 kg gross and 70 kg net.
Why Buyers Choose This Machine
- Cuts steel tube up to 135 mm diameter with 6 mm wall in one pass
- Handles angle iron to 100 x 10 mm channel steel to 126 x 53 mm and round bar to 50 mm
- Wheel line speed of 48 m/s stays well inside the 60 m/s wheel safety line speed
- Tongs rotate plus or minus 45 degrees so mitre cuts are made without a separate setup
- Cast iron body and base give the mass to damp vibration during the cut
- 3 kW 4 HP motor drives the wheel through heavy sections without stalling
- Handle can be matched with a special switch for safe reliable operation
- 80 kg gross weight in a 75 x 44 x 62 cm carton makes it straightforward to ship and relocate
Where Shape Cutter J3GA-400 Earns Its Place
Problems It Solves
- Hand-cutting section with a grinder is slow and leaves an out-of-square end
- Mitred joints need a repeatable angle that a hand cut cannot give
- A light machine bounces on a heavy section and the wheel binds or shatters
- Running a wheel above its safety line speed is a real hazard in a busy shop
- Underpowered cut-off saws stall in thick-walled tube and channel
- Heavy stationary saws cannot be moved to where the steel is
Who It Is For
- Steel fabrication and structural workshops
- Construction contractors cutting section on site
- Maintenance workshops cutting stock material
- Metal window door and frame makers
- Distributors supplying abrasive cut-off saws to the trade
Application Scenarios
- Cutting steel tube and pipe to length in a fabrication shop
- Cutting angle iron and channel steel for structural fabrication
- Mitring sections at 45 degrees for frames and brackets
- Cutting round bar stock to length before machining
- Site or workshop cutting where a compact machine has to be moved between jobs
- Cutting reinforcement and light structural steel on construction projects
Technical Detail
Technical Features
- Motor 3 kW 4 HP
- Spindle no-load speed 2280 rpm
- Emery wheel no-load line speed 48 m/s and safety line speed 60 m/s
- Fibre-reinforced grinding wheel 400 x 32 x 3.2 mm or 400 x 25.4 x 3.2 mm
- Cutting ability steel tube 135 x 6 mm angle iron 100 x 10 mm channel steel 126 x 53 mm round bar 50 mm
- Tongs rotary angle plus or minus 45 degrees
- Cast iron body and base
- Handle able to take a special switch for safe operation
Specifications
| Machine type | Abrasive cut-off shape cutter |
|---|---|
| Models | J3GA-400 |
| Motor | 3 kW (4 HP) |
| Spindle no-load speed | 2280 r/min |
| Wheel no-load line speed | 48 m/s |
| Wheel safety line speed | 60 m/s |
| Cutting wheel | Φ400 x Φ32 x 3.2 mm or Φ400 x Φ25.4 x 3.2 mm fibre reinforced |
| Cutting ability | Steel tube Φ135 x 6 angle iron 100 x 10 channel steel 126 x 53 round bar Φ50 |
| Tongs rotary angle | ±45° |
| Base dimensions | 540 x 320 mm |
| Gross / net weight | 80 kg / 70 kg |
| Packing dimensions | 75 x 44 x 62 cm |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Abrasive cut-off sawing
- Cutting to length
- Mitre cutting
Materials Handled
- Cast iron body and base
Quality Control
- Spindle no-load speed checked against the rated 2280 rpm before shipment
- Wheel guard and wheel mounting checked for fit at both 32 mm and 25.4 mm bore sizes
- Tongs rotation checked at square and at the 45 degree positions
- Motor run under load and checked for temperature and current draw
- Switch and handle operation tested
- Test cuts taken on tube and angle and checked for squareness
Customisation Options
- Wheel bore specified as 32 mm or 25.4 mm to match the wheels available in your market
- Supply voltage frequency and phase built for your market
- Special switch fitted to the handle where your safety rules require it
- Manual and machine plates prepared in your working language
- Carton or wooden case packing to suit your shipping route
How It Compares With the Alternatives
| CS-315 cold cutting saw | The cold saw leaves a square cool machined end ready to weld; the J3GA-400 is the lower-cost faster way to cut structural section where a ground finish is not needed |
|---|---|
| Hand-held angle grinder cutting | A grinder cut is freehand and rarely square; the J3GA-400 clamps the section in rotating tongs and cuts to a set angle |
| Band sawing structural section | A bandsaw gives a cleaner cut with no sparks but costs more and runs slower; the abrasive cutter gets through 135 mm tube quickly at a fraction of the machine cost |
Running the Machine
Step 1
Fit a fibre-reinforced 400 mm wheel with the correct bore and check it is undamaged before mounting
Step 2
Check the wheel is rated for at least the 48 m/s line speed of the machine
Step 3
Set the tongs angle square or up to plus or minus 45 degrees and clamp the section
Step 4
Keep the section seated against the fixed jaw so it cannot rotate during the cut
Step 5
Bring the wheel down at a steady rate and let it cut without forcing it
Step 6
Let the wheel stop before removing the cut piece and clear hot swarf away
Step 7
Replace the wheel before it wears below the size where it loses cutting depth
Related Applications and Guides
General Machining Job Shops
Job shops take whatever work comes through the door, which means their equipment has to cover a wide range rather than do one thing perfectly. XAIMC s
How to Choose a Metal Band Saw for a Fabrication Shop
A metal band saw cuts bar, tube, section and plate to length ahead of machining, welding and assembly, and the right one depends on section size, mate
Questions About Shape Cutter J3GA-400
What sizes will the J3GA-400 cut?
Steel tube up to 135 mm diameter with 6 mm wall, angle iron 100 x 10 mm, channel steel 126 x 53 mm and round bar up to 50 mm diameter.
What cutting wheel does it take?
A fibre-reinforced wheel of 400 x 32 x 3.2 mm or 400 x 25.4 x 3.2 mm. Tell us which bore size is standard in your market and we will supply the machine to suit.
Is the machine safe at its running speed?
The wheel no-load line speed is 48 m/s against a wheel safety line speed of 60 m/s, so the machine runs below the wheel rating. Always fit a wheel rated at or above the machine line speed.
Can it cut mitres?
Yes. The tongs rotate plus or minus 45 degrees.
How heavy is it and how is it packed?
Gross weight is 80 kg and net weight 70 kg, packed in a carton of 75 x 44 x 62 cm. Tell us your quantity and destination and we will confirm the shipping volume.
What motor and supply does it need?
The motor is 3 kW, 4 HP. Send us your supply voltage frequency and phase and the machine will be built to your market.
What are your payment and trade terms?
FOB CFR and CIF are available. Payment is 30 percent by T/T on order with 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the Shape Cutter J3GA-400
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.