
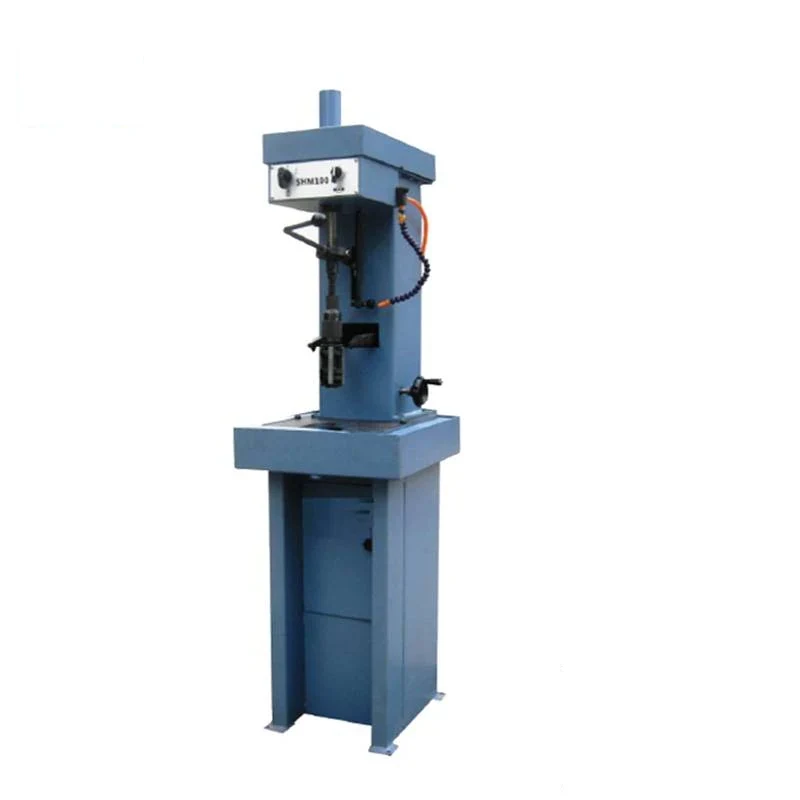
Cylinder Honing Machine SHM100
The SHM100 hones bored holes in cylinder blocks for motorcycles, factories and air compressors, and also holes in other mechanical parts. Honing diameter runs from 28 to 100 mm to a maximum depth of 200 mm, with a worktable of 290 x 150 mm and a work chamber of 390 x 200 mm. Spindle up and down reciprocating movement i...
What This Machine Does
The SHM100 hones bored holes in cylinder blocks for motorcycles, factories and air compressors, and also holes in other mechanical parts. Honing diameter runs from 28 to 100 mm to a maximum depth of 200 mm, with a worktable of 290 x 150 mm and a work chamber of 390 x 200 mm. Spindle up and down reciprocating movement is manual, which keeps the machine simple and puts stroke control in the operator's hands. Two spindle speeds are available in each supply configuration: 125 and 250 rpm on three-phase and 200 and 290 rpm on single-phase, with a main motor of 0.37/0.18 kW on three-phase and 0.55 kW on single-phase. That single-phase option matters for a small workshop without a three-phase supply. Voltage options are 3-380 V, 3-220 V and 1-220 V at 50 or 60 Hz. A 0.04 kW cooling pump serves the honing area. External dimensions are 400 x 580 x 1600 mm.
Why Buyers Choose This Machine
- Single-phase 220 V option lets a workshop without three-phase power hone properly
- 28 to 100 mm honing diameter covers motorcycle and air compressor cylinder bores
- Two spindle speeds in either supply configuration for different bore sizes
- Manual spindle reciprocation keeps stroke control with the operator and the machine simple
- 50 or 60 Hz supply options so the machine fits either mains standard
- 400 x 580 x 1600 mm external dimensions suit a bench-adjacent installation
- Cooling pump fitted, so the honing area stays flooded during the cycle
Where Cylinder Honing Machine SHM100 Earns Its Place
Problems It Solves
- A bored hole left unhoned has the wrong surface for ring or seal bedding
- Three-phase honing machines cannot be installed in a single-phase workshop
- A single spindle speed cannot suit both a 28 mm and a 100 mm bore
- Larger honing machines take floor space a small shop cannot give up
- Honing dry damages stones and the bore surface when no coolant pump is fitted
Who It Is For
- Motorcycle repair workshops honing their own cylinders
- Air compressor service and rebuild shops
- Small workshops limited to a single-phase electrical supply
- Distributors supplying compact honing equipment to repair shops
Application Scenarios
- Honing motorcycle cylinder bores after boring
- Air compressor cylinder honing in a compressor service shop
- Honing holes in other mechanical parts within the 28 to 100 mm range
- Factory cylinder block work where bores must be finished on site
- Workshops on single-phase supply that cannot run three-phase equipment
Technical Detail
Technical Features
- Honing diameter 28 to 100 mm
- Maximum honing depth 200 mm
- Manual spindle up and down reciprocating movement
- Worktable size 290 x 150 mm and work chamber 390 x 200 mm
- Spindle speed 125 and 250 rpm on three-phase, 200 and 290 rpm on single-phase
- Main motor 0.37/0.18 kW three-phase or 0.55 kW single-phase
- Voltage 3-380 V, 3-220 V or 1-220 V at 50 or 60 Hz
- Cooling pump motor power 0.04 kW
- External dimensions 400 x 580 x 1600 mm
Specifications
| Machine type | Vertical cylinder honing machine |
|---|---|
| Models | SHM100 |
| Honing diameter | 28 to 100 mm |
| Max honing depth | 200 mm |
| Spindle up and down reciprocating speed | Manual |
| Worktable size (L x W) | 290 x 150 mm |
| Work chamber scope (L x W) | 390 x 200 mm |
| Spindle speed | 125 and 250 rpm (three-phase); 200 and 290 rpm (single-phase) |
| Main motor power | 0.37 / 0.18 kW (three-phase); 0.55 kW (single-phase) |
| Cooling pump motor power | 0.04 kW |
| Voltage | 3-380 V, 3-220 V, 1-220 V |
| Frequency | 50 or 60 Hz |
| External dimensions (L x W x H) | 400 x 580 x 1600 mm |
Figures above are taken from the product information we hold. Send us your application and we will confirm the exact specification for the model quoted.
How It Is Built and What Can Be Changed
Operations Performed
- Honing
- Inner hole finishing
Quality Control
- Honed bore surface and diameter checked on a test part before shipment
- Spindle speeds verified against their ratings for the supply configuration ordered
- Cooling pump flow checked into the work chamber
- Honing depth verified against the 200 mm rating
- Machine run in through a honing cycle before packing
Customisation Options
- Supply configuration chosen as 3-380 V, 3-220 V or 1-220 V at 50 or 60 Hz
- Honing heads and stones specified within the 28 to 100 mm range for your bores
- Fixturing specified for the blocks or parts you hone most
- Manual prepared in the language your shop works in
How It Compares With the Alternatives
| XAIMC 3MB9808 vertical honing machine | The 3MB9808 hones 40 to 82 mm to 200 mm on a 450 kg press; the SHM100 covers 28 to 100 mm with a single-phase option and a smaller 400 x 580 x 1600 mm footprint |
|---|---|
| XAIMC VHM170 automatic honing machine | The VHM170 is a CNC machine with powered stroke control for production honing; the SHM100 uses manual spindle reciprocation and two fixed speeds |
| XAIMC SBM100 boring and honing machine | The SBM100 bores and hones on one frame; the SHM100 is a dedicated honing machine with a wider 28 to 100 mm honing range |
Running the Machine
Step 1
Confirm your supply is 3-380 V, 3-220 V or 1-220 V at 50 or 60 Hz and order the matching configuration
Step 2
Mount the cylinder block or part on the 290 x 150 mm worktable
Step 3
Fit honing stones for the bore diameter within 28 to 100 mm
Step 4
Select the spindle speed available in your supply configuration
Step 5
Check the cooling pump is delivering coolant into the work chamber
Step 6
Reciprocate the spindle manually through the bore within the 200 mm depth
Step 7
Check bore size and surface finish on the first part before running the batch
Other Machines in Engine Rebuilding Machine
Vertical Cylinder Honing Machine 3M9817
View Machine →
Automatic Cylinder Honing Machine VHM170
View Machine →
Vertical Cylinder Honing Machine 3MB9808
View Machine →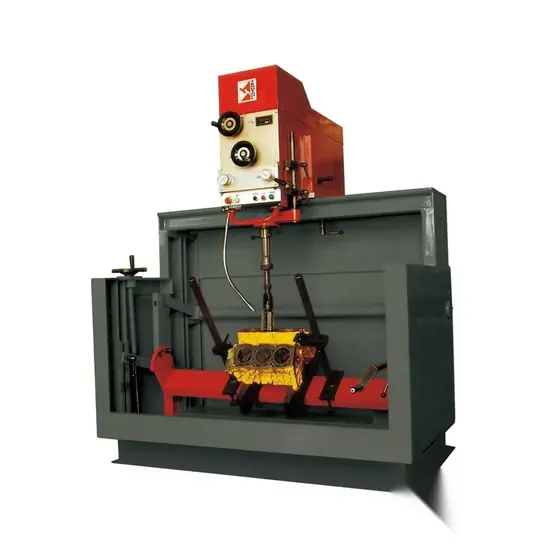
Vertical Air-Floating Cylinder Honing Machine THM170
View Machine →Related Applications and Guides
Engine Rebuilding Workshops
Engine rebuilding workshops recondition blocks heads crankshafts and valves to a geometry the engine will hold for a full service life. XAIMC supplies
Automotive Service and Fleet Workshops
Service centres and fleet depots keep vehicles moving. XAIMC supplies the lifting tyre wheel and fluid handling equipment those workshops use, includi
Cylinder Boring vs Honing - What Each Operation Does
Boring removes metal to bring a worn cylinder back to a round straight bore at a new oversize, while honing produces the final diameter, geometry and
How to Choose a Valve Seat Cutting Machine
A valve seat cutting machine machines the seat angles and the valve guide bore in a cylinder head so that the valve seals concentrically against the s
Questions About Cylinder Honing Machine SHM100
Can I run it on single-phase power?
Yes. The machine is offered for 1-220 V single-phase as well as 3-380 V and 3-220 V three-phase, at 50 or 60 Hz. Tell us your supply when you order.
What bore sizes will it hone?
28 to 100 mm diameter to a maximum honing depth of 200 mm.
Is the stroke powered?
No. Spindle up and down reciprocating movement is manual.
What spindle speeds are available?
125 and 250 rpm on three-phase supply, or 200 and 290 rpm on single-phase.
How big a part will fit?
The worktable is 290 x 150 mm and the work chamber scope is 390 x 200 mm. Send us your part dimensions and we will confirm.
Are honing stones included?
Honing heads and stones are specified against your bore sizes and material. Send us the bores you hone and we will quote them with the machine.
What are your payment and trade terms?
FOB CFR and CIF. Payment is 30 percent by T/T on order and 70 percent before shipment, or an irrevocable L/C at sight.
Request a Quote on the Cylinder Honing Machine SHM100
Send us the work you need it to do, the voltage on your site and the port you ship to. We will come back with the model, the tooling and the lead time.