Cylinder Blocks for Axial and Bent Axis Pumps
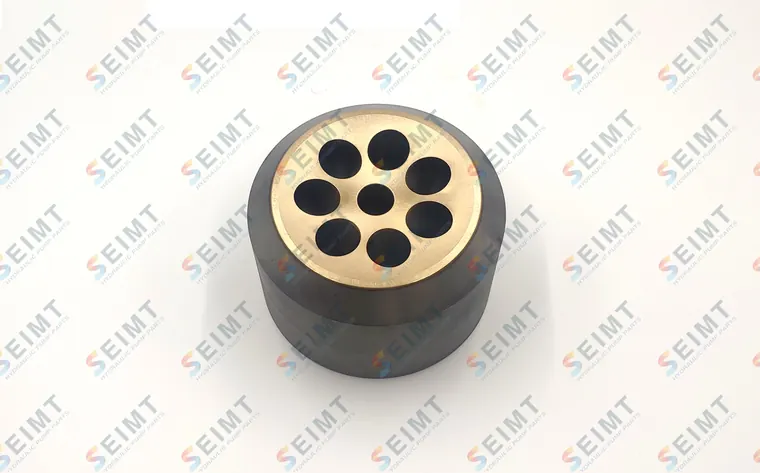
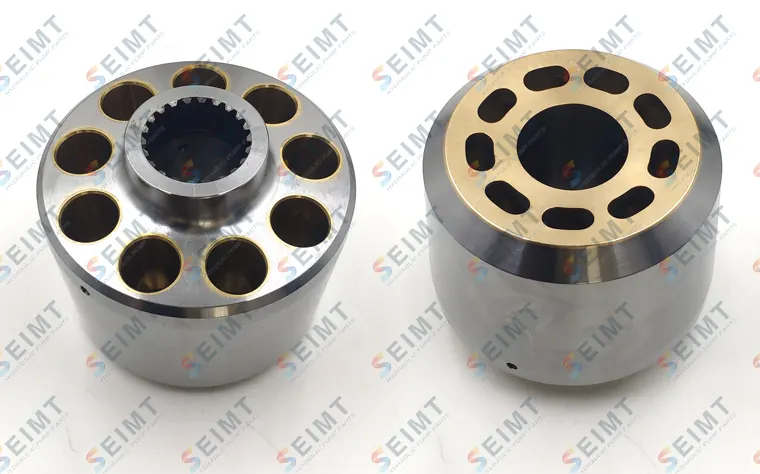
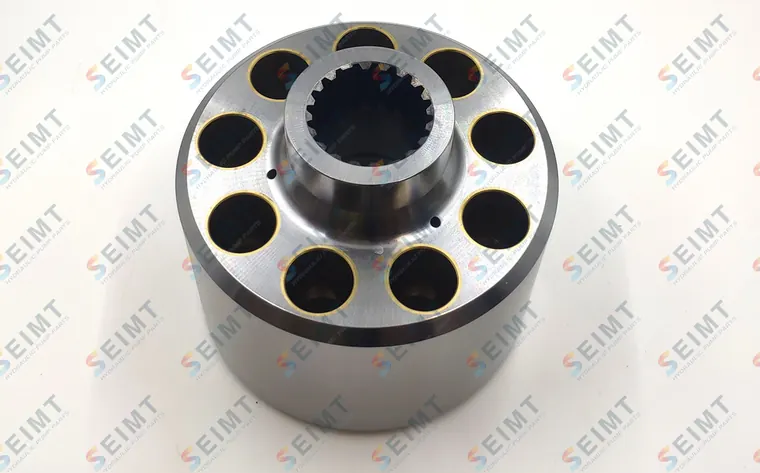
Cylinder blocks for axial and bent axis piston pumps with sintered bronze running faces bonded and machined after sintering then lapped flat.
Product Overview
The cylinder block carries the pistons and runs against the valve plate under full system pressure. It is the part that decides how long a rebuild lasts. Our blocks are machined from case hardening steel, the bronze running face is sintered and bonded then machined after sintering, and the face is lapped so it seals against the valve plate rather than merely touching it.
| Rexroth pattern frames | A2F A2FO A2FM A4V A4VSO A4VG A6V A6VM A7V A7VO A8VO A10VO A10VG A11VO A11VG |
|---|---|
| Other patterns | Sauer pattern and Uchida pattern blocks on request |
Key Benefits
- Bronze face bonded and machined after sintering so it does not lift in service
- Face lapped flat, which is what keeps case drain flow low
- Bore spacing and spline made to the original drawing, not copied from a worn sample
- Supplied singly or matched with pistons and a valve plate as a set
Application Scenarios
- Rebuild of excavator and loader main pumps
- Industrial power unit overhaul
- Winch and drum motor repair
- Exchange unit programmes in rebuild shops
Who It Is For
- Pump rebuild specialists
- Distributors supplying rebuild shops
- Plant maintenance workshops
- Machine builders running an exchange programme
Problems It Solves
- The old block face is scored and cannot be reclaimed by lapping
- The bronze face on the previous replacement lifted after a short time in service
- Case drain flow is high and the pump will not hold pressure
- A single block is needed rather than a whole rotary group
Technical Features
- Case hardening steel body, carburised and hardened
- Sintered bronze running face bonded to the steel
- Face machined after sintering then lapped
- Piston bores honed to size and checked for clearance
- Spline ground and checked over pins
Specifications
Performance figures depend on the exact variant, so we confirm them against your model code rather than publishing a number that may not apply to your pump.
| Body material | Case hardening steel, carburised and hardened |
|---|---|
| Running face | Sintered bronze, bonded and machined after sintering |
| Face finish | Lapped |
| Bores | Honed and gauged for piston clearance |
| Spline | Ground and checked over pins |
| Supply | Single part or matched with pistons and valve plate |
Materials
| Cylinder blocks | Case hardening steel with a sintered bronze running face, bonded and machined after sintering |
|---|---|
| Pistons and shoes | Case hardening steel with a bronze shoe face, swaged and hydrostatically balanced |
| Valve plates | Bearing steel or bronze faced steel depending on the frame, lapped to a mirror finish |
| Drive shafts | Alloy steel, carburised and hardened on the spline and bearing seats, ground on centres |
| Vanes and rotors | High speed tool steel and case hardening steel, hardened and ground on all working faces |
| Cam rings | Bearing quality alloy steel, through hardened then profile ground |
| Seals | Nitrile as standard, fluorocarbon or polyurethane on request for hot or fire resistant fluid duty |
Manufacturing Process
- Turning and millingBlanks are turned and milled from certified bar and forging stock on CNC machines.
- Heat treatmentCarburising, quenching, tempering or nitriding to the route the original part uses.
- GrindingBores, spline seats and running faces are ground after heat treatment so distortion is removed.
- Lapping and superfinishingValve plates, shoe faces and block faces are lapped so the pair seals under pressure.
- InspectionDimensions, hardness and surface finish are recorded against the drawing on a sampling plan.
- Assembly and testComplete pumps are built, run in and tested for efficiency, leakage and noise before packing.
Quality Control
- Incoming material certificates are checked against the grade called for on the drawing.
- Hardness is measured after heat treatment on every batch and recorded on the batch card.
- Critical bores and running faces are gauged against the drawing tolerance, not against a sample part.
- Mating parts are matched as a set so the block, shoes and valve plate run in together.
- Rebuilt pumps are bench tested for volumetric efficiency, external leakage and sound level.
- Parts are cleaned, oiled and vacuum sealed so they arrive without surface rust.
Certifications and Documentation
Supplied on request with an order. We do not claim approvals we cannot evidence.
| Material certificate | Mill certificate for the steel grade used in the batch |
|---|---|
| Hardness report | Surface and core hardness readings after heat treatment |
| Dimensional report | Measured values for the critical features named on the drawing |
| Test bench report | Flow, efficiency, leakage and sound readings for a rebuilt pump |
| Packing list and photographs | Carton contents and photographs of the packed goods before shipment |
Customization Options
- Shaft and splineKeyed, straight or splined shaft ends built to your sample or drawing.
- Port and mountingFlange, thread and mounting pattern matched to the pump already on the machine.
- Seal materialNitrile, fluorocarbon or polyurethane for hot oil, fire resistant fluid or low temperature duty.
- Rotation and displacementLeft or right hand rotation and the displacement code your circuit was set up for.
- Marking and packingNeutral packing, your own carton artwork and your own part number laser marked on the part.
Comparison With Other Products
| Point | New Cylinder Block | Relapping the Old Block | Complete Rotary Group |
|---|---|---|---|
| Cost | Middle | Lowest | Highest |
| When it works | Face scored or bronze worn through | Light marking only | Block, shoes and plate all worn |
| Result | As new running face | Buys some time | As new running set |
| Risk | Low if pistons are also checked | Face may not clean up | Lowest |
Use Guide
- Measure the piston to bore clearance before deciding to reuse the pistons.
- Inspect the valve plate. A worn plate will mark a new block within hours.
- Clean the spline and check it against the shaft before assembly.
- Assemble with clean oil and never dry.
- Run in at low pressure before applying full load.
Product Photographs
Related Products
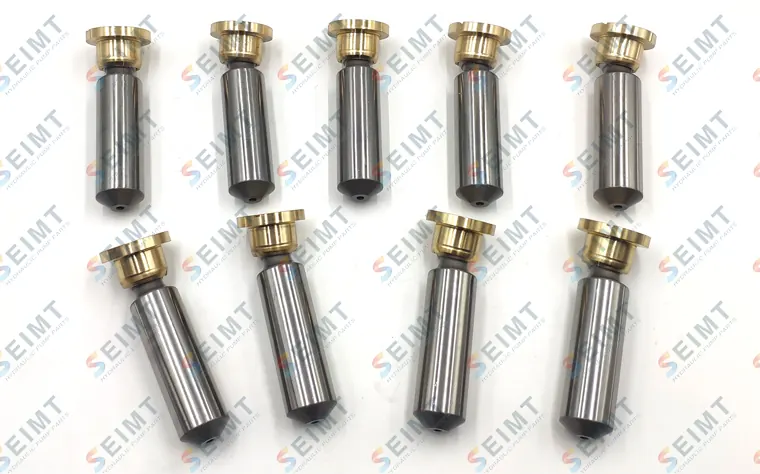
Piston and Shoe Assemblies
Piston and shoe assemblies for axial piston pumps, swaged and checked for shoe clearance with hydrostatically balanced bronze shoe faces.
View Series and Sizes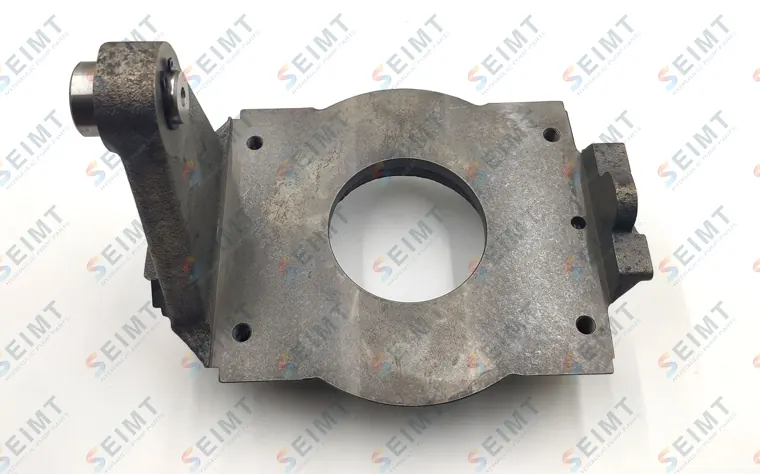
Valve Plates and Swash Plates
Valve plates swash plates cradles retainer plates and ball guides for axial and bent axis piston pumps lapped and ground to the original drawing.
View Series and Sizes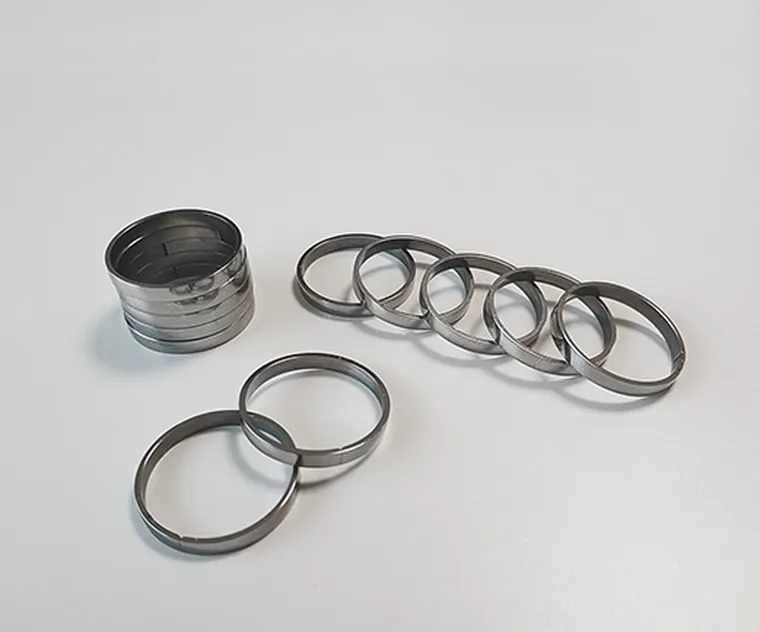
Hydraulic Piston Rings
Piston rings for A2F A2FO A2FM A6V A6VM A7V A7VO and A8VO bent axis pumps and motors, ground and gap checked by size group.
View Series and Sizes
Related Industry Applications
Construction Machinery
See the ApplicationMining and Quarry
See the ApplicationMarine and Offshore
See the Application
Related Project Cases
Excavator Travel Motor Rebuild Programme in Turkey
Read the CaseStocking Cartridge Kit Programme for a German Distributor
Read the CaseMarine Winch Pump Refit for a Canadian Repair Yard
Read the Case
Related Articles
Frequently Asked Questions
Can I fit a new block and keep the old pistons?
Why does the bronze face matter so much?
Do you machine blocks for Sauer pattern pumps?
Is the block supplied with the spring and pins?
How is the block packed?
Send Us the Model Code and We Will Quote
Tell us the model code stamped on the pump, the quantity and your delivery port. A quotation with lead time usually comes back within one working day.