Tension Control Modes For Non Woven Converting Explained
Magnetic powder, lateral, conveyor belt and servo tension control: what each one does, and which non woven materials suit which mode.
Why Tension Decides Roll And Fold Quality
Every fault operators blame on the material, telescoping rolls, folded sizes that drift, edges that wander, traces back to tension. Web tension has to stay constant while roll diameter changes by a factor of three during a run, which is why the control method matters more than the motor size.
Magnetic Powder Tension Control
A magnetic powder brake or clutch gives smooth, adjustable resistance and holds tension steadily as diameter changes. It is our standard choice on wide folding and bed cover lines, where dimensional accuracy of the folded product depends on the web arriving at the folder under constant tension.
Medical Bed Cover Folding Machine (AQ-B(2400))
Lateral And Conveyor Belt Control
Lateral tension control manages the web across its width rather than along its length, which matters on wide material that tends to bag in the middle. Conveyor belt control carries light material without pulling it, and is used where a web is too weak to be drawn through by tension alone.
Servo Tension Control
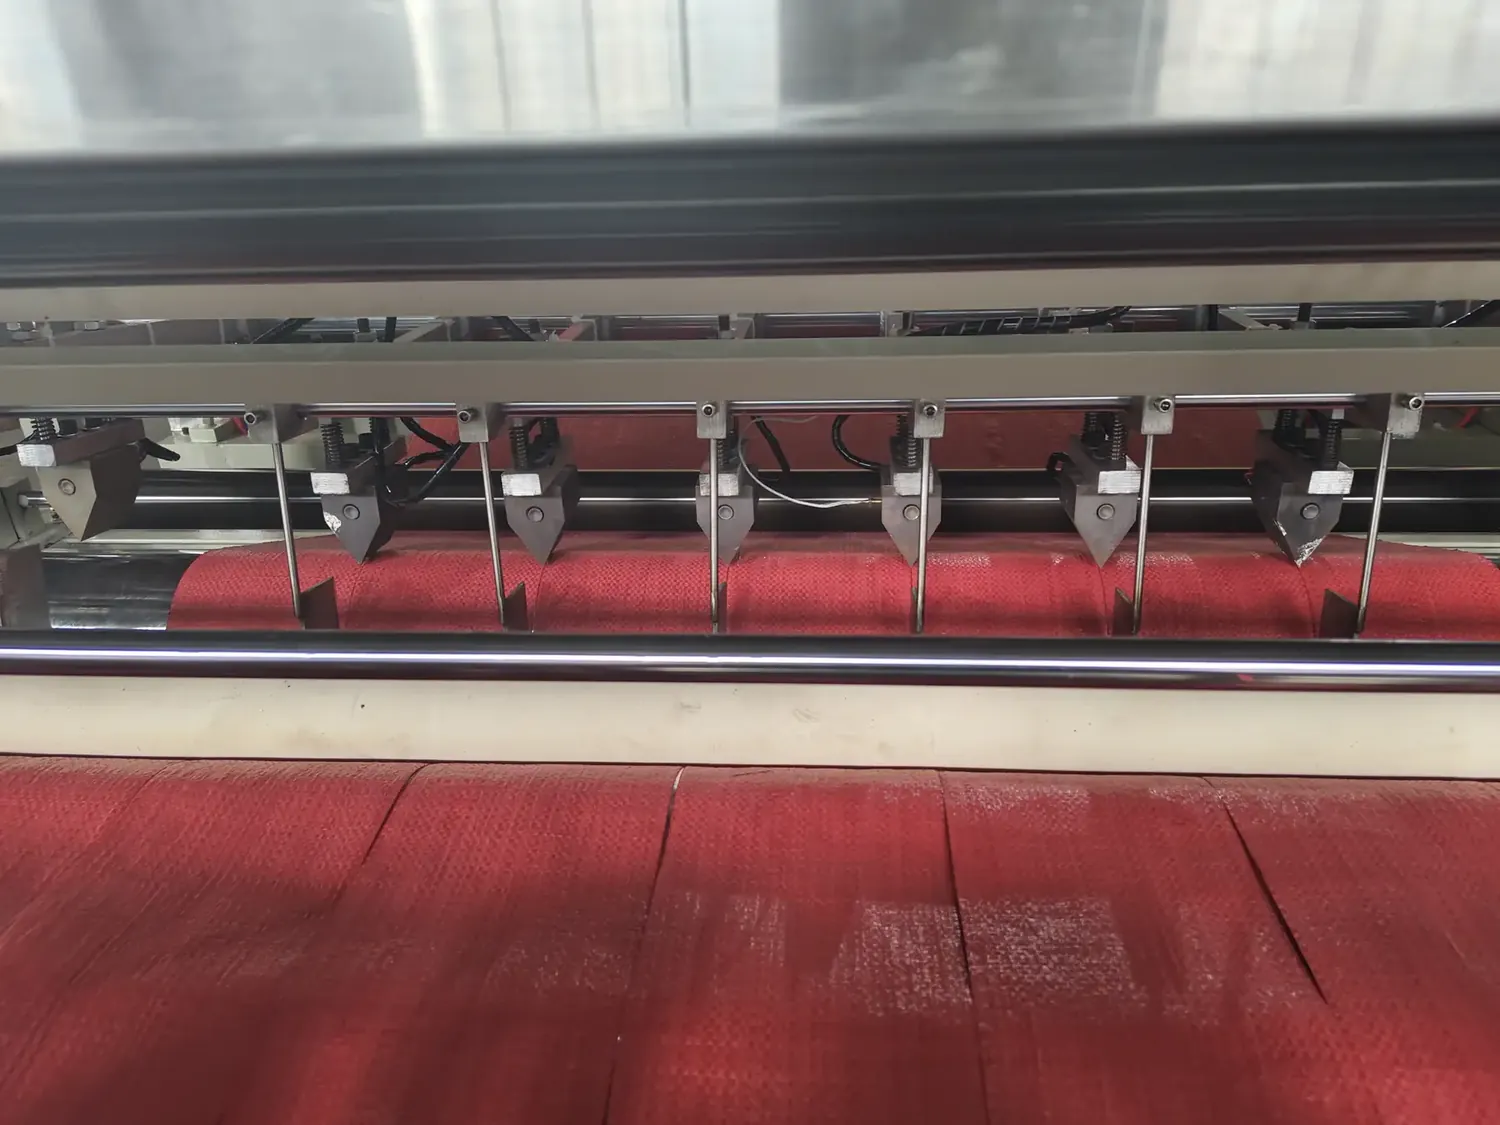
Servo control closes the loop electronically and reacts fastest to changes in speed and diameter. It is the right choice when the line starts and stops often, or when several operations run in registration, as on our AQ-R(3500) which embosses, scores, counts, slits and rewinds together.
Large Non Woven Rewinding Machine (AQ-R(3500))
One Machine With Four Modes
Converters who run PP woven, spunlace, needle punched and paper on the same floor should look at the AQ-R (1200-3500), which offers all four modes on one frame. Selecting the mode for the material avoids the compromise setting that spoils half your production.
Machine Families In This Guide
Machines Mentioned Here
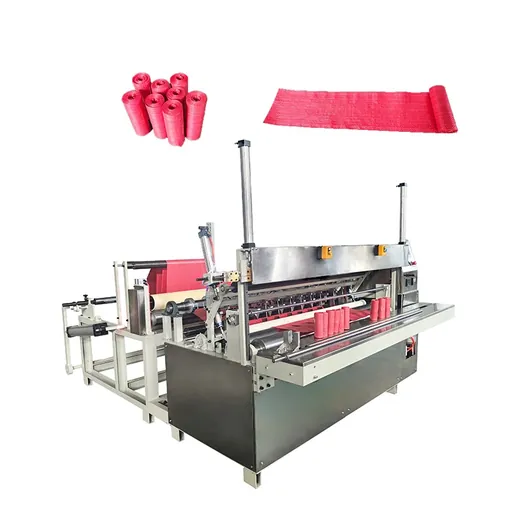
Woven Fabrics Slitting And Rewinding Machine
PP Woven And Non Woven Slitting With Four Selectable Tension Modes
Model AQ-R (1200-3500)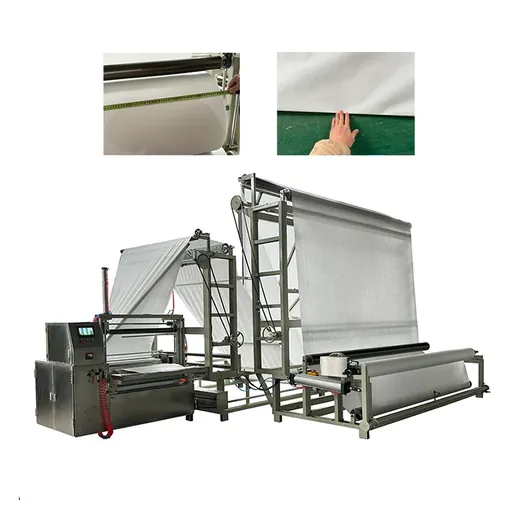
Non Woven Folding And Rewinding Machine
Fold Wide Non Woven Twice Then Rewind To Set Length At 90 M Per Minute
Model AQ-R(3200)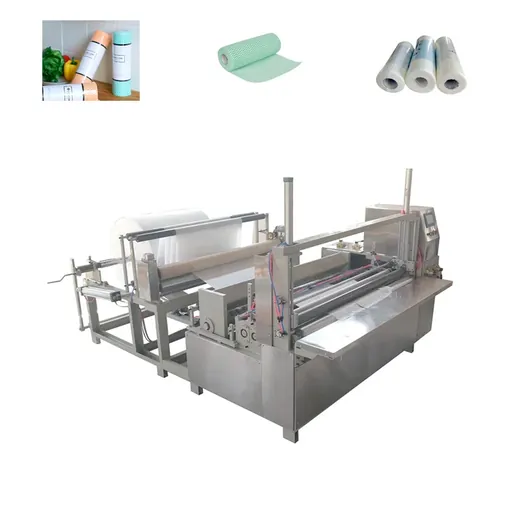
Non Woven Rewinding Machine
Servo Rewinding With Embossing Scoring Counting And Slitting
Model AQ-R(1800)Continue Reading
How To Choose A Non Woven Slitting And Rewinding Machine
Five questions that decide which rewinder you should buy: jumbo roll width, finished roll format, material fam...
Ultrasonic Bonding Versus Sewing For Disposable Non Woven Products
Why disposable bed covers, dust bags, filters and glove liners moved from thread to ultrasonic welding, and wh...
How To Specify A Disposable Bed Sheet Line
Working width, fold pattern, ultrasonic forming and counted stacking: the four decisions that set the cost and...
Questions On This Topic
Which mode is best for spunlace?
Spunlace is soft and low strength, so magnetic powder or servo control with a light setting usually gives the best result. We set and record the value against your fabric during run-off.
Can tension settings be saved?
On PLC controlled machines settings are stored as recipes. On frequency conversion machines we supply the recorded values from factory run-off so operators can repeat them.
Does tension affect perforation quality?
Yes. Perforation that tears early or not at all is usually a tension problem rather than a tooling problem.
Apply This To Your Own Line
Send your product and material details and we will tell you which machine and settings fit, with the specification in writing.