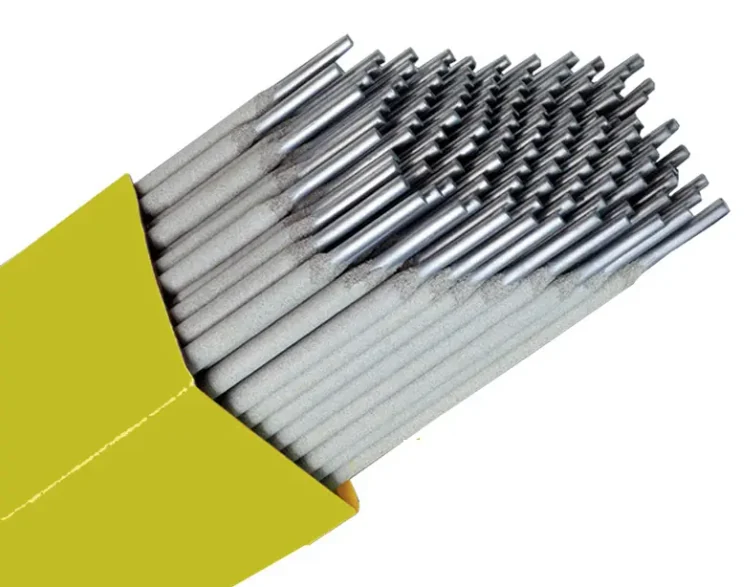
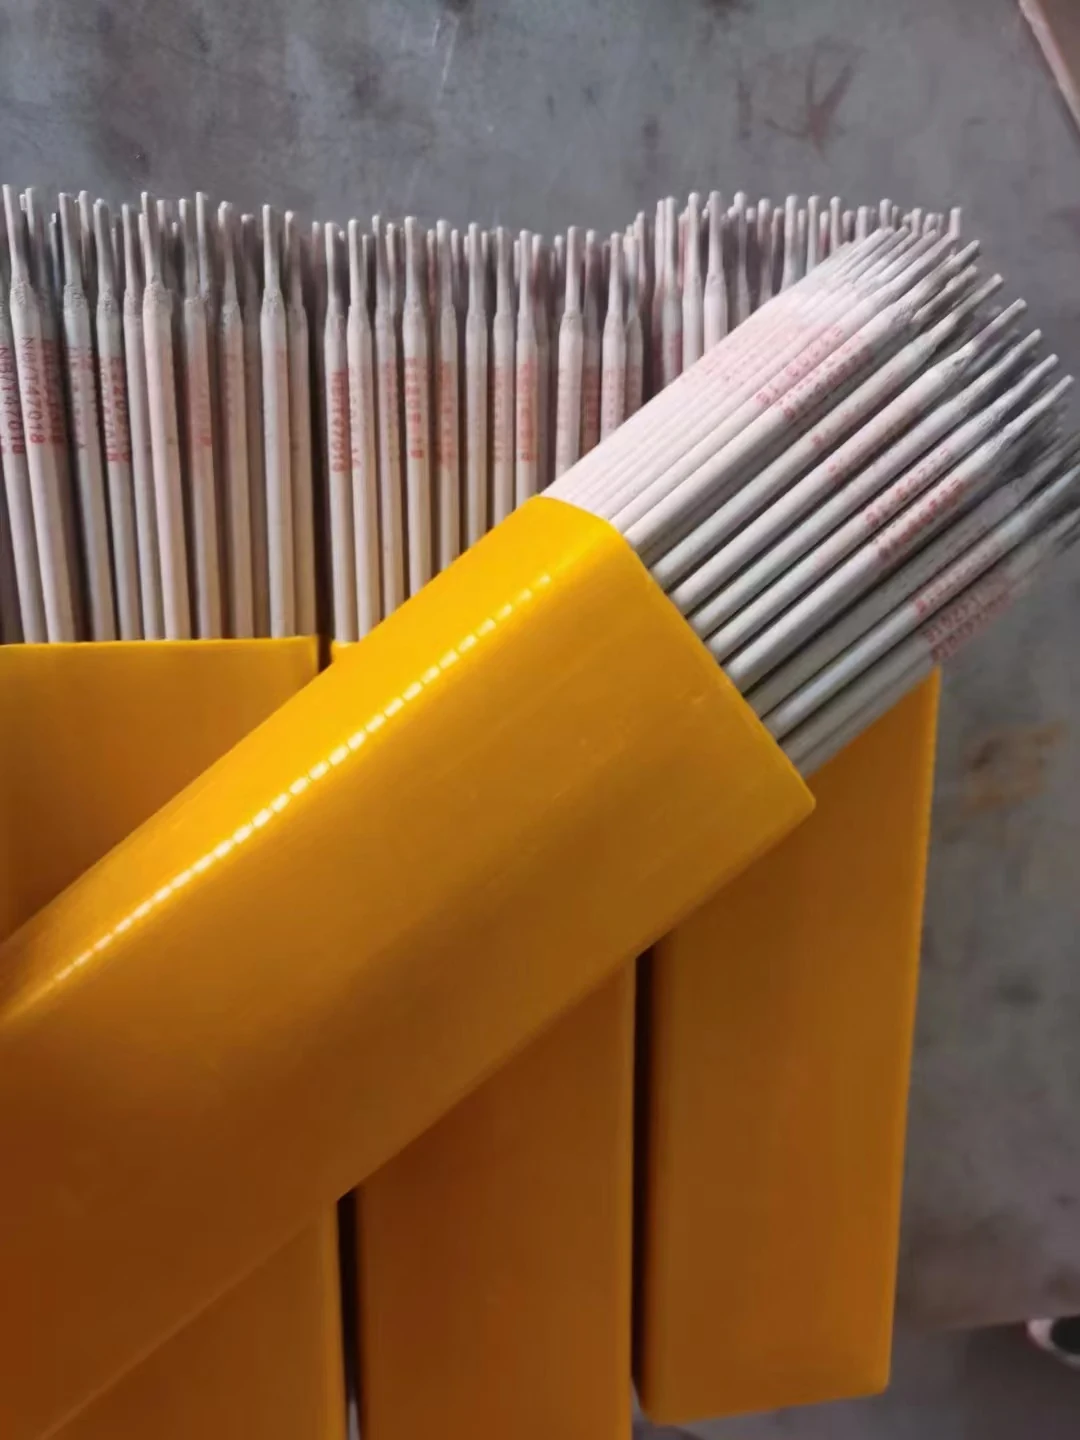
E7018 Stick Electrode 3/32″ 1/8″ 3/16″ Welding rod
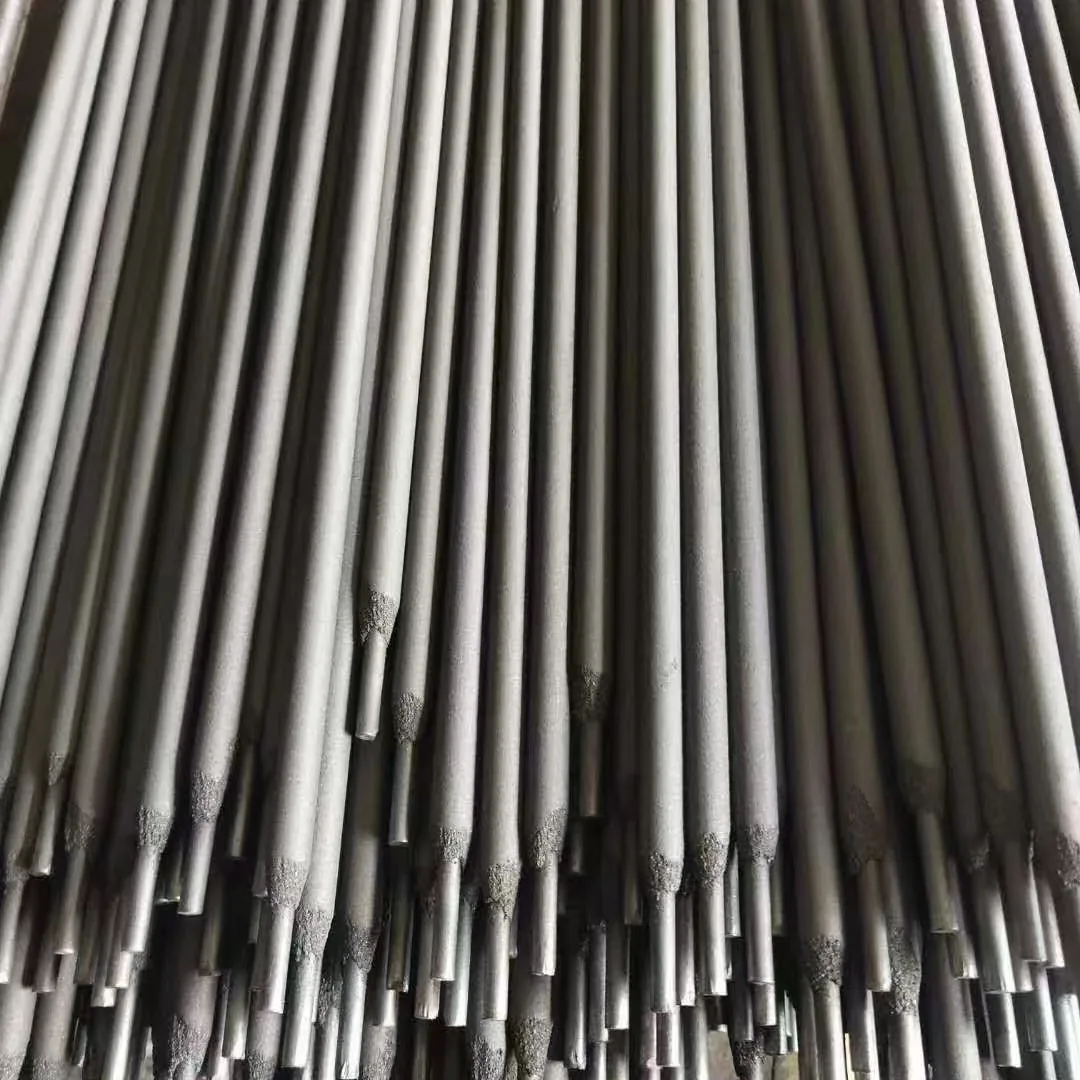
E7018 low hydrogen iron powder stick electrodes for carbon steel, all-position welding on AC or DC.
What this product does
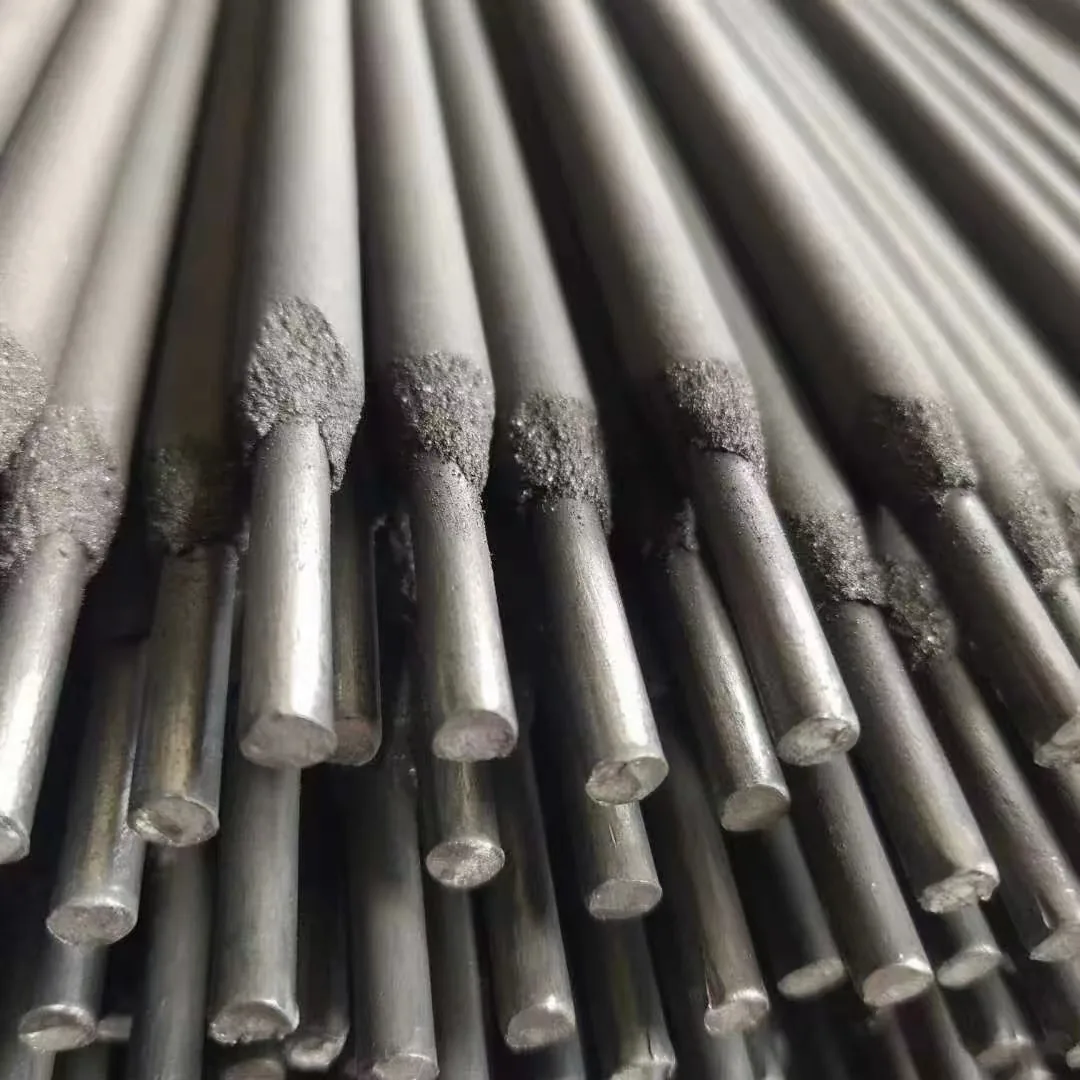
E7018 is a carbon steel electrode with an iron powder, low hydrogen potassium coating. The iron powder in the coating raises deposition so fewer passes fill the joint, and the low hydrogen character is what keeps hydrogen cracking out of restrained welds in hull structure. It runs on both AC and DC and is capable of all-position welding. Supplied in 3/32 inch, 1/8 inch and 3/16 inch plus 2mm, 3.2mm and 4mm.
Selection notes
- Low hydrogen potassium coating for restrained structural welds
- Iron powder coating raises deposition rate and reduces the number of passes
- AC or DC, all-position; 3/32 to 3/16 inch and 0.8mm to 4mm diameters
Specification
| Certificate | ABS, BV, LR, RINA, DNV, CCS, etc... |
|---|---|
| Package | Standard Exporting Wooden Box Packing, easy for forklift to transport. |
| Accessories | All neccessory Accessories of ELectric System like control Box |
| Category | Ship Outfittings |
| Warranty | One year, with installation instructions and spare parts support afterwards |
| Lead time | Confirmed per order with the quotation |
Published technical data
Reproduced from the manufacturer's own product data for this item. Figures are confirmed against your order before production.
Ordering and documentation
Name the classification society with your enquiry and the certificate is applied for at the same time as production. Every unit is tested before dispatch and the test report and video can be supplied before shipment. Warranty is one year, with installation instructions and spare parts support afterwards.
Related ship outfittings
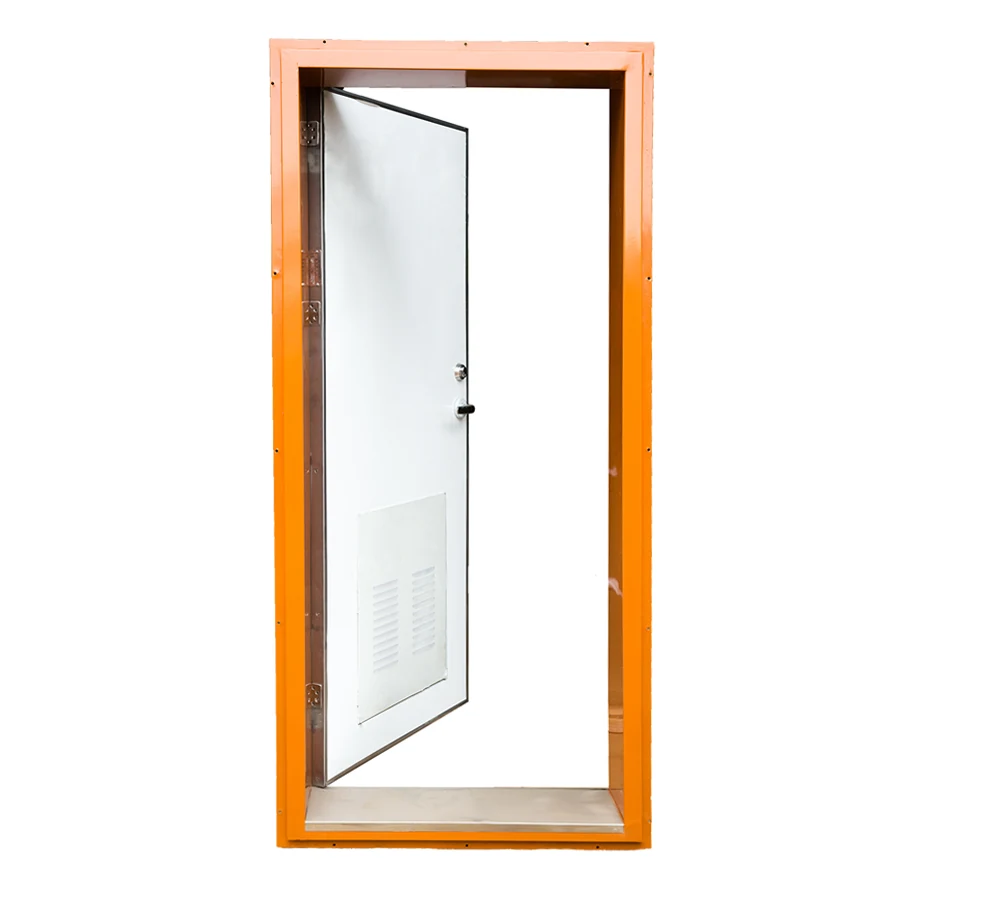
A60 fire proof door A30/B0/B15/C Marine fire rated door on Ship/Vessel
View specification →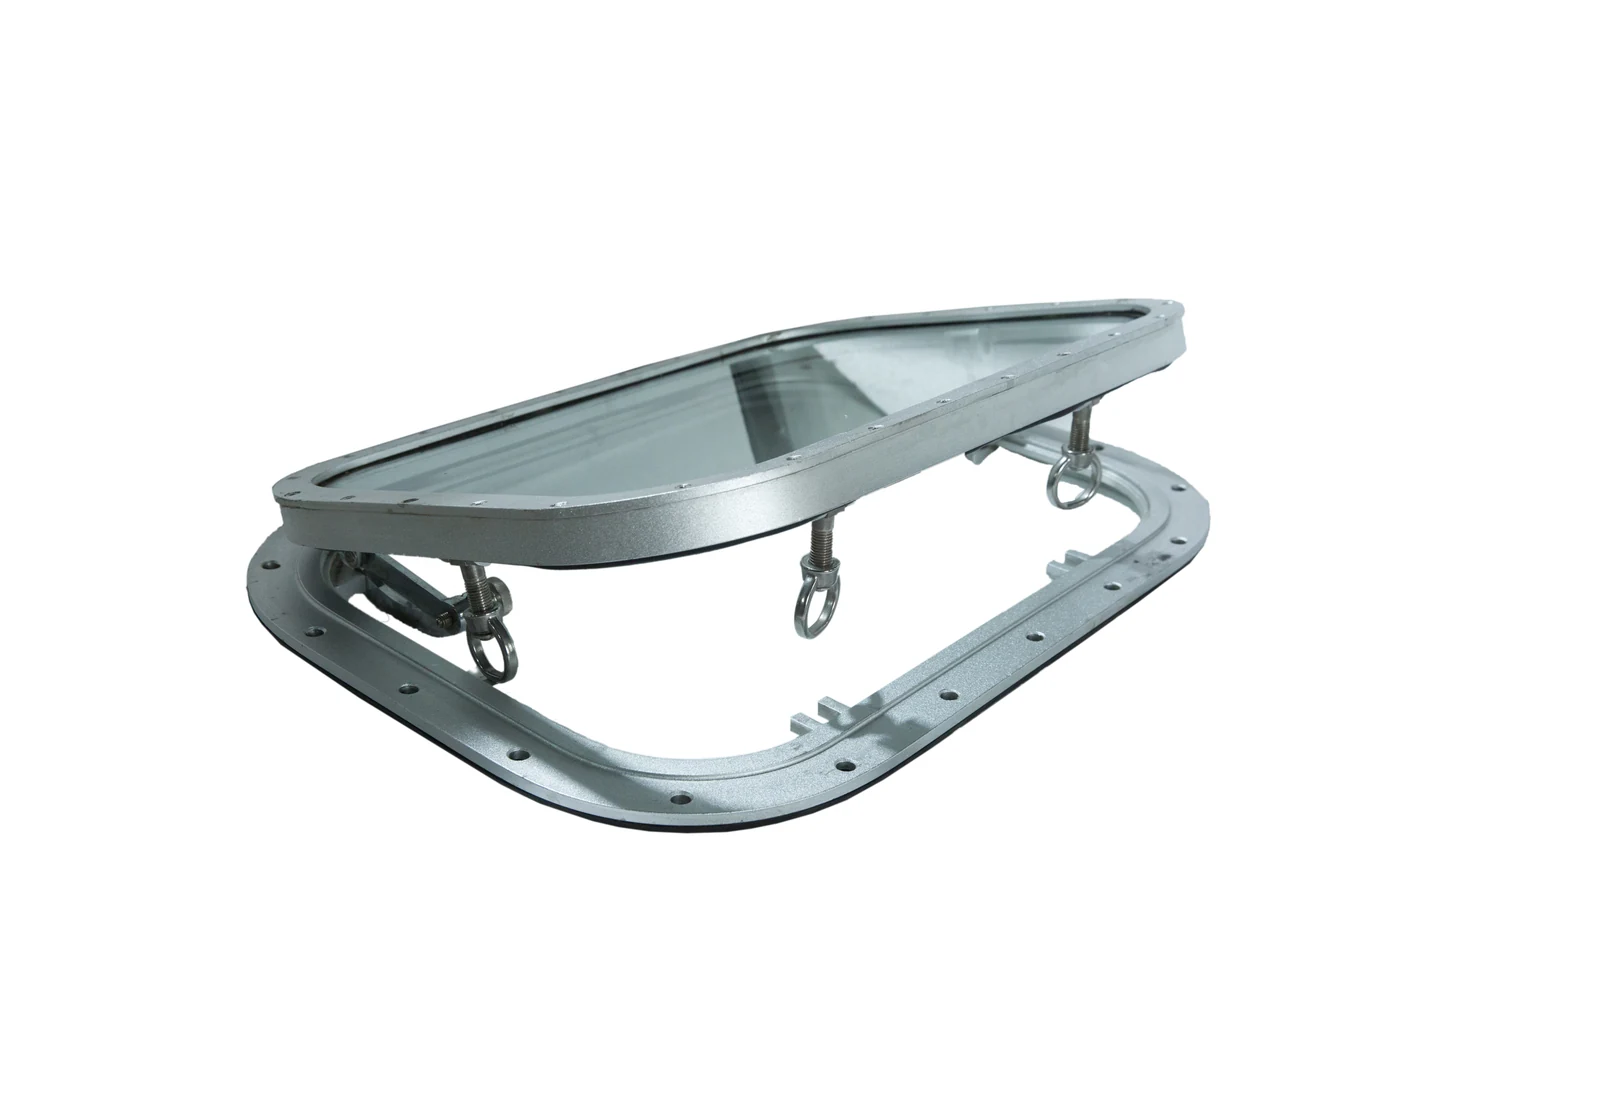
Marine Window Opening Type Aluminum Rectangular window Ship Window for boat (Type 2)
View specification →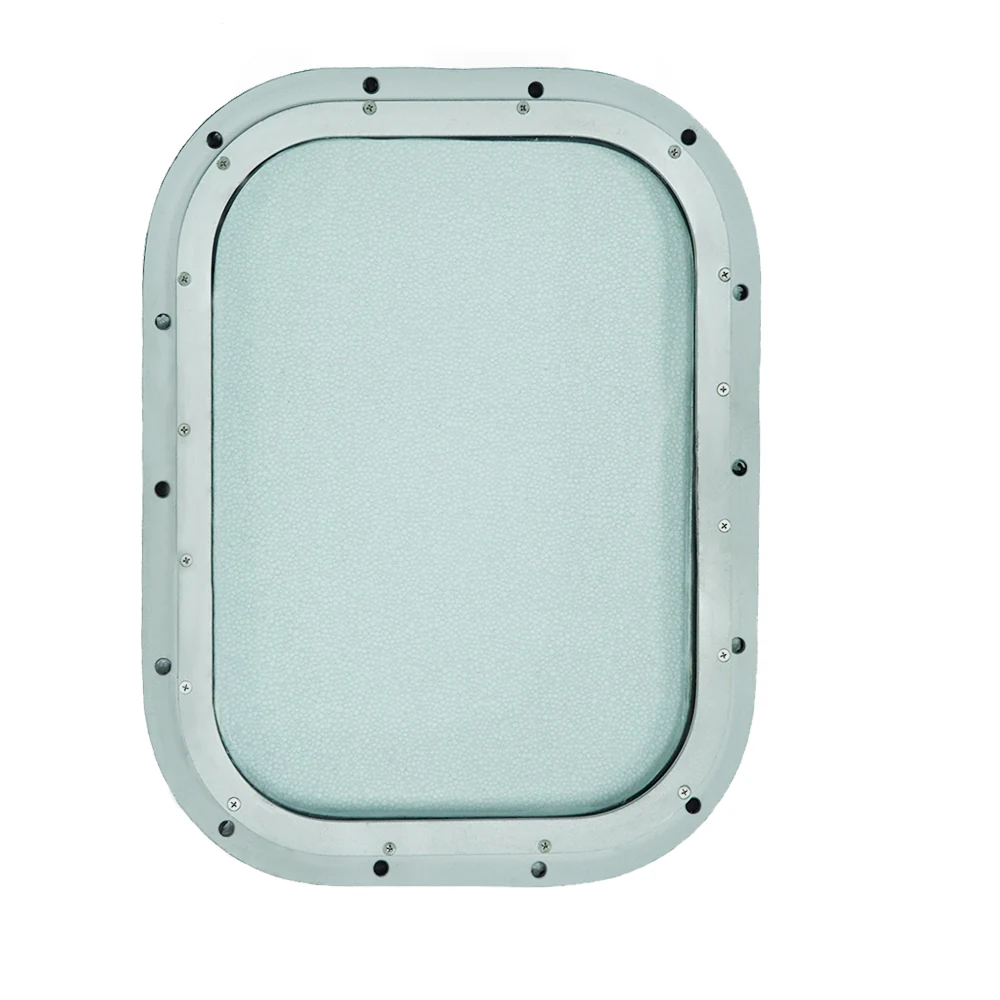
Marine fixed window Aluminum Ship Window Boat fixed window sliding window
View specification →
Ship Side Scuttles φ250,φ300, φ350 Marine Aluminum Portholes/Side scuttles in ship
View specification →Send the vessel data, get a specified quotation
Tell us the vessel, the duty and the classification society. We come back with the specification, the certificate list and the packing method — not just a price.