Tungsten Carbide Rods And Rotary Tool Blanks
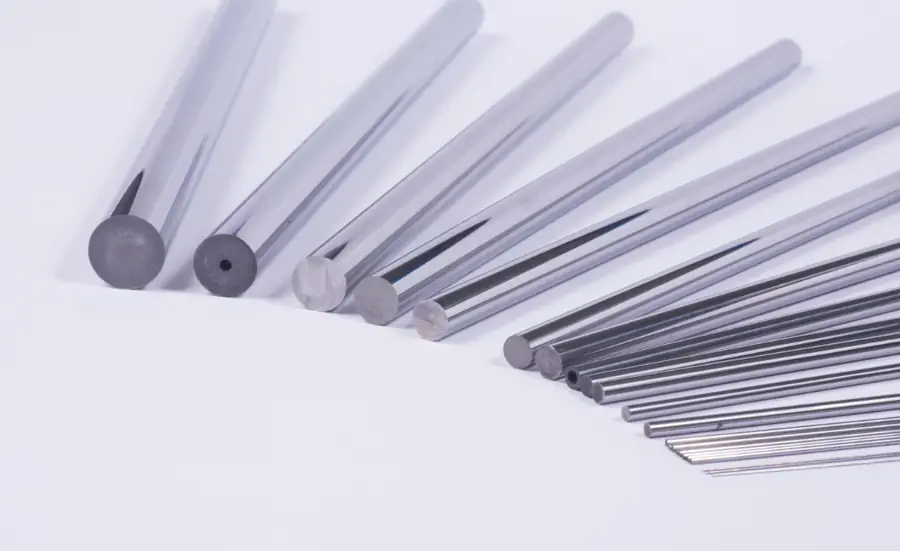
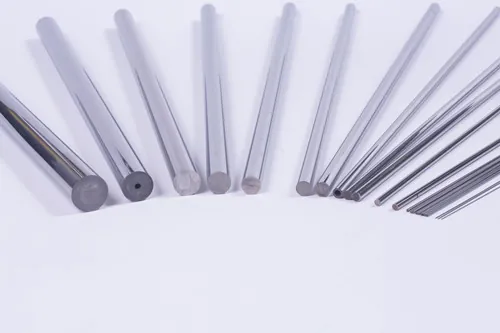
Rotary tool blanks are the raw material for solid carbide cutting tools, so they have to be accurate and consistent rod after rod. GWM supplies precision ground blanks, open tolerance blanks, coolant channel rods and long rods from 0.5 to 41 mm.
Product Overview
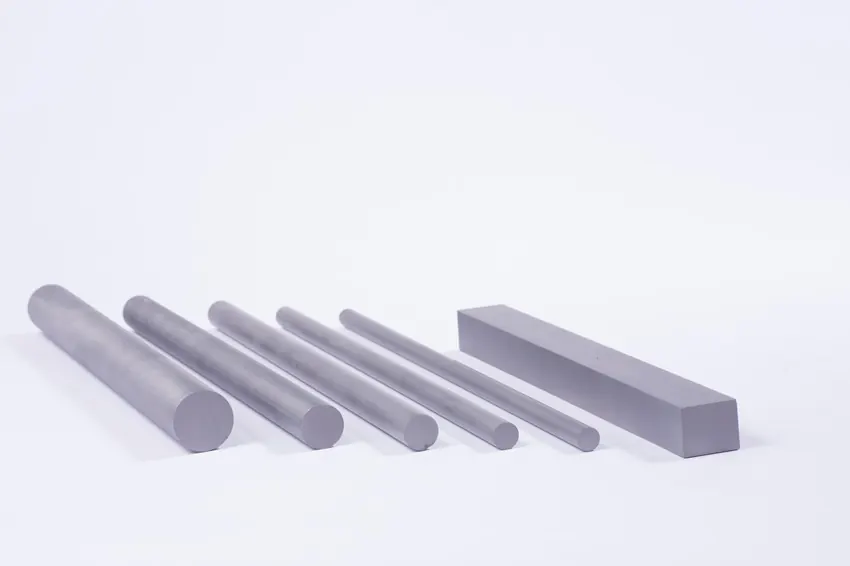
Rotary tool blanks normally take the shape of long cylinders. They are the raw material for precision cutting tools, which is why they need to be highly accurate and consistent. GWM rotary tool blank offering includes precision ground blanks, open tolerance blanks, coolant channel rods and long rods.
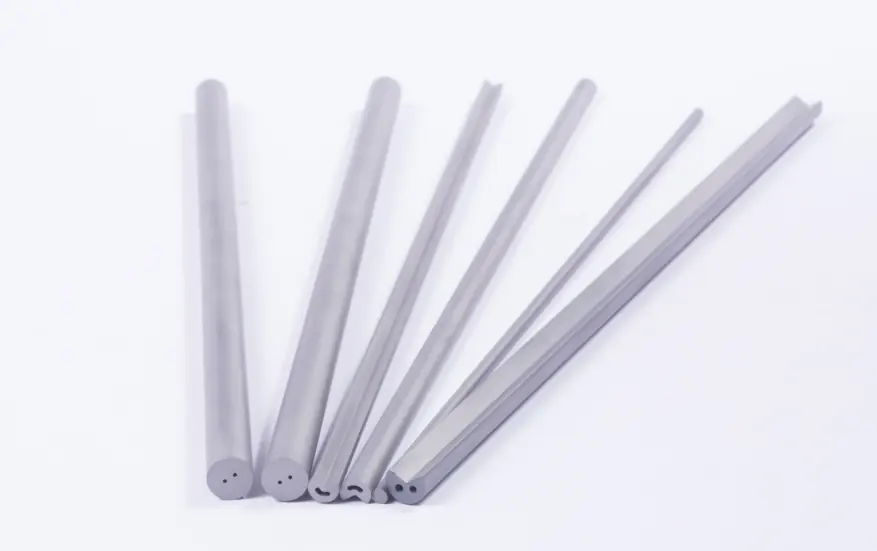
Three families are available: solid blanks, coolant blanks and bio-medical blanks. Coolant channel rods are offered in single, twin, straight and helix hole options. End mill blanks are supplied with a chamfer, ground to fine tolerance with a polished finish in fixed lengths.
Key Benefits
Consistent From Rod To Rod
Grain size, binder content and density are held to one grade specification so tool grinders get repeatable results.
Coolant Right To The Cutting Edge
Central, twin straight and helical channels carry high pressure coolant to the tip, which clears chips and holds temperature down.
Ground Or As Sintered
Take the rod ground to H6 for direct fluting, or take it as sintered with grinding stock when you finish in house.
Application Scenarios
Rod blanks leave our plant as the starting stock for these tools.
Solid Carbide End Mills
Blanks with a chamfer, polished finish and fixed length, ready for flute grinding.
Drills And Reamers
Coolant channel rods in single, twin, straight and helical configurations for deep hole and high feed drilling.
Bio-Medical Tools
Open tolerance ground long rods for the bio-medical tool market.
PCB Micro Tools
Small diameter ultra fine grain rods in GW10U for PCB bits and reamers.
Woodworking Cutters
Ultra fine grain rods in GW03U and GW05U for wood and bamboo cutters.
Wear Parts And Punches
Larger diameters cut to length for punches, guides and wear-resistant components.
Who It Is For
- Cutting tool factories that grind their own end mills, drills and reamers.
- Tool regrinding and OEM tooling shops that need blanks in small repeat batches.
- Distributors supplying carbide blanks to regional tool makers.
- Machine builders that need long rods cut into wear parts, punches or guides.
Problems It Solves
- Diameter drifting between batches, which forces the grinder to re-set for every delivery.
- Coolant holes that wander off centre and break through the flute during grinding.
- Rods that arrive with too much grinding stock and waste wheel life and machine hours.
- Long lead times on odd diameters that are not held in stock anywhere locally.
Technical Features
- Solid rods listed from Ø0.5 mm to Ø41 mm, in 310 mm and 330 mm lengths.
- Diameter tolerance tightens with size, from +0.50/+0.25 mm on small rods to +0.75/+0.35 mm on large.
- Ground rods finished to H6.
- Central coolant hole rods from Ø3 to Ø30 mm, hole diameters 0.5 to 3.0 mm.
- Two straight coolant hole rods from Ø6 to Ø26 mm, bore circle 1.5 to 7.5 mm.
- Two helical coolant holes at 30 degrees available on request.
- Eccentricity of the coolant hole controlled and published for every diameter.
- Cobalt and nickel binder grades, ultra fine to medium grain.
Specifications
| Part no. | Diameter mm | Diameter tol. mm | Length mm | Length tol. mm |
|---|---|---|---|---|
| RCT0L | 0.5 | +0.50/+0.25 | 310/330 | +5.0/+0 |
| RC01L | 1.0 | +0.50/+0.25 | 310/330 | +5.0/+0 |
| RCT1L | 1.5 | +0.50/+0.25 | 310/330 | +5.0/+0 |
| RC02L | 2.0 | +0.50/+0.25 | 310/330 | +5.0/+0 |
| RCT2L | 2.5 | +0.50/+0.25 | 310/330 | +5.0/+0 |
| RC03L | 3.0 | +0.50/+0.25 | 310/330 | +5.0/+0 |
| RCT3L | 3.5 | +0.50/+0.25 | 310/330 | +5.0/+0 |
| RC04L | 4.0 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RCT4L | 4.5 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RC05L | 5.0 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RCT5L | 5.5 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RC06L | 6.0 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RCT6L | 6.5 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RC07L | 7.0 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RCT7L | 7.5 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RC08L | 8.0 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RCT8L | 8.5 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RC09L | 9.0 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RCT9L | 9.5 | +0.60/+0.25 | 310/330 | +5.0/+0 |
| RC10L | 10.0 | +0.70/+0.30 | 310/330 | +5.0/+0 |
| RCT10L | 10.5 | +0.70/+0.30 | 310/330 | +5.0/+0 |
| RC11L | 11.0 | +0.70/+0.30 | 310/330 | +5.0/+0 |
| RCT11L | 11.5 | +0.70/+0.30 | 310/330 | +5.0/+0 |
| RC12L | 12.0 | +0.70/+0.35 | 310/330 | +5.0/+0 |
| RCT12L | 12.5 | +0.70/+0.35 | 310/330 | +5.0/+0 |
| RC13L | 13.0 | +0.70/+0.35 | 310/330 | +5.0/+0 |
| RCT13L | 13.5 | +0.70/+0.35 | 310/330 | +5.0/+0 |
| RC14L | 14.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RCT14L | 14.5 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC15L | 15.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RCT15L | 15.5 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC16L | 16.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RCT16L | 16.5 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC17L | 17.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC18L | 18.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC19L | 19.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC20L | 20.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC21L | 21.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC22L | 22.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC23L | 23.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC24L | 24.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC25L | 25.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC26L | 26.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC27L | 27.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC28L | 28.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC29L | 29.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC30L | 30.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC31L | 31.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC32L | 32.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC33L | 33.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC34L | 34.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC35L | 35.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC36L | 36.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC37L | 37.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC38L | 38.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC39L | 39.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC40L | 40.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| RC41L | 41.0 | +0.75/+0.35 | 310/330 | +5.0/+0 |
| Part no. | Diameter mm | Unground tol. mm | Ground tol. | Length mm | Hole dia. mm | Hole tol. mm | Eccentricity mm |
|---|---|---|---|---|---|---|---|
| GC1030330050 | 3.0 | +0.30/+0.50 | H6 | 330 (+5.0/+0) | 0.5 | ±0.1 | 0.10 |
| GC1040330080 | 4.0 | +0.30/+0.50 | H6 | 330 (+5.0/+0) | 0.8 | ±0.1 | 0.10 |
| GC1050330080 | 5.0 | +0.30/+0.50 | H6 | 330 (+5.0/+0) | 0.8 | ±0.1 | 0.13 |
| GC1060330100 | 6.0 | +0.30/+0.50 | H6 | 330 (+5.0/+0) | 1.0 | ±0.15 | 0.15 |
| GC1070330100 | 7.0 | +0.30/+0.60 | H6 | 330 (+5.0/+0) | 1.0 | ±0.15 | 0.15 |
| GC1080330100 | 8.0 | +0.30/+0.60 | H6 | 330 (+5.0/+0) | 1.0 | ±0.15 | 0.15 |
| GC1090330140 | 9.0 | +0.30/+0.60 | H6 | 330 (+5.0/+0) | 1.4 | ±0.15 | 0.20 |
| GC1100330140 | 10.0 | +0.30/+0.60 | H6 | 330 (+5.0/+0) | 1.4 | ±0.15 | 0.20 |
| GC1110330140 | 11.0 | +0.30/+0.60 | H6 | 330 (+5.0/+0) | 1.4 | ±0.15 | 0.28 |
| GC1120330175 | 12.0 | +0.30/+0.60 | H6 | 330 (+5.0/+0) | 1.4 | ±0.15 | 0.30 |
| GC1130330175 | 13.0 | +0.30/+0.70 | H6 | 330 (+5.0/+0) | 1.8 | ±0.15 | 0.34 |
| GC1140330175 | 14.0 | +0.30/+0.70 | H6 | 330 (+5.0/+0) | 1.8 | ±0.15 | 0.37 |
| GC1150330200 | 15.0 | +0.30/+0.70 | H6 | 330 (+5.0/+0) | 1.8 | ±0.20 | 0.40 |
| GC1160330200 | 16.0 | +0.30/+0.70 | H6 | 330 (+5.0/+0) | 2.0 | ±0.20 | 0.40 |
| GC1170330200 | 17.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 2.0 | ±0.20 | 0.47 |
| GC1180330200 | 18.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 2.0 | ±0.20 | 0.50 |
| GC1190330200 | 19.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 2.0 | ±0.20 | 0.50 |
| GC1200330250 | 20.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 2.0 | ±0.25 | 0.50 |
| GC1210330250 | 21.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 2.5 | ±0.25 | 0.50 |
| GC1220330250 | 22.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 2.5 | ±0.25 | 0.50 |
| GC1230330250 | 23.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 2.5 | ±0.25 | 0.50 |
| GC1240330300 | 24.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 2.5 | ±0.25 | 0.50 |
| GC1250330300 | 25.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 3.0 | ±0.25 | 0.50 |
| GC1260330300 | 26.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 3.0 | ±0.25 | 0.50 |
| GC1270330300 | 27.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 3.0 | ±0.25 | 0.50 |
| GC1280330300 | 28.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 3.0 | ±0.25 | 0.50 |
| GC1290330300 | 29.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 3.0 | ±0.25 | 0.50 |
| GC1300330300 | 30.0 | +0.30/+0.80 | H6 | 330 (+5.0/+0) | 3.0 | ±0.25 | 0.50 |
| Part no. | Diameter mm | Unground tol. mm | Ground tol. | Length mm | Hole dia. mm | Hole tol. mm | Bore circle TK mm | TK tol. mm | Eccentricity mm |
|---|---|---|---|---|---|---|---|---|---|
| GCS1060330080015 | 6 | +0.30/+0.50 | H6 | 330 | 0.8 | ±0.1 | 1.5 | (+0/−0.2) | 0.15 |
| GCS1070330080015 | 7 | +0.30/+0.60 | H6 | 330 | 0.8 | ±0.1 | 1.5 | (+0/−0.2) | 0.15 |
| GCS1080330100015 | 8 | +0.30/+0.60 | H6 | 330 | 1 | ±0.15 | 1.5 | (+0/−0.3) | 0.15 |
| GCS1090330100026 | 9 | +0.30/+0.60 | H6 | 330 | 1 | ±0.15 | 2.6 | (+0/−0.3) | 0.2 |
| GCS1100330100026 | 10 | +0.30/+0.60 | H6 | 330 | 1 | ±0.15 | 2.6 | (+0/−0.3) | 0.2 |
| GCS1110330120036 | 11 | +0.30/+0.60 | H6 | 330 | 1.2 | ±0.15 | 3.6 | (+0/−0.3) | 0.28 |
| GCS1120330120036 | 12 | +0.30/+0.60 | H6 | 330 | 1.2 | ±0.15 | 3.6 | (+0/−0.3) | 0.3 |
| GCS1130330120036 | 13 | +0.30/+0.70 | H6 | 330 | 1.2 | ±0.15 | 3.6 | (+0/−0.3) | 0.34 |
| GCS1140330150050 | 14 | +0.30/+0.70 | H6 | 330 | 1.5 | ±0.15 | 5 | (+0/−0.3) | 0.37 |
| GCS1150330150050 | 15 | +0.30/+0.70 | H6 | 330 | 1.5 | ±0.15 | 5 | (+0/−0.3) | 0.4 |
| GCS1160330150050 | 16 | +0.30/+0.70 | H6 | 330 | 1.5 | ±0.15 | 5 | (+0/−0.3) | 0.4 |
| GCS1170330200062 | 17 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 6.2 | (+0/−0.3) | 0.47 |
| GCS1180330200062 | 18 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 6.2 | (+0/−0.3) | 0.5 |
| GCS1190330200062 | 19 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 6.2 | (+0/−0.3) | 0.5 |
| GCS1200330200062 | 20 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 6.2 | (+0/−0.4) | 0.5 |
| GCS1210330200062 | 21 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 6.2 | (+0/−0.4) | 0.5 |
| GCS1220330200062 | 22 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 6.2 | (+0/−0.4) | 0.5 |
| GCS1230330200075 | 23 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 7.5 | (+0/−0.4) | 0.5 |
| GCS1240330200075 | 24 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 7.5 | (+0/−0.5) | 0.5 |
| GCS1250330200075 | 25 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 7.5 | (+0/−0.5) | 0.5 |
| GCS1260330200075 | 26 | +0.30/+0.80 | H6 | 330 | 2 | ±0.20 | 7.5 | (+0/−0.5) | 0.5 |
Part numbers, tolerances and eccentricity figures are taken from the GWM rod dimension sheets. Diameters, lengths and hole sizes outside these tables are made to order.
Materials
Every part is quoted against a grade from the GWM chart. Cobalt and nickel binder grades are both available.
Rods are pressed from the same grade family as the rest of our range. Ultra fine grain grades such as GW02U, GW03U and GW05U give the highest wear resistance for wood, bamboo and water jet work. Sub-fine grades GW10U, GW20U and GW30U cover PCB bits, drills and general milling. GW40U and GW45U carry more binder for end mills that have to survive hard steels and titanium.
Recommended starting grades for this product: GW02UGW03UGW05UGW10UGW20UGW30UGW40UGW45UYG6XYG10X
Manufacturing Process
- Step 01
Powder Blending
WC and binder powders are wet milled in ball mills to the grain size the grade calls for.
- Step 02
Forming
Extrusion, two-way pressing or oil pressing, depending on the section and the length of the part.
- Step 03
Sintering
Vacuum sintering and pressure sintering furnaces. Every order is sinter-HIPped.
- Step 04
Finishing
Blank CNC machining, centreless grinding and cryogenic treatment to the drawing.
Quality Control
- Incoming powder checked before milling so grain size and binder content match the grade.
- Density and hardness measured on sintered parts against the published grade values.
- Metallographic microscope used to check porosity and structure after sintering.
- Dimensions and tolerances verified against the drawing before packing.
Certifications
Chengdu Golden Wolfran Carbide is an ISO certificated enterprise. Copies of the current certificates are sent with the quotation on request, so ask us for the version that applies to your order.
Customization Options
We manufacture small and large scale carbide products to your drawing, supplied either as sintered or precision ground.
Diameters And Lengths To Drawing
Anything outside the published range is quoted from your drawing, including lengths beyond 330 mm.
Hole Configuration
Single, twin, straight or helix coolant channels, with the hole diameter and bore circle you specify.
Surface Condition
As sintered with grinding stock, ground to H6, or ground and polished with a chamfer.
Comparison With Other Products
| Rod type | Diameter range | Coolant supply | Typical finished tool |
|---|---|---|---|
| Solid rod | 0.5 to 41 mm | External coolant only | End mills, reamers, burrs, punches and wear parts |
| Central coolant hole | 3 to 30 mm | One axial channel, 0.5 to 3.0 mm | Single flute and gun style drills, deep hole reamers |
| Two straight coolant holes | 6 to 26 mm | Two channels on a 1.5 to 7.5 mm bore circle | Two flute solid carbide drills |
| Two helical coolant holes | Made to order | Two channels twisted at 30 degrees | Twist drills where the channel has to follow the flute |
Use Guide
Choosing The Rod
Start from the finished tool. Fix the flute geometry first, because that sets the core diameter and therefore how much room is left for coolant channels. Then pick the channel type: a single central hole suits a one flute or gun style tool, two straight holes suit a two flute drill, and helical holes are only needed when the channel has to follow a twisted flute.
Allowing For Grinding Stock
An as sintered rod carries stock on the diameter, which the tables list as a plus tolerance. A rod ordered at Ø12.0 mm with +0.70/+0.35 mm will arrive between 12.35 and 12.70 mm, so there is material to grind away. If you want to skip that step, order the rod ground to H6 instead.
Checking Eccentricity
The eccentricity column tells you how far the coolant hole can sit off centre. On a Ø12 mm rod that figure is 0.30 mm, on a Ø25 mm rod it is 0.50 mm. Compare it against your flute depth before you release the drawing, because a deep flute on a large rod is where a hole is most likely to break through.
Storage And Handling
Carbide is hard but it is not tough. Keep rods in their sleeves until they go on the machine, do not let ground rods knock against each other, and support long rods along their length rather than at the two ends.
Frequently Asked Questions
What diameters of tungsten carbide rod do you make?
Solid rods are listed from 0.5 mm to 41 mm. Rods with a central coolant hole run from 3 to 30 mm and rods with two straight coolant holes run from 6 to 26 mm. Sizes outside these tables are made to your drawing.
What lengths are standard?
Solid rods are listed at 310 mm and 330 mm with a +5.0/+0 mm tolerance. Coolant hole rods are listed at 330 mm. Other lengths are cut to order.
Do you supply ground rods or only sintered blanks?
Both. Carbide products can be supplied in either the as sintered or the precision ground form, whichever suits your process. Ground rods are finished to H6.
Which grade should I order for a solid carbide end mill?
GW40U and GW45U are the grades we recommend first for end mills, especially high speed milling and work on hard steels, stainless steel, titanium alloy and die steel below 60 HRC. GW30U is a good all round substrate if the tool will also be coated.
Can you make rods with helical coolant holes?
Yes. Coolant channels are offered in single, twin, straight and helix hole options. Helical rods at 30 degrees are made to order, so send the diameter, hole size, bore circle and helix length with your enquiry.
What is the minimum order quantity?
It depends on the diameter and whether the rod is a listed size or a new tool. Send the size and the quantity you have in mind and we will come back with the quantity break that works, usually within 24 hours.
Related Products
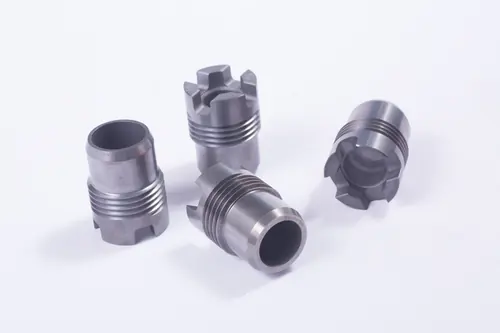
Tungsten Carbide Nozzles
Downhole, blast and threaded nozzles
View product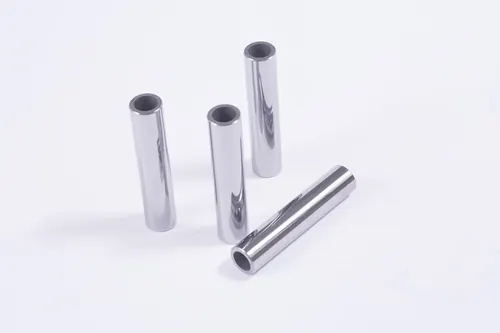
Tungsten Carbide Choke Beans
Flow control liners, seats, points, cages
View product
Tungsten Carbide Gun Drills
Deep hole drill blanks 10.5 to 35 mm
View product
Tungsten Carbide Inserts
Drill bit inserts and PDC substrates
View productRelated Applications
Related Articles
Related Downloads
Send Us The Diameter And We Will Quote The Rod
Tell us the diameter, length, hole configuration and grade, or attach your drawing. Quotations go out in 24 hours or less.