Tungsten Carbide Gun Drill Blanks
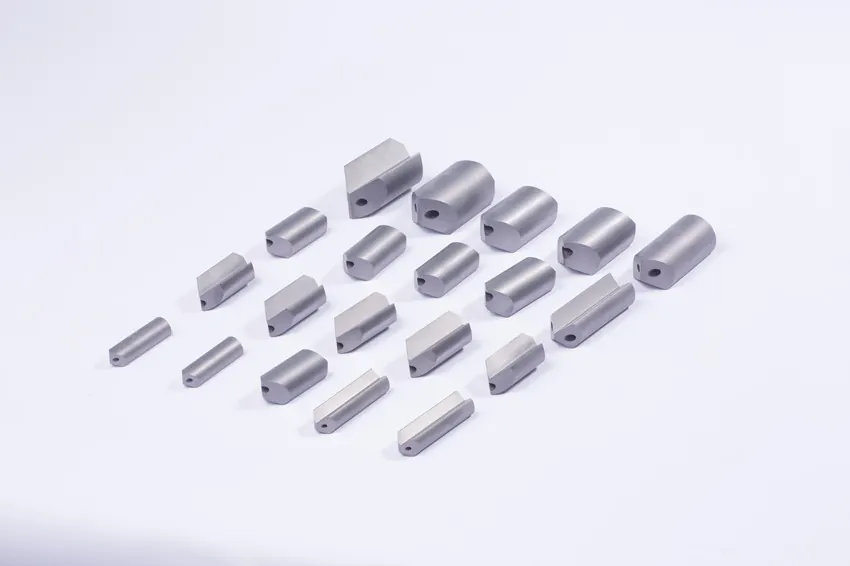
Gun drilling reaches depths that a twist drill cannot hold straight. GWM is an expert in making tungsten carbide gun drills, both as blanks and as finished parts, effective in diameters from 10.5 to 35 mm.
Product Overview
Gun drilling is a special deep hole cutting tool method for outer cuttings. The V type angle is 120 degrees, and for deep hole drilling the V angle goes to 160 degrees. It has to be used on a special machine tool. The process drills deep holes beyond what is possible with conventional machinery and tooling such as twist drills, by using high pressure coolant for clean chip exhaust even at extreme depths.
With a standard twist drill it is difficult to drill a straight and accurately sized hole deeper than about five times the diameter. The gun drill was developed for exactly that problem. We make the blanks and the finished parts, and we can also produce the gun drill according to the customer's request.
Key Benefits
Straight Holes Well Past 5xD
The single flute geometry and the guide pads keep the tool on line where a twist drill would wander.
Coolant Through The Body
A hole bored down the centre of the fluted rod carries coolant to the cutting face and flushes chips back along the flute.
Blank Or Finished
Take the blank and grind it yourself, or have the finished profile made here to your drawing.
Application Scenarios
Where deep hole drilling is the only way to make the part.
Hydraulic Manifolds
Long cross drillings that have to stay on centre and stay sized.
Mould And Die Cooling
Conformal cooling lines drilled deep into tool steel blocks.
Firearm Barrels
The classic gun drilling job, where the bore is many times longer than its diameter.
Injector And Valve Bodies
Small deep bores where surface finish matters as much as position.
Shafts And Spindles
Axial oil feed holes in long rotating parts.
Heat Exchanger Parts
Repeat deep bores across a plate where every hole has to match.
Who It Is For
- Deep hole drilling shops running dedicated gun drilling machines.
- Tool manufacturers that braze or grind their own gun drill tips.
- Mould and die makers drilling cooling circuits.
- Hydraulic component manufacturers with long cross drillings.
Problems It Solves
- Twist drills that wander once the hole passes about five times the diameter.
- Chip packing at depth, which welds the tool into the hole.
- Bore size opening up along the length so the hole fails the gauge at the far end.
- Buying finished gun drills when only the carbide tip needs replacing.
Technical Features
- Effective diameters from 10.5 to 35 mm.
- V type angle of 120 degrees, going to 160 degrees for deep hole work.
- Diameter tolerance of +0.45/−0.10 mm on the finished profile.
- Coolant hole tolerances of ±0.20 mm on both ΦB and ΦC.
- Overall length tolerance of +3.0/+0 mm on the finished profile.
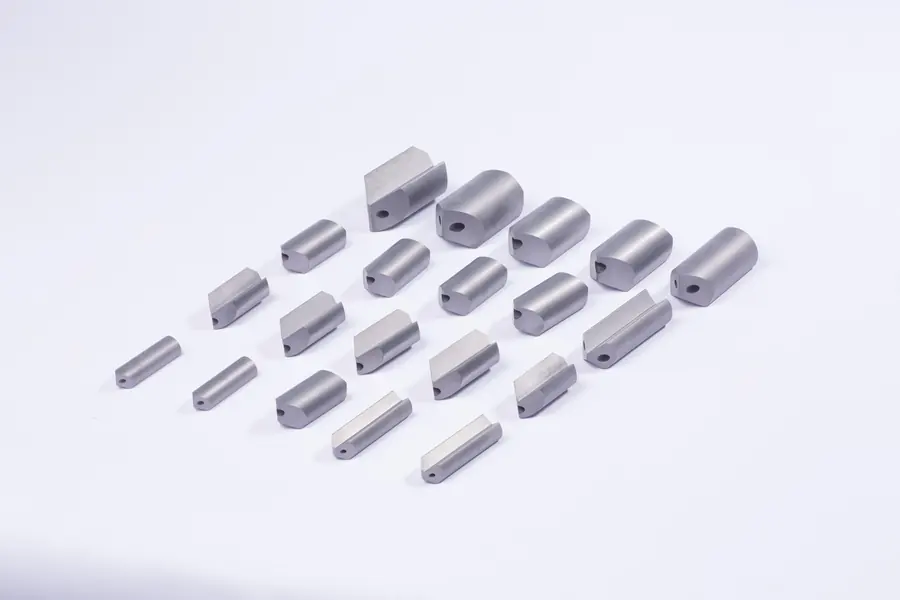
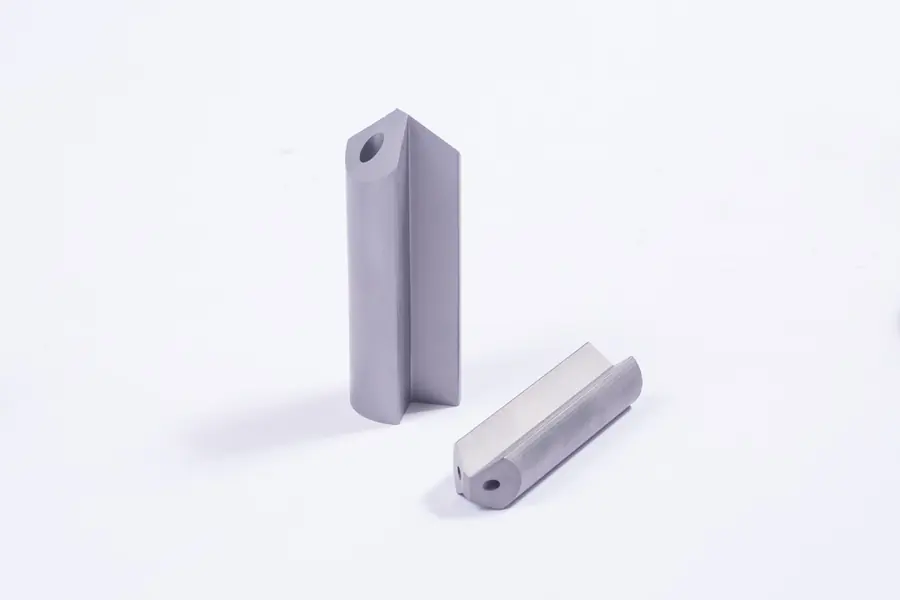
- 330 mm double hole blanks from 10 to 25 mm diameter.
- Blank diameter tolerance from +0.5/+0.3 mm up to +0.5/+0.8 mm depending on size.
- Made to customer request for sizes outside the tables.
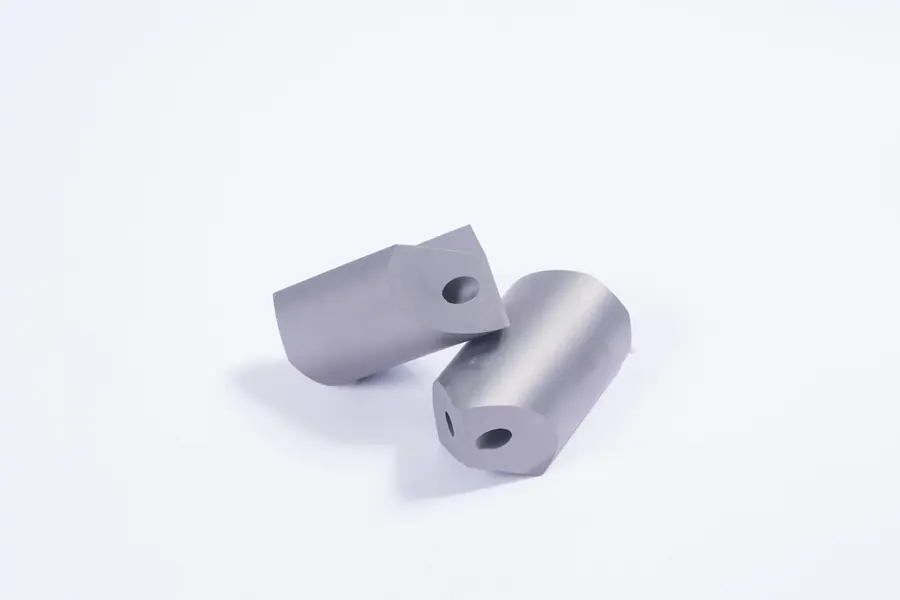
Specifications
| Type | D mm (+0.45/−0.10) | ΦB mm ±0.20 | ΦC mm ±0.20 | L mm (+3.0/+0) |
|---|---|---|---|---|
| QZ10036S | 10.5 | 1.9 | 2.3 | 36 |
| QZ11038S | 11 | 2 | 2.4 | 38 |
| QZ12040S | 12 | 2.2 | 2.5 | 40 |
| QZ13040S | 13 | 2.4 | 2.7 | 40 |
| QZ14040S | 14 | 2.5 | 2.8 | 40 |
| QZ15042S | 15 | 2.4 | 3.3 | 42 |
| QZ16045S | 16 | 2.5 | 3.5 | 45 |
| QZ17045S | 17 | 2.6 | 3.7 | 45 |
| QZT17045S | 17.5 | 2.6 | 3.7 | 45 |
| QZ18051S | 18 | 3.2 | 3.9 | 51 |
| QZ19051S | 19 | 3.2 | 3.9 | 51 |
| QZ20055S | 20 | 3.5 | 4.2 | 55 |
| QZ21055S | 21 | 3.5 | 4.2 | 55 |
| QZ22058S | 22 | 3.5 | 4.5 | 58 |
| QZ23058S | 23 | 3.5 | 4.5 | 58 |
| QZ24058S | 24 | 4 | 5.5 | 58 |
| QZ25061S | 25 | 4 | 5.5 | 61 |
| QZ26061S | 26 | 4 | 5 | 61 |
| QZ27061S | 27 | 4.5 | 5.5 | 61 |
| QZ28063S | 28 | 4.5 | 5.5 | 63 |
| QZ29063S | 29 | 4.5 | 5.5 | 63 |
| QZ30065S | 30 | 5 | 6 | 65 |
| QZ31065S | 31 | 5 | 6 | 65 |
| QZ32065S | 32 | 5 | 6 | 65 |
| QZ33065S | 33 | 5 | 6 | 65 |
| QZ34065S | 34 | 5.5 | 6.5 | 65 |
| QZ35065S | 3 | 5.5 | 6.5 | 65 |
| D mm | D tol. mm | d1 mm ±0.2 | d2 mm ±0.2 | Length mm ±5.0 |
|---|---|---|---|---|
| 10 | (+0.5/+0.3) | 1.9 | 2.3 | 330 |
| 10.5 | (+0.5/+0.3) | 1.9 | 2.3 | 330 |
| 11 | (+0.5/+0.3) | 2 | 2.4 | 330 |
| 12 | (+0.5/+0.3) | 2.2 | 2.5 | 330 |
| 12.5 | (+0.5/+0.3) | 2.2 | 2.5 | 330 |
| 13 | (+0.5/+0.3) | 2.4 | 2.7 | 330 |
| 13.5 | (+0.5/+0.3) | 2.4 | 2.7 | 330 |
| 14 | (+0.6/+0.4) | 2.5 | 2.8 | 330 |
| 14.5 | (+0.6/+0.4) | 2.5 | 2.8 | 330 |
| 15 | (+0.6/+0.4) | 2.6 | 3.3 | 330 |
| 15.5 | (+0.6/+0.4) | 2.8 | 3.3 | 330 |
| 16 | (+0.6/+0.4) | 2.8 | 3.5 | 330 |
| 16.5 | (+0.6/+0.4) | 3 | 3.5 | 330 |
| 18 | (+0.5/+0.8) | 3.2 | 3.7 | 330 |
| 20 | (+0.5/+0.8) | 3.4 | 3.9 | 330 |
| 22 | (+0.5/+0.8) | 3.6 | 4.1 | 330 |
| 24 | (+0.5/+0.8) | 3.8 | 4.3 | 330 |
| 25 | (+0.5/+0.8) | 4 | 4.5 | 330 |
Figures are taken from the GWM deep hole drill sheets. Note that the D value shown for QZ35065S on the original sheet reads 3 mm; the customer is asked to confirm this row before it is used for ordering. Everything else in the tables is as published.
Materials
Every part is quoted against a grade from the GWM chart. Cobalt and nickel binder grades are both available.
Gun drill work asks for hardness at the cutting edge and enough toughness to survive entry. Sub-fine grades in the GW10U to GW30U range cover most drilling duty, and GW30U is the grade we point to when the tool will also be coated. For harder workpiece materials, GW40U carries more binder and stands up better to interrupted entry.
Recommended starting grades for this product: GW10UGW20UGW30UGW40UYG10X
Manufacturing Process
- Step 01
Powder Blending
WC and binder powders are wet milled in ball mills to the grain size the grade calls for.
- Step 02
Forming
Extrusion, two-way pressing or oil pressing, depending on the section and the length of the part.
- Step 03
Sintering
Vacuum sintering and pressure sintering furnaces. Every order is sinter-HIPped.
- Step 04
Finishing
Blank CNC machining, centreless grinding and cryogenic treatment to the drawing.
Quality Control
- Incoming powder checked before milling so grain size and binder content match the grade.
- Density and hardness measured on sintered parts against the published grade values.
- Metallographic microscope used to check porosity and structure after sintering.
- Dimensions and tolerances verified against the drawing before packing.
Certifications
Chengdu Golden Wolfran Carbide is an ISO certificated enterprise. Copies of the current certificates are sent with the quotation on request, so ask us for the version that applies to your order.
Customization Options
We manufacture small and large scale carbide products to your drawing, supplied either as sintered or precision ground.
Any Diameter In Range
Sizes between and beyond the listed types are produced according to your request.
Blank Or Ground Profile
Order 330 mm double hole blanks for your own grinding, or a finished profile to drawing.
Hole Geometry
Coolant hole diameter and position set to your drawing rather than to a fixed standard.
Comparison With Other Products
| Method | How coolant and chips move | Practical diameter limit |
|---|---|---|
| Gun drilling | Coolant is pumped through a hole inside the drill and flows back outside through the flute, carrying the chips with it | Common from 3 to 50 mm, possible from 1 to 3 mm with special equipment |
| BTA / STS | The tool is a tube. Coolant is pumped around the outside and carries chips out through the centre tube | Over 15.6 mm, because tubes have minimum sizes |
| Ejector system | A tube nested inside another tube. Coolant flows down the smaller tube and returns with the chips through the larger one | Over 18.4 mm |
Gun drilling is also possible between 50 and 75 mm, although it is less efficient than BTA deep hole drilling in that range.
Use Guide
Reading The Type Code
QZ22058S describes a 22 mm drill with a 58 mm listed length in the finished profile table, and the ΦB and ΦC columns give the two coolant hole dimensions. Blank part numbers work from the D column instead, with d1 and d2 giving the hole sizes on the 330 mm double hole blank.
Setting Up The Machine
Gun drilling must be used on a special machine tool, not on a machining centre with a long drill in the spindle. The coolant pressure and the flow are as much part of the tool as the geometry, because clean chip exhaust at depth is what keeps the tool alive.
Starting The Hole
Start in a bushing or a pre-drilled pilot. The single flute geometry relies on the guide pads riding an existing bore to stay on line, so entering into open material is the fastest way to send the hole off centre.
Ordering Blanks Instead Of Tools
If you grind your own tools, the 330 mm double hole blank is the part to order. Match the D column to your finished diameter plus grinding stock, and check d1 and d2 against the coolant geometry you grind to.
Frequently Asked Questions
What is gun drilling?
Gun drilling is a kind of special deep hole cutting tool method for the outer cuttings. The angle of the V type is 120 degrees, and for deep hole drilling the V angle goes to 160. It must be used with a special machine tool.
What diameters are your gun drills effective in?
Our gun drilling is effective in diameters from 10.5 to 35 mm. The 330 mm double hole blanks are listed from 10 to 25 mm.
Why not just use a twist drill?
With a standard twist drill it is difficult to drill a straight and accurately sized hole deeper than about five times the diameter. Gun drilling reaches beyond what is possible with conventional machinery and tooling, by using high pressure coolant for clean chip exhaust even at extreme depths.
Do you supply blanks or finished gun drills?
Both. GWM is an expert in making tungsten carbide gun drilling, both blank and finished parts, and we can produce the gun drill according to your request.
How does gun drilling compare with BTA and ejector drilling?
In gun drilling the coolant is pumped through a hole inside the drill and flows back outside through the flute with the chips. BTA pumps coolant around the outside of a tube and takes chips out through the centre, which only works above 15.6 mm. An ejector system nests two tubes and only works above 18.4 mm.
Can you make a size that is not in the table?
Yes. Sizes are produced according to the customer's request, so send the diameter, the length and the coolant hole geometry.
Related Products
Tungsten Carbide Rods
Rotary tool blanks, solid and coolant channel
View product
Tungsten Carbide Nozzles
Downhole, blast and threaded nozzles
View product
Tungsten Carbide Choke Beans
Flow control liners, seats, points, cages
View product
Tungsten Carbide Inserts
Drill bit inserts and PDC substrates
View productRelated Applications
Related Articles
Related Downloads
Send The Diameter Depth And Material
Those three numbers are enough for us to recommend a blank or a finished profile and put a price against it. Quotations go out in 24 hours or less.