Rods With Two Helical Coolant Holes
Two channels twisted at 30 degrees so the coolant follows the flute instead of crossing it. This configuration is made to order.
Overview
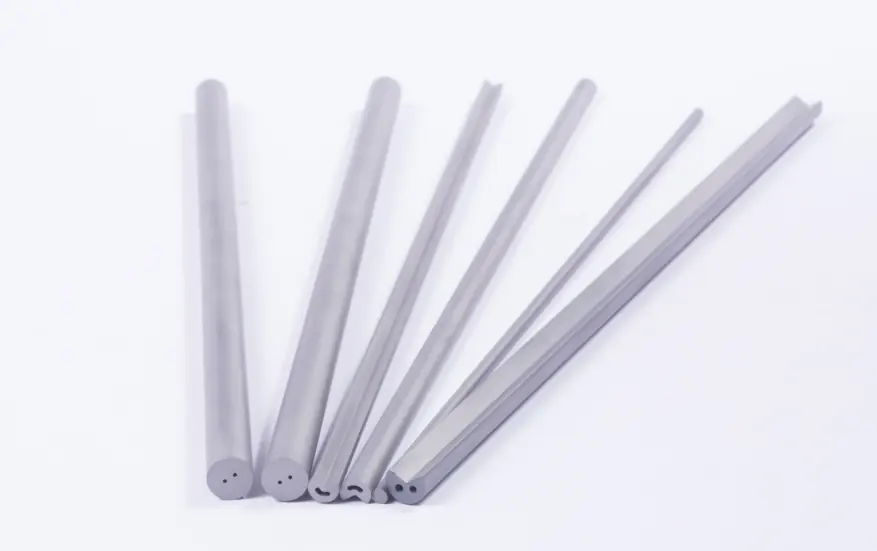
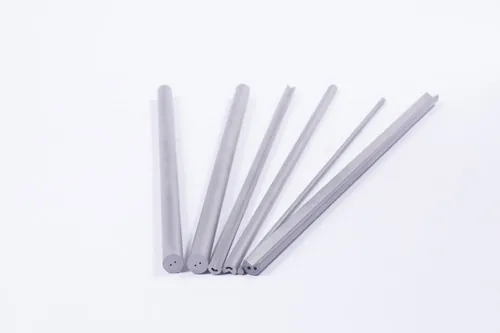
Coolant channel rotary tool blanks are manufactured in single, twin, straight and helix hole options. The helical version twists the two channels through the length of the rod so that the channel stays inside the web as the flute wraps around it.
Because the helix has to match the flute you intend to grind, these rods are made to order rather than held as a listed size. Send the diameter, the hole size, the bore circle and the helix and we will quote against it.
Why This Configuration
- Channels follow the flute, so the web stays intact along the full length.
- 30 degree helix as the listed configuration.
- Made to order in the diameter and hole geometry you specify.
- Same grade choices as the rest of the rod range.
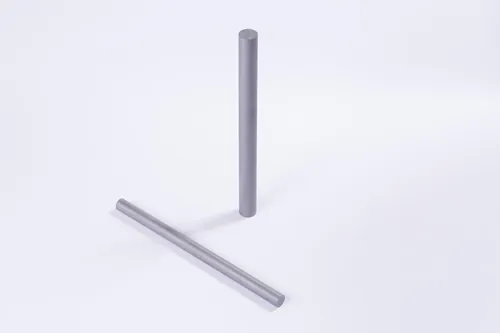
Specifications
| Dimension | What we need from you |
|---|---|
| Rod diameter | Finished diameter, and whether you want it ground to H6 or as sintered with stock |
| Length | 330 mm is our standard rod length; other lengths are cut to order |
| Hole diameter | Channel size and the tolerance you can work with |
| Bore circle | How far the two channels sit from the centreline |
| Helix angle | 30 degrees is the configuration we list; other angles are quoted on request |
| Grade | Pick from the GWM grade chart, or tell us the workpiece material and we will suggest one |
Materials
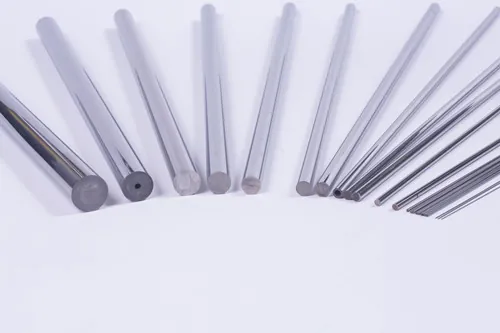
Any grade in the GWM chart can be pressed in this configuration. For cutting tools the usual choices are GW10U, GW20U and GW30U for general drilling, and GW40U or GW45U where the finished tool has to work on hard steels, stainless steel or titanium.
GW10UGW20UGW30UGW40UGW45UYG6XYG10X
Manufacturing Process
- Step 01
Powder Blending
WC and binder powders are wet milled in ball mills to the grain size the grade calls for.
- Step 02
Forming
Extrusion, two-way pressing or oil pressing, depending on the section and the length of the part.
- Step 03
Sintering
Vacuum sintering and pressure sintering furnaces. Every order is sinter-HIPped.
- Step 04
Finishing
Blank CNC machining, centreless grinding and cryogenic treatment to the drawing.
- Incoming powder checked before milling so grain size and binder content match the grade.
- Density and hardness measured on sintered parts against the published grade values.
- Metallographic microscope used to check porosity and structure after sintering.
- Dimensions and tolerances verified against the drawing before packing.
Frequently Asked Questions
Is this a standard stock item?
No. Helical coolant hole rods are made to order because the helix has to match the flute geometry you are grinding.
What helix angle do you list?
30 degrees. Other angles are quoted on request.
Which grades can be used?
The same grades as the rest of the rod range, from ultra fine GW02U through to GW45U, plus the YG and YN series.
What information do you need to quote?
Rod diameter and finish, length, hole diameter, bore circle, helix angle and grade. A drawing covering all of those is ideal.
Related Products
Tungsten Carbide Nozzles
Downhole, blast and threaded nozzles
View product
Tungsten Carbide Choke Beans
Flow control liners, seats, points, cages
View product
Tungsten Carbide Gun Drills
Deep hole drill blanks 10.5 to 35 mm
View product
Tungsten Carbide Inserts
Drill bit inserts and PDC substrates
View productOther Rod Types
Related Articles
Related Applications
Send The Rod Drawing
Diameter, length, hole geometry and grade. Quotations go out in 24 hours or less.