Threaded Flange Bushing With Knurled Collar
A threaded bushing that screws into a housing and still presents a flat, sealable flange face
A Bushing That Locates, Seals And Can Be Tightened By Hand
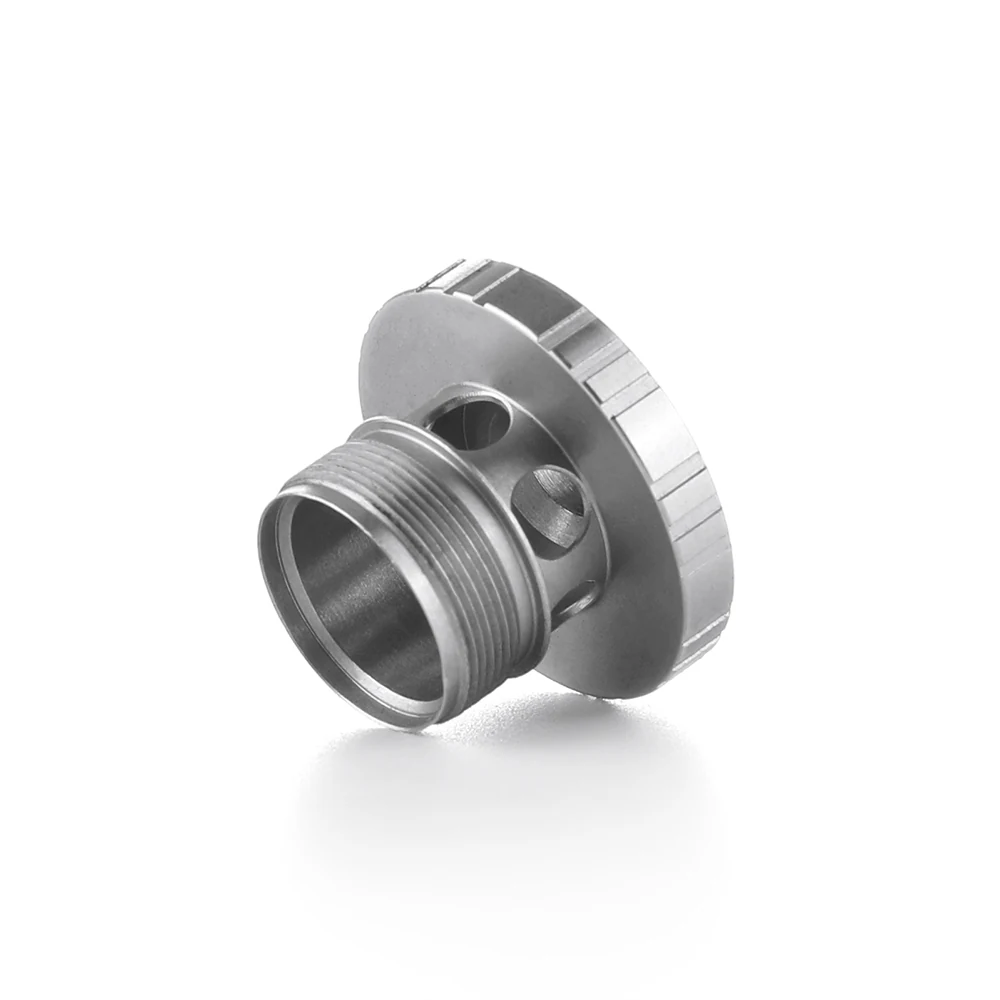
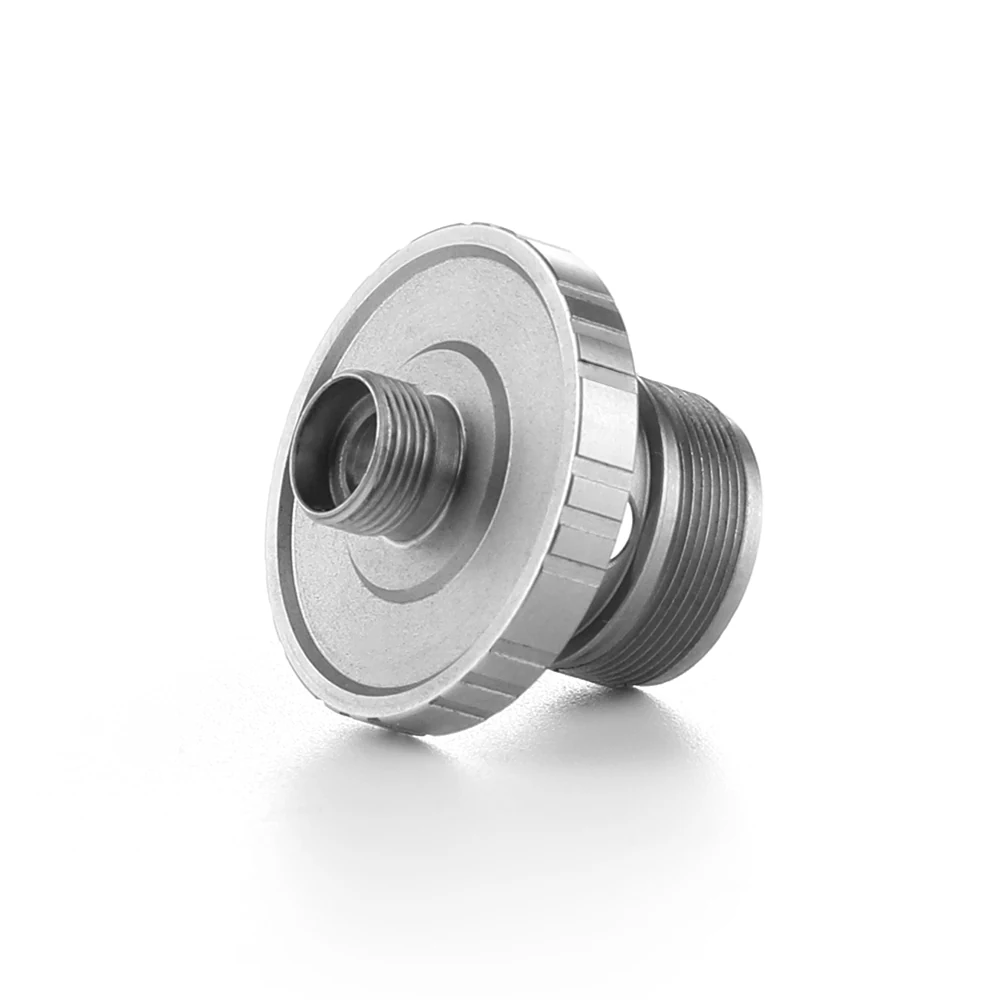
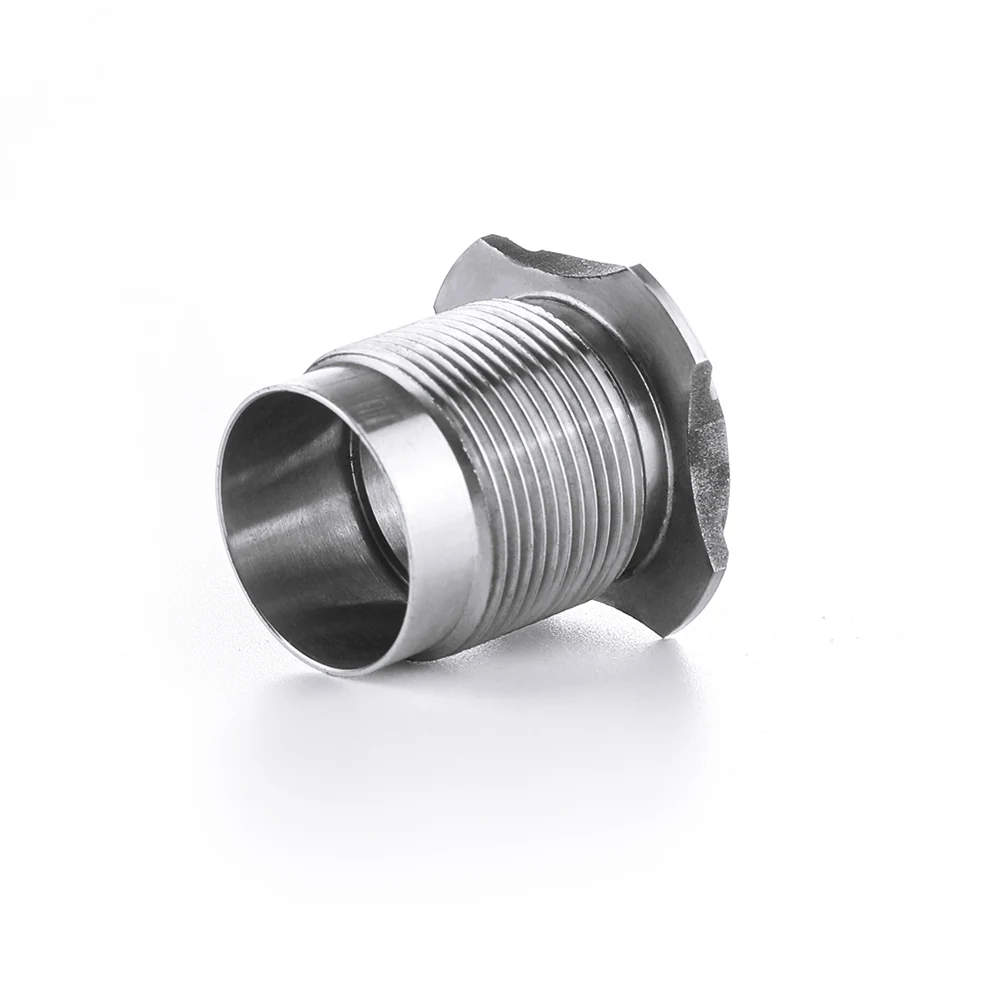
This part combines three jobs in one turning: a male thread that pulls it into the housing, a knurled collar so it can be set by hand before a wrench goes on, and a flange face flat enough to seat a washer or an O-ring. The internal bore is finished after the thread is cut so the bore stays round.
Parts in this family go into fluid and air fittings on office automation and communication equipment, where the assembly has to be serviceable without a special tool.
What The Knurled Flange Design Buys You
Hand-Set Then Torqued
The knurl gives the assembler grip to start the thread square, which is the usual cause of cross-threading on the line.
Sealing Face Machined Last
The flange face is cut after the thread so the thread-cutting forces do not leave it dished.
Bore Kept Round
Finishing the bore after threading avoids the ovality that shows up when the sequence is reversed.
Application Scenarios
- Air and fluid ports on office automation machines
- Serviceable fittings on communication cabinets
- Adjustable stops and adapters in test rigs
- Threaded inserts in machined manifolds
Who It Is For
- Assembly engineers fighting cross-threaded fittings on the line
- Designers who need a flat seat face on a threaded component
- Buyers replacing a two-piece bushing and collar assembly
- Maintenance teams who want a hand-serviceable fitting
What Goes Wrong Without This Geometry
- Cross-threading because the fitter has nothing to grip
- Leaks from a seat face that was dished during thread cutting
- Assemblies that need a special tool for a routine service
- Bore ovality that shows up only after the thread is cut
Grip Where It Matters
A knurl on the collar rather than a spanner flat keeps the part compact.
Right Sequence
Thread first, then face and bore, so the last cut defines the sealing surface.
One-Piece
Nothing to press together, so nothing to work loose in service.
Technical Features
- Male thread to customer specification
- Straight knurled collar for hand tightening
- Flat flange seat suitable for a washer or O-ring
- Relief groove at the thread run-out
- Through bore finished in the final operation
Specifications
| Part Type | Threaded flange bushing |
|---|---|
| Typical Material | Stainless steel or free-cutting steel |
| Primary Process | CNC turning with driven tooling |
| Thread | Metric or imperial to drawing |
| Collar | Straight knurl |
| Tolerance | To customer drawing, confirmed at quotation |
| Inspection | Thread gauge, profile projector |
| Sample Lead Time | Within 30 days of drawing approval |
Thread class, bore size and flange dimensions are taken from your drawing. Nothing here is a stock catalogue dimension.
Materials We Run
- SUS304 for general service
- SUS316L where the fitting sees moisture or cleaning chemicals
- Free-cutting steel with plating for dry indoor use
- Brass where electrical conductivity or non-magnetic behaviour is needed
Manufacturing Process
Turn Body
Outer diameters, collar blank and flange are roughed from bar.
Cut Thread
The male thread and its relief groove are single-point cut or chased.
Knurl Collar
The straight knurl is rolled onto the collar.
Finish Face And Bore
Seat face and through bore are cut last so both stay true.
Quality Control
- Go and no-go thread gauging on first article and during the run
- Seat face flatness checked against the drawing note
- Bore diameter measured on a profile projector
- Knurl depth checked visually against an approved master
- ISO 9001 documented procedures since 2009
Customization Options
- Thread size, pitch and class
- Knurl pattern and collar width
- Flange diameter and seat finish
- Bore diameter and internal chamfers
- Passivation or plating
Against The Usual Alternatives
| Two-piece bushing and pressed collar | One turning removes the press operation and the risk of the collar spinning in service. |
|---|---|
| Hex-headed fitting | A knurl keeps the envelope round and small where there is no room to swing a spanner. |
| Cold-formed blank plus threading | Cold forming wins on very high volumes, machining wins when the seat face and bore carry tight callouts. |
Specifying The Bushing Correctly
State The Thread Class
Give the class as well as the size; it decides how the thread is cut and gauged.
Mark The Sealing Face
Tell us which face seals so we sequence it as the final cut.
Say How It Is Fitted
Hand-tight, torqued or thread-locked changes the knurl and the relief.
Confirm The Finish
Plating affects thread fit, so it is agreed before the sample runs.
Threaded Flange Bushing With Knurled Collar — FAQ
Can you cut both metric and imperial threads?
Yes. The thread is single-point cut or chased from the program, so size, pitch and class come straight from your drawing. Gauges are bought to match before the first article runs.
Will plating change the thread fit?
It can, which is why we agree the finish before the sample. Where the drawing calls for plating we allow for the deposit when the thread is cut and gauge the part after plating.
Is the knurl rolled or cut?
Rolled. A rolled straight knurl work-hardens the surface and keeps the collar diameter predictable, which a cut knurl does not.
What is the minimum order quantity?
There is no fixed minimum. Small first orders are normal while a new part is being qualified; the price per piece simply reflects the setup.
Can you supply the matching housing as well?
Often yes. Send both prints and we will quote them together, which also lets us check the fit before either part ships.
Quote This Bushing From Your Print
Send the thread callout, the seat face requirement and the annual volume. We come back with price, lead time and any note on features worth relaxing.