Square Flange Bearing Housing
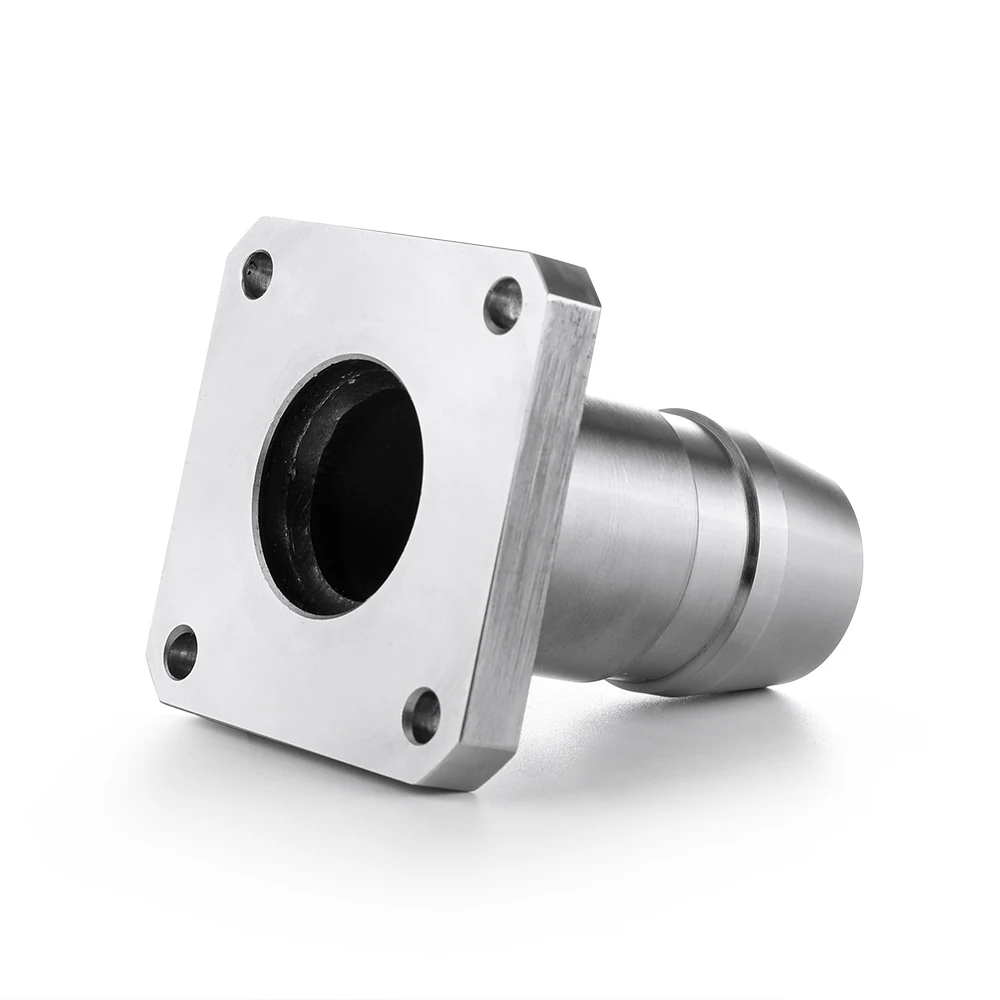
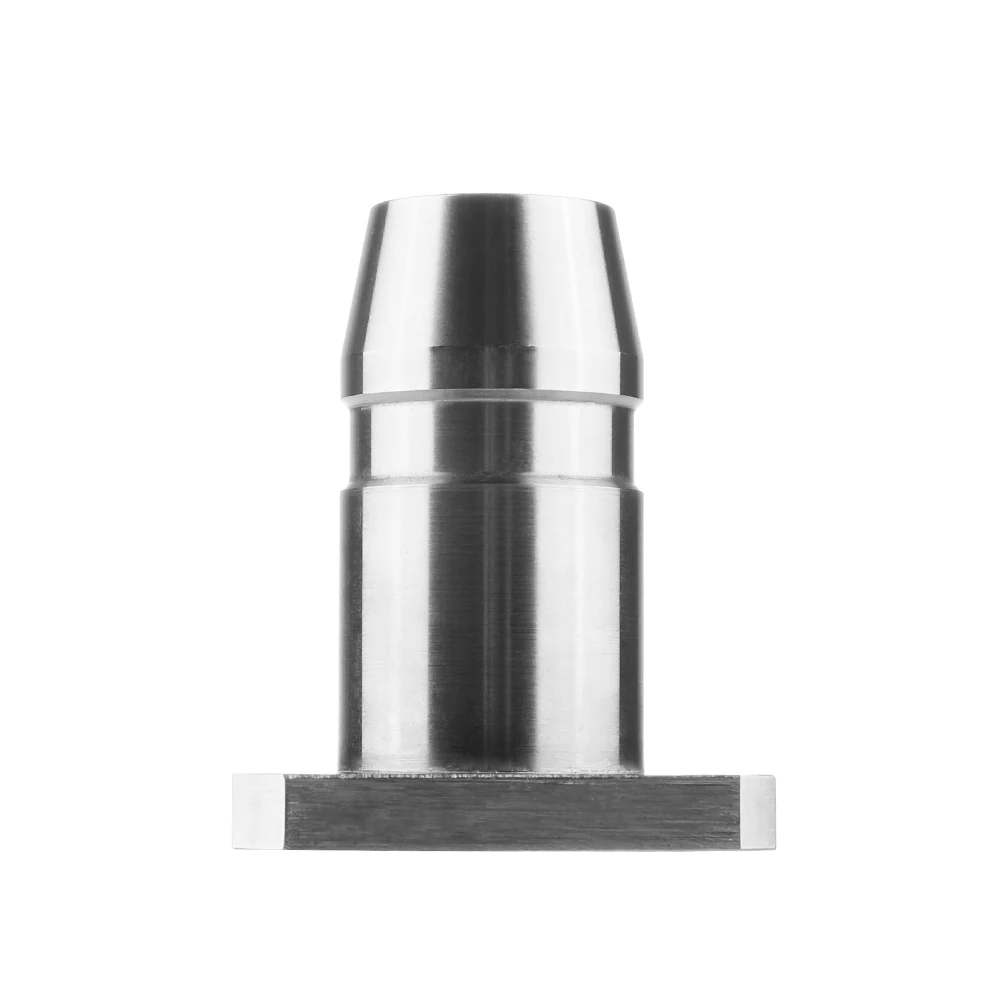
A bolt-on housing where the square flange and the tapered barrel share the bore as their common datum
Flange And Barrel Machined Off One Bore
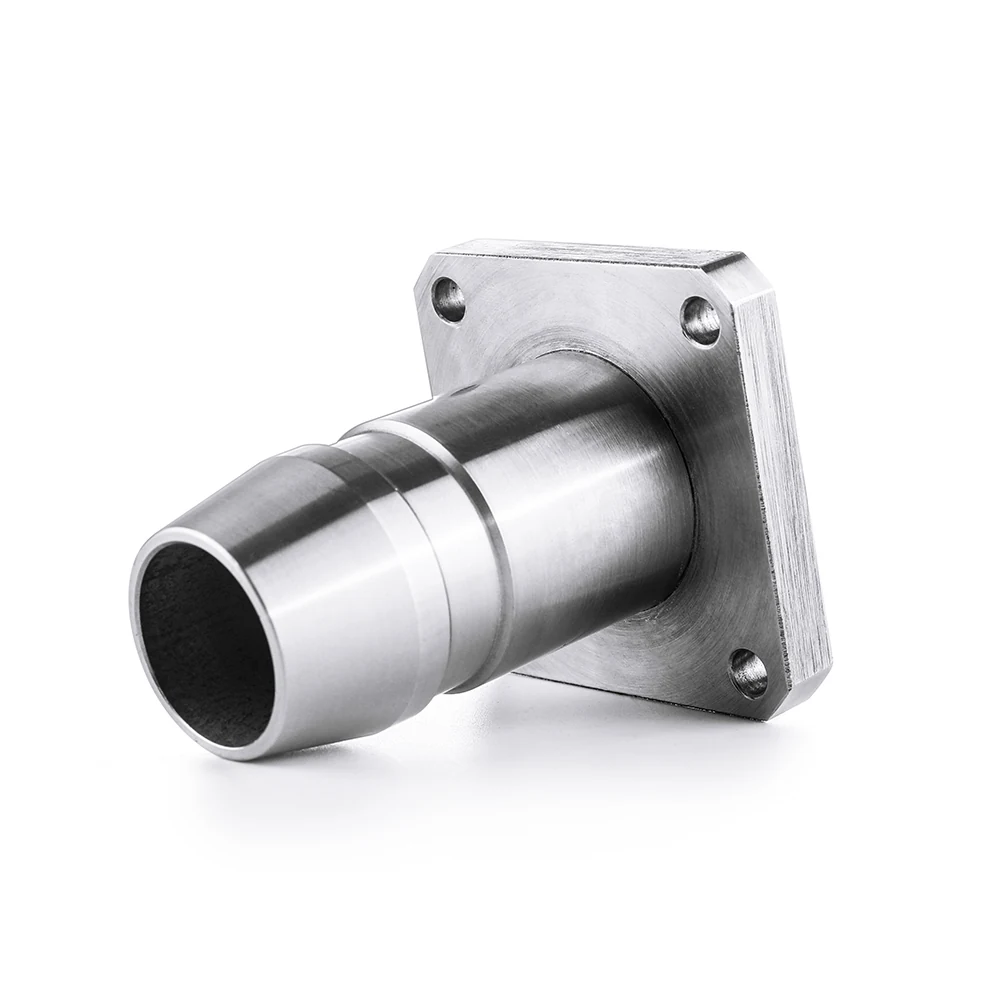
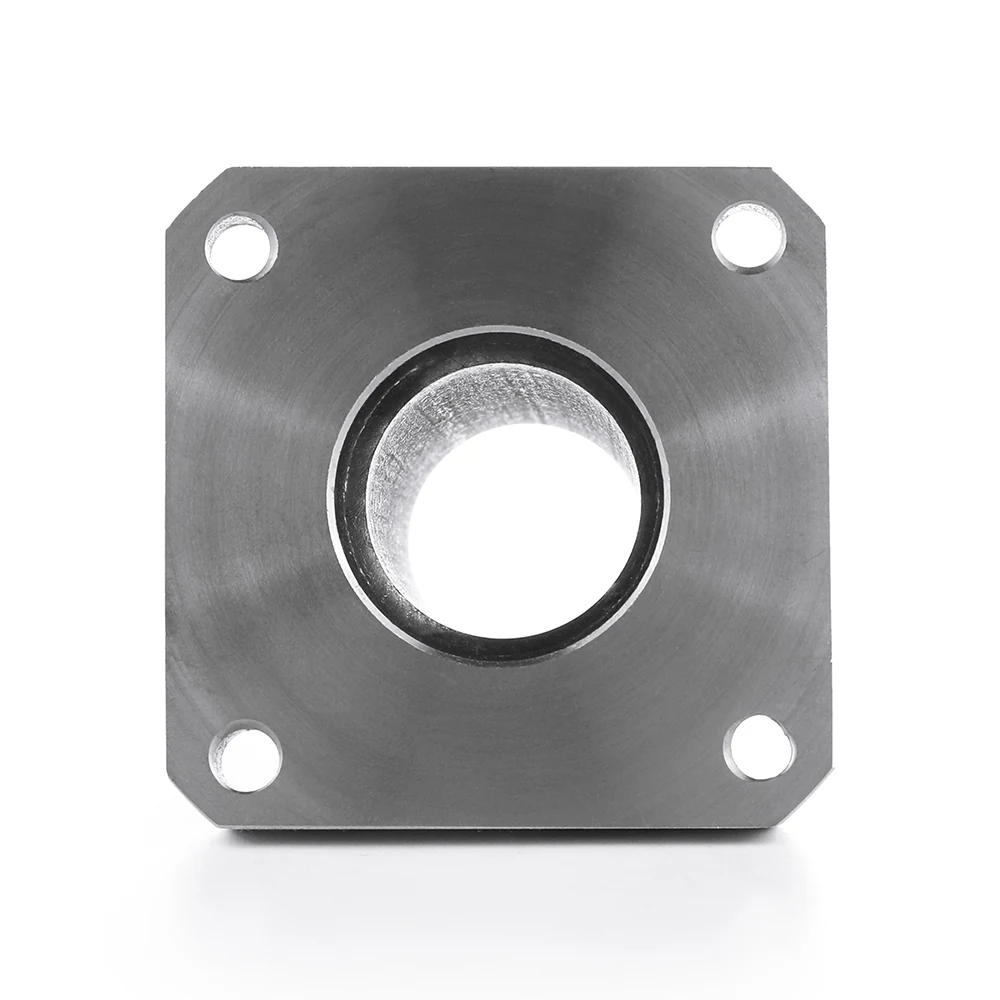
The bore is cut first and everything else is worked from it: the barrel is turned concentric to it, the flange face is squared to it, and the four fixing holes are drilled on a pitch circle that is true to it. That sequence is the whole point of the part, because a bearing housing that is square to nothing will eat bearings.
Parts of this shape carry idler shafts and small bearing sets in office automation and financial machines, where the housing bolts straight to a sheet-metal chassis and has to bring the shaft back onto the design centreline.
What A Single-Datum Housing Gives The Assembly
Bearing Seat True To Mounting Face
Squareness between bore and flange comes from the setup rather than from selective assembly.
Bolt Pattern On Centre
The fixing holes are placed from the bore, so the shaft lands where the chassis expects it.
Tapered Barrel Saves Weight
Material is removed where it does nothing, which also shortens the cycle.
Application Scenarios
- Idler shaft supports in paper and media transports
- Bearing mounts on financial machine chassis
- Small gearbox output supports
- Roller mounts in conveying modules
Who It Is For
- Designers mounting a bearing to a sheet-metal chassis
- Buyers replacing a cast housing with a machined one
- Engineers chasing shaft alignment problems on an existing product
- OEMs standardising on one housing across several machine models
Alignment Problems This Part Removes
- Bearings running hot because the housing is not square to the shaft
- Bolt patterns that force the shaft off the design centreline
- Cast housings with bores that move between batches
- Shims added on the line to correct an out-of-square mount
Bore First
Every later feature is referenced to the finished bore.
Measured Squareness
Flange-to-bore squareness is on the first article report.
Stable Batches
One program, one fixture, archived against the part number.
Technical Features
- Square flange with four counterbored fixing holes
- Tapered barrel turned concentric to the bore
- Bearing seat finished to the drawing fit
- Flange face machined square to the bore axis
- Edge breaks on all handled corners
Specifications
| Part Type | Square flange bearing housing |
|---|---|
| Typical Material | Stainless steel or free-cutting steel |
| Primary Processes | CNC turning and milling |
| Mounting | Four-hole square flange |
| Bore | Bearing seat to drawing fit |
| Tolerance | To customer drawing, confirmed at quotation |
| Inspection | Profile projector, 2D height gauge |
| Sample Lead Time | Within 30 days of drawing approval |
Bore fit is derived from the bearing you nominate. Flange and hole pattern come from your drawing.
Materials We Run
- Free-cutting steel for dry indoor mechanisms
- SUS304 stainless for humid or washdown environments
- SUS316L where cleaning chemicals are used
- Aluminium alloy where mass matters more than wear
Manufacturing Process
Bore First
The bearing seat is cut and becomes the datum for everything else.
Turn Barrel
The tapered body is turned concentric to that bore.
Mill Flange
The square flange is milled and faced square to the bore axis.
Drill Pattern
Fixing holes are drilled and counterbored from the bore centre.
Quality Control
- Bore size checked before the part moves to milling
- Flange-to-bore squareness recorded on the first article
- Hole pitch verified on a profile projector
- Bearing trial fit on sample parts
- Procedures held under the ISO 9001 system certified in 2009
Customization Options
- Bore diameter and fit class
- Flange size, thickness and hole pattern
- Barrel length and taper
- Grease groove or retaining ring groove
- Plating, passivation or black oxide
Machined Housing Against The Alternatives
| Cast iron pillow block | Far smaller envelope and a bore that does not move between foundry batches, at a higher unit price. |
|---|---|
| Pressed sheet-metal bracket | Holds the bearing seat as a machined fit instead of relying on a pressed hole. |
| Welded fabrication | No weld distortion to machine out afterwards, and one part number instead of three. |
Getting The Housing Right First Time
Give The Bearing Part Number
We work the seat fit from the bearing maker's recommendation.
Mark The Datum
Say whether the flange or the bore is datum A on the drawing.
State The Chassis Material
Steel or aluminium chassis changes the bolt and counterbore choice.
Send Quantities By Year
Annual volume decides whether we fixture for batch or for flow.
Square Flange Bearing Housing — FAQ
Can you machine the housing to suit a specific bearing?
Yes. Give us the bearing part number and we work the seat fit from the manufacturer's mounting recommendation rather than guessing at a tolerance band.
Do you check squareness between the flange and the bore?
It is on the first article report for every new part number, because that is the dimension which decides whether the bearing runs cool. Running samples are checked through the batch.
Can the flange be round or rectangular instead of square?
Yes. The flange shape is milled, so it follows your drawing. Changing it does not change the way the part is set up.
Is aluminium an option?
It is, where mass matters more than wear resistance at the bearing seat. We will say if we think the seat will fret in service.
Can you supply the housing already fitted with the bearing?
We can press bearings into the housings if you supply them or nominate the source. Tell us at quotation so the handling and packing are costed in.
Related Guides
Quote The Bearing Housing
Send the print together with the bearing part number and the chassis material. You get price, lead time and a note on the seat fit we intend to hold.