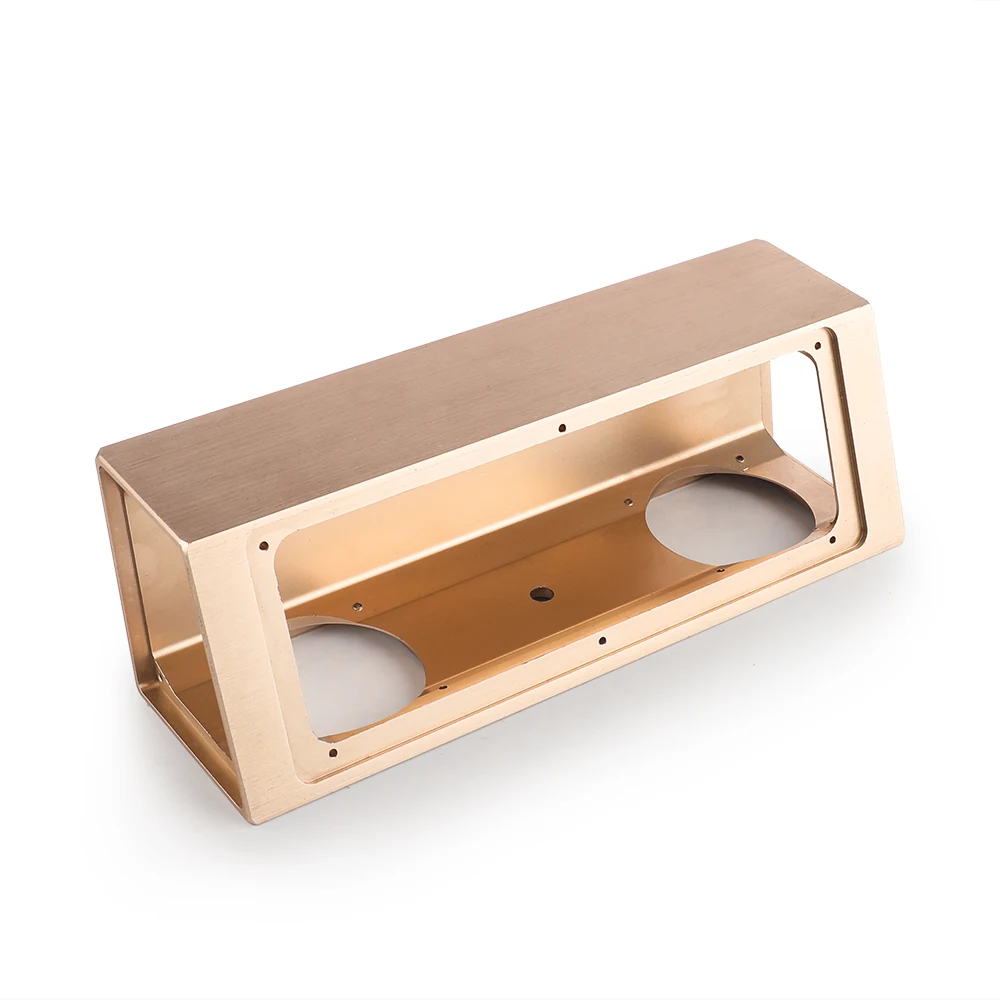
Machined Box Frame Housing
A rigid open frame milled from solid stock, with the window, the pockets and the mounting faces all cut from one datum
A Frame That Stays Square Because It Was Never Welded
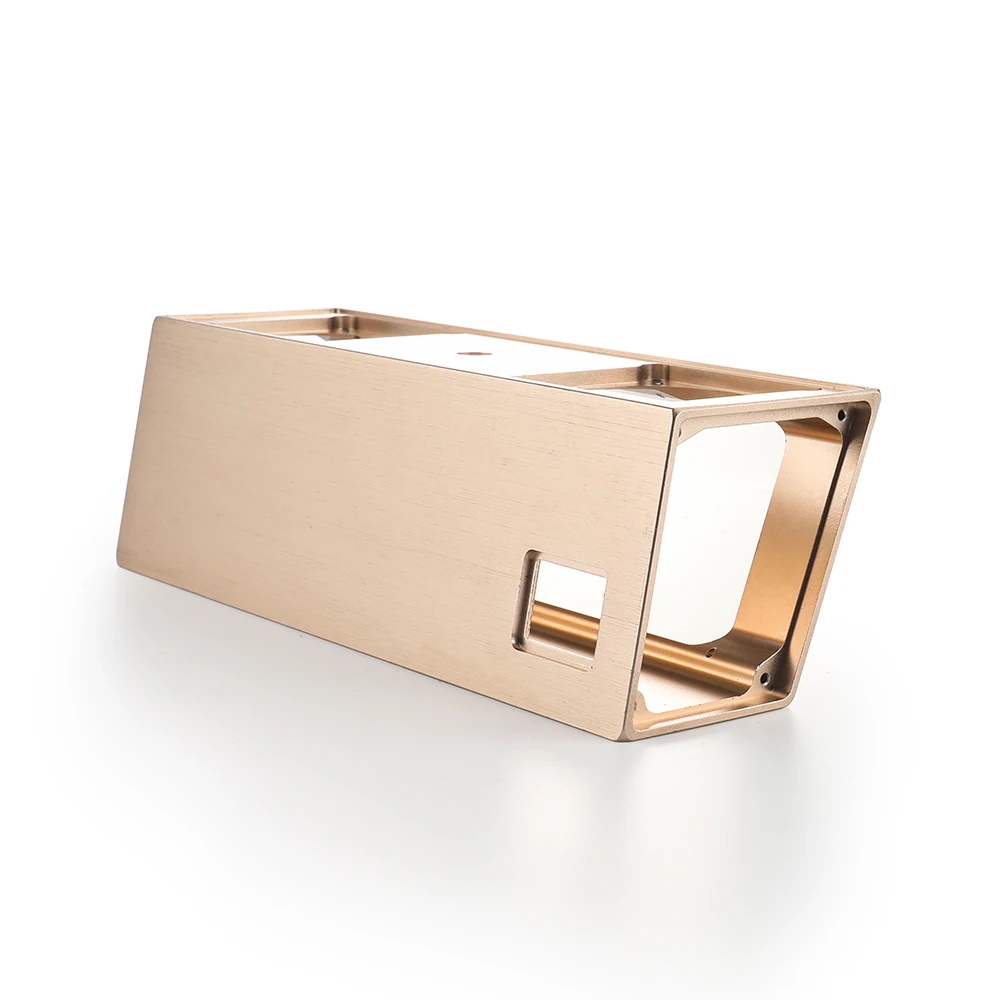
The housing is milled from a solid block: the large window, the internal pockets and the mounting faces are all cut without ever heating the material. That is why the mounting faces stay flat and parallel, which a welded or bolted frame of this size struggles to do.
The original product page lists this item under SUS316L. Frames of this type carry optical, sensing or drive assemblies where the relationship between two mounting faces must not move.
What A Solid-Milled Frame Gives You
No Weld Distortion
Nothing is heated, so nothing pulls out of square after machining.
Faces Cut From One Datum
Parallelism between mounting faces is a machining result you can inspect.
Stiff For Its Mass
Material is removed only where the design allows, leaving the load paths intact.
Application Scenarios
- Optical and sensor mounting frames
- Drive module chassis in automation equipment
- Instrument housings that carry alignment
- Sub-frames inside larger machine structures
Who It Is For
- Designers who need two faces to stay parallel in service
- Buyers replacing a welded frame that needs re-machining
- Engineers with alignment drift on an existing assembly
- Teams needing low volumes without casting tooling
What Welded And Cast Frames Do Wrong
- Welded frames that move after stress relief and need re-machining
- Cast frames with wall thickness variation and hidden porosity
- Alignment that drifts as a bolted frame works loose
- Tooling cost for a frame that will only ever be built in tens
One Block
The frame is a single piece, so there is no joint to relax.
Datum Discipline
Faces, window and pockets all reference the same datum set.
No Tooling Charge
Low volumes are practical because there is no pattern to pay for.
Technical Features
- Open window machined through the body
- Internal pockets cut to reduce mass
- Mounting faces machined parallel from one datum
- Corner radii to the cutter size stated on the drawing
- Tapped holes for mating components
Specifications
| Part Type | Open box frame housing |
|---|---|
| Material | SUS316L stainless steel, as listed on the original product page |
| Primary Process | CNC milling from solid |
| Key Features | Through window, internal pockets, tapped mounting holes |
| Tolerance | To customer drawing, confirmed at quotation |
| Finish | As machined; bead blast or passivation on request |
| Inspection | Dimensional check from the drawing datums |
| Sample Lead Time | Within 30 days of drawing approval |
SUS316L is the grade recorded on the original product listing for this part. All dimensions come from your drawing.
Materials We Run
- SUS316L stainless, the grade named on the original listing
- SUS304 where the environment is less aggressive
- Aluminium alloy where mass is critical
- Brass or copper alloy for conductive or non-sparking duty
Manufacturing Process
Square The Block
The billet is faced and squared to create the datum set.
Rough The Window
Bulk material is removed from the window and pockets.
Finish Faces
Mounting faces and bores are finished from the original datums.
Tap And Deburr
Threads are cut and every edge is broken before inspection.
Quality Control
- Datum faces checked before finishing operations begin
- Parallelism between mounting faces recorded on the first article
- Tapped holes gauged
- Visual inspection for tool marks on visible faces
- ISO 9001 quality system, certified in 2009
Customization Options
- Overall envelope and wall thickness
- Window size and corner radii
- Tapped hole pattern and thread sizes
- Surface finish, bead blast or passivation
- Material substitution after a stiffness review
Milled Frame Against Welded And Cast Frames
| Welded steel frame | No distortion and no stress-relief cycle, at a higher material cost because the window is cut away rather than left out. |
|---|---|
| Aluminium casting | No pattern cost and no porosity; casting wins once volumes justify the tooling. |
| Bolted plate assembly | One rigid piece rather than a stack of joints that can work loose in service. |
Getting A Frame Quoted
Mark The Critical Faces
Tell us which faces carry alignment so we finish them last.
State Corner Radii
Internal radii decide the smallest cutter and therefore the cycle time.
Give The Thread List
Hole sizes and depths belong on the print, not in an email.
Confirm The Finish
Bead blast, passivation or as-machined changes handling and cost.
Machined Box Frame Housing — FAQ
Why is this part listed in SUS316L?
SUS316L is the material recorded on the original product page for this frame, and we have kept that as the stated grade. If your application is less demanding, SUS304 or aluminium will usually cost less.
Can you machine a frame this size from solid economically?
For low and medium volumes, yes, because there is no tooling to pay for. Once the design is frozen and the annual quantity is large, a casting with machined faces is usually cheaper and we will say so.
How do you control parallelism between the mounting faces?
By establishing a datum set when the block is squared and finishing both faces from it, rather than flipping the part and re-datuming. The measured result appears on the first article report.
What internal corner radius should I allow?
The smaller the radius, the smaller the cutter and the longer the cycle. Tell us the function of the corner and we will suggest the largest radius that still works.
Can you supply the frame bead blasted?
Yes, and passivation after blasting is normal for stainless. Both are noted on the drawing so the finished dimensions allow for them.
Quote This Frame From Your Model
Send the 3D model with a dimensioned drawing showing datums and thread sizes. We reply with price, lead time and any machining notes worth acting on.