Injection Moulds and Tooling
Eight mould types, mould bases and components from the brands your drawings already name, and a steel list that runs from 1.1730 through to S136.
TJ-Teck started in 2017 with a single machine and now builds plastic injection moulding tools as its main business. The shop works to the standards used by buyers in Europe and America, which in practice means the mould base, the hot runner and the standard components come from suppliers your maintenance department already stocks.
The eight mould types below are the ones TJ-Teck quotes as standard. Which one your part needs is usually decided by two things: whether the part has a thread or an undercut, and how many parts a year you actually buy.
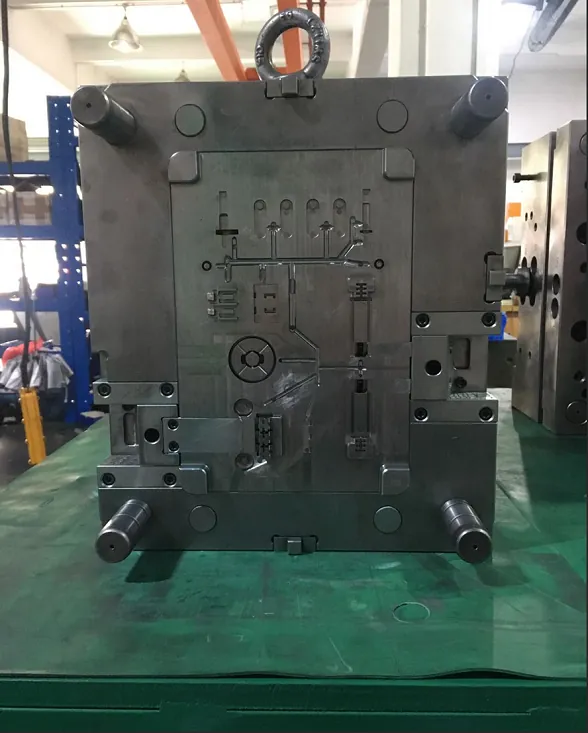
Mould types
What each of the eight is for
These are the mould types TJ-Teck quotes as standard. The right one is usually obvious once the part geometry and the annual volume are both on the table.
| Standard Mold | The default two-plate tool for a part with no undercut. Lowest build cost and the fastest route to first samples. |
|---|---|
| Prototype Mold | A simplified tool for design verification and small pre-production batches, built in softer steel with fewer actions. |
| Reversed Mold | Cavity and core swapped relative to the usual layout, used where the cosmetic face has to stay on the moving half. |
| Multi-cavity Mold | Two or more identical cavities in one tool. The right answer once annual volume makes the extra build cost cheaper than the extra machine hours. |
| Unscrewing Mold | A rotating core that unwinds a moulded thread, so the thread flank has no parting line and the closure seals. |
| Hot runner Mold | No runner to regrind and a gate position that is not tied to the part edge. Built with HRS, Synventive, Husky, Incoe, Mold Master, YUDO, Mastip, Ewikon, Runipsys or DME systems. |
| 2K Over Mold | A rigid substrate moulded first, then a second material moulded over it. Two tools, a transfer step, lower tooling investment. |
| 2K Rotational Mold | The core rotates between two cavities inside one cycle, so a finished two-material part leaves the machine every shot. Higher build cost, much shorter cycle. |
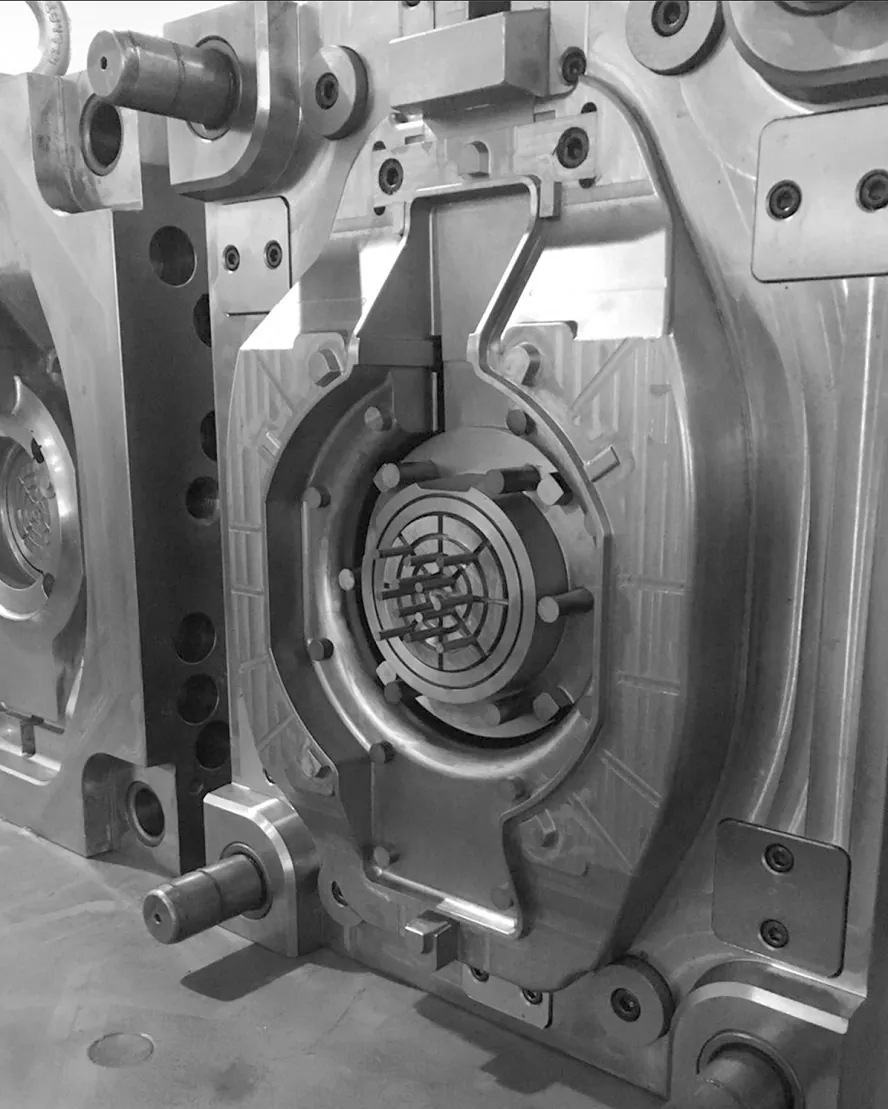
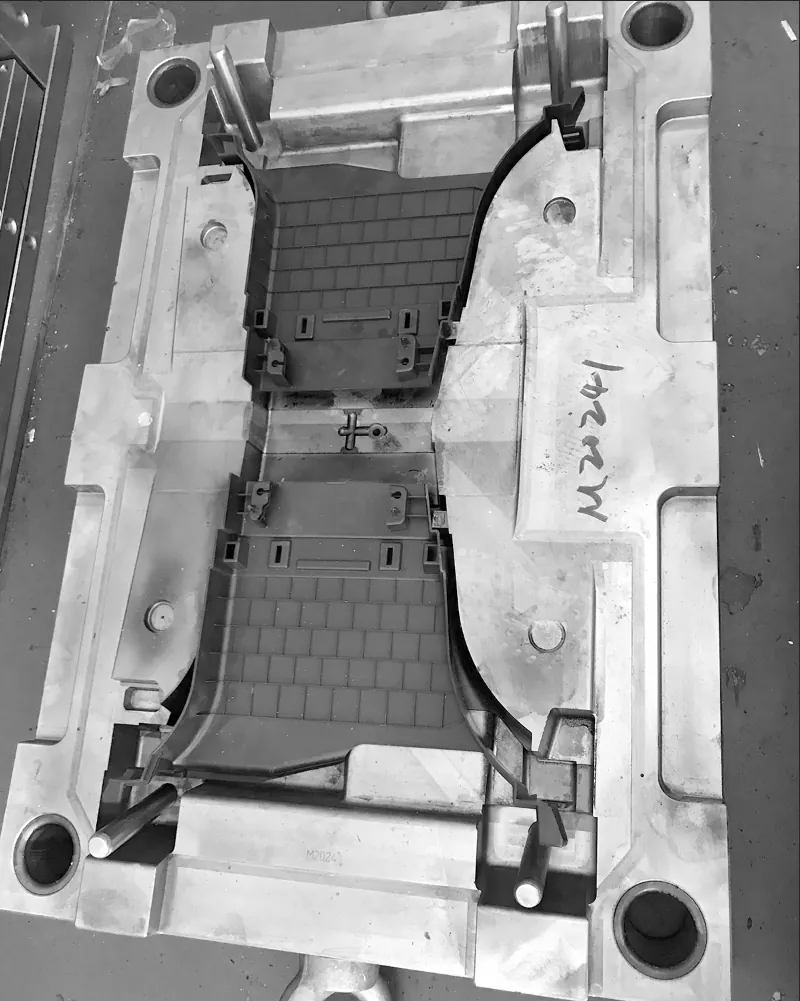
Shop floor
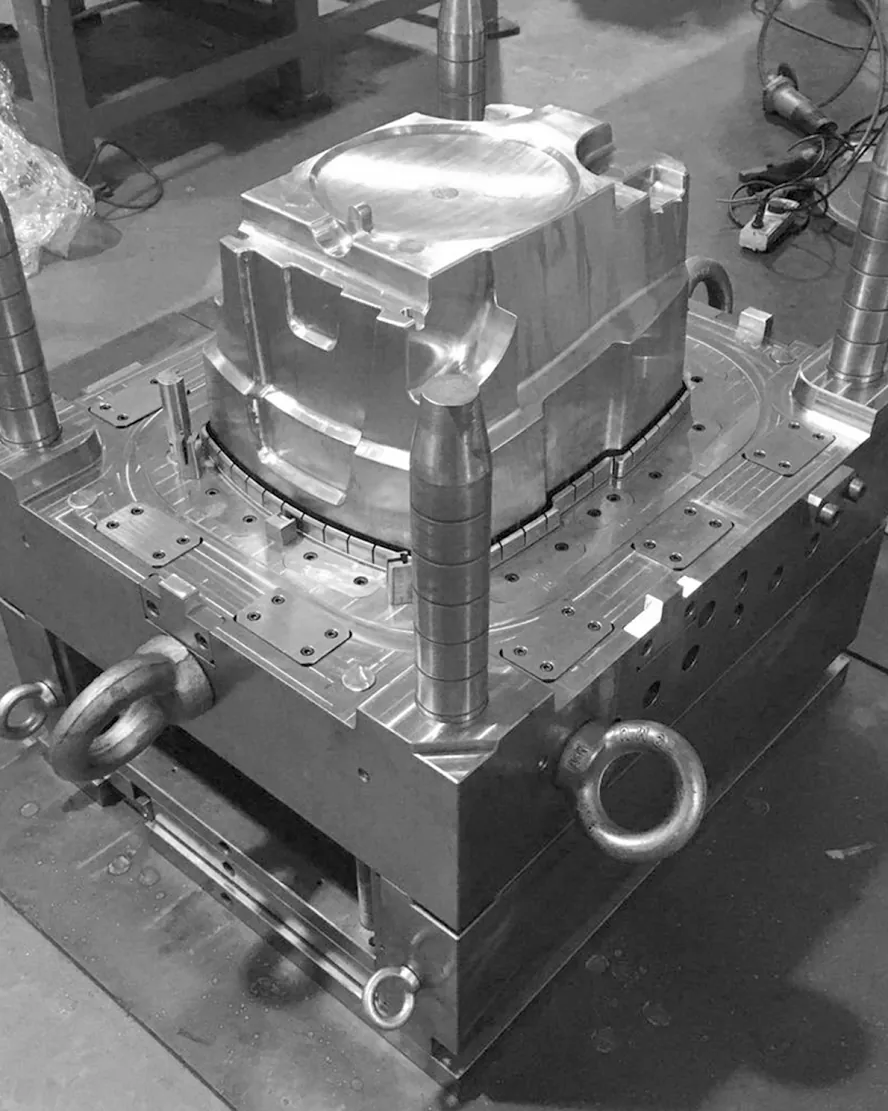
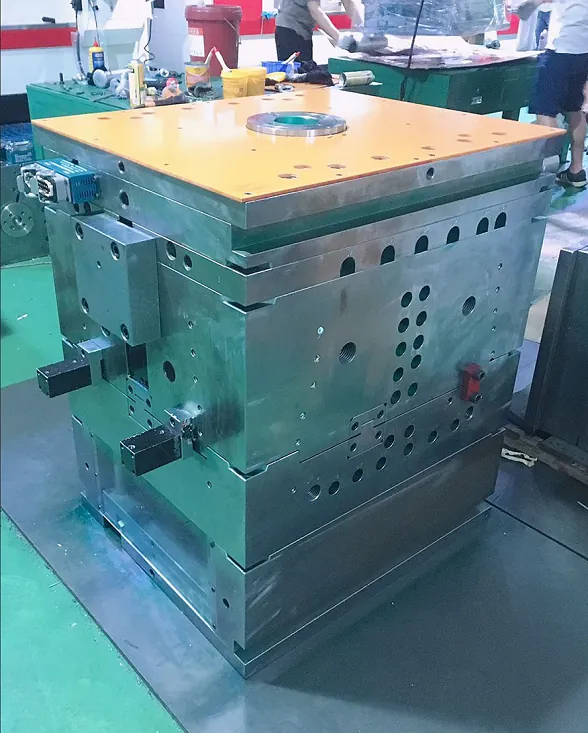
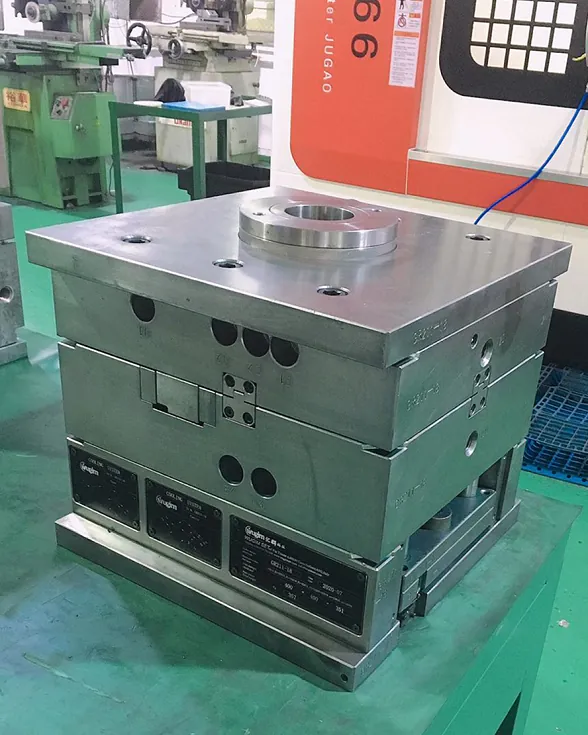
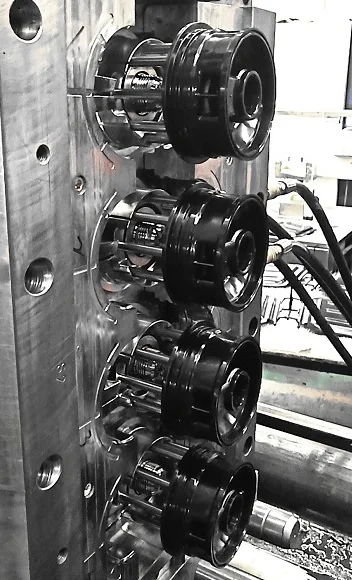
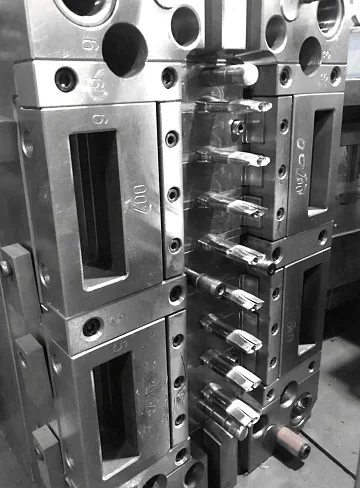
Tooling built and fitted in Chang'an
Cavity and core work, bench fitting, first trial and export crating.
Quotation for injection moulds and tooling
Send 2D and 3D data or a sketch with the annual volume, and the quotation comes back in 1-3 working days.