Design for the Material Not for Steel
A drawing that works in tool steel does not automatically work in carbide. Carbide is far harder and far more brittle so features that a steel part tolerates can become crack starters.
The most useful thing you can do is send the drawing before it is frozen. Small changes at that stage are free and the same changes after tooling has been made are not.
Features Worth Reviewing Early
- Sharp internal corners. They concentrate stress. A radius is almost always better.
- Thin walls. Thin sections are difficult to press and difficult to support during grinding.
- Abrupt section changes. Large changes in thickness produce uneven shrinkage during sintering.
- Dense hole patterns. Possible but they need planning. We have produced a sleeve with 176 holes.
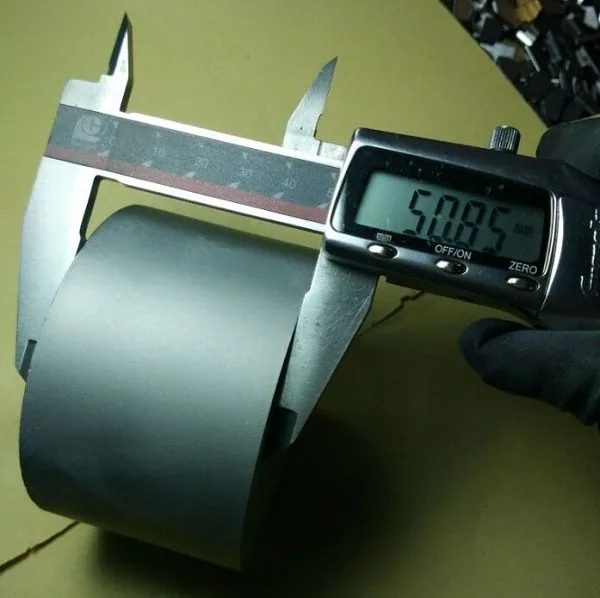
- Large diameters. They need pressing and handling capacity as well as machining capacity.
Mounting Matters as Much as the Part
Many carbide failures are mounting failures. A carbide insert supported unevenly in a steel holder will crack even if the grade and geometry are correct.
Tell us how the part is held. Interference fit shrink fit brazed seat or clamped all place different demands on the geometry.
Say Which Dimensions Are Critical
Not every dimension on a drawing is equally important and pretending otherwise makes a part more expensive than it needs to be.
Mark the dimensions that actually control the function. Those are the ones we inspect before packing and those are the ones both sides measure the same way. See custom parts from drawing.