Double Stage Vacuum Pump
A double stage vacuum pump is a type of pump designed to create a vacuum by removing gas or air molecules from a sealed chamber or system. It consists of two stages or sets of rotating vanes, which work together to increase the efficiency and achieve a higher level of vacuum compared to single-stage pumps. Double...
Introduction
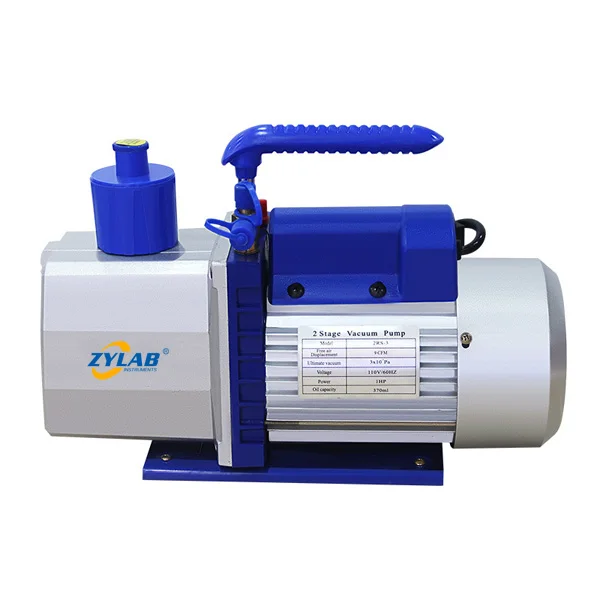
A double stage vacuum pump is a type of pump designed to create a vacuum by removing gas or air molecules from a sealed chamber or system. It consists of two stages or sets of rotating vanes, which work together to increase the efficiency and achieve a higher level of vacuum compared to single-stage pumps.
The working principle of a double stage vacuum pump involves two separate pumping stages, typically referred to as the high vacuum stage and the low vacuum stage.
By using two stages, the double stage vacuum pump can achieve a higher vacuum level compared to a single-stage pump. The low vacuum stage removes the majority of the gas, while the high vacuum stage further reduces the pressure to achieve a deeper vacuum.
Double stage vacuum pumps are commonly used in various applications where a high level of vacuum is required, such as in laboratories, manufacturing processes, scientific research, and industrial applications. They offer improved performance and higher pumping speeds compared to single-stage pumps, making them suitable for applications that demand a more robust vacuum system.
Main Characteristic
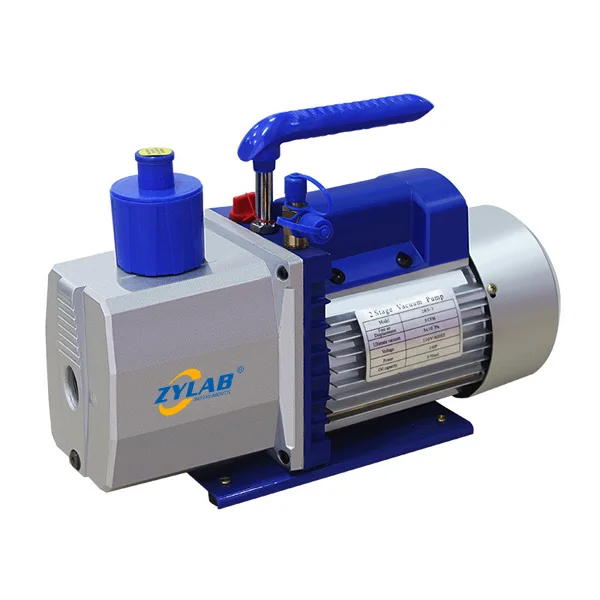
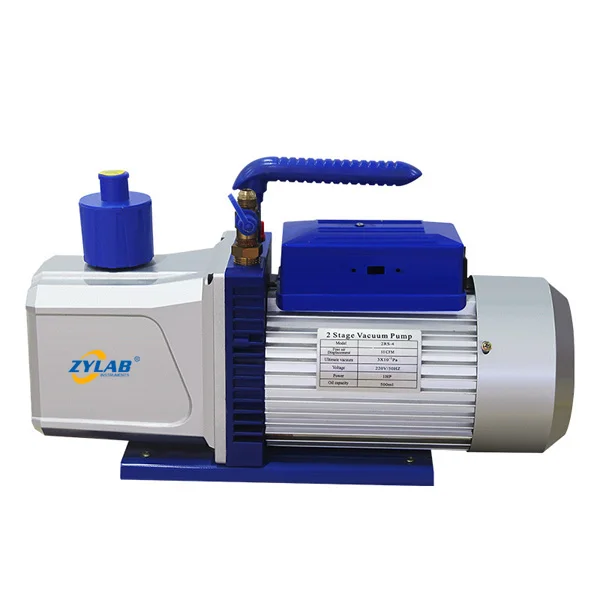
1. Adopting copper wire multi-layer winding motor, providing stable high-power output and long service life.
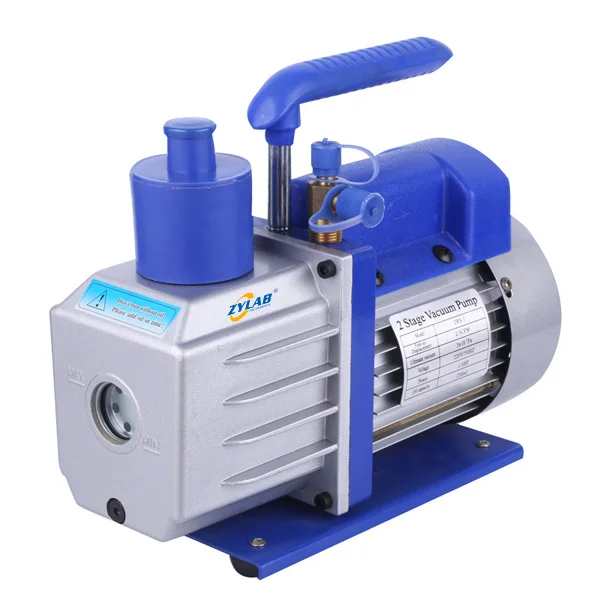
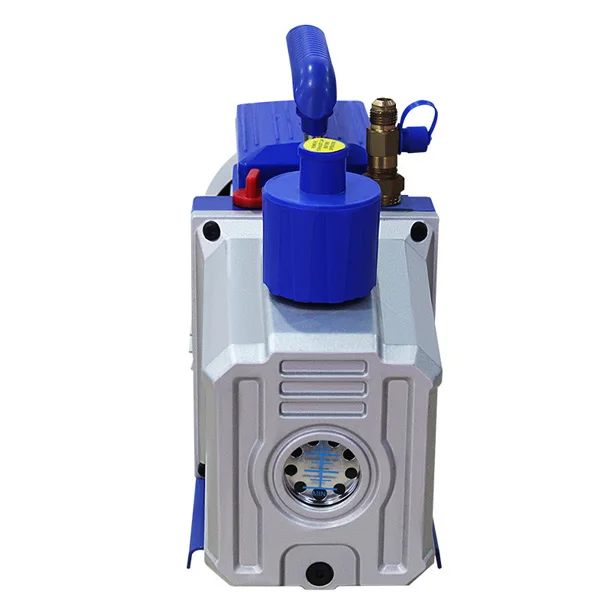
2. The large oil window is convenient for observing the oil level and adding oil in a timely manner.
3. Integral cylinder structure, high precision, high ultimate vacuum.
4. Adopting an oil mist catcher, it functions as a 5-layer filter, effectively preventing oil smoke splashing and reducing noise.
Applications
Double stage vacuum pumps have a wide range of applications across various industries and fields. Some common applications include:
1. Laboratories and Research Facilities
Double stage vacuum pumps are extensively used in laboratories and research facilities for tasks such as vacuum drying, degassing, filtration, distillation, and sample preparation. They provide the necessary vacuum levels required for experiments, analysis, and scientific research.
2. Manufacturing Processes
Double stage vacuum pumps play a crucial role in manufacturing processes, especially in industries such as electronics, pharmaceuticals, food processing, and automotive. They are used for vacuum packaging, vacuum impregnation, vacuum forming, vacuum distillation, and other processes that require precise control over pressure and the removal of gases or vapors.
3. Vacuum Coating
In industries like semiconductor manufacturing, optics, and surface coatings, double stage vacuum pumps are employed for vacuum deposition processes. These pumps help create a controlled environment with a high vacuum level to deposit thin films or coatings onto substrates.
4. Vacuum Furnaces
Double stage vacuum pumps are commonly used in vacuum furnaces for applications such as heat treatment, brazing, sintering, and annealing. They create a vacuum environment inside the furnace, enabling controlled heating and processing of materials at elevated temperatures without oxidation or contamination.
5. Vacuum Evacuation
Double stage vacuum pumps are utilized for rapid evacuation of air or gases from systems or containers. They are commonly used in HVAC systems, refrigeration units, vacuum packaging machines, and other applications where the removal of air or gases is necessary.
6. Analytical Instruments
Many analytical instruments, such as mass spectrometers, electron microscopes, and gas chromatographs, require high vacuum levels for accurate measurements and analysis. Double stage vacuum pumps provide the necessary vacuum environment for these instruments to operate efficiently.
7. Freeze Drying
Freeze drying, also known as lyophilization, is a process used in the pharmaceutical and food industries to preserve perishable materials by removing moisture. Double stage vacuum pumps assist in creating the necessary low-pressure environment for freeze drying, allowing moisture to sublimate directly from the frozen state to a vapor, preserving the integrity of the material.
These are just a few examples of the numerous applications of double stage vacuum pumps. Their ability to achieve high vacuum levels, efficient pumping speeds, and vapor handling capabilities make them indispensable in various industries where vacuum systems are required.
Benefits
Double stage vacuum pumps offer several benefits over single-stage pumps, including:
1. Higher Vacuum Level
The primary advantage of a double stage vacuum pump is its ability to achieve a higher level of vacuum. By utilizing two stages of compression, it can effectively remove more gas molecules from the system, resulting in a deeper vacuum. This is particularly beneficial in applications where an extremely low pressure or high level of vacuum is required.
2. Improved Pumping Efficiency
The two-stage design of these pumps allows for improved pumping efficiency. The low vacuum stage removes the bulk of the gas, while the high vacuum stage further compresses the remaining gas molecules. This division of work between the stages enhances the overall performance and reduces the load on each stage, resulting in more efficient operation.
3. Faster Pumping Speed
Double stage vacuum pumps typically offer higher pumping speeds compared to single-stage pumps. The combined action of the two stages allows for faster removal of gas molecules from the system, reducing the time required to reach the desired vacuum level. This is particularly advantageous in applications that involve large volumes or require rapid evacuation.
4. Enhanced Vapor Handling
Double stage pumps are well-suited for handling vapors or condensable gases. The initial low vacuum stage helps to remove the bulk of the vapors, preventing them from reaching the high vacuum stage where they can cause issues like condensation or damage to the pump. This makes double stage vacuum pumps suitable for applications that involve volatile substances or processes.
5. Wide Range of Applications
Double stage vacuum pumps find applications in various industries and fields. They are commonly used in laboratories, research facilities, pharmaceutical manufacturing, semiconductor manufacturing, vacuum coating, vacuum packaging, and many other industries that require precise control over pressure and a high level of vacuum.
Overall, the benefits of a double stage vacuum pump include achieving a higher vacuum level, improved pumping efficiency, faster pumping speed, enhanced vapor handling capabilities, and suitability for a wide range of applications. These advantages make double stage vacuum pumps a preferred choice in situations where a robust and efficient vacuum system is essential.
Q1: What Is the Difference Between a Single-stage and a Double-stage Vacuum Pump?
A1: The main difference between a single-stage and a double-stage vacuum pump is the number of pumping stages involved in the compression process. A single-stage pump has only one set of rotating vanes that compress the gas molecules, while a double-stage pump has two sets of vanes. The double-stage pump offers higher pumping efficiency and can achieve a deeper vacuum compared to a single-stage pump.
Q2: How Does a Double-stage Vacuum Pump Work?
A2: A double-stage vacuum pump works by using two stages of compression to create a vacuum. The first stage, known as the low vacuum stage, removes the majority of the gas molecules from the system by compressing them against the walls of the pump. The partially evacuated gas is then transferred to the second stage, the high vacuum stage, where it undergoes further compression to achieve a higher level of vacuum.
Q3: What Are the Advantages of Using a Double-stage Vacuum Pump?
A3: The advantages of using a double-stage vacuum pump include:
- Higher vacuum level: Double-stage pumps can achieve a deeper vacuum compared to single-stage pumps.
- Improved pumping efficiency: The two-stage design enhances overall pumping efficiency.
- Faster pumping speed: Double-stage pumps offer higher pumping speeds, reducing evacuation time.
- Enhanced vapor handling: They are effective at handling vapors and condensable gases.
- Wide range of applications: Double-stage pumps find uses in various industries and fields that require a high level of vacuum.
Q4: What Are the Common Applications of Double-stage Vacuum Pumps?
A4: Double-stage vacuum pumps are commonly used in laboratories, research facilities, manufacturing processes, vacuum coating, vacuum furnaces, analytical instruments, and freeze drying. They are employed in tasks such as vacuum drying, degassing, filtration, vacuum packaging, surface coating, heat treatment, mass spectrometry, and freeze drying.
Q5: Can a Double-stage Vacuum Pump Handle Liquids?
A5: Generally, double-stage vacuum pumps are not designed to handle liquids directly. Their primary purpose is to remove gases and create a vacuum. Handling liquids can cause damage to the pump or affect its performance. If liquid removal is required, additional components like condensers or separators are used in conjunction with the vacuum pump to prevent liquid from entering and damaging the pump.
Specifications
Figures below are the manufacturer data for this model. Anything not listed is confirmed in writing with the quotation rather than estimated here.
| Model | 2RS-0.5 | 2RS-1 | 2RS-1.5 | 2RS-2 | 2RS-3 | 2RS-4 | ||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Voltage | 110V | 220V | 110V | 220V | 110V | 220V | 110V | 220V | 110V | 220V | 110V | 220V |
| 60Hz | 50Hz | 60Hz | 50Hz | 60Hz | 50Hz | 60Hz | 50Hz | 60Hz | 50Hz | 60Hz | 50Hz | |
| Pumping speed(CFM) | 2 | 1.5 | 3 | 2.5 | 4 | 3.5 | 5 | 4.5 | 7 | 6 | 12 | 10 |
| Limiting pressure | 3*10-1Pa | 3*10-1Pa | 3*10-1Pa | 3*10-1Pa | 3*10-1Pa | 3*10-1Pa | ||||||
| Speed(rpm) | 3500 | 2800 | 3500 | 2800 | 3500 | 2800 | 3500 | 2800 | 3500 | 2800 | 3500 | 2800 |
| power(HP) | 1/4 | 1/4 | 1/3 | 1/2 | 3/4 | 1 | ||||||
| Oil consumption(ML) | 250 | 250 | 330 | 330 | 370 | 500 | ||||||
| Overall dimensions(MM) | 260*110*240 | 275*115*240 | 290*120*240 | 310*125*255 | 360*135*270 | 430*142*280 | ||||||
| Weight(KG) | 7 | 7.5 | 9.5 | 10 | 13 | 19 |
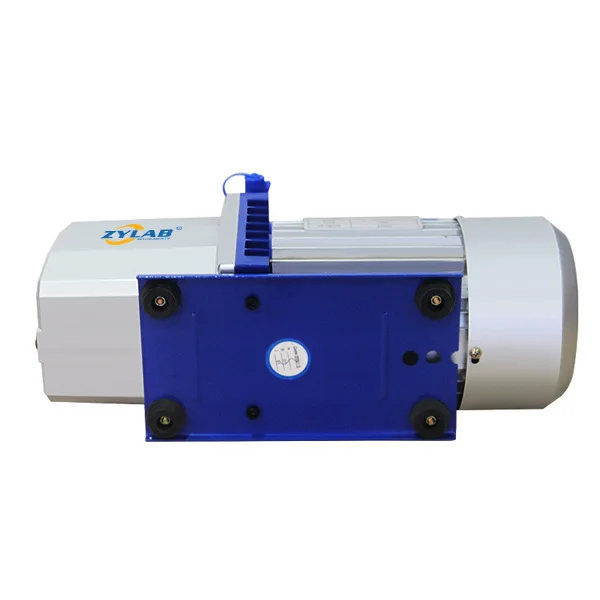
Double Stage Vacuum Pump In Detail
Processes This Unit Supports
These are the applications ZYLAB lists this model under. Each link opens the full equipment set for that process, which is useful when a project needs more than one machine.
Who Orders It
Fields this model already works in, plus what ZYLAB puts behind it: a 2-year warranty on most products, glass excluded, spare parts in stock and free application support by WhatsApp or email.
- University and institute research laboratories
Related Projects
Related Equipment
Models from the same family and the same processes, in case a different chamber size or temperature range fits better.
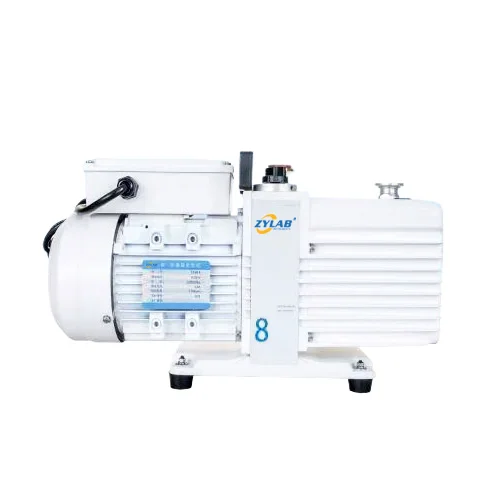
High-Performance Two-Stage Rotary Vane Vacuum Pump for Laboratory
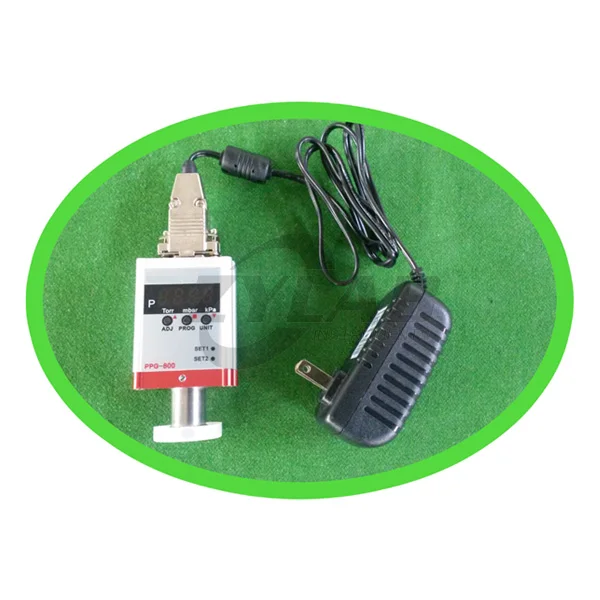
High-Precision Digital Vacuum Gauge
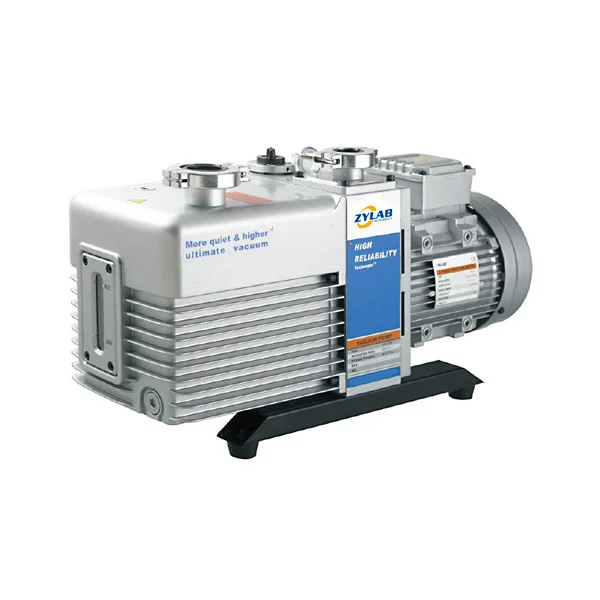
High-Speed Direct-Coupled Lab Mechanical Vacuum Pump – 5×10⁻² Pa Ultimate Pressure
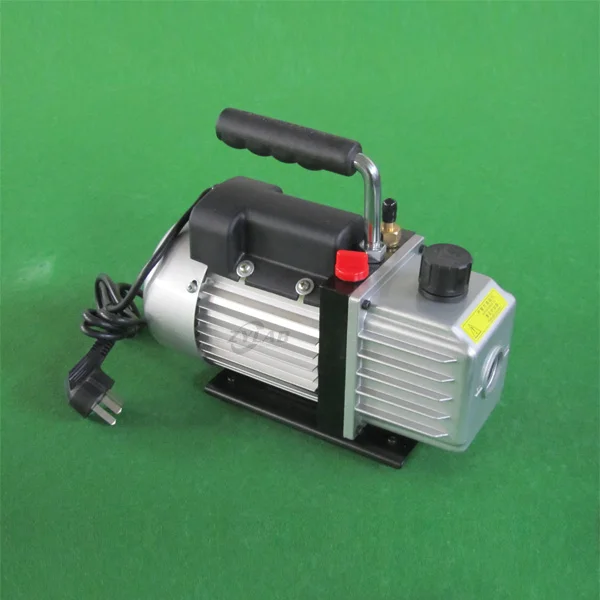
Lab 10pa Direct-Drive Rotary Vane Vacuum Pump for Tube Furnace
4.4 × 10⁻³ Pa High Vacuum System Molecular Pump Unit
Rotary Vane Vacuum Pump for Vacuum Glove Box
MP-401 Top Quality Diaphragm Vacuum Pump with Special Filter
GM-2 High Speed 4cfm Diaphragm Vacuum Pump
Ordering Double Stage Vacuum Pump
What is Double Stage Vacuum Pump typically used for?
A double stage vacuum pump is a type of pump designed to create a vacuum by removing gas or air molecules from a sealed chamber or system. It consists of two stages or sets of rotating vanes, which work together to increase the efficiency and achieve a higher
What warranty comes with Double Stage Vacuum Pump?
Most ZYLAB products carry a 2-year warranty, glass components excluded; the exact term for this model is the one printed in its specification table and repeated on the quotation. Within the warranty period any part that fails through no misuse of your own is replaced free of charge.
Can we get technical help before ordering Double Stage Vacuum Pump?
Yes, and it is free. Our technical staff help with model selection, troubleshooting, manuals and application questions whether or not you have ordered from us before. Write to [email protected] or message us on WhatsApp.
Which shipping methods do you use?
Sea freight for consignments over about 60 kg (11-30 days to North America, 25-33 days to Europe, 7-20 days to Southeast Asia), air freight to airport in roughly 7-10 days, and DHL, FedEx or UPS door to door in about 5-7 days for small urgent items.
How can we pay for Double Stage Vacuum Pump?
Bank (wire) transfer, letter of credit for larger orders, major credit and debit cards, and PayPal. Bank details are printed on the invoice; send us the transfer confirmation and we start processing straight away.
Quote For Double Stage Vacuum Pump
Tell us the sample, the temperature and the atmosphere. You get the configuration, the price and the despatch date in one reply.