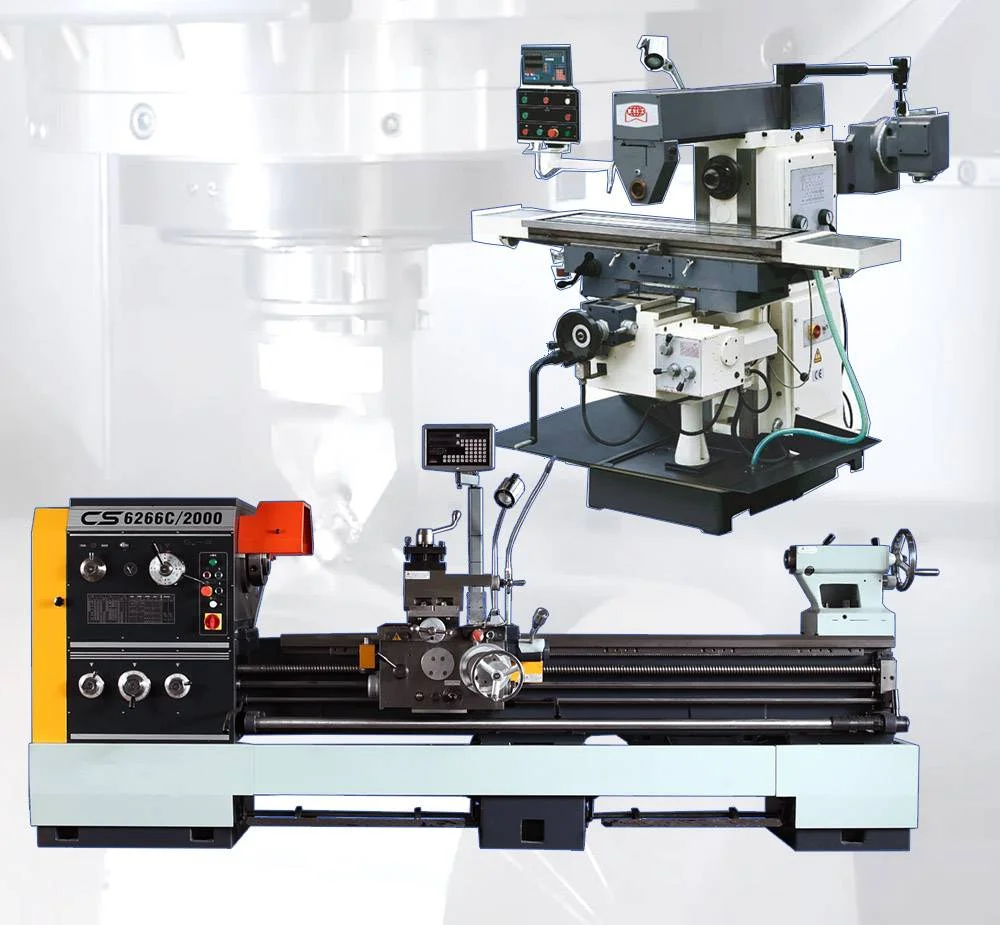
7 machines
Metal Processing Machinery
Chip-removal machine tools for turning, milling, drilling, grinding, boring, sawing and EDM work.
Shaanxi Jiade Group Co., Ltd
Metal processing and forming machinery from Xi'an, China, selected model by model against the workpiece you actually run.
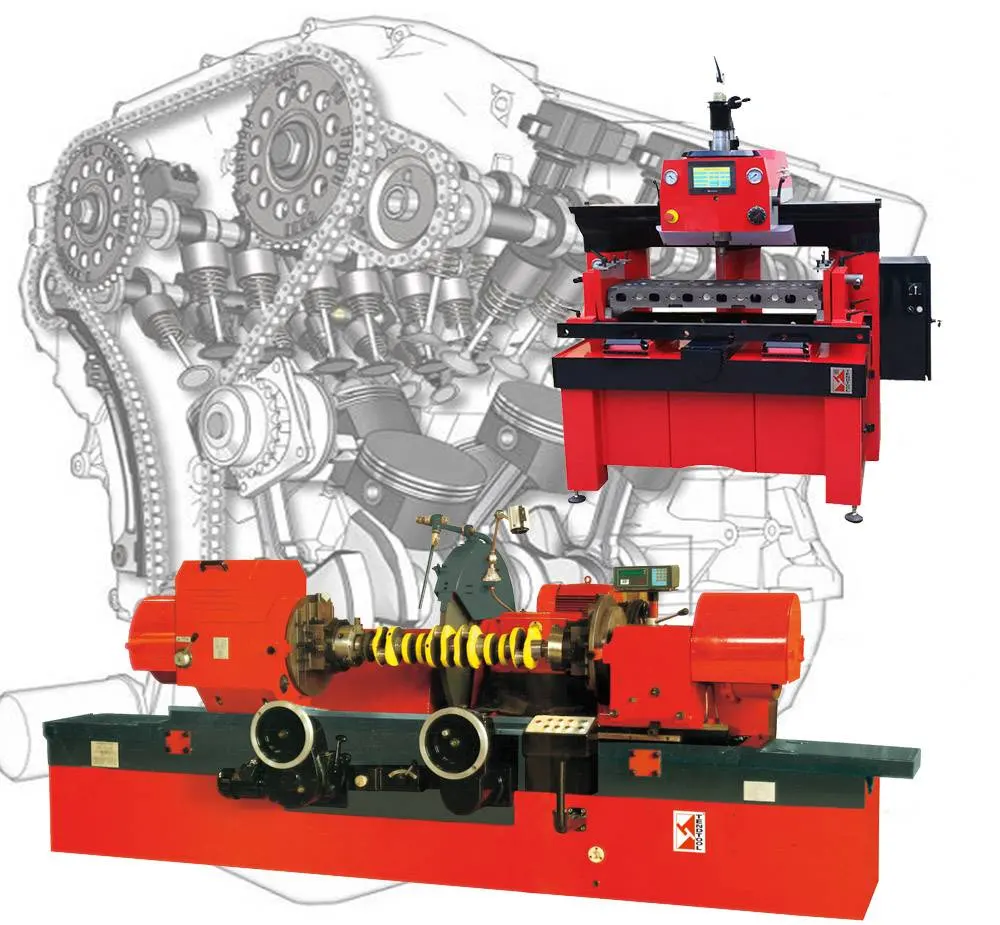
Shaanxi Jiade Group Co., Ltd
Boring, honing, crankshaft grinding and valve seat machines that let a workshop machine an engine instead of scrapping it.
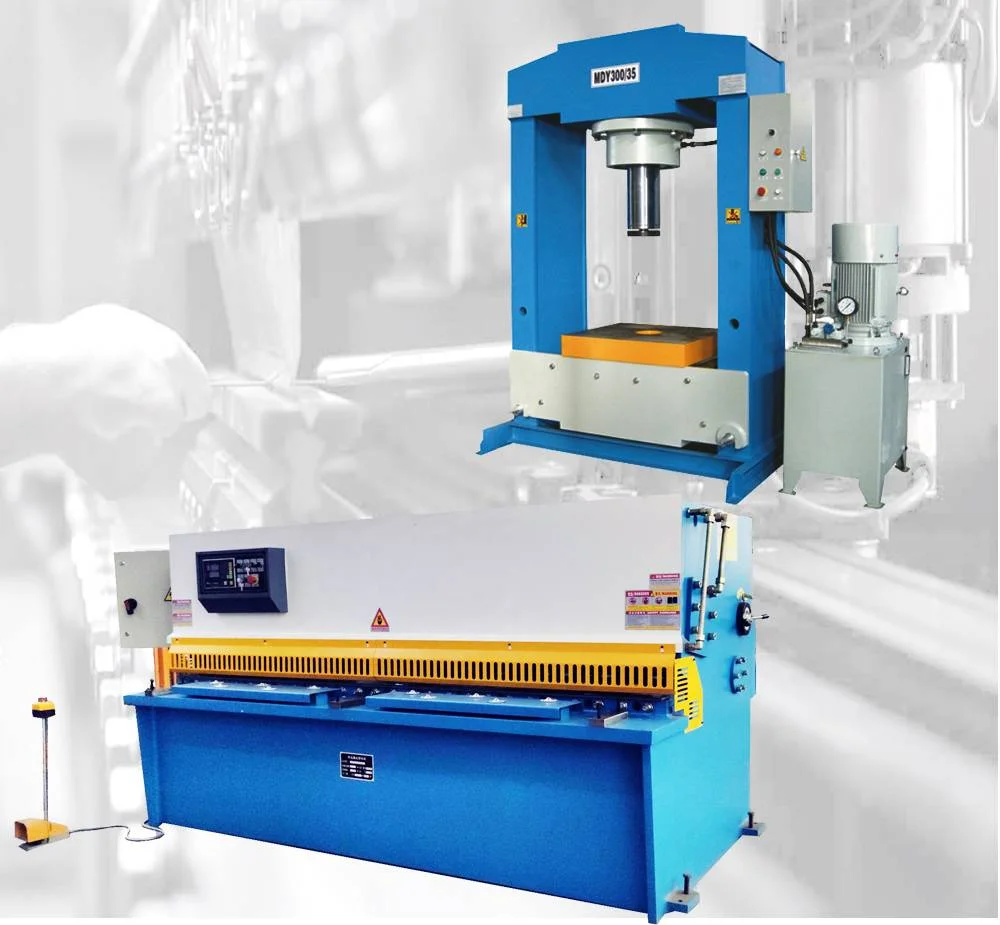
Shaanxi Jiade Group Co., Ltd
Shears, press brakes, plate rolls and laser cutters sized to the plate thickness on your shop floor.
Shaanxi Jiade Group Co., Ltd
Tyre changers, wheel balancers and fluid handling equipment for workshops that turn bays around fast.
What We Make
Every range below is a live part of the catalogue with published parameters, not a placeholder category.
Chip-removal machine tools for turning, milling, drilling, grinding, boring, sawing and EDM work.
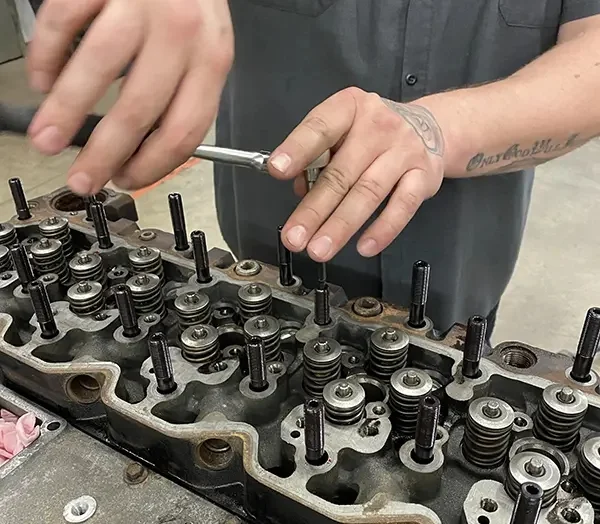
Engine rebuilding machinery and garage service equipment for workshops that repair rather than replace.
Pastillators and process equipment for sulfur and similar granulation lines.
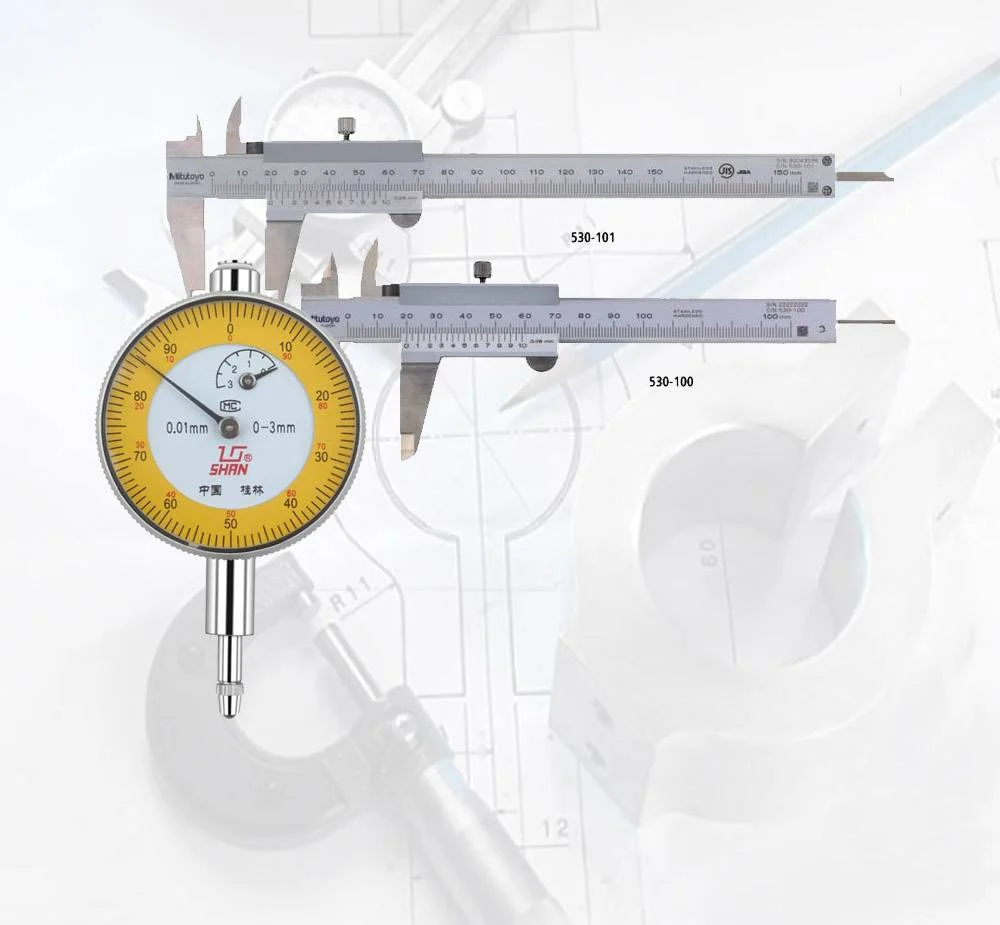
Micrometers, bore gauges, vernier calipers and magnetic stands used to verify the work these machines produce.
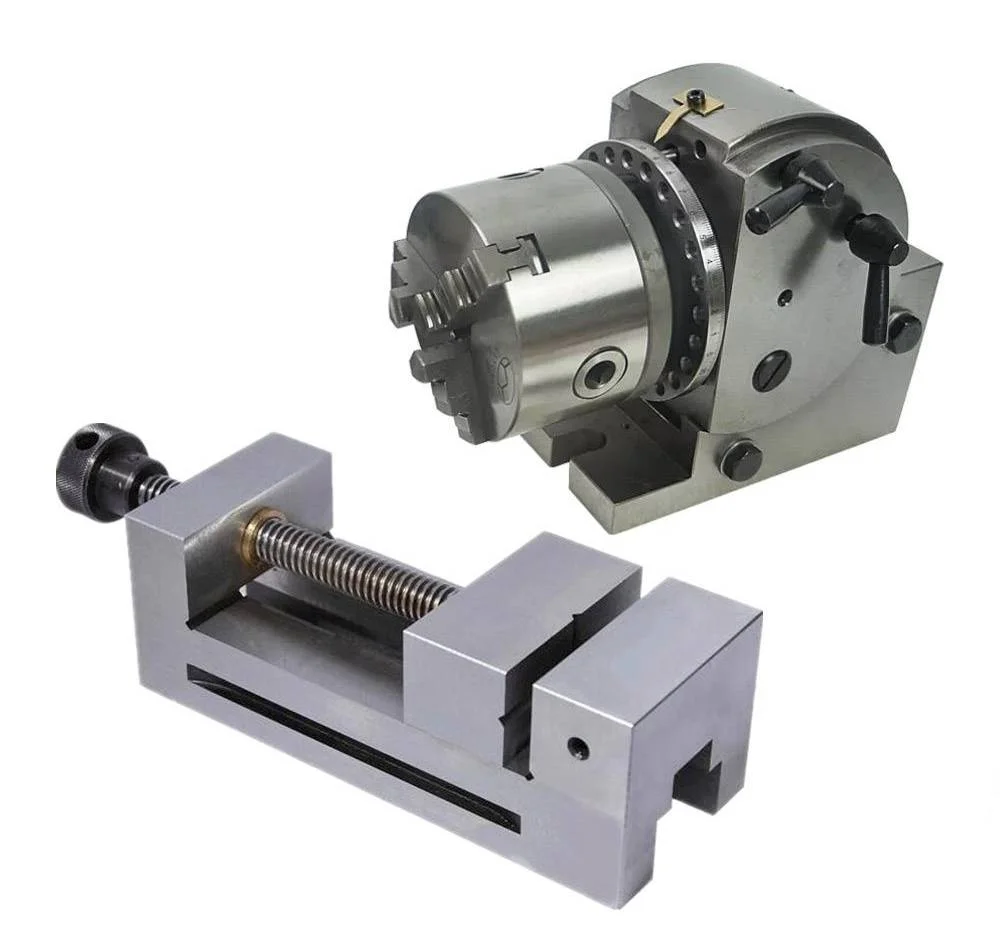
Chucks, arbors, vises, fans and spare parts that keep installed machines running.
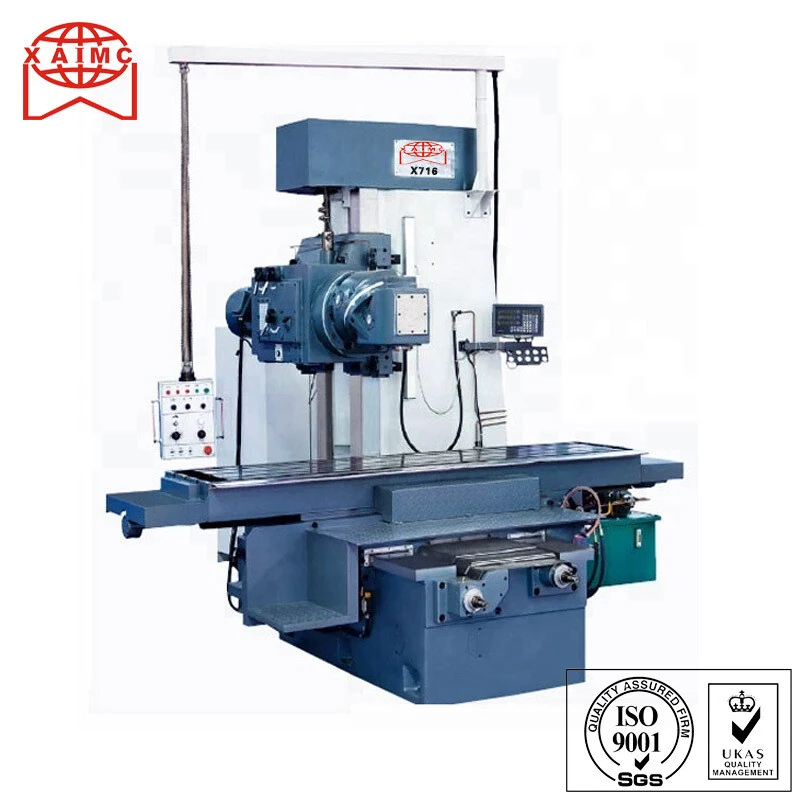
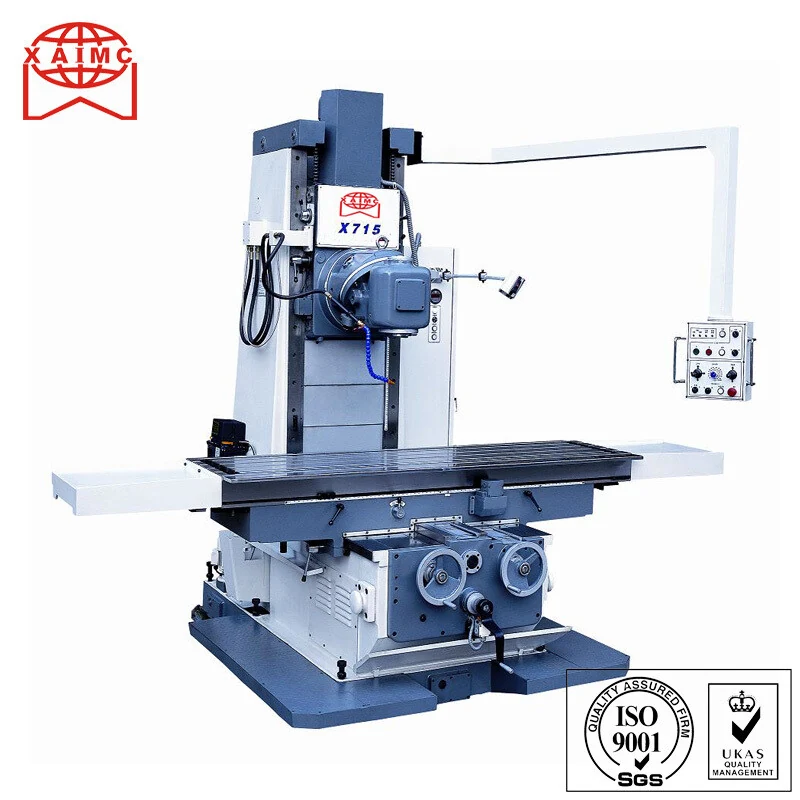
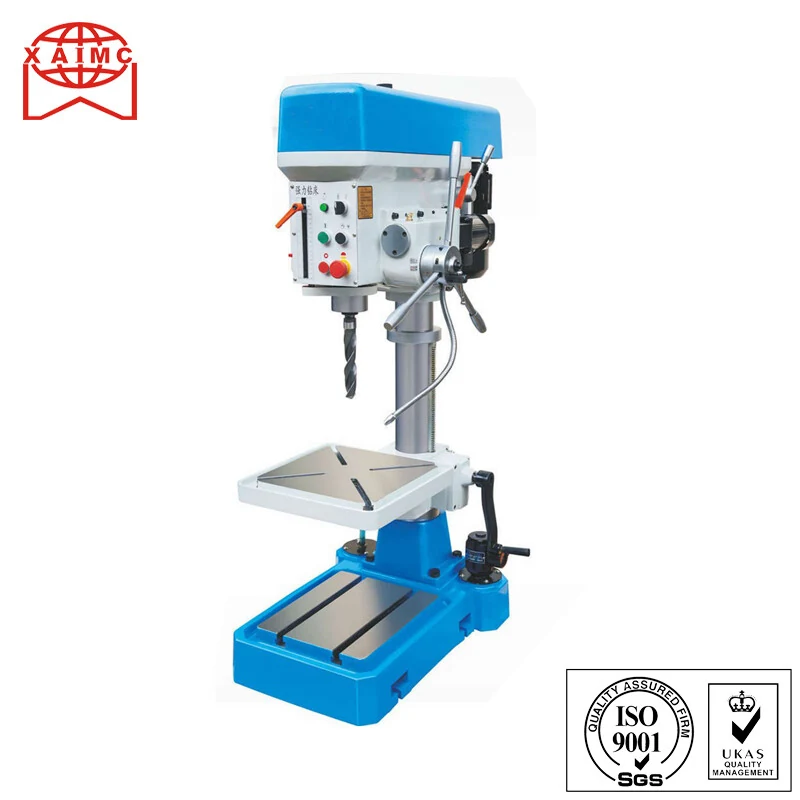
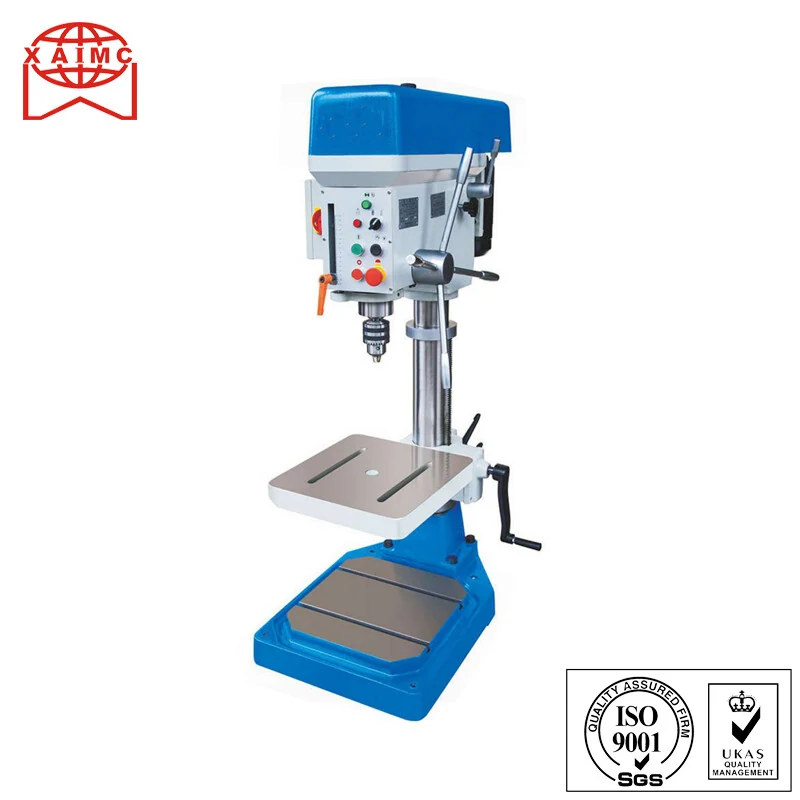
Featured Machines
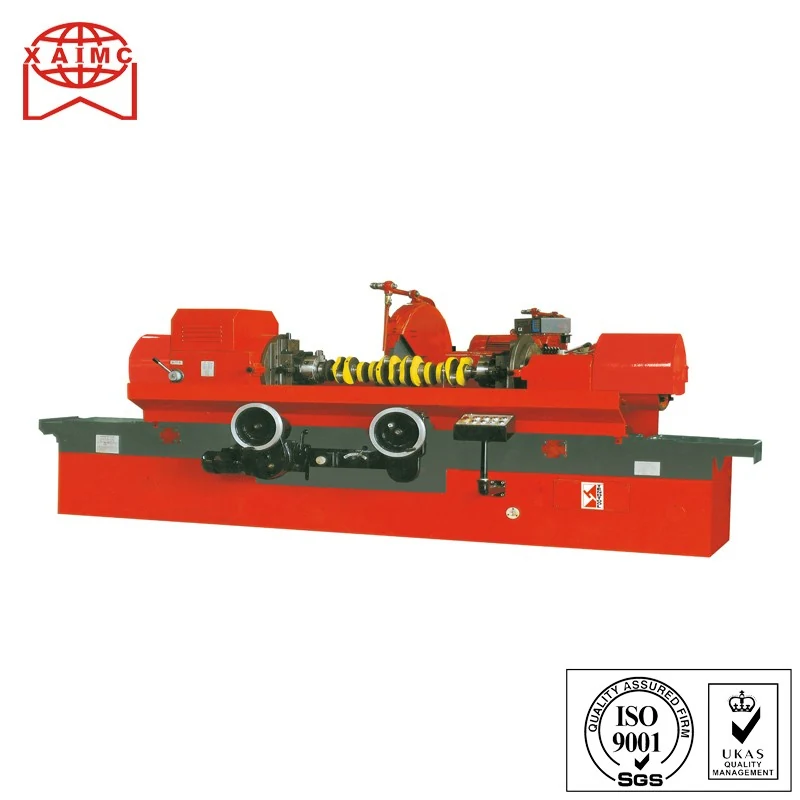
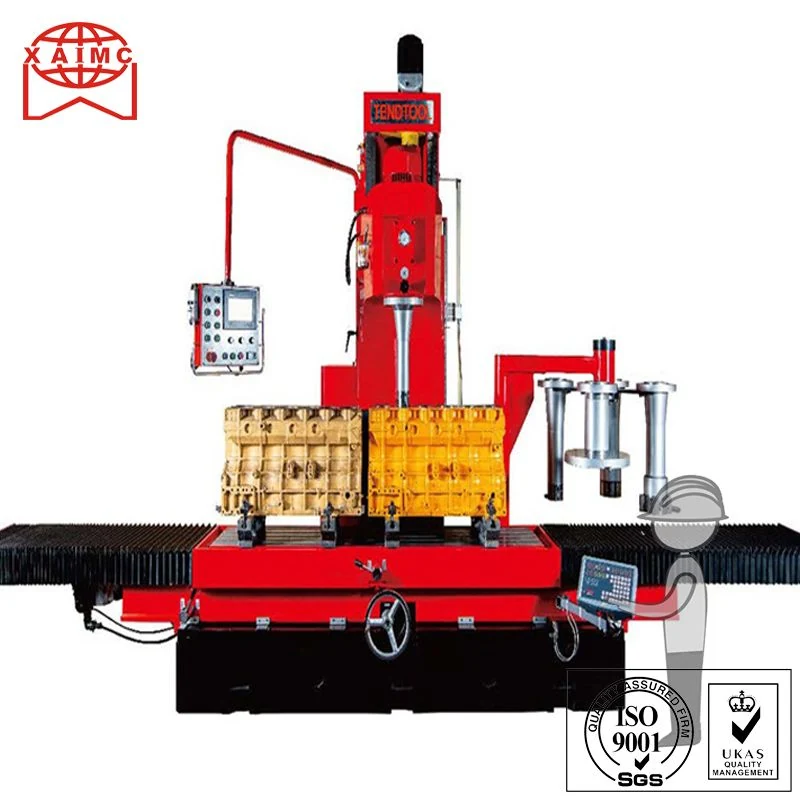
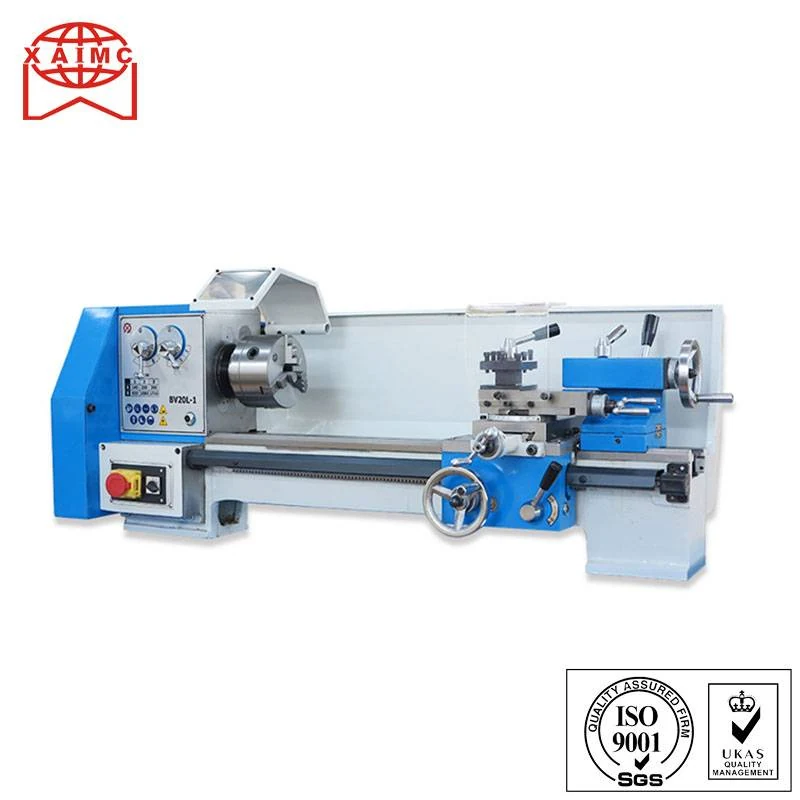
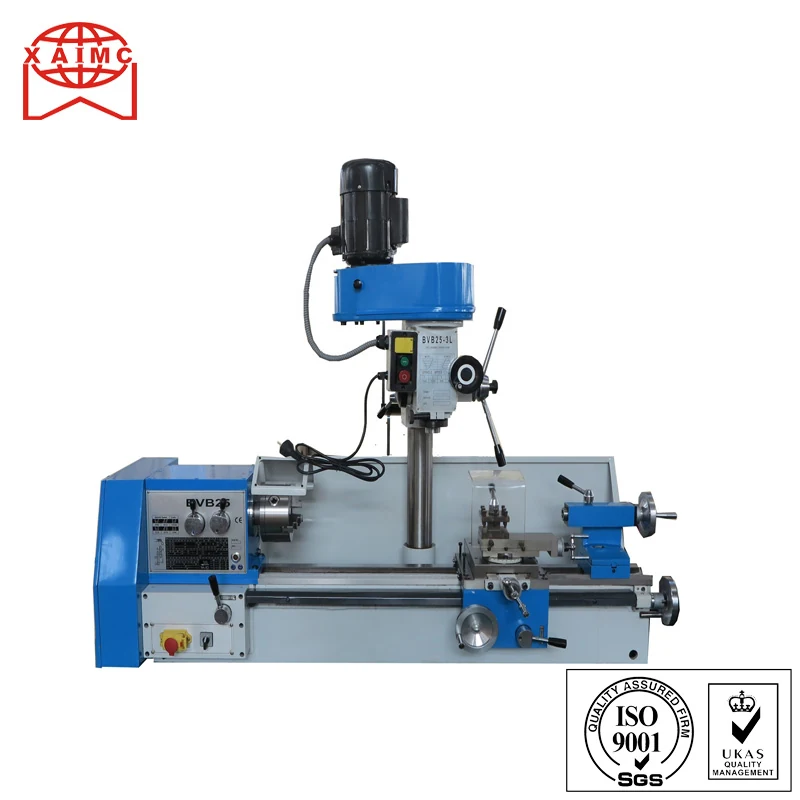
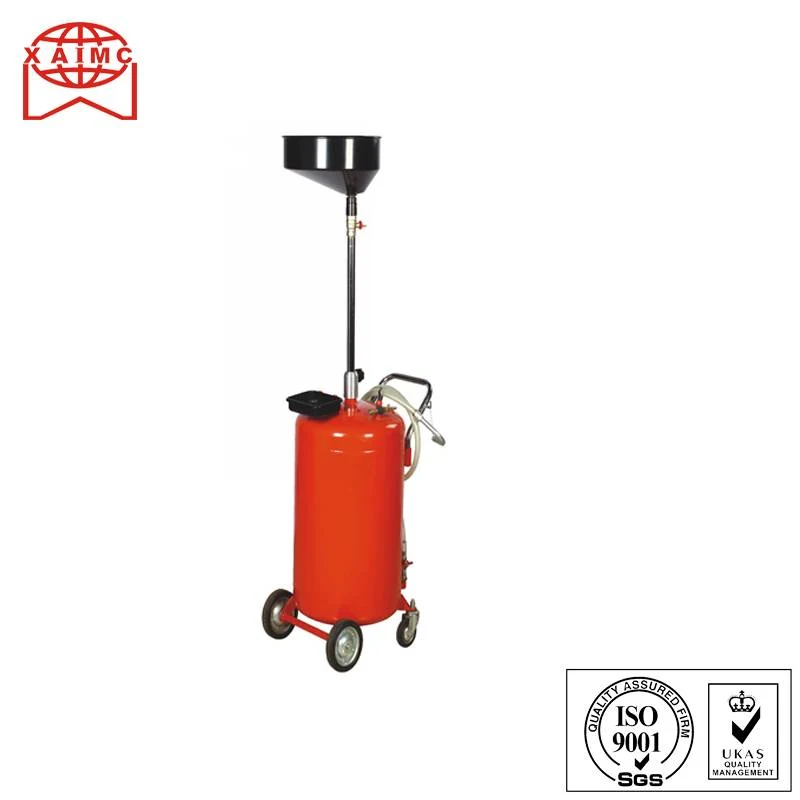
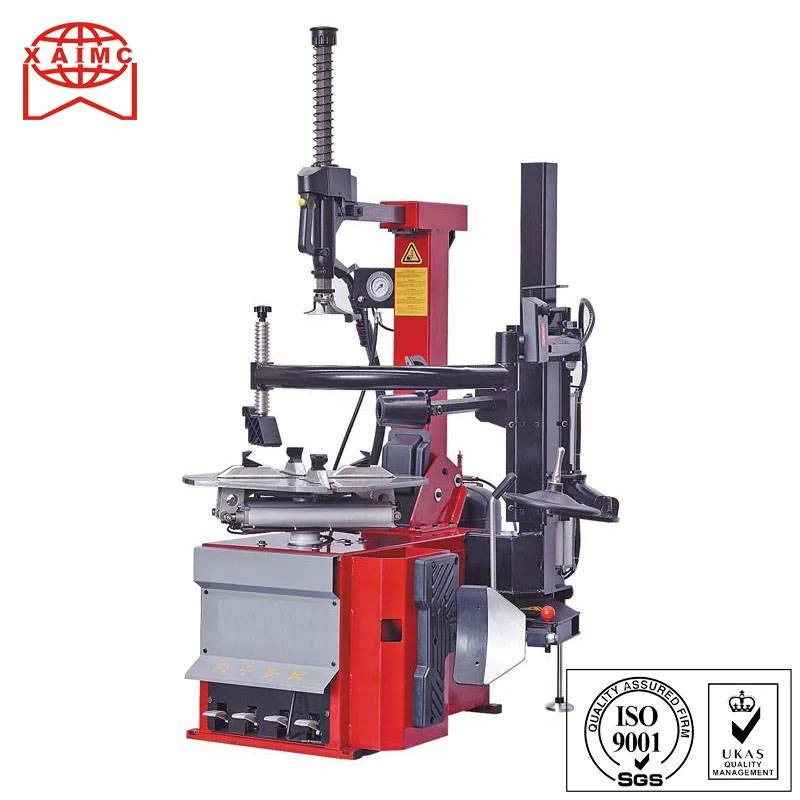
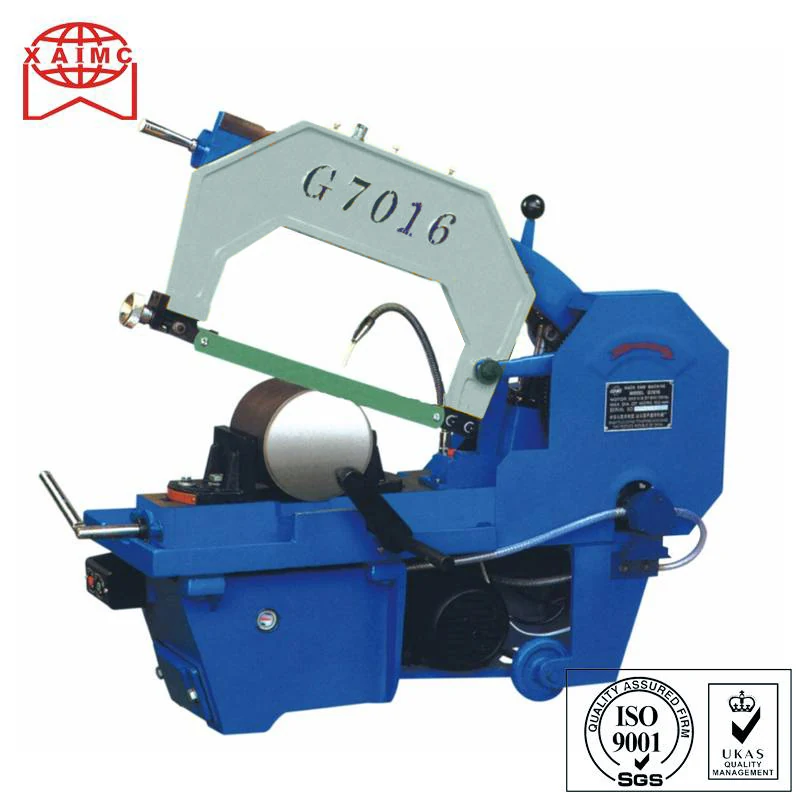
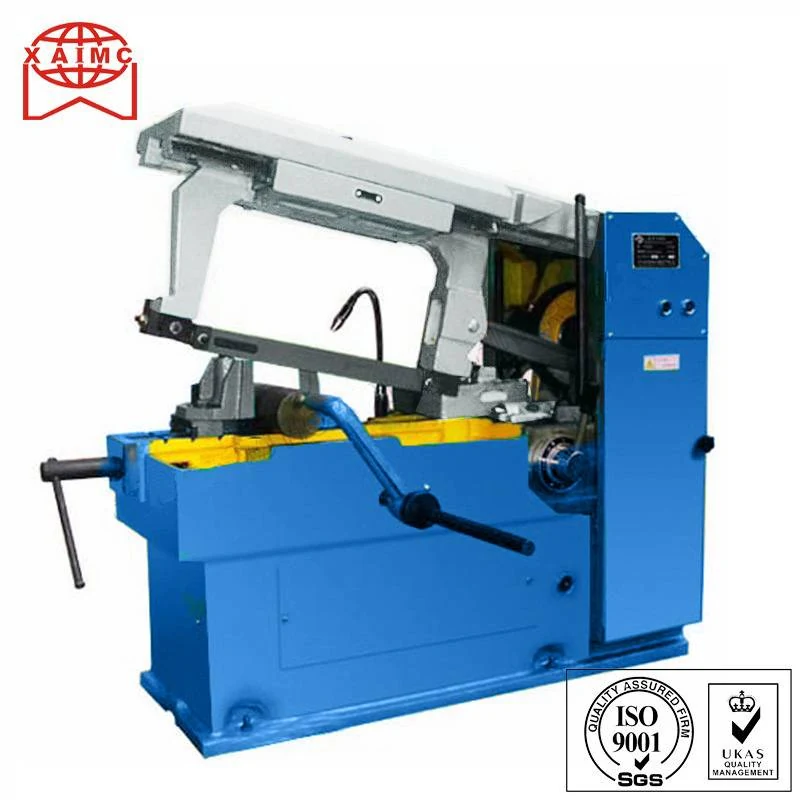
Each card links to the full parameter table, application notes and a direct WhatsApp line for that model.
Who We Serve
Workshops that machine cylinder heads, blocks, crankshafts and valves instead of replacing them.
Read the industry page →Service bays handling tyres, wheels, brakes and fluid work for commercial and passenger vehicles.
Read the industry page →Job shops turning, milling, drilling and grinding to drawing for local industry.
Read the industry page →Fabricators cutting, bending and rolling sheet and plate into panels, enclosures and ducting.
Read the industry page →Shops producing spur gears, helical gears and worm wheels for gearboxes and drives.
Read the industry page →Plant maintenance teams keeping installed machinery running instead of buying new.
Read the industry page →What Problem We Solve
A job goes elsewhere because one process is missing in house. Adding the machine that closes the gap usually pays back faster than subcontracting it for another year.
Gears, bushings and shafts for older machinery are no longer supplied. Turning, hobbing and slotting equipment lets you make the part instead of waiting for an import.
Without boring, honing and grinding capacity a repairable engine becomes scrap. A rebuilding line keeps that work and its margin in your workshop.
Used imports arrive with no manual, no spares and no one to call. We supply new machines with documentation and a named contact.
Micrometers, bore gauges and stands turn a finished part into a measurable one, which is what your own customers audit.
Workholding and spares sourced from a different supplier each time. Our accessories range is matched to the machines we ship.
Why Customers Choose Us
Figures above are taken from our own company records. Certification scope, export country count and per model tolerance data are marked TBC on this site until documents are attached rather than estimated.
Inside the Group
The group runs an R and D department, production and assembly workshops, an inspection department, a paint house and a store, so a machine is designed, cut, assembled, painted and checked in the same plant.
Models are updated from customer feedback rather than left unchanged for a decade.
Beds, columns and spindles are machined in house on conventional and CNC equipment.
Parts pass inspection before assembly and painting, which is where most import complaints start.
Solutions
Most enquiries are about a process, not a model number. These pages list which machines cover which process end to end.
A machine list that covers a cylinder head and block from strip-down to final assembly.
See the machine list →Cutting, bending and rolling equipment sized to the plate thickness you actually run.
See the machine list →The four processes a general job shop needs before it can quote most local work.
See the machine list →Tyre, wheel and fluid handling equipment for commercial vehicle service.
See the machine list →Chucks, arbors, vises and measuring equipment matched to the machines you run.
See the machine list →Knowledge Centre
Swing, centre distance, spindle bore and drive type decide whether a lathe fits your work. Here is how to read those four figures before you compare prices.
ComparisonBench, upright, gear head and radial drilling machines differ by how the work gets under the spindle. That single question usually settles the choice.
Process GuideBoring sets the diameter, honing sets the surface. A rebuild that skips the distinction ends up with a bore that measures right and still burns oil.
ComparisonCarbide seat cutting and stone grinding both produce a sealing seat. They differ in concentricity, repeatability and how much operator skill sits between you and a leak.
Process GuideTwo numbers decide whether a press brake can make your part: the tonnage the bend needs and the allowance the bend consumes. Both can be worked out before you buy.
Buying GuideBlade speed, feed force and how the material is clamped decide cut quality and blade life. Machine class follows from how much you cut, not from what you cut.
Answers
In the group's own plant in Xi'an, Shaanxi, China. Shaanxi Jiade Group Co., Ltd was founded in 2003 and moved to Sanqiao Industrial Park, Xi'an Economic and Technological Development Zone in 2007, where the site covers 38 acres with more than 15,000 square metres of built area.
A single machine is a normal order. Several models also combine well in one container, which is how most workshop packages ship.
Message the WhatsApp number on this page with the model code or a description of the work. Quotations include the machine specification, packing, and the shipping term you ask for.
FOB, CFR, CIF on the trade side. Payment is TT 30% with order and 70% before shipment, or irrevocable L/C at sight.
Our machines have been exported worldwide, and the group exports more than 30,000 sets a year across its product lines. The exact country list and any local certification requirement is confirmed per enquiry rather than claimed here.
TBC. Certificate scope differs by model and destination, so we attach the documents that apply to the model you are buying instead of publishing a blanket claim.
Send a drawing, a part photograph or a model code. You get a specification and a price, not a brochure.