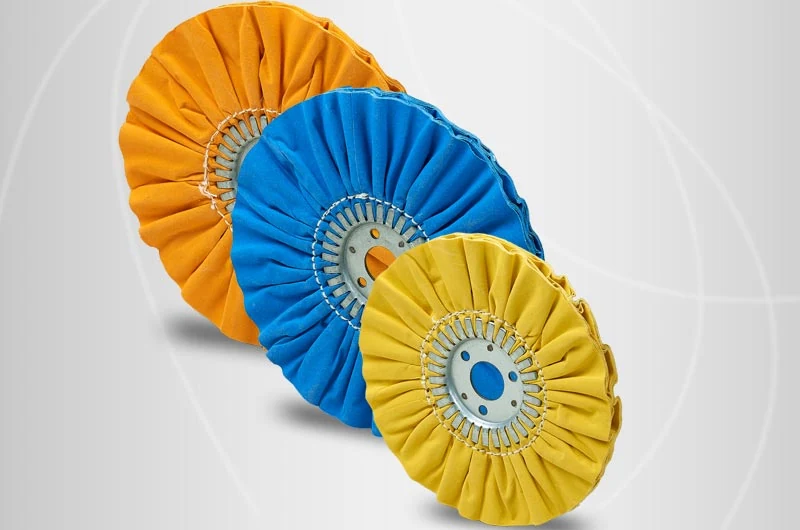
Airway/Ventilated Cotton Buffs (with Plate)
The Airway/Ventilated Cotton Buffs (with plate) are formed using the CRA-800 Bias Airway Buffs Forming Machine, which takes prepared cotton fabric and an iron plate centre to create ventilated wheel bodies. These wheels are used in metal finishing, cookware, tableware and sanitary ware polishing...
Product Overview
The Airway/Ventilated Cotton Buffs (with plate) are formed using the CRA-800 Bias Airway Buffs Forming Machine, which takes prepared cotton fabric and an iron plate centre to create ventilated wheel bodies. These wheels are used in metal finishing, cookware, tableware and sanitary ware polishing lines. The machine supports outer diameters from 200 mm to 600 mm and allows the operator to produce consistent, repeatable wheel shapes. The formed body is then pressed on the CRA-600 and trimmed on the CRA-700 to complete the wheel. This process replaces manual folding and ensures uniform ply spacing across production runs.
Key Benefits
- One operator replaces multiple hand workers on the forming step
- Consistent ply spacing across all wheels reduces finish variation
- Supports 200 to 600 mm outer diameters for standard industrial polishing wheels
- Runs untreated cotton, pink, yellow, orange, and blue treated cotton fabric
- Uses iron plate centres with round or hexagon holes for compatibility with existing tooling
- Machine interface and control panel are in English for clear operation
Application Scenarios
- A polishing shop replacing hand-formed cotton buffs with a repeatable machine process
- A manufacturer adding ventilated cotton buffs to their product range for cookware or sanitary ware
- A factory already using the CRA-800 for sisal wheels wanting to switch to cotton fabric
- A distributor producing their own cotton buffs in-house to reduce import lead time and freight
Who It Is For
- Buffing and polishing wheel manufacturers
- Metal finishing shops using cotton buffs in volume
- Cookware, tableware and sanitary ware polishing lines
- Distributors sourcing cotton buffs with local production flexibility
Problems It Solves
- Manual folding of cotton fabric leads to inconsistent ply spacing and uneven wear
- Hand forming limits daily output and requires multiple workers per shift
- Importing finished cotton buffs adds freight cost and delivery delays
- Changing wheel diameter by hand requires retraining rather than a tool change
Technical Features
- Hydraulic system with left and right cylinders for trestle and turntable movement
- Left and right upper clamps hold the fabric stack during indexing
- Control panel with circuit board and pressure gauge for consistent operation
- Turntable indexes between folds to maintain repeatable ply spacing
- Cutter section trims the formed body before unloading
- Adjustable batching speed to handle soft untreated cotton and harder treated fabrics
Specifications
| Model | Airway/Ventilated Cotton Buffs (with plate) |
|---|---|
| RPM of Batching | Adjustable |
| Max Buff Diameter | 600 mm |
| Min Buff Diameter | 200 mm |
Values taken from the manufacturer data for this model. Anything not listed is confirmed on request before order.
Materials
- Pure cotton fabric
- Flannel fabric
- Yellow treated fabric for buffing
- Pink, orange, blue treated cotton fabric
- Iron plate centres with round hole or hexagon hole
- Square teeth steel ring or iron claw for airway buffs
Manufacturing And Process
Step 1
Prepare cotton fabric on a CRA-500 bias cutting and rolling machine or equivalent
Step 2
Load the fabric roll and select the iron plate centre for the wheel
Step 3
Set the batching speed and clamp set for the target outer diameter
Step 4
The turntable indexes and hydraulic cylinders fold and clamp each ply onto the centre
Step 5
The formed body is trimmed and unloaded, then sent to pressing on a CRA-600
Step 6
Edge trimming on a CRA-700 gives the finished wheel its running face
Quality Control
- Hydraulic pressure maintained at 7 MPa on both moulding and finishing for consistent ply density
- Sample wheels formed and checked before shipment
- Free sample testing available on the buyer's own fabric before purchase
- Installation and operation training provided to ensure first production run is supervised
Customization Options
- Voltage and phase configured for the destination market
- Clamp sets supplied for the diameter bands the buyer actually sells
- Iron plate tooling matched to the buyer's existing centres
- Machine can be quoted as part of a CRA-500, CRA-800, CRA-600, CRA-700 line
Compared With The Alternatives
| CRA-300 Airway Buffs Forming Iris Machine | The CRA-300 covers 100 to 250 mm wheels; use it for small jewellery or bench grinder buffs, not for 200 to 600 mm industrial wheels |
|---|---|
| CRA-360 Airflow Corrugated Buffs Making Machine | The CRA-360 forms corrugated or weave structure buffs, a different wheel type not suitable for ventilated cotton buffs |
| Manual airway wheel forming | Hand forming requires no capital investment but cannot maintain consistent ply spacing or reach 5000 pieces per day |
Use Guide
- Confirm incoming cotton fabric is cut on the bias before forming; straight cut material will not fold evenly
- Change the clamp set to adjust diameter band; a set change takes about the same effort as a tooling swap and is not a daily operation
- Maintain hydraulic pressure at 7 MPa; a drop indicates loose ply spacing before it affects wheel diameter
- Send formed bodies to pressing the same shift to prevent ply stack relaxation
- Contact us on WhatsApp for the English operation video if the operator is new to airway forming
Airway/Ventilated Cotton Buffs (with Plate) FAQ
What diameter of cotton buffs can this machine make?
From 200 mm to 600 mm outer diameter. For 100 to 250 mm wheels use the CRA-300 iris machine instead.
How many people are needed to run it?
One operator. The clamping, indexing, and trimming are handled by the machine's hydraulic and control system.
What is the daily output?
Up to 5000 pieces per day at maximum rate. Real output depends on diameter, ply count, and material type.
Do I need other machines to make a finished wheel?
Yes. Bias fabric preparation comes before forming, and pressing and edge cutting come after. We supply the CRA-500, CRA-600, and CRA-700 for those steps.
What is the lead time?
5 to 15 workdays if the machine is in stock, otherwise 15 to 60 workdays depending on quantity and model.
What are the payment terms?
Orders up to 10000 USD are 100% in advance. Above 10000 USD it is 30% T/T deposit with the balance before shipment.
Can you test my own fabric before I buy?
Yes, sample testing is free. You cover the freight and send the specific material you plan to run.


Lines Industries And Guides
Airway Buff Production Line
A full ventilated airway buff line from fabric roll to finished wheel. The process starts with bias cutting, slitting and rolling...
Buff Raw Material Supply
CRATOOLS supplies raw materials for buffing wheel production from the Qingyuan buffing polish materials production base. The...
Choosing a Buffing Wheel Centre Iron Claw or Iron Plate
Guide
Get A Price On The Airway/Ventilated Cotton Buffs (with Plate)
Send the quantity, the diameters and the material you run. We answer with price, lead time and packing within 24 hours.