Fiber Laser Cutting Machines
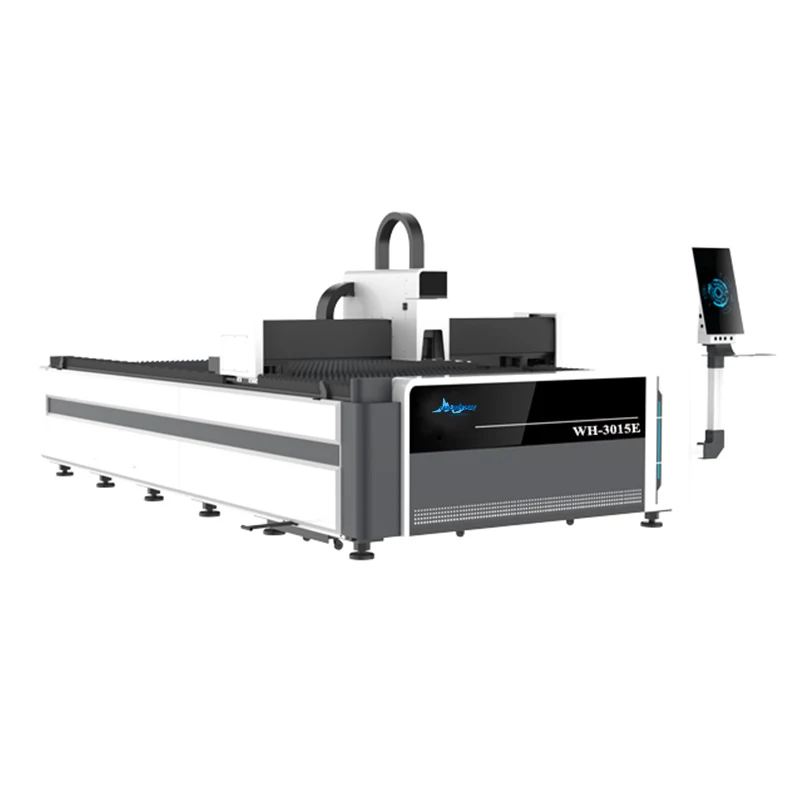
3015 E 3000w Fiber Laser Cutting Machine
The WH-3015E is a single-platform fiber laser cutter with a 1500 x 3000 mm rated sheet size and a laser source selectable at 1500 W, 2000 W or 3000...
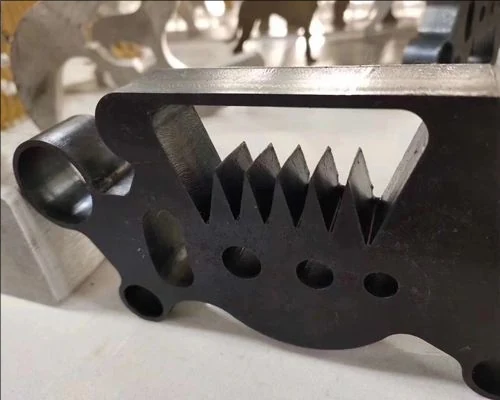
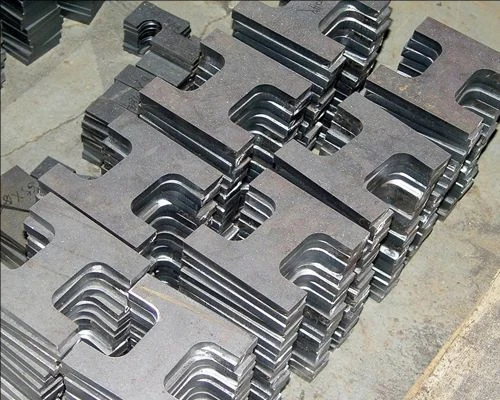
Brackets in this thickness range were being cut on plasma and then ground by hand before welding. Every geometry change meant new nesting and more grinding time, and hole positions were not repeatable enough for the assembly jig, so parts...
A typical buyer for this application is a sheet metal subcontractor supplying brackets and mounting plates to agricultural and construction machinery builders. Order sizes run from tens to a few hundred pieces, the plate mix sits between 3 mm and 14 mm carbon steel, and the drawing changes with almost every purchase order.
Brackets in this thickness range were being cut on plasma and then ground by hand before welding. Every geometry change meant new nesting and more grinding time, and hole positions were not repeatable enough for the assembly jig, so parts were being re-drilled.
A WH-3015E fiber laser cutter with a 3000 W source covers this whole plate range on one 1500 x 3000 mm bed: 14 mm carbon steel, 6 mm stainless and 5 mm aluminium alloy. The Raytools auto-focus head resets focal position for each plate instead of relying on the previous setting, and the annealed and aged bed holds 0.03 mm positioning accuracy with 0.01 mm repeat positioning accuracy, which is what makes hole patterns interchangeable across a batch.
The machine is specified against the buyer's actual plate mix rather than the largest available bed, so the source power and working area match the stock already on the floor. Delivery is by sea, air or international express depending on how quickly the line has to start.
The bed is annealed and aged before precision welding to release internal stress. Positioning and repeat positioning accuracy are checked before the machine leaves the workshop, a secondary configuration check is carried out before the machine runs idle, and every additional component is counted before packaging.
Bracket edges come off the bed ready to weld, so the grinding step between cutting and welding is no longer part of the routing. Because repeat positioning accuracy is 0.01 mm, hole patterns stay interchangeable across the batch and parts drop into the assembly jig without re-drilling. New drawings go straight from DXF to cutting with no tooling to order.
Short-run bracket work becomes quotable again, because the cost of a geometry change is a new nest rather than new tooling, and the finishing labour that used to sit behind plasma cutting is removed from the process.
Fiber Laser Cutting Machines
The WH-3015E is a single-platform fiber laser cutter with a 1500 x 3000 mm rated sheet size and a laser source selectable at 1500 W, 2000 W or 3000...
Fiber Laser Cutting Machines
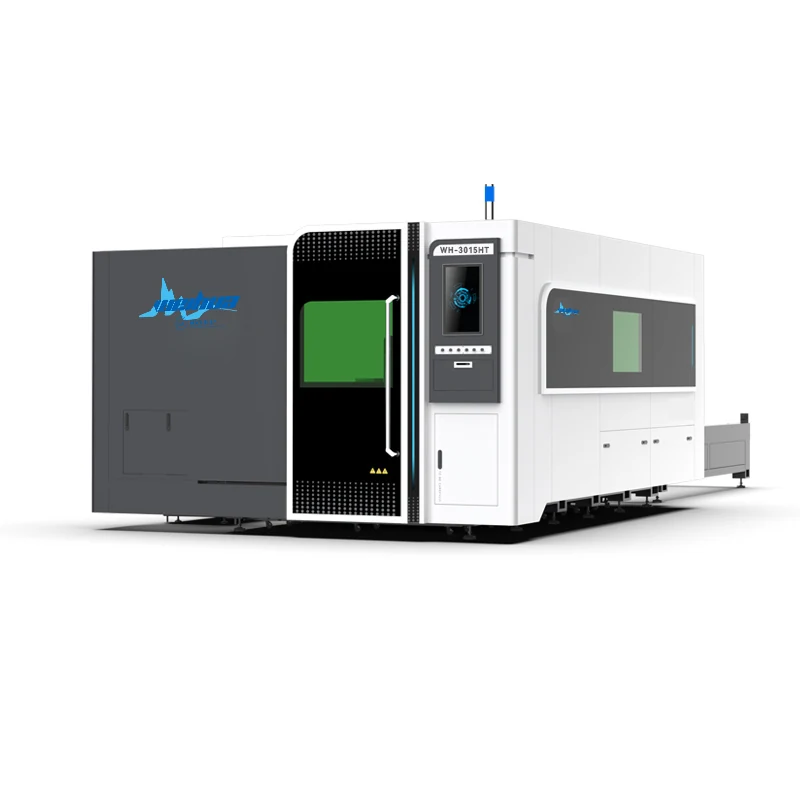
The HT Series is a fully enclosed fiber laser cutter designed to process both metal sheet and pipe on a single machine.
Send a photo or drawing of the part. We will tell you which machine handles it, what it will not do, and what the crate will weigh.