Evaluating Custom
Perforated Aluminum Panel Suppliers
: Bending, Tolerances, and Deburring Standards
When auditing custom metal fabricators, technical execution across these three core fabrication processes serves as the reliable benchmark for quality. Leading manufacturers, such as
Foshan Qi Aluminum Decorative Materials Co., Ltd.
, integrate high-precision CNC machinery and strict quality management (ISO 9001:2015) to maintain consistency across large-scale architectural orders.
1. Bending and Forming Precision
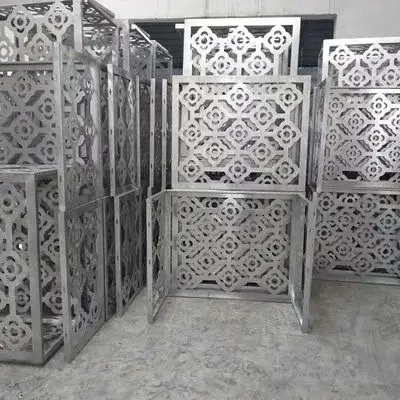
Perforating metal fundamentally alters its structural behavior. When perforated sheet metal undergoes press brake bending, the open hole patterns respond differently than solid metal margins. An experienced supplier must proactively manage these mechanical stresses.
Margin Alignment Along Bend Lines
Bending directly across an open perforation zone distorts hole geometry, resulting in ovaling and uneven flange heights. Advanced fabricators layout panels so primary bend lines fall along solid, unperforated borders.
Springback Control
Aluminum alloys—such as 5052-H32 or 3003-H14—exhibit elasticity and springback during cold forming. Specialized suppliers utilize multi-axis CNC press brakes paired with laser angle-measurement systems to ensure consistent flange angles across 3-meter or 6-meter panel lengths.
Minimum Bend Radii
Overly tight inner radii along the metal grain can induce micro-fractures, particularly on exterior architectural panels exposed to wind loads. Proper tooling selection guarantees bend radii match material grade and sheet thickness (
$t$
).
2. Manufacturing Tolerances & Sheet Flatness
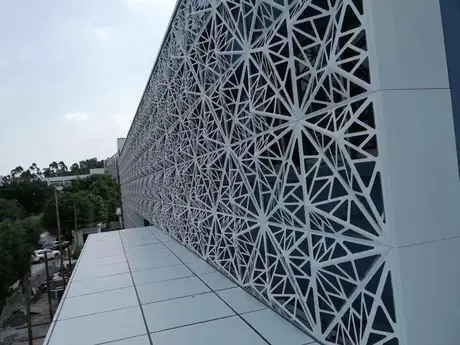
In exterior curtain walls, loose tolerances lead to misaligned shadow lines, joint gaps, and visible oil-canning. When auditing a vendor, compare their factory standards against recognized international quality tiers:
Critical Quality Factor
Punching thousands of holes introduces localized thermal and mechanical stress, causing raw sheets to bow or warp. Industrial producers rely on
heavy-duty multi-roll precision levelers
to eliminate internal stress and restore dead-flat flatness prior to bending and coating.
3. Deburring and Surface Finishing
High-speed turret punching or CNC milling creates burrs on sheet undersides and hole perimeters. Left unaddressed, burrs degrade paint adhesion, impair mechanical fit, and present handling hazards.
Automated Edge Rounding
While basic workshops rely on manual hand-sanding, modern processing lines utilize continuous automated brush deburring systems. These machines apply uniform edge rounding (
$R \ge 0.2\text{ mm}$
) across every perforation edge in a single pass.
Coating Integrity
During curing, liquid PVDF paint and powder coatings naturally pull away from sharp
$90^\circ$
edges due to surface tension. Smoothly rounded edges ensure full paint thickness over hole rims, preventing premature oxidation or filiform corrosion in outdoor environments.
Pre-Treatment Cleanliness
Following deburring, comprehensive degreasing and pre-treatment wash cycles remove micro-fine aluminum powder and punching lubricants, creating a clean substrate for high-performance fluorocarbon (AAMA 2605) or polyester finishes.
Supplier Evaluation Audit Checklist
To verify a fabrication partner during a plant inspection or technical evaluation, consider these direct criteria:
Processing Sequence
Are panels laser-cut or sheared
after
perforation
to ensure exact edge-to-hole margins?
Leveling Technology
Does the facility operate dedicated multi-roll tension levelers to correct sheet distortion post-punching?
Forming Capability
Are press brakes equipped with long-bed CNC control to handle multi-curved or complex hyper-shaped profiles?
Deburring Automation
Is deburring performed using automated brush machines to ensure batch-to-batch consistency?
By enforcing clear benchmarks for forming precision, dimensional tolerance, and deburring quality, project teams can select a custom aluminum fabrication partner capable of delivering clean, structural facade panels tailored to exact engineering specifications.